Sheet Perforating Press
ProductOverview
A sheet perforating press punches a regular field of holes through metal sheet. It carries a tool with many punches arranged in the wanted pattern, and on each stroke all of them shear their holes at once. The sheet then advances by a precise pitch and the press strikes again, so the pattern repeats seamlessly down a strip fed from a coil. Perforated sheet is used for filters and screens, acoustic panels, guards and enclosures, ventilation grilles, walkways, facades, and food and chemical processing, anywhere a sheet needs to pass air, light, liquid, or sound while staying flat and strong.
Sheet feeds from the Uncoiler and Feed through the Servo Roll Feed into the Press Frame and Slide, where the Eccentric Drive drives the slide and the Perforating Tool punches the pattern. The Stripper and Scrap frees the sheet and clears the slugs, the Sheet Leveler flattens the perforated strip, and the Cutoff Shear cuts it to length. The Control System runs the line and the Tool Lubrication system keeps the tool cutting cleanly.
The perforating tool
The tool is what makes this a perforating press rather than a plain stamping press. The Perforating Tool holds many punches, from tens to several hundred, in a Punch Plate arranged to the pattern. Each Punch is a hardened high-speed-steel pin that shears one hole and pushes the slug down into a matching Die Button set into the Die Plate below. The gap between punch and button, the punch clearance, is set to a small fraction of the sheet thickness, because too much clearance tears a rough hole and too little wears the tool fast.
Slender punches would buckle under the punching load, so a Punch Guide Plate plate supports them right down to the sheet face. The whole tool sits in Die Shoe blocks that hold the upper and lower halves in register. Changing the hole pattern, shape, or pitch means changing the tool, so a perforating shop keeps a tool for each pattern it sells: round, square, slotted, hexagonal, or decorative.
Frame, slide, and the punching stroke
Punching hundreds of holes at once is a large, sharp force, so the press is built heavy. The Press Frame and Slide ties a Crown to a Bed with pre-stressed Tie Rod rods so the frame barely flexes under load, which keeps the punches square to the die. The Slide carries the upper tool and runs in adjustable Slide Gib guides; a Overload Protector cushion yields if the tonnage is exceeded so a misfeed cannot wreck the tool.
The Eccentric Drive is a mechanical press drive. A heavy Flywheel stores energy from the Servo Motor and releases it through the Eccentric Shaft and Pitman into the slide, and the Clutch and Brake couples the flywheel for a run and stops the slide at top dead centre. Shut height is set at the pitman so the punches enter the die by the right amount for the sheet thickness.
Feeding to an exact pitch
Pattern quality depends almost entirely on feed accuracy: if the pitch drifts, the fields of holes from successive strokes will not line up. The Servo Roll Feed is a servo roll feed whose Feed Roll rolls advance the sheet by a programmed pitch during the open part of the stroke, timed by the Feed Servo Cam. For the tightest patterns a Pilot Release lets pilots in the tool drop into already-punched holes and pull the sheet to its exact position while the feed grip releases, so the tool, not the feed roll, sets final registration. Upstream, the Uncoiler and Feed keeps a slack Loop Control loop so the steady uncoiler never fights the stepped feed.
Stripping, slug removal, and finishing
As the slide rises the sheet tends to cling to the punches, so the Stripper Plate, loaded by Stripper Spring springs, holds the sheet down and peels it off. The punched slugs fall through the die and land on the Slug Conveyor, which carries them to the Slug Bin for recycling, since slug volume on a dense pattern is large.
Punching dense holes builds stress into the sheet and leaves it wavy, so the Sheet Leveler runs it through a bank of offset Leveling Roll rolls that work the sheet flat. The Cutoff Shear then crops the strip to finished sheet length, its Shear Blade driven across the full width against the Shear Anvil. Sheet can also be recoiled instead of sheared when the customer wants perforated coil.
Materials, variants, and use
The press runs mild steel, stainless, aluminium, brass, and copper, in thickness from thin sheet for fine filter mesh up to several millimetres for heavy screens and walkway. Patterns are described by hole size, shape, and centre spacing, and by open area, the percentage of the sheet that is hole. Light high-speed machines run small holes in thin sheet at high stroke rates for filters and grilles, while heavy presses punch large holes in thick plate for screening and architectural panels. The Tool Lubrication system sprays the strip from Spray Bar nozzles so the punches shear cleanly and stay cool, which lengthens tool life on long runs.
Control and tooling life
The Control System ties the line together. A PLC sets stroke rate and feed pitch, sequences uncoiler, feed, press, strip, level, and shear, and runs the shear to a programmed length. A Tonnage Monitor reads strain on the frame through Pressure Sensor gauges every stroke, because a broken or dull Punch shifts the force signature and the monitor can stop the press before a slug jam damages the rest of the tool. Operators set pattern, pitch, length, and tonnage limits at the LCD Panel. Holding the feed pitch exact and the punches sharp is what keeps a perforated sheet uniform across its full width and down its full length.
Sheet Perforating Press parts and their functions
10 top-level parts · 782 parts in total · full bill of materials below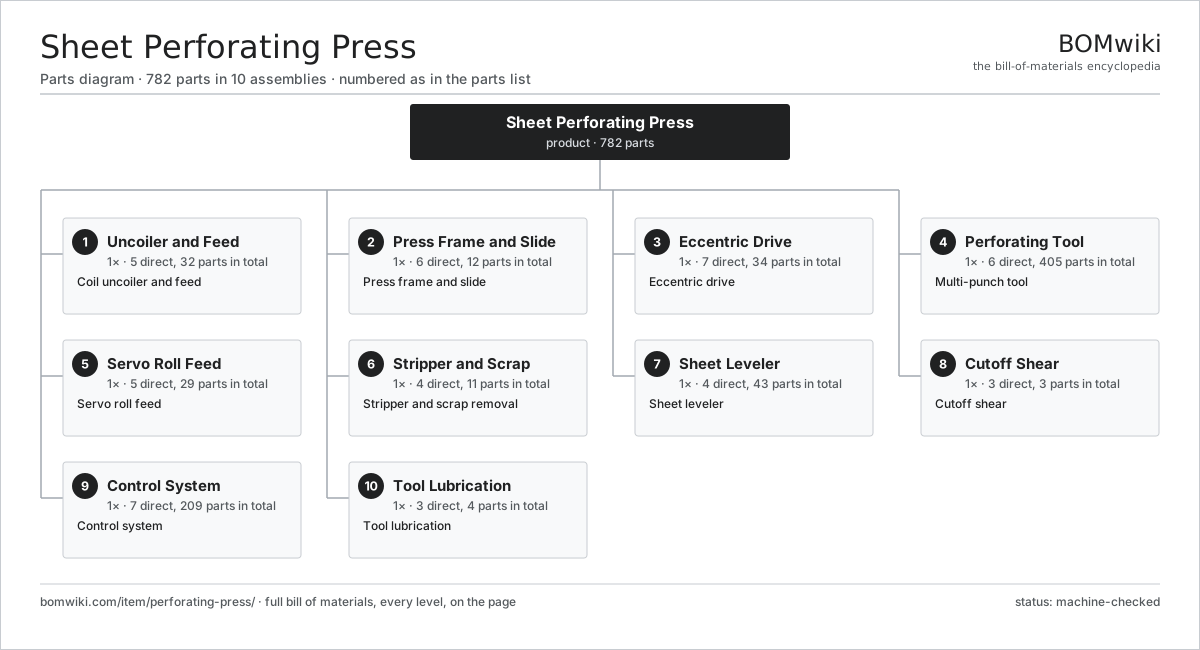
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Uncoiler and Feed 5 parts | 1× | Coil uncoiler and feed |
| 2 | Press Frame and Slide 6 parts | 1× | Press frame and slide |
| 3 | Eccentric Drive 7 parts | 1× | Eccentric drive |
| 4 | Perforating Tool 6 parts | 1× | Multi-punch tool |
| 5 | Servo Roll Feed 5 parts | 1× | Servo roll feed |
| 6 | Stripper and Scrap 4 parts | 1× | Stripper and scrap removal |
| 7 | Sheet Leveler 4 parts | 1× | Sheet leveler |
| 8 | Cutoff Shear 3 parts | 1× | Cutoff shear |
| 9 | Control System 7 parts | 1× | Control system |
| 10 | Tool Lubrication 3 parts | 1× | Tool lubrication |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Sheet Perforating Press
10 top-level lines · 83 rows shown · 782 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Uncoiler and Feed 5 parts | perforating-press-uncoiler | 1× | 1 | 32 | assembly |
| 1.1 | Expanding Mandrel | perforating-press-mandrel | 1× | 1 | · | part |
| 1.2 | Loop Control | perforating-press-loop-pit | 1× | 1 | · | part |
| 1.3 | Pinch Roll | perforating-press-pinch-rolls | 2× | 2 | · | part |
| 1.4 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 1.5 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 1.5.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 1.5.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 1.5.3 | Encoder | encoder | 1× | 1 | · | part |
| 1.5.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 2 | Press Frame and Slide 6 parts | perforating-press-press-frame | 1× | 1 | 12 | assembly |
| 2.1 | Crown | perforating-press-crown | 1× | 1 | · | part |
| 2.2 | Slide | perforating-press-slide | 1× | 1 | · | part |
| 2.3 | Slide Gib | perforating-press-slide-gib | 4× | 4 | · | part |
| 2.4 | Bed | perforating-press-bed | 1× | 1 | · | part |
| 2.5 | Tie Rod | perforating-press-tie-rod | 4× | 4 | · | part |
| 2.6 | Overload Protector | perforating-press-overload | 1× | 1 | · | part |
| 3 | Eccentric Drive 7 parts | perforating-press-drive | 1× | 1 | 34 | assembly |
| 3.1 | Flywheel | perforating-press-flywheel | 1× | 1 | · | part |
| 3.2 | Eccentric Shaft | perforating-press-eccentric-shaft | 1× | 1 | · | part |
| 3.3 | Pitman | perforating-press-pitman | 1× | 1 | · | part |
| 3.4 | Clutch and Brake | perforating-press-clutch-brake | 1× | 1 | · | part |
| 3.5 | Helical Gear Pair | gear-pair | 2× | 2 | · | part |
| 3.6 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 3.6.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 3.6.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 3.6.3 | Encoder | encoder | 1× | 1 | · | part |
| 3.6.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 3.7 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 4 | Perforating Tool 6 parts | perforating-press-perforating-tool | 1× | 1 | 405 | assembly |
| 4.1 | Punch Plate | perforating-press-punch-plate | 1× | 1 | · | part |
| 4.2 | Punch | perforating-press-punch | 200× | 200 | · | part |
| 4.3 | Die Plate | perforating-press-die-plate | 1× | 1 | · | part |
| 4.4 | Die Button | perforating-press-die-button | 200× | 200 | · | part |
| 4.5 | Punch Guide Plate | perforating-press-punch-guide | 1× | 1 | · | part |
| 4.6 | Die Shoe | perforating-press-die-shoe | 2× | 2 | · | part |
| 5 | Servo Roll Feed 5 parts | perforating-press-feed | 1× | 1 | 29 | assembly |
| 5.1 | Feed Roll | perforating-press-feed-roll | 2× | 2 | · | part |
| 5.2 | Feed Servo Cam | perforating-press-feed-servo | 1× | 1 | · | part |
| 5.3 | Pilot Release | perforating-press-pilot-release | 1× | 1 | · | part |
| 5.4 | Helical Gear Pair | gear-pair | 1× | 1 | · | part |
| 5.5 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 5.5.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 5.5.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 5.5.3 | Encoder | encoder | 1× | 1 | · | part |
| 5.5.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 6 | Stripper and Scrap 4 parts | perforating-press-stripper | 1× | 1 | 11 | assembly |
| 6.1 | Stripper Plate | perforating-press-stripper-plate | 1× | 1 | · | part |
| 6.2 | Stripper Spring | perforating-press-stripper-spring | 8× | 8 | · | part |
| 6.3 | Slug Conveyor | perforating-press-slug-conveyor | 1× | 1 | · | part |
| 6.4 | Slug Bin | perforating-press-slug-bin | 1× | 1 | · | part |
| 7 | Sheet Leveler 4 parts | perforating-press-leveler | 1× | 1 | 43 | assembly |
| 7.1 | Leveling Roll | perforating-press-leveler-roll | 9× | 9 | · | part |
| 7.2 | Leveler Frame | perforating-press-leveler-frame | 1× | 1 | · | part |
| 7.3 | Ball Bearing | ball-bearing | 9× | 9 | · | part |
| 7.4 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 7.4.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 7.4.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 7.4.3 | Encoder | encoder | 1× | 1 | · | part |
| 7.4.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 8 | Cutoff Shear 3 parts | perforating-press-shear | 1× | 1 | 3 | assembly |
| 8.1 | Shear Blade | perforating-press-shear-blade | 1× | 1 | · | part |
| 8.2 | Shear Cylinder | perforating-press-shear-cylinder | 1× | 1 | · | part |
| 8.3 | Shear Anvil | perforating-press-shear-anvil | 1× | 1 | · | part |
| 9 | Control System 7 parts | perforating-press-control | 1× | 1 | 209 | assembly |
| 9.1 | PLC 3 parts | perforating-press-plc | 1× | 1 | 122 | assembly |
| 9.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 9.1.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 9.1.3 | SMD Passive (R/C/L) | smd-passives | 120× | 120 | · | part |
| 9.2 | Tonnage Monitor 4 parts | perforating-press-tonnage-monitor | 1× | 1 | 64 | assembly |
| 9.2.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 9.2.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 9.2.3 | Pressure Sensor | pressure-sensor | 2× | 2 | · | part |
| 9.2.4 | SMD Passive (R/C/L) | smd-passives | 60× | 60 | · | part |
| 9.3 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 9.4 | Power Supply | power-supply | 1× | 1 | · | part |
| 9.5 | Relay | relay | 8× | 8 | · | part |
| 9.6 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 9.7 | Connector | connector | 12× | 12 | · | part |
| 10 | Tool Lubrication 3 parts | perforating-press-lube | 1× | 1 | 4 | assembly |
| 10.1 | Lube Pump | perforating-press-lube-pump | 1× | 1 | · | part |
| 10.2 | Spray Bar | perforating-press-spray-bar | 2× | 2 | · | part |
| 10.3 | Lube Tank | perforating-press-lube-tank | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Bed-Type Milling Machine
151 parts · shares 3 with this page
 Bevel Gear Generator
201 parts · shares 3 with this page
Billet Heating Furnace
358 parts · shares 3 with this page
Centering and Facing Machine
1,419 parts · shares 3 with this page
 Centerless Grinder
129 parts · shares 3 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
1,048-word article