Multi-Blanking Line
ProductOverview
A multi-blanking line turns a heavy steel coil into a stack of square-cut rectangular blanks in one continuous pass. It combines two jobs that older shops ran on separate machines: slitting, which splits the wide strip into narrow lanes lengthwise, and cut-to-length, which crops those lanes into blanks of a set length. Because both happen on one line, a single coil becomes a finished pile of blanks ready for a press, a laser, or a forming line without a second handling step. The strip threads through the line in order: it pays off the Uncoiler, is flattened in the Straightener, split into lanes by the Slitter Head, buffered in the Loop Accumulator, metered by the Servo Roll Feed, cropped at the Cutoff Shear, and caught by the Blank Stacker. The Line Control sequences the whole line and the Hydraulic Power Unit supply the high-force cylinders.
Uncoiling and levelling
The coil is loaded by the Coil Car, which lifts it on a V-Saddle and aligns the bore to the Expanding Mandrel. That mandrel is segmented: a Expansion Wedge driven by the Expansion Cylinder pushes four Mandrel Segment shoes outward until they grip the coil inner diameter. A Peeler Arm pries up the loose coil end to start threading and the Hold-Down Roll stops the coil from snapping open. The Uncoiler Drive pays the strip off under torque control so it never sags or pulls tight.
Coil steel arrives with set and crossbow, a memory of the curve it was wound on. The Straightener removes that memory by bending the strip back and forth between many small Work Roll rolls supported by larger Backup Roll rolls. The bends push the outer fibres of the strip past their yield point so the strip leaves flat. A Gap Actuator sets how deeply the upper roll bank penetrates, which is the main control over flatness, and the Leveller Drive both turns the rolls and pulls strip from the uncoiler.
Slitting into lanes
The Slitter Head splits the flat strip into parallel lanes. Two Slitter Arbor shafts carry stacks of Circular Knife knives separated by ground Arbor Spacer rings. Each upper and lower knife pair overlaps slightly, so the strip is sheared, not torn, along each lane edge. The width of each lane is set entirely by the spacer stack, so changing product width means restacking the arbors. Stripper Ring rubber rings lift the slit strip off the knives and the Overarm Separator holds the lanes apart afterward. The Slitter Drive turns both arbors at matched surface speed so the lanes do not stretch or buckle.
Buffering, feeding, and shearing
Slitting runs best at constant speed, but the shear must stop the strip dead for each cut. The Loop Accumulator reconciles the two: it holds a free loop of strip whose depth is watched by a Loop Sensor over Loop Guide Roll guide rolls. The upstream section feeds the loop continuously while the downstream section draws from it in stops and starts. Below the loop, the Servo Roll Feed uses a Feed Servo to drive Feed Roll pinch rolls a precise distance, the blank length, then halts. A Length Encoder measuring wheel checks the fed length, and the Pinch Cylinder lifts the roll to let the strip relax during the cut.
The Cutoff Shear crops the metered strip. A heavy Shear Frame carries the Shear Cylinder cylinders that drive a raked Upper Blade down against the fixed Lower Blade. The rake means the blade enters at one edge and shears progressively across the width, which cuts the peak force the line must supply. A Blade Gap Screw sets blade clearance for each gauge, and a Scrap Chopper cuts trimmed edge waste into short pieces for the scrap bin.
Stacking and control
Each finished blank lands on the Blank Stacker. A Magnetic Conveyor holds the blank flat and slows it, then drops it onto the Drop Table. That table is a scissor lift on Scissor Leg legs that lowers one blank thickness per cut through its Table Cylinder, so the drop height stays constant as the pile grows. Side Jogger paddles and a Back Stop tap the pile square on every side, leaving a neat stack a forklift can move.
The Line Control ties the line together. A Line PLC holds the cut-length recipe, counts blanks, and runs the interlocks; the Drive Cabinet houses the Servo Amplifier amplifiers that power the line motors; and the operator sets blank size and quantity at the Operator HMI. Safety is handled by a Safety Relay and Light Curtain barriers that stop motion if anyone reaches into the shear zone.
Hydraulics, materials, and use
The high-force jobs of clamping the mandrel and driving the shear run on the Hydraulic Power Unit. A Hydraulic Pump feeds a Valve Manifold manifold of Directional Valve valves, a Relief Valve caps the pressure, and an Accumulator stores a burst of oil so the shear stroke is fast and crisp. An Oil Cooler holds oil temperature steady. The cutting parts are made from hardened tool steel because they wear against coil all day, while frames are heavy welded steel that stays rigid under load. Multi-blanking lines feed appliance, automotive, and HVAC plants that need flat, accurately sized blanks in volume, replacing the slower route of slitting a coil first and shearing the lanes on a separate machine later.
Multi-Blanking Line parts and their functions
9 top-level parts · 492 parts in total · full bill of materials below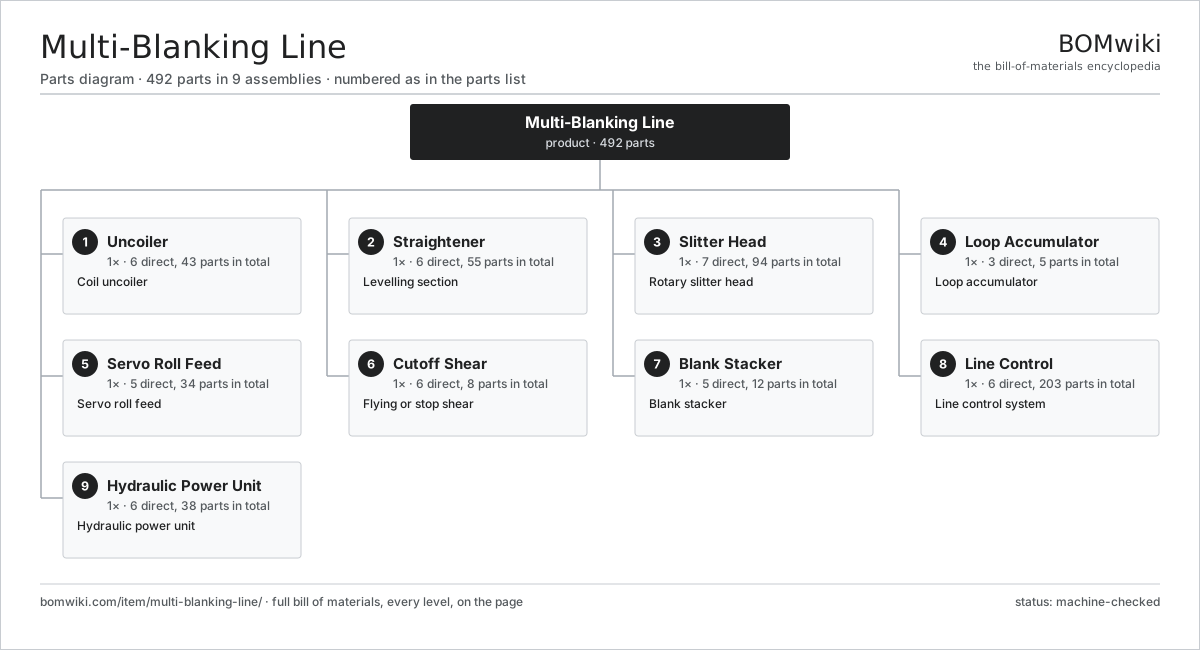
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Uncoiler 6 parts | 1× | Coil uncoiler |
| 2 | Straightener 6 parts | 1× | Levelling section |
| 3 | Slitter Head 7 parts | 1× | Rotary slitter head |
| 4 | Loop Accumulator 3 parts | 1× | Loop accumulator |
| 5 | Servo Roll Feed 5 parts | 1× | Servo roll feed |
| 6 | Cutoff Shear 6 parts | 1× | Flying or stop shear |
| 7 | Blank Stacker 5 parts | 1× | Blank stacker |
| 8 | Line Control 6 parts | 1× | Line control system |
| 9 | Hydraulic Power Unit 6 parts | 1× | Hydraulic power unit |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Multi-Blanking Line
9 top-level lines · 98 rows shown · 492 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Uncoiler 6 parts | multi-blanking-line-uncoiler | 1× | 1 | 43 | assembly |
| 1.1 | Expanding Mandrel 4 parts | multi-blanking-line-mandrel | 1× | 1 | 7 | assembly |
| 1.1.1 | Mandrel Segment | multi-blanking-line-mandrel-segment | 4× | 4 | · | part |
| 1.1.2 | Expansion Wedge | multi-blanking-line-mandrel-wedge | 1× | 1 | · | part |
| 1.1.3 | Expansion Cylinder | multi-blanking-line-mandrel-cylinder | 1× | 1 | · | part |
| 1.1.4 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 1.2 | Coil Car 3 parts | multi-blanking-line-coil-car | 1× | 1 | 3 | assembly |
| 1.2.1 | V-Saddle | multi-blanking-line-coil-saddle | 1× | 1 | · | part |
| 1.2.2 | Lift Cylinder | multi-blanking-line-lift-cylinder | 1× | 1 | · | part |
| 1.2.3 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 1.3 | Peeler Arm | multi-blanking-line-peeler | 1× | 1 | · | part |
| 1.4 | Hold-Down Roll | multi-blanking-line-holddown | 1× | 1 | · | part |
| 1.5 | Uncoiler Drive 4 parts | multi-blanking-line-uncoiler-drive | 1× | 1 | 27 | assembly |
| 1.5.1 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 1.5.2 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 1.5.3 | Helical Gear Pair | gear-pair | 1× | 1 | · | part |
| 1.5.4 | Brake Disc (rotor) | brake-disc | 1× | 1 | · | part |
| 1.6 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 2 | Straightener 6 parts | multi-blanking-line-straightener | 1× | 1 | 55 | assembly |
| 2.1 | Leveller Frame | multi-blanking-line-leveller-frame | 1× | 1 | · | part |
| 2.2 | Work Roll | multi-blanking-line-work-roll | 11× | 11 | · | part |
| 2.3 | Backup Roll | multi-blanking-line-backup-roll | 6× | 6 | · | part |
| 2.4 | Gap Actuator | multi-blanking-line-gap-actuator | 2× | 2 | · | part |
| 2.5 | Leveller Drive 3 parts | multi-blanking-line-leveller-drive | 1× | 1 | 27 | assembly |
| 2.5.1 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 2.5.2 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 2.5.3 | Helical Gear Pair | gear-pair | 2× | 2 | · | part |
| 2.6 | Ball Bearing | ball-bearing | 8× | 8 | · | part |
| 3 | Slitter Head 7 parts | multi-blanking-line-slitter | 1× | 1 | 94 | assembly |
| 3.1 | Slitter Arbor | multi-blanking-line-slitter-arbor | 2× | 2 | · | part |
| 3.2 | Circular Knife | multi-blanking-line-circular-knife | 24× | 24 | · | part |
| 3.3 | Arbor Spacer | multi-blanking-line-spacer | 22× | 22 | · | part |
| 3.4 | Stripper Ring | multi-blanking-line-stripper-ring | 12× | 12 | · | part |
| 3.5 | Overarm Separator | multi-blanking-line-overarm | 1× | 1 | · | part |
| 3.6 | Slitter Drive 3 parts | multi-blanking-line-slitter-drive | 1× | 1 | 27 | assembly |
| 3.6.1 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 3.6.2 | Helical Gear Pair | gear-pair | 2× | 2 | · | part |
| 3.6.3 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 3.7 | Ball Bearing | ball-bearing | 6× | 6 | · | part |
| 4 | Loop Accumulator 3 parts | multi-blanking-line-loop-pit | 1× | 1 | 5 | assembly |
| 4.1 | Loop Guide Roll | multi-blanking-line-loop-pit-roll | 2× | 2 | · | part |
| 4.2 | Loop Sensor | multi-blanking-line-loop-sensor | 2× | 2 | · | part |
| 4.3 | Pit Liner | multi-blanking-line-pit-liner | 1× | 1 | · | part |
| 5 | Servo Roll Feed 5 parts | multi-blanking-line-feed | 1× | 1 | 34 | assembly |
| 5.1 | Feed Roll | multi-blanking-line-feed-roll | 2× | 2 | · | part |
| 5.2 | Feed Servo 2 parts | multi-blanking-line-feed-servo | 1× | 1 | 25 | assembly |
| 5.2.1 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 5.2.2 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 5.3 | Pinch Cylinder | multi-blanking-line-pinch-cylinder | 2× | 2 | · | part |
| 5.4 | Length Encoder | multi-blanking-line-encoder | 1× | 1 | · | part |
| 5.5 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 6 | Cutoff Shear 6 parts | multi-blanking-line-shear | 1× | 1 | 8 | assembly |
| 6.1 | Shear Frame | multi-blanking-line-shear-frame | 1× | 1 | · | part |
| 6.2 | Upper Blade | multi-blanking-line-upper-blade | 1× | 1 | · | part |
| 6.3 | Lower Blade | multi-blanking-line-lower-blade | 1× | 1 | · | part |
| 6.4 | Shear Cylinder | multi-blanking-line-shear-cylinder | 2× | 2 | · | part |
| 6.5 | Blade Gap Screw | multi-blanking-line-blade-gap-screw | 2× | 2 | · | part |
| 6.6 | Scrap Chopper | multi-blanking-line-scrap-chopper | 1× | 1 | · | part |
| 7 | Blank Stacker 5 parts | multi-blanking-line-stacker | 1× | 1 | 12 | assembly |
| 7.1 | Magnetic Conveyor | multi-blanking-line-magnetic-belt | 1× | 1 | · | part |
| 7.2 | Drop Table 3 parts | multi-blanking-line-drop-table | 1× | 1 | 6 | assembly |
| 7.2.1 | Scissor Leg | multi-blanking-line-scissor-leg | 4× | 4 | · | part |
| 7.2.2 | Table Cylinder | multi-blanking-line-table-cylinder | 1× | 1 | · | part |
| 7.2.3 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 7.3 | Side Jogger | multi-blanking-line-side-jogger | 2× | 2 | · | part |
| 7.4 | Back Stop | multi-blanking-line-back-stop | 1× | 1 | · | part |
| 7.5 | Drive Belt | drive-belt | 2× | 2 | · | part |
| 8 | Line Control 6 parts | multi-blanking-line-control | 1× | 1 | 203 | assembly |
| 8.1 | Line PLC 4 parts | multi-blanking-line-plc | 1× | 1 | 161 | assembly |
| 8.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.1.2 | Microcontroller | mcu | 2× | 2 | · | part |
| 8.1.3 | Relay | relay | 8× | 8 | · | part |
| 8.1.4 | SMD Passive (R/C/L) | smd-passives | 150× | 150 | · | part |
| 8.2 | Drive Cabinet 4 parts | multi-blanking-line-drive-cabinet | 1× | 1 | 35 | assembly |
| 8.2.1 | Servo Amplifier | multi-blanking-line-servo-amp | 4× | 4 | · | part |
| 8.2.2 | Power Supply | power-supply | 1× | 1 | · | part |
| 8.2.3 | Power MOSFET | mosfet | 24× | 24 | · | part |
| 8.2.4 | DC-Link Capacitor | dc-link-cap | 6× | 6 | · | part |
| 8.3 | Operator HMI 3 parts | multi-blanking-line-hmi | 1× | 1 | 3 | assembly |
| 8.3.1 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 8.3.2 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.3.3 | Microcontroller | mcu | 1× | 1 | · | part |
| 8.4 | Safety Relay | multi-blanking-line-safety-relay | 1× | 1 | · | part |
| 8.5 | Light Curtain | multi-blanking-line-light-curtain | 2× | 2 | · | part |
| 8.6 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 9 | Hydraulic Power Unit 6 parts | multi-blanking-line-hydraulics | 1× | 1 | 38 | assembly |
| 9.1 | Hydraulic Pump 3 parts | multi-blanking-line-hyd-pump | 1× | 1 | 27 | assembly |
| 9.1.1 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 9.1.2 | Pump Cartridge | multi-blanking-line-pump-cartridge | 1× | 1 | · | part |
| 9.1.3 | Oil Seal | oil-seal | 2× | 2 | · | part |
| 9.2 | Oil Reservoir | multi-blanking-line-hyd-tank | 1× | 1 | · | part |
| 9.3 | Valve Manifold 3 parts | multi-blanking-line-valve-block | 1× | 1 | 6 | assembly |
| 9.3.1 | Directional Valve | multi-blanking-line-directional-valve | 4× | 4 | · | part |
| 9.3.2 | Relief Valve | multi-blanking-line-relief-valve | 1× | 1 | · | part |
| 9.3.3 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 9.4 | Accumulator | multi-blanking-line-accumulator | 1× | 1 | · | part |
| 9.5 | Oil Cooler | multi-blanking-line-oil-cooler | 1× | 1 | · | part |
| 9.6 | Pressure Sensor | pressure-sensor | 2× | 2 | · | part |
Related products
same domain, ranked by shared parts Servo Stamping Press
633 parts · shares 4 with this page
 Industrial TIG Welder
492 parts · shares 4 with this page
 Railway Wheel Lathe
1,201 parts · shares 7 with this page
Twin-Column Vertical Turret Lathe
1,387 parts · shares 5 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
1,076-word article