Rotary-Table Surface Grinder
ProductOverview
A rotary-table surface grinder finishes flat faces by spinning the work under the wheel instead of sliding it back and forth. The Rotary Table and Chuck is a horizontal magnetic chuck, 300 to 2000 mm across, that holds a ring of round or flat parts and turns them at 5 to 150 rpm. As the table rotates, every part passes under the Grinding Wheelhead many times per minute, so the wheel sees a continuous stream of work rather than a single reciprocating part. That continuous presentation is what makes the machine fast: a full table of seal faces, valve plates, gears, or ceramic substrates is ground in one loading. The Column and Down-Feed Slide lowers the wheel into the parts in small increments, and the amount taken off is metered by the down-feed slide across many revolutions of the table. Flatness of 2 to 5 µm across the whole table and part-to-part parallelism of a few microns are normal production results.
How it works
Two arrangements share the name. A vertical-spindle machine carries a large cup wheel or a ring of abrasive segments whose flat annular face sits parallel to the table. The wheel covers a wide arc of contact, so it removes stock quickly, often a millimetre or more per setup, and it is the type used for roughing flat batches of parts. A horizontal-spindle rotary machine carries a peripheral wheel that touches the work along a narrow line as the table turns beneath it; it removes less per pass but leaves a finer finish and is preferred for precision flatness work. In both, the Table Drive sets table rpm and the Z Down-Feed Slide sets the down-feed. The product of the two, plus the wheel width, fixes the material removal rate. At the end of a cycle the down-feed stops advancing and the table runs several more revolutions of spark-out, letting the machine grind out its own deflection so the final face is flat rather than dished.
Work holding
Holding is the reason these machines suit round parts. The Rotary Magnetic Chuck is an electromagnetic or permanent-magnetic chuck whose pole face pulls every ferrous part down flat against the grinding force, with no clamps to obstruct the wheel and no fixture to set up per part. Excitation current reaches the spinning chuck through the Rotary Coupling, and the Chuck Controller sets holding force and runs a controlled demagnetising cycle so finished parts lift off without residual magnetism that would attract swarf in later operations. Non-ferrous and ceramic parts are held in pockets or with adhesive instead, since the magnet has nothing to grip. The Table Platter under the chuck is ground flat and true to a few microns, because any runout in the platter is copied straight onto the faces of the parts it carries.
Structure and accuracy
Grinding forces are modest but the process is sensitive to vibration, heat, and squareness. The Machine Bed is grey iron at 2 to 15 t, sized by table diameter, and its mass damps the regenerative chatter that otherwise prints waviness onto a face. The Table Bearing supporting the platter must run with very low axial runout, since its wobble is the floor on achievable flatness. The Column Casting holds the wheel square over the table, and its squareness governs how parallel the ground face is to the held face. A Wheelhead Counterbalance offloads the wheelhead weight from the ball screw so down-feed resolution of half a micron is not lost to backlash under gravity. Heat is the main size error: the Coolant System system floods the wide contact zone, the Filter Unit strips grit that would scratch the finish, and the Coolant Chiller holds coolant within about a degree so the table and column do not grow during a shift.
Wheels and dressing
The wheel is consumable and must be kept flat. Vitrified aluminium-oxide suits steel and cast iron, while CBN segments are used for hardened and high-volume work because they hold their form far longer. The Wheel Dressing Unit traverses a Dressing Diamond across the wheel face to renew sharp grain and true the face parallel to the table. On segmental wheels the dresser also levels the ring after a worn segment is replaced in the Wheel Flange and Segment Holder. Every dress removes wheel material, so the CNC Control compensates the down-feed position automatically to hold finished thickness across the life of the wheel.
Use and variants
The machine earns its place in batch flat-finishing of round and disc-shaped parts: mechanical seal faces, hydraulic valve plates, clutch and brake discs, gear blanks, turbine and compressor blade roots, magnetic-disc substrates, and ceramic plates. Small machines with a 300 mm chuck serve toolrooms; large machines with a 2000 mm chuck run production cells fed by the Load/Unload Interface. Where a part path is wider than the wheel, or a profile must be plunged, a Cross-Traverse Slide adds radial motion. The economics favour volume: load a full table once, grind every part to the same flatness in one cycle, then index the table clear and load the next batch.
Rotary-Table Surface Grinder parts and their functions
7 top-level parts · 172 parts in total · full bill of materials below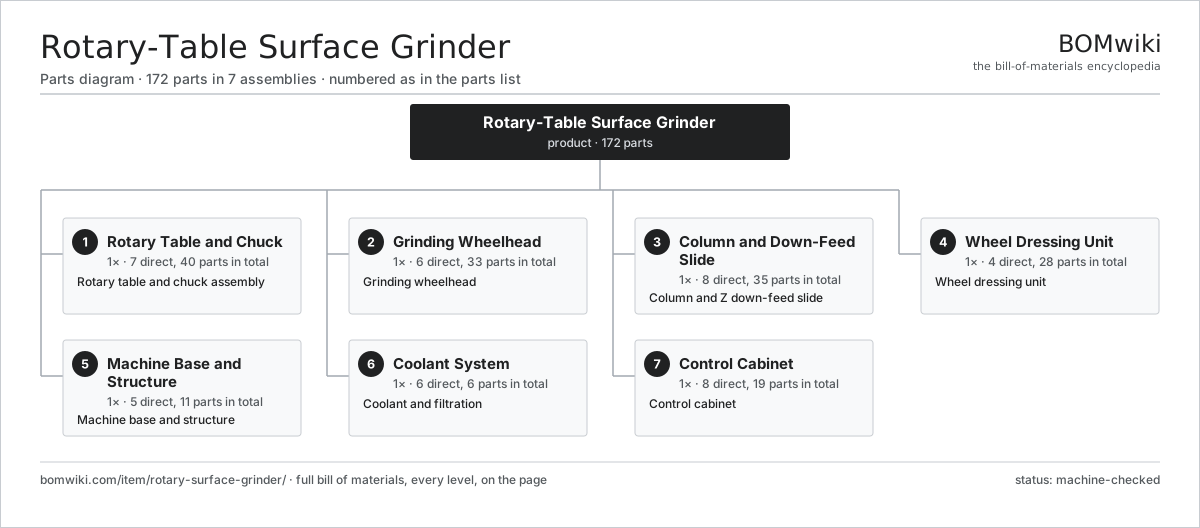
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Rotary Table and Chuck 7 parts | 1× | Rotary table and chuck assembly |
| 2 | Grinding Wheelhead 6 parts | 1× | Grinding wheelhead |
| 3 | Column and Down-Feed Slide 8 parts | 1× | Column and Z down-feed slide |
| 4 | Wheel Dressing Unit 4 parts | 1× | Wheel dressing unit |
| 5 | Machine Base and Structure 5 parts | 1× | Machine base and structure |
| 6 | Coolant System 6 parts | 1× | Coolant and filtration |
| 7 | Control Cabinet 8 parts | 1× | Control cabinet |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Rotary-Table Surface Grinder
7 top-level lines · 86 rows shown · 172 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Rotary Table and Chuck 7 parts | rotary-surface-grinder-table | 1× | 1 | 40 | assembly |
| 1.1 | Rotary Magnetic Chuck | rotary-surface-grinder-chuck | 1× | 1 | · | part |
| 1.2 | Table Platter | rotary-surface-grinder-table-platter | 1× | 1 | · | part |
| 1.3 | Table Bearing 2 parts | rotary-surface-grinder-table-bearing | 1× | 1 | · | part |
| 1.3.1 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 1.3.2 | Oil Seal | oil-seal | 2× | 2 | · | part |
| 1.4 | Table Drive 4 parts | rotary-surface-grinder-table-drive | 1× | 1 | · | part |
| 1.4.1 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 1.4.2 | Helical Gear Pair | gear-pair | 1× | 1 | · | part |
| 1.4.3 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 1.4.4 | Encoder | encoder | 1× | 1 | · | part |
| 1.5 | Chuck Controller 3 parts | rotary-surface-grinder-chuck-controller | 1× | 1 | · | part |
| 1.5.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 1.5.2 | IGBT Power Module | igbt-module | 1× | 1 | · | part |
| 1.5.3 | SMD Passive (R/C/L) | smd-passives | 1× | 1 | · | part |
| 1.6 | Rotary Coupling | rotary-surface-grinder-slip-ring | 1× | 1 | · | part |
| 1.7 | Table Seal 2 parts | rotary-surface-grinder-table-seal | 1× | 1 | · | part |
| 1.7.1 | Oil Seal | oil-seal | 2× | 2 | · | part |
| 1.7.2 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 2 | Grinding Wheelhead 6 parts | rotary-surface-grinder-wheelhead | 1× | 1 | 33 | assembly |
| 2.1 | Grinding Wheel | rotary-surface-grinder-wheel | 1× | 1 | · | part |
| 2.2 | Wheel Spindle 2 parts | rotary-surface-grinder-spindle | 1× | 1 | · | part |
| 2.2.1 | Ball Bearing | ball-bearing | 3× | 3 | · | part |
| 2.2.2 | Oil Seal | oil-seal | 2× | 2 | · | part |
| 2.3 | Wheel Motor 2 parts | rotary-surface-grinder-wheel-motor | 1× | 1 | · | part |
| 2.3.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 2.3.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 2.4 | Wheel Flange and Segment Holder | rotary-surface-grinder-wheel-flange | 1× | 1 | · | part |
| 2.5 | Wheel Guard 2 parts | rotary-surface-grinder-wheel-guard | 1× | 1 | · | part |
| 2.5.1 | Sheet Metal Panel | sheet-panel | 2× | 2 | · | part |
| 2.5.2 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 2.6 | Drive Belt | drive-belt | 1× | 1 | · | part |
| 3 | Column and Down-Feed Slide 8 parts | rotary-surface-grinder-column | 1× | 1 | 35 | assembly |
| 3.1 | Column Casting | rotary-surface-grinder-column-casting | 1× | 1 | · | part |
| 3.2 | Z Down-Feed Slide | rotary-surface-grinder-z-slide | 1× | 1 | · | part |
| 3.3 | Ball Screw | ball-screw | 1× | 1 | · | part |
| 3.4 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 3.5 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 3.5.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 3.5.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 3.5.3 | Encoder | encoder | 1× | 1 | · | part |
| 3.5.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 3.6 | Encoder | encoder | 1× | 1 | · | part |
| 3.7 | Wheelhead Counterbalance 1 parts | rotary-surface-grinder-counterbalance | 1× | 1 | · | part |
| 3.7.1 | Coil Spring | coil-spring | 2× | 2 | · | part |
| 3.8 | Cross-Traverse Slide 2 parts | rotary-surface-grinder-cross-slide | 1× | 1 | · | part |
| 3.8.1 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 3.8.2 | Ball Screw | ball-screw | 1× | 1 | · | part |
| 4 | Wheel Dressing Unit 4 parts | rotary-surface-grinder-dresser | 1× | 1 | 28 | assembly |
| 4.1 | Dresser Arm | rotary-surface-grinder-dress-arm | 1× | 1 | · | part |
| 4.2 | Dressing Diamond | rotary-surface-grinder-diamond | 1× | 1 | · | part |
| 4.3 | Dresser Slide 2 parts | rotary-surface-grinder-dress-slide | 1× | 1 | · | part |
| 4.3.1 | Ball Screw | ball-screw | 1× | 1 | · | part |
| 4.3.2 | Linear Guide Rail | linear-guide | 1× | 1 | · | part |
| 4.4 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 4.4.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 4.4.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 4.4.3 | Encoder | encoder | 1× | 1 | · | part |
| 4.4.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 5 | Machine Base and Structure 5 parts | rotary-surface-grinder-base | 1× | 1 | 11 | assembly |
| 5.1 | Machine Bed | rotary-surface-grinder-bed | 1× | 1 | · | part |
| 5.2 | Leveling Mount | rotary-surface-grinder-leveling | 4× | 4 | · | part |
| 5.3 | Machine Enclosure 1 parts | rotary-surface-grinder-enclosure | 1× | 1 | · | part |
| 5.3.1 | Sheet Metal Panel | sheet-panel | 4× | 4 | · | part |
| 5.4 | Load/Unload Interface | rotary-surface-grinder-loader | 1× | 1 | · | part |
| 5.5 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 6 | Coolant System 6 parts | rotary-surface-grinder-coolant | 1× | 1 | 6 | assembly |
| 6.1 | Coolant Pump | coolant-pump | 1× | 1 | · | part |
| 6.2 | Coolant Tank | rotary-surface-grinder-coolant-tank | 1× | 1 | · | part |
| 6.3 | Filter Unit | rotary-surface-grinder-filter-unit | 1× | 1 | · | part |
| 6.4 | Coolant Nozzles | rotary-surface-grinder-coolant-nozzles | 1× | 1 | · | part |
| 6.5 | Coolant Chiller 1 parts | rotary-surface-grinder-chiller | 1× | 1 | · | part |
| 6.5.1 | Heating Element | heating-element | 1× | 1 | · | part |
| 6.6 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 7 | Control Cabinet 8 parts | rotary-surface-grinder-controls | 1× | 1 | 19 | assembly |
| 7.1 | CNC Control 3 parts | rotary-surface-grinder-cnc | 1× | 1 | · | part |
| 7.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 7.1.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 7.1.3 | SMD Passive (R/C/L) | smd-passives | 1× | 1 | · | part |
| 7.2 | Operator HMI | rotary-surface-grinder-hmi | 1× | 1 | · | part |
| 7.3 | Power Supply | power-supply | 1× | 1 | · | part |
| 7.4 | IGBT Power Module | igbt-module | 2× | 2 | · | part |
| 7.5 | Relay | relay | 4× | 4 | · | part |
| 7.6 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 7.7 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 7.8 | Connector | connector | 6× | 6 | · | part |
Related products
same domain, ranked by shared parts Crankshaft Grinder
511 parts · shares 10 with this page
Spline Rolling Machine
138 parts · shares 11 with this page
 Bevel Gear Generator
201 parts · shares 11 with this page
Camshaft Grinder
489 parts · shares 9 with this page
 Radial Forging Machine
288 parts · shares 11 with this page
Double-Disc Grinder
153 parts · shares 10 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
911-word article