Blanking Press Line
ProductOverview
A blanking press line takes a coil of flat metal strip and shears it into a steady stream of flat blanks, the simple cut-out shapes that feed downstream forming presses. Blanking is the first operation in most sheet-metal parts: a car door skin, an appliance panel, or a bracket starts as a blank cut to a profile, and only later is it drawn, bent, or stamped into shape. The line exists because feeding loose sheets one at a time is slow and wasteful, while a coil holds a long continuous run that can be unwound, flattened, fed, and cut without an operator touching each piece.
The line is a sequence of stations. The Coil Handling loads a coil and pays the strip off. The Straightener flattens the curl out of it. The Loop Control holds a slack loop so the smooth pay-off and the start-stop feed do not fight each other. The Servo Roll Feed pulls a measured length of strip into the Blanking Press, which drives the Blanking Die Set through the strip to shear out a blank. The Blank Stacker stacks the blanks, the Scrap Handling disposes of the leftover web, and the Line Control keeps all of it in step.
Coil handling and straightening
A coil arrives as tightly wound strip, often weighing many tonnes, and it carries a strong curl from being wound. A Coil Car with a V-saddle lifts the coil and rolls it onto the Decoiler. The decoiler uses a Expanding Mandrel whose Mandrel Segment wedges press outward against the coil bore to grip it, so the coil turns with the mandrel rather than slipping. A double-mandrel decoiler holds two coils, so a fresh one can be loaded while the running coil pays out, which avoids a long stop at every coil change. A Peeler Arm presses on the coil with a Hold-down Roller and lifts the loose lead end with a Peeler Blade, threading it into the next station.
The strip still has coil set, a lengthwise curve, and often edge wave or crossbow. The Straightener removes these. Driven Entry Pinch Roll units push the strip into a stack of small Work Roll rolls offset above and below each other. The strip is forced to bend back and forth over these rolls, which works the metal past its yield point repeatedly and leaves it flat. Because the work rolls are slim and would deflect under load, a row of Backup Roll rolls sits behind them. The whole stack lives in a Roll Cassette that can be pulled and swapped when the strip gauge changes, and Gap Screw jacks set the roll gap to the thickness in use.
Feed and shearing
Strip flows off the decoiler at a roughly steady rate, but the press feeds in quick bursts between strokes. The Loop Pit absorbs the mismatch by holding a free hanging loop of strip; a Loop Sensor watches the loop depth and tells the decoiler to speed up or slow down so the loop never runs out or piles to the floor.
The Servo Roll Feed does the precise work. A Feed Roll pair driven by a Feed Servo advances the strip exactly one blank pitch per stroke, the progression, to a typical accuracy of a few hundredths of a millimetre. A Release Cam lifts the upper feed roll for an instant so the die's Pilot Pin pins can pull the strip into final register before the cut, removing any small feed error.
Shearing itself is a clean mechanical event. As the Slide descends, the Blanking Punch is driven into the strip against the opening in the Die Plate. With the right clearance between punch and die, usually a few percent of the strip thickness, the metal does not tear randomly: it deforms, then a crack starts at the punch edge and a matching crack at the die edge, and the two meet to separate the blank cleanly. The Stripper Plate holds the strip flat during the cut and then strips it off the punch as the slide rises.
The press and its drive
In a mechanical line the press is a crank machine. A Main Motor spins a heavy Flywheel up to speed; the flywheel stores energy so the motor does not have to supply the whole punching peak in the brief instant of the cut. A Clutch-Brake couples the flywheel to the Eccentric Shaft for one stroke and then brakes the slide at the top. The eccentric's throw, carried through the Connecting Rod rods, converts rotation into the slide's up-and-down stroke. Gib strips guide the slide and keep it square against off-center cutting loads, and Counterbalance Cylinder cylinders carry the slide and tooling weight off the rods.
Materials, variants, and use
Lines run mild steel, high-strength steel, aluminium, brass, and stainless, in thicknesses from thin 0.5 mm sheet up to 3 mm plate, at coil widths reaching about 2000 mm. Tonnage is sized to the cut: blanking force scales with the cut perimeter, the strip thickness, and the shear strength of the metal, so a long or thick profile in strong steel needs a larger press, commonly 300 to 1000 tonnes.
There are two main ways to make blanks. In press blanking the Blanking Die Set cuts the full blank profile in one stroke, fast and accurate for high volume. In die blanking on a hydraulic press, or with a single fixed die, the line trades speed for flexibility and lower tooling cost, which suits short runs and large parts. Either way the Blank Stacker handles the output: a Magnetic Belt conveyor with a Belt Magnet holds each steel blank flat as it leaves the die, and the Stacking Station squares them into counted stacks while a Shuttle Table swaps full pallets without stopping. The leftover web goes to the Scrap Chopper, which cuts it into short pieces so it falls free instead of tangling. Tying it together, the Line PLC times the Feed Sync Encoder so feeding only happens with the slide up, and Die Protection Sensor sensors stop the press if a blank misfeeds before the expensive die is damaged.
Blanking Press Line parts and their functions
9 top-level parts · 350 parts in total · full bill of materials below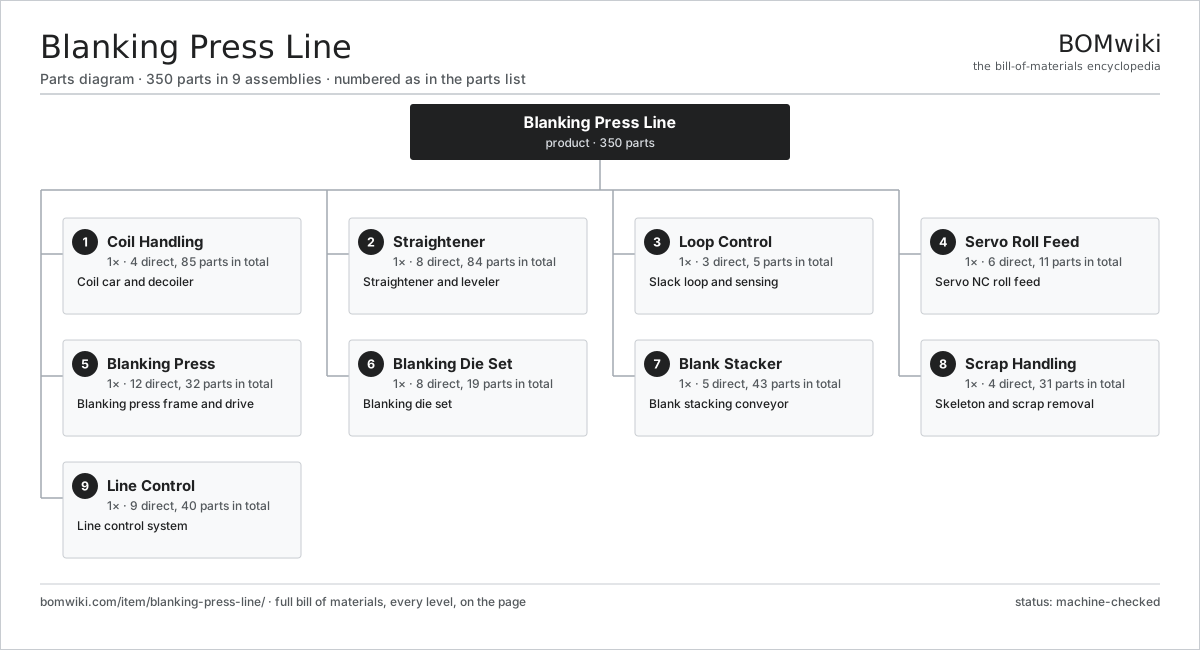
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Coil Handling 4 parts | 1× | Coil car and decoiler |
| 2 | Straightener 8 parts | 1× | Straightener and leveler |
| 3 | Loop Control 3 parts | 1× | Slack loop and sensing |
| 4 | Servo Roll Feed 6 parts | 1× | Servo NC roll feed |
| 5 | Blanking Press 12 parts | 1× | Blanking press frame and drive |
| 6 | Blanking Die Set 8 parts | 1× | Blanking die set |
| 7 | Blank Stacker 5 parts | 1× | Blank stacking conveyor |
| 8 | Scrap Handling 4 parts | 1× | Skeleton and scrap removal |
| 9 | Line Control 9 parts | 1× | Line control system |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Blanking Press Line
9 top-level lines · 110 rows shown · 350 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Coil Handling 4 parts | blanking-press-line-coil-handling | 1× | 1 | 85 | assembly |
| 1.1 | Coil Car 4 parts | blanking-press-line-coil-car | 1× | 1 | 31 | assembly |
| 1.1.1 | Coil Saddle | blanking-press-line-coil-saddle | 1× | 1 | · | part |
| 1.1.2 | Lift Cylinder | blanking-press-line-lift-cylinder | 2× | 2 | · | part |
| 1.1.3 | Travel Wheel | blanking-press-line-travel-wheel | 4× | 4 | · | part |
| 1.1.4 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 1.2 | Decoiler 6 parts | blanking-press-line-decoiler | 1× | 1 | 49 | assembly |
| 1.2.1 | Expanding Mandrel | blanking-press-line-expanding-mandrel | 2× | 2 | · | part |
| 1.2.2 | Mandrel Segment | blanking-press-line-mandrel-segment | 8× | 8 | · | part |
| 1.2.3 | Expansion Cylinder | blanking-press-line-expand-cylinder | 2× | 2 | · | part |
| 1.2.4 | Decoiler Gearbox 4 parts + deeper › | blanking-press-line-decoiler-gearbox | 1× | 1 | 9 | assembly |
| 1.2.5 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 1.2.6 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 1.3 | Peeler Arm 3 parts | blanking-press-line-peeler-arm | 1× | 1 | 3 | assembly |
| 1.3.1 | Hold-down Roller | blanking-press-line-holddown-roller | 1× | 1 | · | part |
| 1.3.2 | Peeler Blade | blanking-press-line-peeler-blade | 1× | 1 | · | part |
| 1.3.3 | Arm Cylinder | blanking-press-line-arm-cylinder | 1× | 1 | · | part |
| 1.4 | Coil Keeper Roller | blanking-press-line-coil-keeper | 2× | 2 | · | part |
| 2 | Straightener 8 parts | blanking-press-line-straightener | 1× | 1 | 84 | assembly |
| 2.1 | Entry Pinch Roll | blanking-press-line-entry-pinch-roll | 2× | 2 | · | part |
| 2.2 | Work Roll | blanking-press-line-work-roll | 9× | 9 | · | part |
| 2.3 | Backup Roll | blanking-press-line-backup-roll | 14× | 14 | · | part |
| 2.4 | Roll Cassette | blanking-press-line-roll-cassette | 1× | 1 | · | part |
| 2.5 | Gap Screw | blanking-press-line-gap-screw | 4× | 4 | · | part |
| 2.6 | Straightener Gearbox 4 parts | blanking-press-line-straightener-gearbox | 1× | 1 | 14 | assembly |
| 2.6.1 | Helical Gear Pair | gear-pair | 4× | 4 | · | part |
| 2.6.2 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 2.6.3 | Ball Bearing | ball-bearing | 6× | 6 | · | part |
| 2.6.4 | Oil Seal | oil-seal | 3× | 3 | · | part |
| 2.7 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 2.7.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 2.7.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 2.7.3 | Encoder | encoder | 1× | 1 | · | part |
| 2.7.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 2.8 | Ball Bearing | ball-bearing | 16× | 16 | · | part |
| 3 | Loop Control 3 parts | blanking-press-line-loop-control | 1× | 1 | 5 | assembly |
| 3.1 | Loop Pit | blanking-press-line-loop-pit | 1× | 1 | · | part |
| 3.2 | Loop Sensor | blanking-press-line-loop-sensor | 2× | 2 | · | part |
| 3.3 | Strip Guide | blanking-press-line-strip-guide | 2× | 2 | · | part |
| 4 | Servo Roll Feed 6 parts | blanking-press-line-servo-feed | 1× | 1 | 11 | assembly |
| 4.1 | Feed Roll | blanking-press-line-feed-roll | 2× | 2 | · | part |
| 4.2 | Feed Servo | blanking-press-line-feed-servo | 1× | 1 | · | part |
| 4.3 | Release Cam | blanking-press-line-release-cam | 1× | 1 | · | part |
| 4.4 | Edge Guide | blanking-press-line-edge-guide | 2× | 2 | · | part |
| 4.5 | Pilot Release | blanking-press-line-pilot-release | 1× | 1 | · | part |
| 4.6 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 5 | Blanking Press 12 parts | blanking-press-line-press | 1× | 1 | 32 | assembly |
| 5.1 | Crown | blanking-press-line-crown | 1× | 1 | · | part |
| 5.2 | Upright | blanking-press-line-upright | 2× | 2 | · | part |
| 5.3 | Bed and Bolster | blanking-press-line-bed-bolster | 1× | 1 | · | part |
| 5.4 | Slide | blanking-press-line-slide | 1× | 1 | · | part |
| 5.5 | Eccentric Shaft | blanking-press-line-eccentric-shaft | 1× | 1 | · | part |
| 5.6 | Connecting Rod | blanking-press-line-connecting-rod | 2× | 2 | · | part |
| 5.7 | Flywheel | blanking-press-line-flywheel | 1× | 1 | · | part |
| 5.8 | Clutch-Brake 4 parts | blanking-press-line-clutch-brake | 1× | 1 | 10 | assembly |
| 5.8.1 | Clutch Plate | blanking-press-line-clutch-plate | 2× | 2 | · | part |
| 5.8.2 | Brake Plate | blanking-press-line-brake-plate | 1× | 1 | · | part |
| 5.8.3 | Clutch Cylinder | blanking-press-line-clutch-cylinder | 1× | 1 | · | part |
| 5.8.4 | Coil Spring | coil-spring | 6× | 6 | · | part |
| 5.9 | Gib | blanking-press-line-gib | 4× | 4 | · | part |
| 5.10 | Counterbalance Cylinder | blanking-press-line-counterbalance | 2× | 2 | · | part |
| 5.11 | Main Motor | blanking-press-line-main-motor | 1× | 1 | · | part |
| 5.12 | Ball Bearing | ball-bearing | 6× | 6 | · | part |
| 6 | Blanking Die Set 8 parts | blanking-press-line-die-set | 1× | 1 | 19 | assembly |
| 6.1 | Upper Die Shoe | blanking-press-line-upper-die-shoe | 1× | 1 | · | part |
| 6.2 | Lower Die Shoe | blanking-press-line-lower-die-shoe | 1× | 1 | · | part |
| 6.3 | Blanking Punch | blanking-press-line-punch | 1× | 1 | · | part |
| 6.4 | Die Plate | blanking-press-line-die-plate | 1× | 1 | · | part |
| 6.5 | Stripper Plate | blanking-press-line-stripper-plate | 1× | 1 | · | part |
| 6.6 | Guide Pin | blanking-press-line-guide-pin | 4× | 4 | · | part |
| 6.7 | Pilot Pin | blanking-press-line-pilot-pin | 2× | 2 | · | part |
| 6.8 | Coil Spring | coil-spring | 8× | 8 | · | part |
| 7 | Blank Stacker 5 parts | blanking-press-line-destacker | 1× | 1 | 43 | assembly |
| 7.1 | Magnetic Belt 3 parts | blanking-press-line-magnetic-belt | 1× | 1 | 12 | assembly |
| 7.1.1 | Belt Magnet | blanking-press-line-belt-magnet | 6× | 6 | · | part |
| 7.1.2 | Drive Belt | drive-belt | 2× | 2 | · | part |
| 7.1.3 | Conveyor Roller | blanking-press-line-conveyor-roller | 4× | 4 | · | part |
| 7.2 | Stacking Station 3 parts | blanking-press-line-stacking-station | 1× | 1 | 5 | assembly |
| 7.2.1 | Back Stop | blanking-press-line-back-stop | 2× | 2 | · | part |
| 7.2.2 | Side Jogger | blanking-press-line-side-jogger | 2× | 2 | · | part |
| 7.2.3 | Sheet Metal Panel | sheet-panel | 1× | 1 | · | part |
| 7.3 | Shuttle Table | blanking-press-line-shuttle | 1× | 1 | · | part |
| 7.4 | Edge Fanner | blanking-press-line-blank-fanner | 1× | 1 | · | part |
| 7.5 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 7.5.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 7.5.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 7.5.3 | Encoder | encoder | 1× | 1 | · | part |
| 7.5.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 8 | Scrap Handling 4 parts | blanking-press-line-scrap-handling | 1× | 1 | 31 | assembly |
| 8.1 | Scrap Chopper | blanking-press-line-scrap-chopper | 1× | 1 | · | part |
| 8.2 | Scrap Conveyor 3 parts | blanking-press-line-scrap-conveyor | 1× | 1 | 4 | assembly |
| 8.2.1 | Drive Belt | drive-belt | 1× | 1 | · | part |
| 8.2.2 | Conveyor Roller | blanking-press-line-conveyor-roller | 2× | 2 | · | part |
| 8.2.3 | Scrap Hopper | blanking-press-line-scrap-hopper | 1× | 1 | · | part |
| 8.3 | Chopper Blade | blanking-press-line-chopper-blade | 2× | 2 | · | part |
| 8.4 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 8.4.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 8.4.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 8.4.3 | Encoder | encoder | 1× | 1 | · | part |
| 8.4.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 9 | Line Control 9 parts | blanking-press-line-control | 1× | 1 | 40 | assembly |
| 9.1 | Line PLC | blanking-press-line-plc | 1× | 1 | · | part |
| 9.2 | Servo Drive | blanking-press-line-servo-drive | 4× | 4 | · | part |
| 9.3 | Feed Sync Encoder | blanking-press-line-feed-sync | 1× | 1 | · | part |
| 9.4 | Die Protection Sensor | blanking-press-line-die-protect | 4× | 4 | · | part |
| 9.5 | Light Curtain | blanking-press-line-light-curtain | 2× | 2 | · | part |
| 9.6 | Operator HMI | blanking-press-line-hmi | 1× | 1 | · | part |
| 9.7 | Power Supply | power-supply | 1× | 1 | · | part |
| 9.8 | Wire Bundle | wire-bundle | 2× | 2 | · | part |
| 9.9 | Connector | connector | 24× | 24 | · | part |
Related products
same domain, ranked by shared parts Creep-Feed Grinder
571 parts · shares 6 with this page
 Railway Wheel Lathe
1,201 parts · shares 6 with this page
 Rotary-Table Surface Grinder
172 parts · shares 6 with this page
Spline Rolling Machine
138 parts · shares 6 with this page
 Multi-Spindle Automatic Lathe
352 parts · shares 5 with this page
Upsetter Forging Machine
125 parts · shares 5 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
1,172-word article