Superfinishing Machine
ProductOverview
A superfinishing machine produces mirror-smooth surfaces on parts that have already been ground or hard-turned. Grinding leaves a surface that looks bright but carries a dense field of fine peaks and a thin smeared layer of disturbed metal. Those peaks carry load on a very small real contact area, they wear quickly in the first hours of service, and they trap and release abrasive debris into oil films. Superfinishing removes them. An oscillating abrasive Abrasive Stone is pressed lightly against the rotating workpiece, and the short rubbing motion shears off the peaks and leaves a flat-topped plateau surface with a fine cross-hatch. The result is a finish of Ra 0.01 to 0.05 micron with a high bearing area ratio, which is why the process is standard on bearing races, rollers, crankshaft and camshaft journals, and hydraulic and fuel-injection components.
The machine is built around the rotating workpiece and the oscillating stone. A heavy Machine Base and Slideways carries a Workhead Spindle that turns the part and an Stone Oscillation Head that drives the stone back and forth. The Stone Pressure and Feed System system holds the stone against the part at a regulated contact pressure, the Stone Holder and Abrasive Stones presents the abrasive, and a Workpiece Drive and Support supports and rotates the part. A Coolant System flushes the contact, a Control Cabinet runs the cycle, and a Part Loader feeds parts in volume.
How Superfinishing Works
Three motions combine. The workpiece rotates, the stone oscillates along the axis, and the stone is fed radially under light pressure. The rotation speed is low compared with grinding, often 50 to 1500 rpm, and the radial pressure is light, 0.2 to 2 MPa, so the stone abrades only the high points rather than cutting the part to size. The axial oscillation, 200 to 2500 strokes per minute over a 1 to 6 mm stroke, makes each abrasive grain trace a long cross-hatched path instead of a single circle, which breaks up the directional pattern grinding left and prevents the stone from glazing.
The stone self-dresses as it works. Because contact pressure is held constant and the part is already round, the stone wears into conformity with the surface, the loaded grain fractures and exposes fresh cutting edges, and material removal slows as the peaks disappear. Cycle control watches for this: the cycle ends when the surface has plateaued, typically after removing only 2 to 10 micron of stock. The cross-hatch angle is tuned through the ratio of oscillation frequency to rotation speed, which matters for parts like cylinder bores and crankshaft journals where the finish controls oil retention.
Workhead and Workpiece Drive
The Workhead Spindle rotates the part. Its Workhead Spindle runs in preloaded angular-contact Ball Bearing sets with runout under 0.001 mm, driven by the Workhead Drive Motor and sealed by Oil Seal elements. A Collet Chuck centers shaft and journal work without distortion. For ring and roller work the part is not chucked but carried on the Workpiece Drive and Support: a pair of Regulating Roll units turned by the Regulating Roll Motor spin the ring while a Backing Shoe locates it against stone pressure. Shaft and crankshaft work is supported between the workhead and a Tailstock Center.
Oscillation, Pressure, and Stone
The Stone Oscillation Head makes the defining motion. An Oscillation Drive eccentric, turned by the Oscillation Motor, converts rotation into axial stroke through the Stone Carrier Arm, and the Amplitude Adjuster sets the stroke length. The arm is kept light because it reverses direction thousands of times a minute.
The Stone Pressure and Feed System system controls contact. A Stone Pressure Cylinder applies the stone load, the Pressure Regulator holds that load steady as the stone wears, and a Pressure Sensor closes the force loop. The Radial Infeed Slide, a preloaded Ball Screw and Linear Guide Rail slide driven by a Servo Motor and read by the Infeed Linear Scale, sets the radial position to 0.001 mm. The Stone Holder and Abrasive Stones carries the Abrasive Stone in a Stone Holder Body, retained by a Stone Clamp and backed by a Conforming Shoe that wraps the stone to the part radius and spreads contact.
Materials and Abrasives
The base is GG-25 grey cast iron, chosen for its damping, since the high-frequency oscillation would ring through a welded steel frame. The Base Casting is stress-relieved so geometry holds over years. Slides run on Linear Guide Rail rails protected by a Way Cover and lubricated by the Way Lubrication Pump. The abrasive stone is the consumable that decides the finish: vitrified-bond aluminium oxide for general steel, silicon carbide for cast iron and harder finishes, and CBN for high-volume hardened-steel bearing work, in grits from 320 for stock removal to 1200 for the finest plateau. Coolant is a light, low-viscosity oil rather than the heavy emulsions used in grinding, because it must penetrate the narrow stone contact and float away the very fine swarf.
Coolant and Filtration
The Coolant System floods the contact line. A Coolant Pump draws from the Coolant Tank and delivers 20 to 80 L/min through the holder. The returning oil carries fine metal and spent grit that would scratch a finished surface, so a Magnetic Separator pulls ferrous swarf and a Fine Filter polishes the oil to 3 to 5 micron before it returns. Clean oil is as important to the final Ra as the stone.
Control, Variants, and Use
The Control Cabinet runs the cycle. A CNC Controller sequences workhead speed, oscillation frequency, stone pressure, and timed infeed through Servo Drive amplifiers fed by a Power Supply, with a Bare PCB backplane, an Microcontroller for sequencing, SMD Passive (R/C/L), Relay outputs, Connector panels, and a Wire Bundle harness. The operator sets recipes and finish targets at the Operator Panel. Plunge machines finish one feature at a time, through-feed machines pass cylindrical rollers continuously between rolls, and crankshaft machines wrap several stones around each journal at once. High-volume lines add the Part Loader, a Loader Gantry with Part Gripper heads and a Feed Conveyor driven by Drive Belt elements and Servo Motor axes, holding cycle times of a few seconds per part. In bearing and engine plants these machines run inline after grinding, and the plateau finish they leave is what lets a bearing or journal survive its first hours without break-in damage.
Superfinishing Machine parts and their functions
9 top-level parts · 160 parts in total · full bill of materials below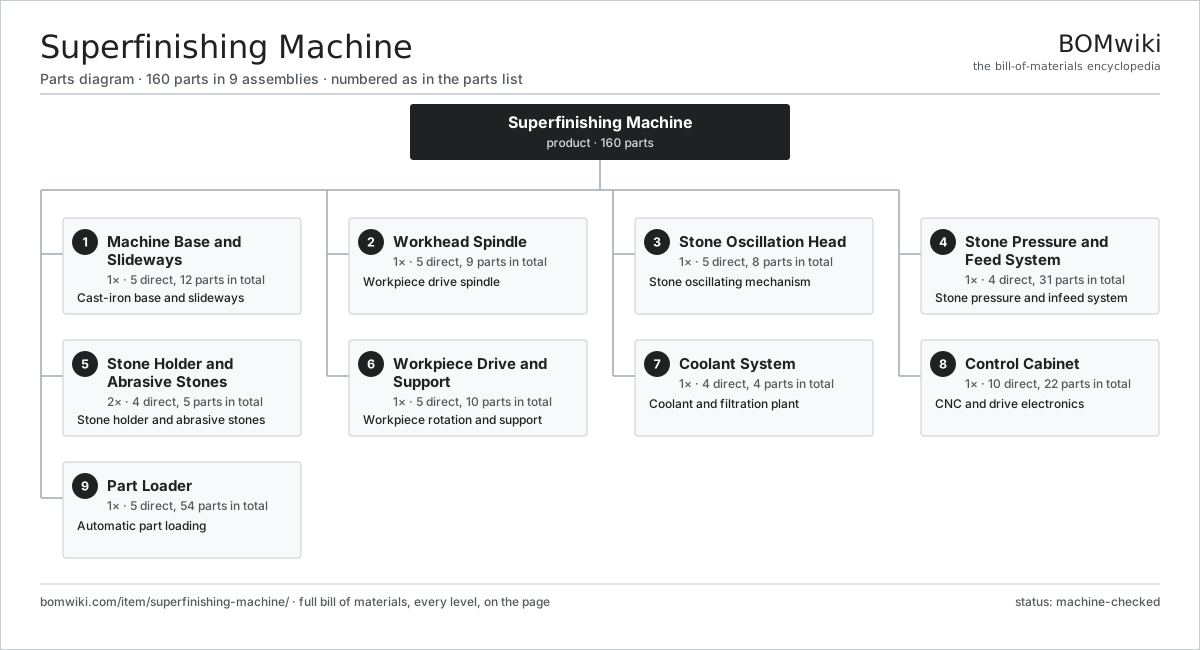
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Machine Base and Slideways 5 parts | 1× | Cast-iron base and slideways |
| 2 | Workhead Spindle 5 parts | 1× | Workpiece drive spindle |
| 3 | Stone Oscillation Head 5 parts | 1× | Stone oscillating mechanism |
| 4 | Stone Pressure and Feed System 4 parts | 1× | Stone pressure and infeed system |
| 5 | Stone Holder and Abrasive Stones 4 parts | 2× | Stone holder and abrasive stones |
| 6 | Workpiece Drive and Support 5 parts | 1× | Workpiece rotation and support |
| 7 | Coolant System 4 parts | 1× | Coolant and filtration plant |
| 8 | Control Cabinet 10 parts | 1× | CNC and drive electronics |
| 9 | Part Loader 5 parts | 1× | Automatic part loading |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Superfinishing Machine
9 top-level lines · 64 rows shown · 160 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Machine Base and Slideways 5 parts | sfm-machine-base | 1× | 1 | 12 | assembly |
| 1.1 | Base Casting | sfm-base-casting | 1× | 1 | · | part |
| 1.2 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 1.3 | Way Cover | sfm-way-cover | 2× | 2 | · | part |
| 1.4 | Leveling Mount | sfm-leveling-mount | 6× | 6 | · | part |
| 1.5 | Way Lubrication Pump | sfm-lube-pump | 1× | 1 | · | part |
| 2 | Workhead Spindle 5 parts | sfm-workhead | 1× | 1 | 9 | assembly |
| 2.1 | Workhead Spindle | sfm-workhead-spindle | 1× | 1 | · | part |
| 2.2 | Workhead Drive Motor | sfm-workhead-motor | 1× | 1 | · | part |
| 2.3 | Collet Chuck | sfm-collet-chuck | 1× | 1 | · | part |
| 2.4 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 2.5 | Oil Seal | oil-seal | 2× | 2 | · | part |
| 3 | Stone Oscillation Head 5 parts | sfm-oscillation-head | 1× | 1 | 8 | assembly |
| 3.1 | Oscillation Drive | sfm-oscillation-drive | 1× | 1 | · | part |
| 3.2 | Oscillation Motor | sfm-oscillation-motor | 1× | 1 | · | part |
| 3.3 | Stone Carrier Arm | sfm-oscillation-arm | 1× | 1 | · | part |
| 3.4 | Amplitude Adjuster | sfm-amplitude-adjuster | 1× | 1 | · | part |
| 3.5 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 4 | Stone Pressure and Feed System 4 parts | sfm-pressure-feed | 1× | 1 | 31 | assembly |
| 4.1 | Stone Pressure Cylinder | sfm-pressure-cylinder | 1× | 1 | · | part |
| 4.2 | Pressure Regulator | sfm-pressure-regulator | 1× | 1 | · | part |
| 4.3 | Radial Infeed Slide 4 parts | sfm-infeed-slide | 1× | 1 | 28 | assembly |
| 4.3.1 | Ball Screw | ball-screw | 1× | 1 | · | part |
| 4.3.2 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 4.3.3 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 4.3.4 | Infeed Linear Scale | sfm-linear-scale | 1× | 1 | · | part |
| 4.4 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 5 | Stone Holder and Abrasive Stones 4 parts | sfm-stone-holder | 2× | 2 | 5 | assembly |
| 5.1 | Stone Holder Body | sfm-holder-body | 1× | 2 | · | part |
| 5.2 | Abrasive Stone | sfm-abrasive-stone | 2× | 4 | · | part |
| 5.3 | Stone Clamp | sfm-stone-clamp | 1× | 2 | · | part |
| 5.4 | Conforming Shoe | sfm-conform-shoe | 1× | 2 | · | part |
| 6 | Workpiece Drive and Support 5 parts | sfm-workpiece-drive | 1× | 1 | 10 | assembly |
| 6.1 | Regulating Roll | sfm-regulating-roll | 2× | 2 | · | part |
| 6.2 | Regulating Roll Motor | sfm-roll-drive-motor | 1× | 1 | · | part |
| 6.3 | Backing Shoe | sfm-backing-shoe | 2× | 2 | · | part |
| 6.4 | Tailstock Center | sfm-tailstock-center | 1× | 1 | · | part |
| 6.5 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 7 | Coolant System 4 parts | sfm-coolant-system | 1× | 1 | 4 | assembly |
| 7.1 | Coolant Pump | sfm-coolant-pump | 1× | 1 | · | part |
| 7.2 | Coolant Tank | sfm-coolant-tank | 1× | 1 | · | part |
| 7.3 | Fine Filter | sfm-fine-filter | 1× | 1 | · | part |
| 7.4 | Magnetic Separator | sfm-magnetic-separator | 1× | 1 | · | part |
| 8 | Control Cabinet 10 parts | sfm-control-cabinet | 1× | 1 | 22 | assembly |
| 8.1 | CNC Controller | sfm-cnc-unit | 1× | 1 | · | part |
| 8.2 | Servo Drive | sfm-servo-drive | 3× | 3 | · | part |
| 8.3 | Power Supply | power-supply | 1× | 1 | · | part |
| 8.4 | Operator Panel | sfm-operator-panel | 1× | 1 | · | part |
| 8.5 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.6 | Microcontroller | mcu | 1× | 1 | · | part |
| 8.7 | Relay | relay | 4× | 4 | · | part |
| 8.8 | SMD Passive (R/C/L) | smd-passives | 1× | 1 | · | part |
| 8.9 | Connector | connector | 8× | 8 | · | part |
| 8.10 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 9 | Part Loader 5 parts | sfm-loader | 1× | 1 | 54 | assembly |
| 9.1 | Loader Gantry | sfm-loader-gantry | 1× | 1 | · | part |
| 9.2 | Part Gripper | sfm-gripper | 2× | 2 | · | part |
| 9.3 | Feed Conveyor | sfm-feed-conveyor | 1× | 1 | · | part |
| 9.4 | Servo Motor 4 parts | servo-motor | 2× | 2 | 24 | assembly |
| 9.4.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 2 | 3 | assembly |
| 9.4.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 2 | 19 | assembly |
| 9.4.3 | Encoder | encoder | 1× | 2 | · | part |
| 9.4.4 | Motor Housing | motor-housing | 1× | 2 | · | part |
| 9.5 | Drive Belt | drive-belt | 2× | 2 | · | part |
Related products
same domain, ranked by shared parts Bevel Gear Generator
201 parts · shares 4 with this page
Camshaft Grinder
489 parts · shares 4 with this page
Cold Rolling Mill
991 parts · shares 4 with this page
 Crankshaft Grinder
511 parts · shares 4 with this page
 Creep-Feed Grinder
571 parts · shares 4 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
1,098-word article