Capstan Lathe
ProductOverview
A capstan lathe is a small-part production lathe closely related to the turret lathe, but arranged for short, fast cycles on smaller bar stock. The difference is in how the turret moves. On a turret lathe the turret rides a saddle that traverses the whole bed; on a capstan lathe the turret sits on a short quick-return slide carried by a saddle that is clamped in a fixed position. The operator pulls a capstan wheel to feed the turret over its short stroke, then lets it snap back, and the turret indexes to the next tool. This short-stroke, quick-return action gives very fast cycle times on small components such as screws, pins, terminals, nipples, and bushings, which is what the machine was made for.
The machine is built on a compact Bed & Ways, with a Geared Headstock driving the bar spindle, a fixed Fixed Turret Saddle carrying the Quick-Return Capstan Slide and its Capstan Turret, and a Cross Slide & Tooling for forming and parting. A Bar Feed Magazine keeps the spindle supplied with fresh stock.
Headstock and bar handling
The Geared Headstock drives a hollow Bar Spindle bored to pass the bar, through a Speed Gearbox off the Main Drive Motor. Work is gripped by the Collet Workholding: a Draw Tube pulls a Spring Collet into its taper to clamp the bar concentrically, and a Collet Closer opens and closes it between parts. After each finished part is cut off, the Bar Feed Magazine takes over: a sprung Bar Pusher advances the bar through the spindle until it meets the Bar Stop on the turret, presenting the right length of stock for the next part with no measuring.
The fixed saddle and quick-return slide
The Fixed Turret Saddle is what distinguishes the machine. It is clamped to the bed by Saddle Clamps and does not move during the cycle, acting only as a rigid bridge for the slide. Riding on it is the Quick-Return Capstan Slide, a short ram driven by the Capstan Wheel through a Pinion & Rack. The operator pulls the wheel to feed the turret into the work, and at the end of the cut a Quick-Return Spring snaps the slide back. Because the stroke is short and the return is quick, the operator can run through six operations in seconds. The fixed saddle limits the machine to shorter parts than a saddle-type turret lathe, which is the trade made for speed and simplicity.
The capstan turret
The Capstan Turret holds six tools on its Turret Head, each face bored for a Turret Tool Holder such as a drill, a die head, a knee tool, or a box tool that turns a diameter. As the slide returns, the Indexing Mechanism rotates the head to the next station. A Geneva Cam produces the stepped motion and a spring Index Plunger seats each face accurately, so every tool returns to the same position. The sequence around the six faces is planned so the part is built up in one pass of the turret: center, drill, turn, thread, and so on.
Cross slide and parting
The Cross Slide & Tooling works the diameter while the turret works the end. A Front Tool Post holds a forming or chamfer tool, and a Rear Tool Post holds the parting blade that cuts the finished part off the bar at the end of the cycle. Forming tools on the cross slide let a complex profile be produced in a single plunge, which keeps the cycle short.
Stops, auxiliaries, and use
Repeatability comes from the Turret Length Stops, a Stop Drum with one Length Stop Screw per station setting how far each tool advances. A Lubrication System system oils the slides and headstock, a Coolant System system floods the cut, and the Electrical Control cabinet carries the motor controls and an operator Operator Pendant. Castings are gray iron, ways and the turret index parts are hardened. The capstan slide and its pinion and rack are hardened and ground because they cycle constantly, and the return spring is sized to snap the slide back briskly without slamming the stops.
The capstan lathe suits high-volume runs of small turned parts from bar, the kind of work once done in their thousands for fasteners, electrical hardware, and instrument components. Typical products are screws, studs, terminals, contact pins, gland nuts, and small bushings, each built up in one pass of the six-station turret and parted off by the rear tool post. The economics favor it wherever the part is small enough to fit the short stroke and the run is long enough to justify tooling the turret: setup takes time, but afterward the cycle is fast and the operator's role is reduced to feeding bar and watching the stops. The machine is the manual ancestor of the automatic screw machine, and it remains a clear illustration of how preset tooling, collet loading, and per-station stops turn a plain lathe into a repeatable production machine.
Capstan Lathe parts and their functions
13 top-level parts · 197 parts in total · full bill of materials below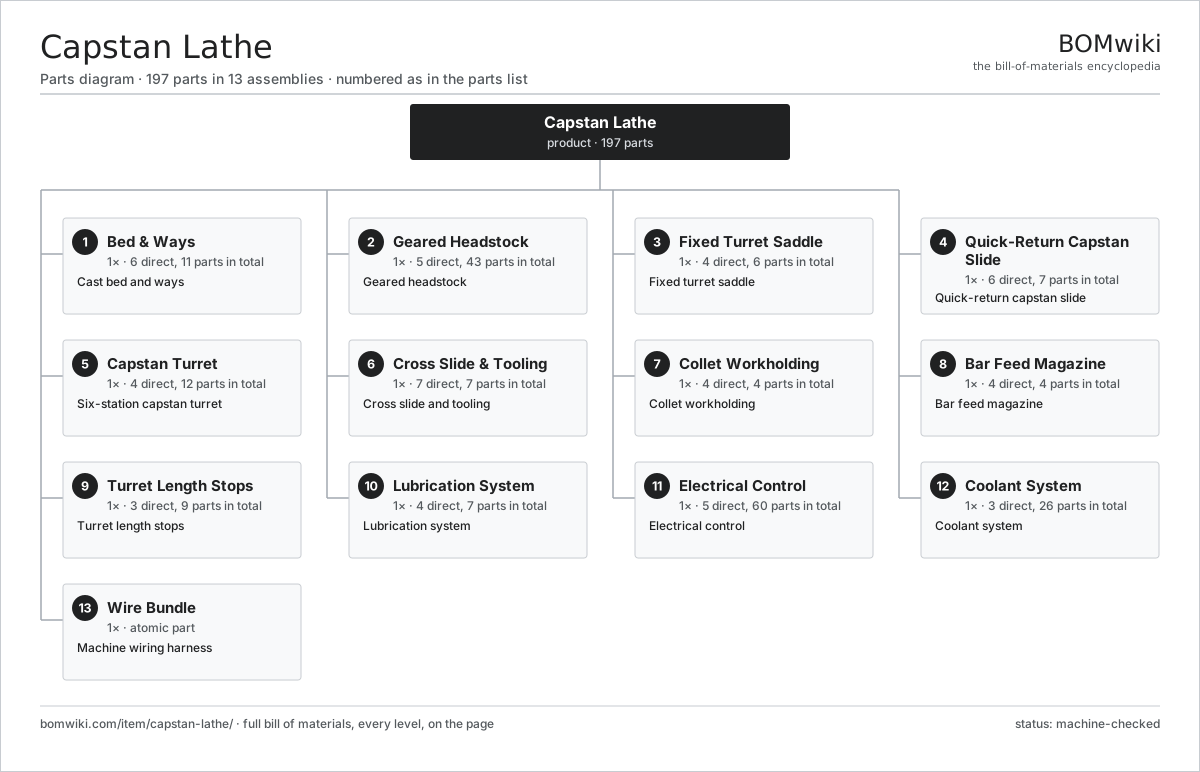
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Bed & Ways 6 parts | 1× | Cast bed and ways |
| 2 | Geared Headstock 5 parts | 1× | Geared headstock |
| 3 | Fixed Turret Saddle 4 parts | 1× | Fixed turret saddle |
| 4 | Quick-Return Capstan Slide 6 parts | 1× | Quick-return capstan slide |
| 5 | Capstan Turret 4 parts | 1× | Six-station capstan turret |
| 6 | Cross Slide & Tooling 7 parts | 1× | Cross slide and tooling |
| 7 | Collet Workholding 4 parts | 1× | Collet workholding |
| 8 | Bar Feed Magazine 4 parts | 1× | Bar feed magazine |
| 9 | Turret Length Stops 3 parts | 1× | Turret length stops |
| 10 | Lubrication System 4 parts | 1× | Lubrication system |
| 11 | Electrical Control 5 parts | 1× | Electrical control |
| 12 | Coolant System 3 parts | 1× | Coolant system |
| 13 | Wire Bundle | 1× | Machine wiring harness |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Capstan Lathe
13 top-level lines · 88 rows shown · 197 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Bed & Ways 6 parts | capstan-lathe-bed | 1× | 1 | 11 | assembly |
| 1.1 | Bed Casting | capstan-lathe-bed-casting | 1× | 1 | · | part |
| 1.2 | Hardened V-Way | capstan-lathe-v-way | 2× | 2 | · | part |
| 1.3 | Hardened Flat Way | capstan-lathe-flat-way | 1× | 1 | · | part |
| 1.4 | Way Wiper | capstan-lathe-way-wiper | 4× | 4 | · | part |
| 1.5 | Bed Leg & Foot | capstan-lathe-bed-foot | 2× | 2 | · | part |
| 1.6 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 2 | Geared Headstock 5 parts | capstan-lathe-headstock | 1× | 1 | 43 | assembly |
| 2.1 | Bar Spindle | capstan-lathe-spindle | 1× | 1 | · | part |
| 2.2 | Headstock Casting | capstan-lathe-headstock-casting | 1× | 1 | · | part |
| 2.3 | Speed Gearbox 4 parts | capstan-lathe-speed-gearbox | 1× | 1 | 13 | assembly |
| 2.3.1 | Helical Gear Pair | gear-pair | 5× | 5 | · | part |
| 2.3.2 | Shift Fork | capstan-lathe-shift-fork | 2× | 2 | · | part |
| 2.3.3 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 2.3.4 | Ball Bearing | ball-bearing | 5× | 5 | · | part |
| 2.4 | Main Drive Motor 5 parts | capstan-lathe-main-motor | 1× | 1 | 26 | assembly |
| 2.4.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 2.4.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 2.4.3 | Copper Winding | copper-winding | 1× | 1 | · | part |
| 2.4.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 2.4.5 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 2.5 | Spindle Bearing | capstan-lathe-spindle-bearing | 2× | 2 | · | part |
| 3 | Fixed Turret Saddle 4 parts | capstan-lathe-saddle | 1× | 1 | 6 | assembly |
| 3.1 | Saddle Casting | capstan-lathe-saddle-casting | 1× | 1 | · | part |
| 3.2 | Saddle Clamp | capstan-lathe-saddle-clamp | 2× | 2 | · | part |
| 3.3 | Capstan Slide Way | capstan-lathe-slide-way | 2× | 2 | · | part |
| 3.4 | Saddle Gib | capstan-lathe-saddle-gib | 1× | 1 | · | part |
| 4 | Quick-Return Capstan Slide 6 parts | capstan-lathe-capstan-slide | 1× | 1 | 7 | assembly |
| 4.1 | Slide Casting | capstan-lathe-slide-casting | 1× | 1 | · | part |
| 4.2 | Capstan Wheel | capstan-lathe-capstan-wheel | 1× | 1 | · | part |
| 4.3 | Pinion & Rack | capstan-lathe-pinion-rack | 1× | 1 | · | part |
| 4.4 | Quick-Return Spring | capstan-lathe-return-spring | 1× | 1 | · | part |
| 4.5 | Feed Trip | capstan-lathe-feed-trip | 1× | 1 | · | part |
| 4.6 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 5 | Capstan Turret 4 parts | capstan-lathe-turret | 1× | 1 | 12 | assembly |
| 5.1 | Turret Head | capstan-lathe-turret-head | 1× | 1 | · | part |
| 5.2 | Indexing Mechanism 4 parts | capstan-lathe-index-mechanism | 1× | 1 | 4 | assembly |
| 5.2.1 | Geneva Cam | capstan-lathe-geneva-cam | 1× | 1 | · | part |
| 5.2.2 | Index Plunger | capstan-lathe-index-plunger | 1× | 1 | · | part |
| 5.2.3 | Coil Spring | coil-spring | 1× | 1 | · | part |
| 5.2.4 | Helical Gear Pair | gear-pair | 1× | 1 | · | part |
| 5.3 | Turret Tool Holder | capstan-lathe-turret-tool | 6× | 6 | · | part |
| 5.4 | Turret Clamp | capstan-lathe-turret-clamp | 1× | 1 | · | part |
| 6 | Cross Slide & Tooling 7 parts | capstan-lathe-cross-slide | 1× | 1 | 7 | assembly |
| 6.1 | Cross-Slide Casting | capstan-lathe-cross-casting | 1× | 1 | · | part |
| 6.2 | Cross-Slide Screw | capstan-lathe-cross-screw | 1× | 1 | · | part |
| 6.3 | Cross-Slide Nut | capstan-lathe-cross-nut | 1× | 1 | · | part |
| 6.4 | Cross Handwheel | capstan-lathe-cross-handwheel | 1× | 1 | · | part |
| 6.5 | Front Tool Post | capstan-lathe-front-post | 1× | 1 | · | part |
| 6.6 | Rear Tool Post | capstan-lathe-rear-post | 1× | 1 | · | part |
| 6.7 | Cross-Slide Gib | capstan-lathe-cross-gib | 1× | 1 | · | part |
| 7 | Collet Workholding 4 parts | capstan-lathe-collet | 1× | 1 | 4 | assembly |
| 7.1 | Spring Collet | capstan-lathe-spring-collet | 1× | 1 | · | part |
| 7.2 | Draw Tube | capstan-lathe-draw-tube | 1× | 1 | · | part |
| 7.3 | Collet Closer | capstan-lathe-collet-closer | 1× | 1 | · | part |
| 7.4 | Chuck Nose | capstan-lathe-chuck-nose | 1× | 1 | · | part |
| 8 | Bar Feed Magazine 4 parts | capstan-lathe-bar-feed | 1× | 1 | 4 | assembly |
| 8.1 | Bar Feed Tube | capstan-lathe-feed-tube | 1× | 1 | · | part |
| 8.2 | Bar Pusher | capstan-lathe-bar-pusher | 1× | 1 | · | part |
| 8.3 | Pusher Spring | capstan-lathe-bar-spring | 1× | 1 | · | part |
| 8.4 | Bar Stop | capstan-lathe-bar-stop | 1× | 1 | · | part |
| 9 | Turret Length Stops 3 parts | capstan-lathe-stops | 1× | 1 | 9 | assembly |
| 9.1 | Stop Drum | capstan-lathe-stop-drum | 1× | 1 | · | part |
| 9.2 | Length Stop Screw | capstan-lathe-stop-screw | 6× | 6 | · | part |
| 9.3 | Trip Dog | capstan-lathe-trip-dog | 2× | 2 | · | part |
| 10 | Lubrication System 4 parts | capstan-lathe-lube | 1× | 1 | 7 | assembly |
| 10.1 | Lube Pump | capstan-lathe-lube-pump | 1× | 1 | · | part |
| 10.2 | Metering Unit | capstan-lathe-lube-meter | 4× | 4 | · | part |
| 10.3 | Distribution Tubing | capstan-lathe-lube-line | 1× | 1 | · | part |
| 10.4 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 11 | Electrical Control 5 parts | capstan-lathe-control | 1× | 1 | 60 | assembly |
| 11.1 | Control Board 3 parts | capstan-lathe-control-board | 1× | 1 | 42 | assembly |
| 11.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 11.1.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 11.1.3 | SMD Passive (R/C/L) | smd-passives | 40× | 40 | · | part |
| 11.2 | Relay | relay | 6× | 6 | · | part |
| 11.3 | Connector | connector | 10× | 10 | · | part |
| 11.4 | Operator Pendant | capstan-lathe-pendant | 1× | 1 | · | part |
| 11.5 | Control Enclosure | capstan-lathe-control-enclosure | 1× | 1 | · | part |
| 12 | Coolant System 3 parts | capstan-lathe-coolant | 1× | 1 | 26 | assembly |
| 12.1 | Coolant Pump 4 parts | capstan-lathe-coolant-pump | 1× | 1 | 24 | assembly |
| 12.1.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 12.1.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 12.1.3 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 12.1.4 | Oil Seal | oil-seal | 1× | 1 | · | part |
| 12.2 | Coolant Tank | capstan-lathe-coolant-tank | 1× | 1 | · | part |
| 12.3 | Coolant Nozzle | capstan-lathe-coolant-nozzle | 1× | 1 | · | part |
| 13 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Bevel Gear Generator
201 parts · shares 4 with this page
Centering and Facing Machine
1,419 parts · shares 4 with this page
 Continuous Belt Furnace
130 parts · shares 4 with this page
 Creep-Feed Grinder
571 parts · shares 4 with this page
Forging Roll Machine
135 parts · shares 4 with this page
 Industrial Band Saw
131 parts · shares 4 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
888-word article