Industrial TIG Welder
ProductOverview
An industrial TIG welder joins metal with an arc struck between a non-consumable tungsten electrode and the work, under a blanket of inert argon gas. Unlike processes that melt a wire into the joint, here the tungsten only carries the arc; the welder feeds a separate filler rod by hand when one is needed. The result is the cleanest and most controllable arc weld available, which is why TIG is the standard for stainless steel, aluminium, titanium, and thin precision work where appearance and metallurgy both matter. The penalty is speed: TIG is slower than MIG or stick and demands a skilled operator, so it is used where quality outweighs deposition rate.
The machine is built around an inverter Inverter Power Source that makes a stable, finely controlled welding current. A HF Arc Starter strikes the arc without touching the work, the TIG Torch holds the electrode and directs the gas, and a Water Cooler keeps the torch from overheating at high current. The Gas System times the argon flow, the Control Panel sets the parameters, and a Foot Pedal lets the welder trim current on the fly.
The inverter power source
The Inverter Power Source replaced the heavy mains transformers of older welders with a switch-mode design that is lighter and far more precise. Mains power first passes through the Input Rectifier, whose Rectifier Diode devices turn three-phase AC into a DC bus. A PFC Stage keeps the current draw sinusoidal so the machine is kind to the supply. The IGBT Inverter Bridge then chops that bus at around forty kilohertz, driving the HF Main Transformer, a compact ferrite-core unit that steps the voltage down and isolates the output. The Output Rectifier and the Output Inductor turn the high-frequency secondary into smooth welding current. Overseeing all of this is the DSP Control Board, which closes the current loop thousands of times a second and shapes the pulse and AC waveforms that give TIG its control.
Striking and shielding the arc
TIG cannot strike by scratching, because dragging the tungsten on the work contaminates the electrode and the weld. Instead the HF Arc Starter uses a HF Spark Transformer and a Spark Gap to raise several kilovolts across the gap, ionising the argon so the main arc jumps across without contact. Around that arc, the Gas System delivers a steady envelope of argon: a Gas Solenoid Valve opens a pre-flow before the arc, holds flow during the weld, and runs a post-flow that protects the cooling tungsten and weld pool from oxidation. A Flow Meter sets the rate and a Gas Regulator drops the cylinder pressure.
The torch and cooling
The TIG Torch is where current, gas, and coolant all converge. The Tungsten Electrode electrode is gripped by a Collet inside a Collet Body, and the Ceramic Cup shapes the gas flow around the arc. A Back Cap seals the rear and clamps a long electrode. Everything reaches the torch through the Torch Cable, a bundle of power conductor, gas hose, and coolant lines. At currents above roughly 200 A the torch would overheat, so the Water Cooler circulates water with a Coolant Pump through a Cooler Radiator, and a Flow Switch stops welding if that flow is lost.
Operator control
What separates a usable TIG machine from a frustrating one is how finely the welder can govern heat. The Control Panel sets the base current, pulse frequency, and, for aluminium, the AC balance that decides how much of each cycle cleans oxide versus penetrates. The Foot Pedal is the signature control: its Pedal Potentiometer maps foot travel directly to current, letting the welder add heat as the joint warms and back off to fill a crater at the end, all without lifting the torch. The Encoder Knob and display let the operator dial in repeatable settings for production work.
Materials and use
DC TIG with the electrode negative suits steel, stainless steel, copper, and titanium, depositing a narrow, clean bead. AC TIG is the path to aluminium and magnesium, because reversing the current part of each cycle breaks up the tough oxide skin that otherwise blocks fusion. The Inverter Power Source supports both, plus pulse modes that limit heat input on thin material and control the pool on out-of-position work. Because of this range and cleanliness, industrial TIG welders are found in aerospace, food and pharmaceutical fabrication, tube and pipe shops, and any work where the weld must be sound, low in spatter, and presentable without grinding. The whole machine is housed in the Cabinet, a wheeled cabinet with forced-air cooling that keeps the power electronics protected on the shop floor.
Industrial TIG Welder parts and their functions
8 top-level parts · 492 parts in total · full bill of materials below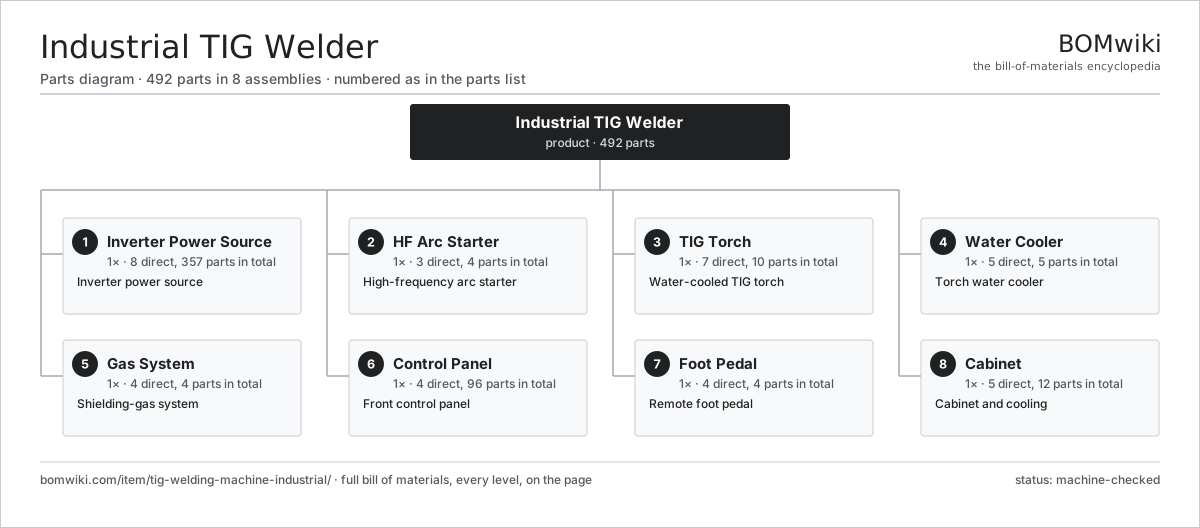
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Inverter Power Source 8 parts | 1× | Inverter power source |
| 2 | HF Arc Starter 3 parts | 1× | High-frequency arc starter |
| 3 | TIG Torch 7 parts | 1× | Water-cooled TIG torch |
| 4 | Water Cooler 5 parts | 1× | Torch water cooler |
| 5 | Gas System 4 parts | 1× | Shielding-gas system |
| 6 | Control Panel 4 parts | 1× | Front control panel |
| 7 | Foot Pedal 4 parts | 1× | Remote foot pedal |
| 8 | Cabinet 5 parts | 1× | Cabinet and cooling |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Industrial TIG Welder
8 top-level lines · 71 rows shown · 492 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Inverter Power Source 8 parts | tig-welding-machine-industrial-power-source | 1× | 1 | 357 | assembly |
| 1.1 | Input Rectifier 3 parts | tig-welding-machine-industrial-input-rectifier | 1× | 1 | 9 | assembly |
| 1.1.1 | Rectifier Diode | tig-welding-machine-industrial-bridge-diode | 6× | 6 | · | part |
| 1.1.2 | Heat Sink | heat-sink | 1× | 1 | · | part |
| 1.1.3 | DC-Link Capacitor | dc-link-cap | 2× | 2 | · | part |
| 1.2 | PFC Stage 5 parts | tig-welding-machine-industrial-pfc-stage | 1× | 1 | 65 | assembly |
| 1.2.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 1.2.2 | Power Inductor | power-inductor | 1× | 1 | · | part |
| 1.2.3 | Power MOSFET | mosfet | 2× | 2 | · | part |
| 1.2.4 | Gate Driver IC | gate-driver-ic | 1× | 1 | · | part |
| 1.2.5 | SMD Passive (R/C/L) | smd-passives | 60× | 60 | · | part |
| 1.3 | IGBT Inverter Bridge 3 parts | tig-welding-machine-industrial-inverter-bridge | 1× | 1 | 90 | assembly |
| 1.3.1 | IGBT Power Module | igbt-module | 4× | 4 | · | part |
| 1.3.2 | Gate Drive Board 3 parts + deeper › | tig-welding-machine-industrial-gate-board | 1× | 1 | 85 | assembly |
| 1.3.3 | Heat Sink | heat-sink | 1× | 1 | · | part |
| 1.4 | HF Main Transformer | tig-welding-machine-industrial-main-transformer | 1× | 1 | · | part |
| 1.5 | Output Rectifier 2 parts | tig-welding-machine-industrial-output-rectifier | 1× | 1 | 5 | assembly |
| 1.5.1 | Fast Recovery Diode | tig-welding-machine-industrial-fast-diode | 4× | 4 | · | part |
| 1.5.2 | Heat Sink | heat-sink | 1× | 1 | · | part |
| 1.6 | Output Inductor | tig-welding-machine-industrial-output-inductor | 1× | 1 | · | part |
| 1.7 | DSP Control Board 4 parts | tig-welding-machine-industrial-dsp-board | 1× | 1 | 184 | assembly |
| 1.7.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 1.7.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 1.7.3 | Current Sensor | current-sensor | 2× | 2 | · | part |
| 1.7.4 | SMD Passive (R/C/L) | smd-passives | 180× | 180 | · | part |
| 1.8 | Heat Sink | heat-sink | 2× | 2 | · | part |
| 2 | HF Arc Starter 3 parts | tig-welding-machine-industrial-hf-unit | 1× | 1 | 4 | assembly |
| 2.1 | HF Spark Transformer | tig-welding-machine-industrial-hf-transformer | 1× | 1 | · | part |
| 2.2 | Spark Gap | tig-welding-machine-industrial-spark-gap | 1× | 1 | · | part |
| 2.3 | Coupling Capacitor | tig-welding-machine-industrial-coupling-cap | 2× | 2 | · | part |
| 3 | TIG Torch 7 parts | tig-welding-machine-industrial-torch | 1× | 1 | 10 | assembly |
| 3.1 | Torch Body | tig-welding-machine-industrial-torch-body | 1× | 1 | · | part |
| 3.2 | Tungsten Electrode | tig-welding-machine-industrial-tungsten | 1× | 1 | · | part |
| 3.3 | Collet | tig-welding-machine-industrial-collet | 1× | 1 | · | part |
| 3.4 | Collet Body | tig-welding-machine-industrial-collet-body | 1× | 1 | · | part |
| 3.5 | Ceramic Cup | tig-welding-machine-industrial-ceramic-cup | 1× | 1 | · | part |
| 3.6 | Back Cap | tig-welding-machine-industrial-back-cap | 1× | 1 | · | part |
| 3.7 | Torch Cable 3 parts | tig-welding-machine-industrial-torch-cable | 1× | 1 | 4 | assembly |
| 3.7.1 | Power Conductor | tig-welding-machine-industrial-power-conductor | 1× | 1 | · | part |
| 3.7.2 | Coolant Hose | tig-welding-machine-industrial-coolant-hose | 2× | 2 | · | part |
| 3.7.3 | Gas Hose | tig-welding-machine-industrial-gas-hose | 1× | 1 | · | part |
| 4 | Water Cooler 5 parts | tig-welding-machine-industrial-cooler | 1× | 1 | 5 | assembly |
| 4.1 | Coolant Pump | tig-welding-machine-industrial-coolant-pump | 1× | 1 | · | part |
| 4.2 | Cooler Radiator | tig-welding-machine-industrial-radiator | 1× | 1 | · | part |
| 4.3 | Coolant Tank | tig-welding-machine-industrial-coolant-tank | 1× | 1 | · | part |
| 4.4 | Cooler Fan | tig-welding-machine-industrial-cooler-fan | 1× | 1 | · | part |
| 4.5 | Flow Switch | tig-welding-machine-industrial-flow-switch | 1× | 1 | · | part |
| 5 | Gas System 4 parts | tig-welding-machine-industrial-gas-system | 1× | 1 | 4 | assembly |
| 5.1 | Gas Solenoid Valve | tig-welding-machine-industrial-gas-valve | 1× | 1 | · | part |
| 5.2 | Flow Meter | tig-welding-machine-industrial-flow-meter | 1× | 1 | · | part |
| 5.3 | Gas Regulator | tig-welding-machine-industrial-gas-regulator | 1× | 1 | · | part |
| 5.4 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 6 | Control Panel 4 parts | tig-welding-machine-industrial-control-panel | 1× | 1 | 96 | assembly |
| 6.1 | Interface Board 3 parts | tig-welding-machine-industrial-hmi-board | 1× | 1 | 92 | assembly |
| 6.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 6.1.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 6.1.3 | SMD Passive (R/C/L) | smd-passives | 90× | 90 | · | part |
| 6.2 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 6.3 | Encoder Knob | tig-welding-machine-industrial-encoder-knob | 2× | 2 | · | part |
| 6.4 | Membrane Keypad | tig-welding-machine-industrial-membrane | 1× | 1 | · | part |
| 7 | Foot Pedal 4 parts | tig-welding-machine-industrial-foot-pedal | 1× | 1 | 4 | assembly |
| 7.1 | Pedal Potentiometer | tig-welding-machine-industrial-pedal-pot | 1× | 1 | · | part |
| 7.2 | Pedal Housing | tig-welding-machine-industrial-pedal-housing | 1× | 1 | · | part |
| 7.3 | Coil Spring | coil-spring | 1× | 1 | · | part |
| 7.4 | Pedal Cable | tig-welding-machine-industrial-pedal-cable | 1× | 1 | · | part |
| 8 | Cabinet 5 parts | tig-welding-machine-industrial-enclosure | 1× | 1 | 12 | assembly |
| 8.1 | Sheet Metal Panel | sheet-panel | 5× | 5 | · | part |
| 8.2 | Cabinet Fan | tig-welding-machine-industrial-cabinet-fan | 1× | 1 | · | part |
| 8.3 | Caster | tig-welding-machine-industrial-caster | 4× | 4 | · | part |
| 8.4 | Power Supply | power-supply | 1× | 1 | · | part |
| 8.5 | Fastener Set | fastener-set | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Flash Butt Welding Machine
294 parts · shares 2 with this page
 Servo Stamping Press
633 parts · shares 6 with this page
Chain Link Welding Machine
440 parts · shares 4 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
927-word article