Tandem Press Line
ProductOverview
A tandem press line is a row of large stamping presses that turn flat steel blanks into finished sheet-metal panels, one forming operation per press. The flat blank enters at one end, the Lead Draw Press draws it into a deep shape, and each Secondary Press downstream trims, pierces, flanges, or restrikes the part until a complete panel leaves the far end. Between every press, the Interpress Automation lifts the part out of the open die and sets it into the next one, so the line behaves like a single machine even though each press strokes on its own. These lines run in automotive body shops, where one line might press 4 to 6 panels per minute: doors, hoods, roofs, fenders, and floor pans, all from coil-fed blanks.
A line is built from the Blank Destacker and Blank Conditioning at the front, the press stations in the middle, the Turnover Station where a panel must be reposed, and the End of Line that inspects and racks the output. The Die Set gives each press its shape, and the Control System keeps every stroke and transfer in step.
Feeding the blanks
Blanks arrive on pallets, stacked flat. The Blank Destacker sits over the pallet on a Lift Table that raises the stack as it empties so the top sheet always stays at pick height. Stacked oiled sheets cling together, so a Magnetic Fanner on each edge induces like magnetic poles in the top few sheets and they repel apart. A Vacuum Pick Head then lifts a single blank on its Vacuum Cup array and carries it off the stack. A Double-blank Detector checks that only one sheet was taken, because two blanks in the die would wreck the tooling.
The blank next passes through Blank Conditioning. The Blank Washer wipes off mill scale and dirt with felt rollers, the Blank Oiler lays an even film of drawing oil so the steel flows into the die without tearing, and the Centering Station reads the blank edges with cameras and nudges it to the exact position the first transfer expects. Position matters here because the draw die has no time to find a misplaced blank at line speed.
Forming in the lead press
The first and largest press does the hard work. The Slide of the Lead Draw Press carries the upper half of the Draw Die down onto the blank, driving it over the Draw Punch to stretch the flat steel into a deep panel. The press frame, a heavy Crown tied to the Press Bed by prestressed Upright columns, holds 1000 to 2500 tonnes of forming force without flexing enough to spoil the part. A mechanical Mechanical Drive stores energy in a Flywheel and releases it through a Clutch-brake for each stroke, so the motor sees a steady load while the slide delivers a brief peak.
A draw needs a counterforce on the blank edge or the panel wrinkles. The Die Cushion under the bed pushes up on the Blank Holder through a set of Cushion Pin supports, gripping the blank rim while the center is drawn down. A Hydraulic Pack sets that cushion force as a curve over slide position, and Draw Bead ribs in the holder restrain metal flow so the steel stretches where the part needs it.
Moving panels between presses
The panel must travel from each press to the next without a person reaching into a die. The Interpress Automation does this with either Transfer Robot units or Crossbar Feeder bars. A robot is a six-axis arm beside the line that reaches into the open die, grips the panel on its End Effector, swings it out, and sets it into the next press. A crossbar feeder spans the die on a light Crossbar of carbon fiber and indexes the part one station forward in a straight line, which is faster but less flexible. Some panels need a flip, so a Turnover Station with a Rotary Table turns the part over so the next die meets the correct face. Every transfer must clear the slide before it closes, which is why the line runs at 8 to 15 strokes per minute rather than the speed a single press could reach.
Tooling and die change
Each press holds one Die Set. The lead press carries the Draw Die, the next stations carry a Trim Die that shears off the excess flange and pierces holes, and later ones carry a Flange Die that bends edges up and restrikes the panel to tolerance. Each die half mounts on a Die Shoe that takes the tonnage. A line stamps one panel at a time, so switching to a new panel means changing every die. The Moving Bolster rolls a full die set out of each press and a preset one in, cutting changeover from hours to 10 to 20 minutes.
End of line and control
Finished panels ride the Exit Conveyor to the Inspection Station, where graze lighting and cameras flag splits, wrinkles, and missing pierces before the Panel Stacker racks good parts for the body shop. The whole line answers to the Control System. The Line Master PLC holds the line cycle and tells each press and transfer when to move, each Press Drive Cabinet runs one press motor and clutch, and a safety chain of Light Curtain barriers and interlocked fencing stops every stroke if anyone reaches in. Automotive variants differ mainly in transfer choice and press count: a robot line suits varied panels and frequent changeover, while a crossbar line suits high volume on a fixed set of parts.
Tandem Press Line parts and their functions
9 top-level parts · 2,434 parts in total · full bill of materials below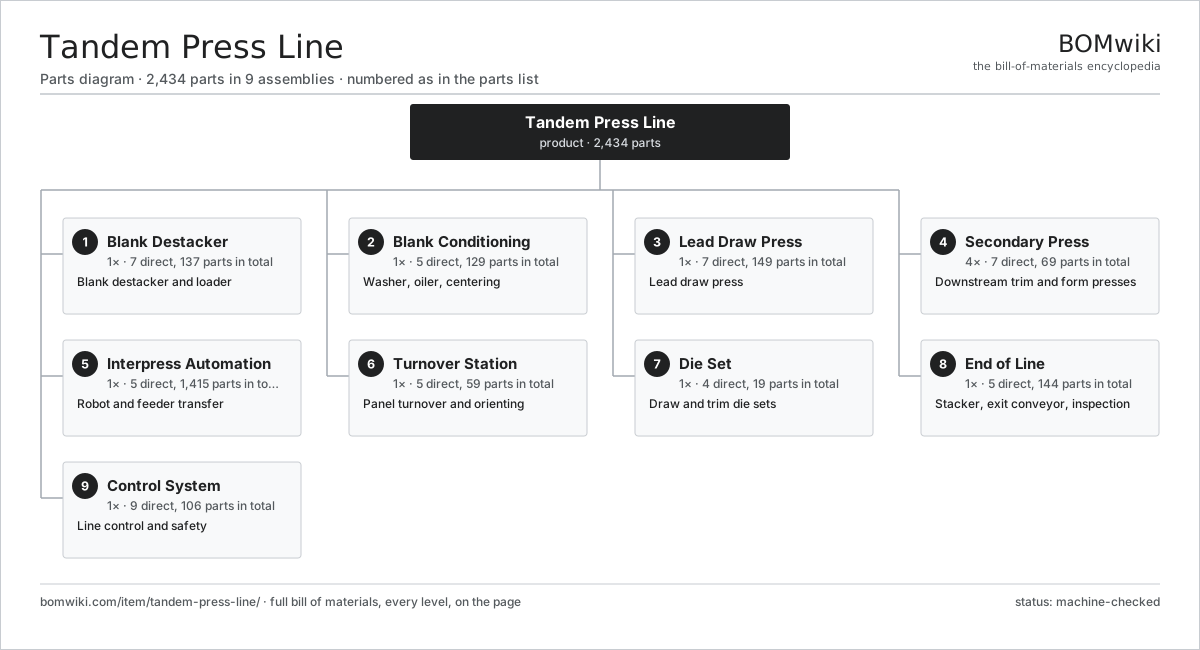
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Blank Destacker 7 parts | 1× | Blank destacker and loader |
| 2 | Blank Conditioning 5 parts | 1× | Washer, oiler, centering |
| 3 | Lead Draw Press 7 parts | 1× | Lead draw press |
| 4 | Secondary Press 7 parts | 4× | Downstream trim and form presses |
| 5 | Interpress Automation 5 parts | 1× | Robot and feeder transfer |
| 6 | Turnover Station 5 parts | 1× | Panel turnover and orienting |
| 7 | Die Set 4 parts | 1× | Draw and trim die sets |
| 8 | End of Line 5 parts | 1× | Stacker, exit conveyor, inspection |
| 9 | Control System 9 parts | 1× | Line control and safety |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Tandem Press Line
9 top-level lines · 133 rows shown · 2,434 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Blank Destacker 7 parts | tandem-press-line-destacker | 1× | 1 | 137 | assembly |
| 1.1 | Lift Table | tandem-press-line-lift-table | 2× | 2 | · | part |
| 1.2 | Magnetic Fanner | tandem-press-line-magnetic-fanner | 4× | 4 | · | part |
| 1.3 | Vacuum Pick Head 4 parts | tandem-press-line-vacuum-pickup | 1× | 1 | 31 | assembly |
| 1.3.1 | Vacuum Cup | tandem-press-line-vacuum-cup | 24× | 24 | · | part |
| 1.3.2 | Vacuum Pump | tandem-press-line-vacuum-pump | 2× | 2 | · | part |
| 1.3.3 | Cup Frame | tandem-press-line-cup-frame | 1× | 1 | · | part |
| 1.3.4 | Pressure Sensor | pressure-sensor | 4× | 4 | · | part |
| 1.4 | Double-blank Detector | tandem-press-line-double-blank-detector | 1× | 1 | · | part |
| 1.5 | Destack Gantry | tandem-press-line-destack-gantry | 1× | 1 | · | part |
| 1.6 | Servo Motor 4 parts | servo-motor | 4× | 4 | 24 | assembly |
| 1.6.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 4 | 3 | assembly |
| 1.6.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 4 | 19 | assembly |
| 1.6.3 | Encoder | encoder | 1× | 4 | · | part |
| 1.6.4 | Motor Housing | motor-housing | 1× | 4 | · | part |
| 1.7 | Ball Screw | ball-screw | 2× | 2 | · | part |
| 2 | Blank Conditioning 5 parts | tandem-press-line-blank-conditioning | 1× | 1 | 129 | assembly |
| 2.1 | Blank Washer 3 parts | tandem-press-line-blank-washer | 1× | 1 | 19 | assembly |
| 2.1.1 | Wash Roller | tandem-press-line-wash-roller | 6× | 6 | · | part |
| 2.1.2 | Wash Pump | tandem-press-line-wash-pump | 1× | 1 | · | part |
| 2.1.3 | Ball Bearing | ball-bearing | 12× | 12 | · | part |
| 2.2 | Blank Oiler | tandem-press-line-blank-oiler | 1× | 1 | · | part |
| 2.3 | Centering Station 3 parts | tandem-press-line-centering-station | 1× | 1 | 104 | assembly |
| 2.3.1 | Centering Camera | tandem-press-line-centering-camera | 4× | 4 | · | part |
| 2.3.2 | Centering Pusher | tandem-press-line-centering-pusher | 4× | 4 | · | part |
| 2.3.3 | Servo Motor 4 parts + deeper › | servo-motor | 4× | 4 | 24 | assembly |
| 2.4 | Feed Belt | tandem-press-line-feed-belt | 1× | 1 | · | part |
| 2.5 | Drive Belt | drive-belt | 4× | 4 | · | part |
| 3 | Lead Draw Press 7 parts | tandem-press-line-lead-press | 1× | 1 | 149 | assembly |
| 3.1 | Crown | tandem-press-line-press-crown | 1× | 1 | · | part |
| 3.2 | Upright | tandem-press-line-press-upright | 4× | 4 | · | part |
| 3.3 | Press Bed | tandem-press-line-press-bed | 1× | 1 | · | part |
| 3.4 | Slide 4 parts | tandem-press-line-press-slide | 1× | 1 | 17 | assembly |
| 3.4.1 | Slide Body | tandem-press-line-slide-body | 1× | 1 | · | part |
| 3.4.2 | Slide Gib | tandem-press-line-gib | 8× | 8 | · | part |
| 3.4.3 | Connecting Rod | tandem-press-line-connecting-rod | 4× | 4 | · | part |
| 3.4.4 | Overload Protector | tandem-press-line-overload-cylinder | 4× | 4 | · | part |
| 3.5 | Mechanical Drive 6 parts | tandem-press-line-press-drive | 1× | 1 | 42 | assembly |
| 3.5.1 | Flywheel | tandem-press-line-flywheel | 1× | 1 | · | part |
| 3.5.2 | Clutch-brake | tandem-press-line-clutch-brake | 1× | 1 | · | part |
| 3.5.3 | Eccentric Shaft | tandem-press-line-eccentric-shaft | 1× | 1 | · | part |
| 3.5.4 | Drive Gearbox 4 parts + deeper › | tandem-press-line-drive-gearbox | 1× | 1 | 9 | assembly |
| 3.5.5 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 3.5.6 | Drive Belt | drive-belt | 6× | 6 | · | part |
| 3.6 | Die Cushion 4 parts | tandem-press-line-die-cushion | 2× | 2 | 41 | assembly |
| 3.6.1 | Cushion Cylinder | tandem-press-line-cushion-cylinder | 4× | 8 | · | part |
| 3.6.2 | Cushion Pin | tandem-press-line-cushion-pin | 24× | 48 | · | part |
| 3.6.3 | Hydraulic Pack 4 parts + deeper › | tandem-press-line-hydraulic-pack | 1× | 2 | 9 | assembly |
| 3.6.4 | Pressure Sensor | pressure-sensor | 4× | 8 | · | part |
| 3.7 | Moving Bolster | tandem-press-line-moving-bolster | 2× | 2 | · | part |
| 4 | Secondary Press 7 parts | tandem-press-line-secondary-press | 4× | 4 | 69 | assembly |
| 4.1 | Crown | tandem-press-line-press-crown | 1× | 4 | · | part |
| 4.2 | Upright | tandem-press-line-press-upright | 4× | 16 | · | part |
| 4.3 | Press Bed | tandem-press-line-press-bed | 1× | 4 | · | part |
| 4.4 | Slide 4 parts | tandem-press-line-press-slide | 1× | 4 | 17 | assembly |
| 4.4.1 | Slide Body | tandem-press-line-slide-body | 1× | 4 | · | part |
| 4.4.2 | Slide Gib | tandem-press-line-gib | 8× | 32 | · | part |
| 4.4.3 | Connecting Rod | tandem-press-line-connecting-rod | 4× | 16 | · | part |
| 4.4.4 | Overload Protector | tandem-press-line-overload-cylinder | 4× | 16 | · | part |
| 4.5 | Mechanical Drive 6 parts | tandem-press-line-press-drive | 1× | 4 | 42 | assembly |
| 4.5.1 | Flywheel | tandem-press-line-flywheel | 1× | 4 | · | part |
| 4.5.2 | Clutch-brake | tandem-press-line-clutch-brake | 1× | 4 | · | part |
| 4.5.3 | Eccentric Shaft | tandem-press-line-eccentric-shaft | 1× | 4 | · | part |
| 4.5.4 | Drive Gearbox 4 parts + deeper › | tandem-press-line-drive-gearbox | 1× | 4 | 9 | assembly |
| 4.5.5 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 4 | 24 | assembly |
| 4.5.6 | Drive Belt | drive-belt | 6× | 24 | · | part |
| 4.6 | Scrap Chute | tandem-press-line-scrap-chute | 2× | 8 | · | part |
| 4.7 | Moving Bolster | tandem-press-line-moving-bolster | 2× | 8 | · | part |
| 5 | Interpress Automation 5 parts | tandem-press-line-interpress-automation | 1× | 1 | 1,415 | assembly |
| 5.1 | Transfer Robot 4 parts | tandem-press-line-transfer-robot | 6× | 6 | 152 | assembly |
| 5.1.1 | Robot Arm | tandem-press-line-robot-arm | 1× | 6 | · | part |
| 5.1.2 | Servo Motor 4 parts + deeper › | servo-motor | 6× | 36 | 24 | assembly |
| 5.1.3 | Helical Gear Pair | gear-pair | 6× | 36 | · | part |
| 5.1.4 | Robot Base | tandem-press-line-robot-base | 1× | 6 | · | part |
| 5.2 | Crossbar Feeder 4 parts | tandem-press-line-crossbar-feeder | 4× | 4 | 93 | assembly |
| 5.2.1 | Crossbar | tandem-press-line-crossbar | 1× | 4 | · | part |
| 5.2.2 | Vacuum Cup | tandem-press-line-vacuum-cup | 16× | 64 | · | part |
| 5.2.3 | Linear Guide Rail | linear-guide | 4× | 16 | · | part |
| 5.2.4 | Servo Motor 4 parts + deeper › | servo-motor | 3× | 12 | 24 | assembly |
| 5.3 | Interpress Shuttle | tandem-press-line-shuttle | 5× | 5 | · | part |
| 5.4 | End Effector 3 parts | tandem-press-line-end-effector | 12× | 12 | 10 | assembly |
| 5.4.1 | Tooling Frame | tandem-press-line-tooling-frame | 1× | 12 | · | part |
| 5.4.2 | Vacuum Cup | tandem-press-line-vacuum-cup | 8× | 96 | · | part |
| 5.4.3 | Quick Coupler | tandem-press-line-quick-coupler | 1× | 12 | · | part |
| 5.5 | Robot Controller | tandem-press-line-robot-controller | 6× | 6 | · | part |
| 6 | Turnover Station 5 parts | tandem-press-line-turnover-station | 1× | 1 | 59 | assembly |
| 6.1 | Rotary Table | tandem-press-line-rotary-table | 1× | 1 | · | part |
| 6.2 | Clamp Arm | tandem-press-line-clamp-arm | 4× | 4 | · | part |
| 6.3 | Servo Motor 4 parts | servo-motor | 2× | 2 | 24 | assembly |
| 6.3.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 2 | 3 | assembly |
| 6.3.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 2 | 19 | assembly |
| 6.3.3 | Encoder | encoder | 1× | 2 | · | part |
| 6.3.4 | Motor Housing | motor-housing | 1× | 2 | · | part |
| 6.4 | Helical Gear Pair | gear-pair | 2× | 2 | · | part |
| 6.5 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 7 | Die Set 4 parts | tandem-press-line-die-set | 1× | 1 | 19 | assembly |
| 7.1 | Draw Die 4 parts | tandem-press-line-draw-die | 1× | 1 | 11 | assembly |
| 7.1.1 | Draw Punch | tandem-press-line-die-punch | 1× | 1 | · | part |
| 7.1.2 | Draw Cavity | tandem-press-line-die-cavity | 1× | 1 | · | part |
| 7.1.3 | Blank Holder | tandem-press-line-blank-holder | 1× | 1 | · | part |
| 7.1.4 | Draw Bead | tandem-press-line-draw-bead | 8× | 8 | · | part |
| 7.2 | Trim Die | tandem-press-line-trim-die | 1× | 1 | · | part |
| 7.3 | Flange Die | tandem-press-line-flange-die | 1× | 1 | · | part |
| 7.4 | Die Shoe | tandem-press-line-die-shoe | 6× | 6 | · | part |
| 8 | End of Line 5 parts | tandem-press-line-end-of-line | 1× | 1 | 144 | assembly |
| 8.1 | Exit Conveyor | tandem-press-line-exit-conveyor | 1× | 1 | · | part |
| 8.2 | Inspection Station 3 parts | tandem-press-line-inspection-station | 1× | 1 | 11 | assembly |
| 8.2.1 | Inspection Camera | tandem-press-line-inspection-camera | 6× | 6 | · | part |
| 8.2.2 | Light Bank | tandem-press-line-light-bank | 4× | 4 | · | part |
| 8.2.3 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 8.3 | Panel Stacker 3 parts | tandem-press-line-panel-stacker | 1× | 1 | 118 | assembly |
| 8.3.1 | Stacker Robot | tandem-press-line-stacker-robot | 2× | 2 | · | part |
| 8.3.2 | End Effector 3 parts + deeper › | tandem-press-line-end-effector | 2× | 2 | 10 | assembly |
| 8.3.3 | Servo Motor 4 parts + deeper › | servo-motor | 4× | 4 | 24 | assembly |
| 8.4 | Shipping Rack | tandem-press-line-rack | 8× | 8 | · | part |
| 8.5 | Drive Belt | drive-belt | 6× | 6 | · | part |
| 9 | Control System 9 parts | tandem-press-line-control-system | 1× | 1 | 106 | assembly |
| 9.1 | Line Master PLC 4 parts | tandem-press-line-line-master-plc | 1× | 1 | 12 | assembly |
| 9.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 9.1.2 | Microcontroller | mcu | 2× | 2 | · | part |
| 9.1.3 | SMD Passive (R/C/L) | smd-passives | 1× | 1 | · | part |
| 9.1.4 | Connector | connector | 8× | 8 | · | part |
| 9.2 | Press Drive Cabinet 3 parts | tandem-press-line-press-drive-cabinet | 5× | 5 | 10 | assembly |
| 9.2.1 | Drive Inverter | tandem-press-line-vfd | 1× | 5 | · | part |
| 9.2.2 | Relay | relay | 8× | 40 | · | part |
| 9.2.3 | Power Supply | power-supply | 1× | 5 | · | part |
| 9.3 | Safety Controller | tandem-press-line-safety-controller | 1× | 1 | · | part |
| 9.4 | Light Curtain | tandem-press-line-light-curtain | 8× | 8 | · | part |
| 9.5 | Operator HMI | tandem-press-line-hmi | 3× | 3 | · | part |
| 9.6 | Perimeter Fencing | tandem-press-line-fencing | 1× | 1 | · | part |
| 9.7 | Power Supply | power-supply | 6× | 6 | · | part |
| 9.8 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 9.9 | Connector | connector | 24× | 24 | · | part |
Related products
same domain, ranked by shared parts Bevel Gear Generator
201 parts · shares 8 with this page
 Creep-Feed Grinder
571 parts · shares 8 with this page
Drag Finishing Machine
735 parts · shares 8 with this page
 Railway Wheel Lathe
1,201 parts · shares 8 with this page
 Rotary-Table Surface Grinder
172 parts · shares 8 with this page
 Shot Peening Machine
586 parts · shares 8 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
1,096-word article