Billet Shearing Machine
ProductOverview
A billet shearing machine cuts metal bar to length by shearing it cleanly in one stroke, the way scissors part paper, rather than sawing through it. It is the first station in most forging lines: continuous bar arrives, the shear crops it into equal billets, and those billets go straight to the furnace and the forge. Shearing makes no chip and removes no kerf, so unlike a saw it wastes no material and runs far faster, cropping a billet in a fraction of a second. The cut face is not flat and finished, but a forging blank does not need one, so the small distortion at the sheared end is acceptable and often pressed out in the first forging blow.
The machine drives a Cutting Ram carrying the moving blade through the bar against a fixed blade, all reacted by the Shear Frame. Energy comes from the Drive and Flywheel, the bar is indexed by the Bar Feed and Gauge, held by the Hydraulic System, and the cut billet leaves through the Slug Discharge, all sequenced by the Control System.
How the shear cuts
The cut happens between the Shear Blade Set. A Moving Blade on the ram drives the bar against the Fixed Blade in the frame, and the bar fails in shear along the plane between them. The secret to a clean billet is the Billet Bushing, a close support that grips the bar right at the cut so it shears straight across instead of bending and tearing. The gap between the two blades is set with Clearance Shims to a small percentage of the bar diameter: too tight and the blades chip, too loose and the cut tears with a long ragged burr. Because no metal is removed, the full bar becomes billets with only a short end crop as scrap.
Frame and ram
Shearing a thick bar releases a large, sudden force, so the Shear Frame must be very stiff or the blade gap would open under load and ruin the cut. The frame is either a heavy Frame Casting or a structure held in compression by pre-stressed Tie Rods, and the ram runs in adjustable Ram Gibs that keep it square. The Cutting Ram carries the load: a forged Ram Block drives the Blade Holder, rides on Wear Plates, and is moved by a Eccentric that converts shaft rotation into the straight cutting stroke.
Drive and stored energy
The shear stroke needs a burst of energy far larger than the motor can supply continuously, so the Drive and Flywheel stores it. A Drive Motor spins a heavy Flywheel up to speed between cuts; when the operator calls a stroke, a Stroke Clutch couples the flywheel to the Crankshaft for exactly one revolution, the Eccentric drives the ram down and back, and a Stop Brake stops the ram at top dead center ready for the next bar. This flywheel-clutch-crank arrangement is the same one used on mechanical forging presses.
Feed, clamping, and discharge
The Bar Feed and Gauge indexes the bar to length. Driven Pinch Rolls, a Servo Motor, and a programmable Length Gauge set the billet length, while a Roller Table carries long bar into the machine. During the cut the Hydraulic System hold everything still: a Hydraulic Pump feeds Clamp Cylinders that grip the bar and a Hold-down Cylinder that stops it lifting, all switched by a Valve Block. After the cut the Slug Discharge clears the zone: a Billet Kicker pushes the billet onto the Discharge Chute toward the forge, and the end crop drops into the Scrap Bin.
Hot shearing, control, and use
Many forge lines shear hot, heating the bar first so it crops with less force and less distortion, and the Control System uses a Temperature Sensor pyrometer to confirm the bar is in the right temperature window before firing. The Machine PLC sequences feed, clamp, and stroke, counts parts, and lets the operator set length and quantity from the Operator HMI. Billet shears feed automotive, fastener, bearing, and general drop-forging lines, anywhere large quantities of equal blanks are needed quickly with no material lost to a saw kerf. Where the cut face must be square and clean, a Cold Saw or Metal Cutting Band Saw is used instead, but for raw billet preparation the shear wins on speed and yield.
Cut quality, tooling, and maintenance
The quality of a sheared billet is judged not by a smooth face but by how square and undistorted the cut is and how little it deforms the bar near the end. The two biggest levers are the blade clearance set by the Clearance Shims and the support given by the Billet Bushing. Correct clearance lets the two fracture planes meet cleanly, while a worn or oversized gap drags the cut and leaves a long burr and a slanted face that wastes material in the first forging blow. Hot shearing helps because warm steel parts with less force and less burr, which is why higher-volume lines heat the bar and let the Temperature Sensor confirm the temperature window. The blades are the main tooling: a Moving Blade and Fixed Blade of hardened tool steel are rotated or reground as their edges round over, and the Billet Bushing is replaced as it wears to keep the cut supported. Maintenance also watches the Stroke Clutch and Stop Brake that must stop the ram reliably at top dead center, the Ram Gibs that hold blade alignment, and the Hydraulic System that clamp the bar. Kept in tune, a billet shear crops thousands of equal blanks an hour with almost no scrap, which is why it remains the standard front end of the forge shop despite its rough cut face.
Billet Shearing Machine parts and their functions
8 top-level parts · 100 parts in total · full bill of materials below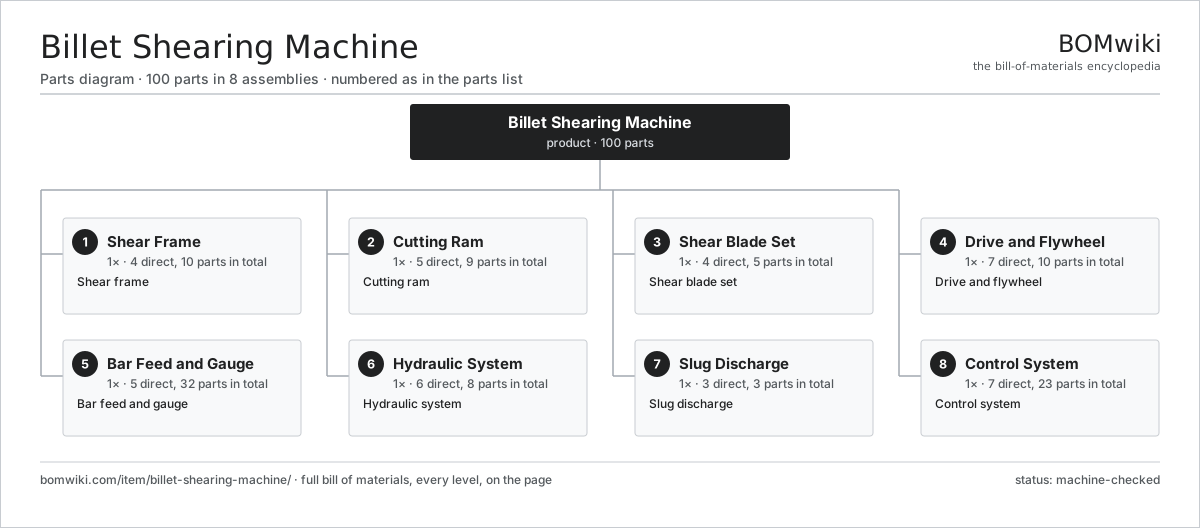
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Shear Frame 4 parts | 1× | Shear frame |
| 2 | Cutting Ram 5 parts | 1× | Cutting ram |
| 3 | Shear Blade Set 4 parts | 1× | Shear blade set |
| 4 | Drive and Flywheel 7 parts | 1× | Drive and flywheel |
| 5 | Bar Feed and Gauge 5 parts | 1× | Bar feed and gauge |
| 6 | Hydraulic System 6 parts | 1× | Hydraulic system |
| 7 | Slug Discharge 3 parts | 1× | Slug discharge |
| 8 | Control System 7 parts | 1× | Control system |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Billet Shearing Machine
8 top-level lines · 53 rows shown · 100 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Shear Frame 4 parts | billet-shearing-machine-frame | 1× | 1 | 10 | assembly |
| 1.1 | Frame Casting | billet-shearing-machine-frame-casting | 1× | 1 | · | part |
| 1.2 | Tie Rod | billet-shearing-machine-tie-rod | 4× | 4 | · | part |
| 1.3 | Ram Gib | billet-shearing-machine-gib | 4× | 4 | · | part |
| 1.4 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 2 | Cutting Ram 5 parts | billet-shearing-machine-ram | 1× | 1 | 9 | assembly |
| 2.1 | Ram Block | billet-shearing-machine-ram-block | 1× | 1 | · | part |
| 2.2 | Blade Holder | billet-shearing-machine-blade-holder | 1× | 1 | · | part |
| 2.3 | Wear Plate | billet-shearing-machine-wear-plate | 4× | 4 | · | part |
| 2.4 | Eccentric | billet-shearing-machine-eccentric | 1× | 1 | · | part |
| 2.5 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 3 | Shear Blade Set 4 parts | billet-shearing-machine-blade-set | 1× | 1 | 5 | assembly |
| 3.1 | Moving Blade | billet-shearing-machine-moving-blade | 1× | 1 | · | part |
| 3.2 | Fixed Blade | billet-shearing-machine-fixed-blade | 1× | 1 | · | part |
| 3.3 | Billet Bushing | billet-shearing-machine-billet-bushing | 2× | 2 | · | part |
| 3.4 | Clearance Shim | billet-shearing-machine-knife-gap-shim | 1× | 1 | · | part |
| 4 | Drive and Flywheel 7 parts | billet-shearing-machine-drive | 1× | 1 | 10 | assembly |
| 4.1 | Drive Motor | billet-shearing-machine-drive-motor | 1× | 1 | · | part |
| 4.2 | Flywheel | billet-shearing-machine-flywheel | 1× | 1 | · | part |
| 4.3 | Stroke Clutch | billet-shearing-machine-clutch | 1× | 1 | · | part |
| 4.4 | Stop Brake | billet-shearing-machine-brake | 1× | 1 | · | part |
| 4.5 | Crankshaft | billet-shearing-machine-crankshaft | 1× | 1 | · | part |
| 4.6 | Helical Gear Pair | gear-pair | 1× | 1 | · | part |
| 4.7 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 5 | Bar Feed and Gauge 5 parts | billet-shearing-machine-feed | 1× | 1 | 32 | assembly |
| 5.1 | Pinch Roll | billet-shearing-machine-pinch-roll | 2× | 2 | · | part |
| 5.2 | Length Gauge | billet-shearing-machine-length-gauge | 1× | 1 | · | part |
| 5.3 | Roller Table | billet-shearing-machine-roller-table | 1× | 1 | · | part |
| 5.4 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 5.4.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 5.4.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 5.4.3 | Encoder | encoder | 1× | 1 | · | part |
| 5.4.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 5.5 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 6 | Hydraulic System 6 parts | billet-shearing-machine-hydraulics | 1× | 1 | 8 | assembly |
| 6.1 | Hydraulic Pump | billet-shearing-machine-hydraulic-pump | 1× | 1 | · | part |
| 6.2 | Clamp Cylinder | billet-shearing-machine-clamp-cylinder | 2× | 2 | · | part |
| 6.3 | Hold-down Cylinder | billet-shearing-machine-holddown-cylinder | 1× | 1 | · | part |
| 6.4 | Valve Block | billet-shearing-machine-valve-block | 1× | 1 | · | part |
| 6.5 | Pressure Sensor | pressure-sensor | 2× | 2 | · | part |
| 6.6 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 7 | Slug Discharge 3 parts | billet-shearing-machine-discharge | 1× | 1 | 3 | assembly |
| 7.1 | Discharge Chute | billet-shearing-machine-discharge-chute | 1× | 1 | · | part |
| 7.2 | Scrap Bin | billet-shearing-machine-scrap-bin | 1× | 1 | · | part |
| 7.3 | Billet Kicker | billet-shearing-machine-kicker | 1× | 1 | · | part |
| 8 | Control System 7 parts | billet-shearing-machine-control | 1× | 1 | 23 | assembly |
| 8.1 | Machine PLC | billet-shearing-machine-plc | 1× | 1 | · | part |
| 8.2 | Operator HMI | billet-shearing-machine-hmi | 1× | 1 | · | part |
| 8.3 | Temperature Sensor | billet-shearing-machine-hot-shear-sensor | 1× | 1 | · | part |
| 8.4 | Relay | relay | 8× | 8 | · | part |
| 8.5 | Power Supply | power-supply | 1× | 1 | · | part |
| 8.6 | Connector | connector | 10× | 10 | · | part |
| 8.7 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Bed-Type Milling Machine
151 parts · shares 3 with this page
 Bevel Gear Generator
201 parts · shares 3 with this page
Centering and Facing Machine
1,419 parts · shares 3 with this page
CNC Tube Bender
131 parts · shares 3 with this page
Cold Rolling Mill
991 parts · shares 3 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
1,105-word article