Cut-to-Length Line
ProductOverview
A cut-to-length line turns a coil of metal strip into a stack of flat, square sheets cut to an exact length. The strip is paid off a reel, pulled straight, flattened in a roller leveler, fed forward in measured steps and sheared across its width, after which each sheet is conveyed to a stack. The whole machine exists to do two things well: make the sheet truly flat, and cut it to a length that holds tolerance over thousands of cuts. Steel, stainless, aluminum and coated products all run on the same line with recipe changes for tension, leveler intermesh and blade gap.
The line is laid out in process order. The Entry Section handles the coil, the Pinch and Feed Section grips and centers the strip, the Roller Leveler flattens it, the Loop Pit holds slack, the Servo Roll Feeder meters length, the Flying Shear cuts, and the Stacker and Exit Conveyor piles the sheets. Behind all of this sit the Hydraulic Power Unit and the Drive and Control System, carried on a common Machine Frame.
Entry and pay-off
The coil arrives on the Coil Loading Car, a hydraulic V-saddle car that lifts the coil and presents its bore to the Expanding Mandrel of the Uncoiler. The mandrel expands inside the coil bore through its Mandrel Expansion Cylinder, and a Servo Motor holds back-tension so the strip pays off without slack. The Peeler and Threading Table lifts the loose head end off the wrap and threads it across the Threading Table, while the Hold-Down and Snubber Roll presses the wrap to stop the coil from springing open.
Feed and leveling
From the reel the strip enters the Entry Pinch Roll Unit, which drives it forward, and the Strip Edge Guide, which keeps it centered using Edge Position Sensor feedback so the sheets come off square. The strip then runs into the Roller Leveler, the part that decides sheet flatness. Inside the Leveler Roll Cassette a row of small Leveling Work Roll rolls bends the strip alternately up and down. Small diameter matters: a thin roll bends the strip sharply, which is what drives the surface fibers past yield and erases coil set. Because such slender rolls would deflect under load, each is propped by Backup Roll rolls. How far the upper rolls reach down between the lower rolls is set by the Intermesh Adjustment Actuator through its Intermesh Adjusting Screw, with the gap read back by a Roll Position Transducer. The whole cassette is a quick-change unit pulled on the Cassette Change Cradle when a different product needs a different roll set.
Loop and length measurement
The leveler runs continuously, but the shear cuts in stops and starts, so the two are decoupled by the Loop Pit. A free loop of strip hangs in a lined floor pit, and Loop Height Sensor units watch its depth so the leveler entry speed and the feeder pull speed stay balanced. Downstream the Servo Roll Feeder pulls a measured length of strip and stops it dead. Its Feed Roll rolls advance the strip while a separate Measuring Roll reads true fed length on a Length Encoder, independent of any roll slip. Between cuts the Feeder Release Clamp lifts so the strip floats free while the shear works.
Shearing
The Flying Shear cuts the sheet to length. The Upper Shear Blade and Lower Shear Blade are tool steel, and the clearance between them is set for strip thickness and grade by the Blade Gap Adjuster. The cut is driven by the Shear Cutting Cylinder pair while the Shear Hold-Down Clamp pins the strip flat so the cut edge stays square. On a flying shear the Shear Carriage accelerates the whole shear up to line speed during the cut, so the strip never has to stop, which is how high cut rates are reached.
Stacking and support
Each cut sheet is caught by the Magnetic Belt Conveyor, whose Magnet Bar elements hold the steel against the belt and carry it clear of the shear. At the Drop Stacker the magnetic hold is broken so the sheet falls onto the Stacking Table, which lowers as the pile grows and squares it with side and back gauges. Defect sheets and the leading scrap end are thrown aside by the Scrap Ejector before they reach the stack. Hydraulic power for the shear stroke and the mandrel comes from the Hydraulic Power Unit, with an Bladder Accumulator giving the shear a fast stroke. The Drive and Control System ties it together: the Length Cut Controller fires the shear at the measured length and counts sheets per batch, the Line PLC runs the line sequence, and the operator sets cut-length recipes at the Operator HMI.
Cut-to-Length Line parts and their functions
10 top-level parts · 500 parts in total · full bill of materials below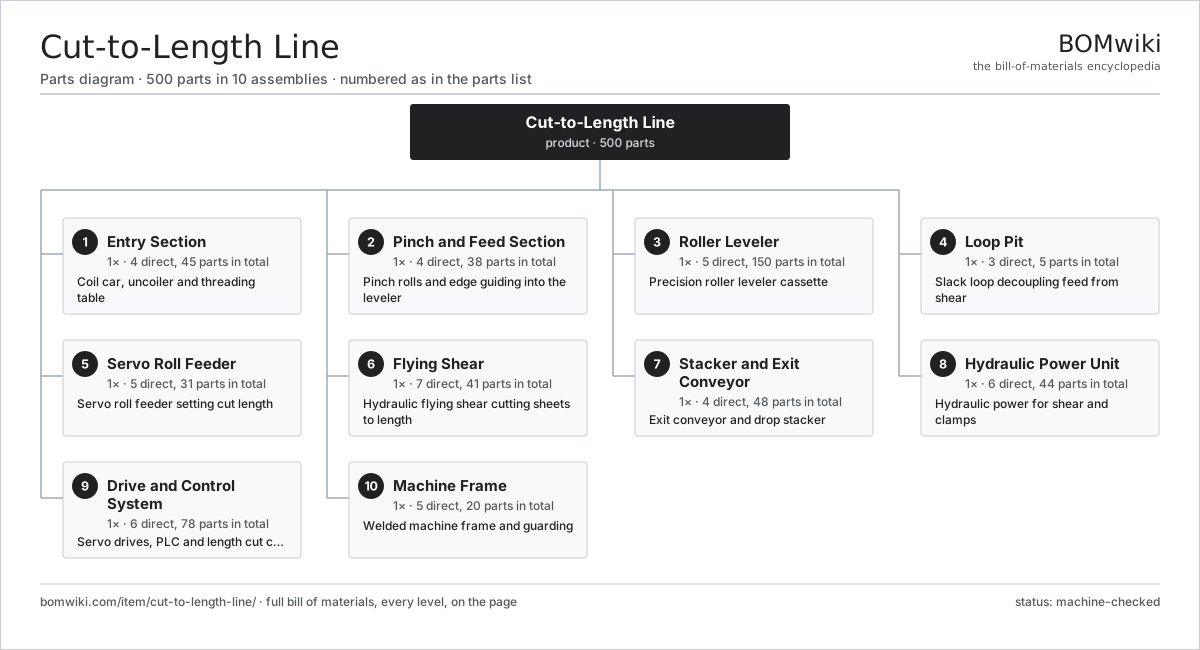
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Entry Section 4 parts | 1× | Coil car, uncoiler and threading table |
| 2 | Pinch and Feed Section 4 parts | 1× | Pinch rolls and edge guiding into the leveler |
| 3 | Roller Leveler 5 parts | 1× | Precision roller leveler cassette |
| 4 | Loop Pit 3 parts | 1× | Slack loop decoupling feed from shear |
| 5 | Servo Roll Feeder 5 parts | 1× | Servo roll feeder setting cut length |
| 6 | Flying Shear 7 parts | 1× | Hydraulic flying shear cutting sheets to length |
| 7 | Stacker and Exit Conveyor 4 parts | 1× | Exit conveyor and drop stacker |
| 8 | Hydraulic Power Unit 6 parts | 1× | Hydraulic power for shear and clamps |
| 9 | Drive and Control System 6 parts | 1× | Servo drives, PLC and length cut control |
| 10 | Machine Frame 5 parts | 1× | Welded machine frame and guarding |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Cut-to-Length Line
10 top-level lines · 152 rows shown · 500 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Entry Section 4 parts | cut-to-length-line-entry-section | 1× | 1 | 45 | assembly |
| 1.1 | Coil Loading Car 3 parts | cut-to-length-line-coil-car | 1× | 1 | 7 | assembly |
| 1.1.1 | V-Saddle Cradle | cut-to-length-line-car-saddle | 1× | 1 | · | part |
| 1.1.2 | Car Lift Cylinder | cut-to-length-line-car-cylinder | 2× | 2 | · | part |
| 1.1.3 | Car Travel Wheel | cut-to-length-line-car-wheel | 4× | 4 | · | part |
| 1.2 | Uncoiler 5 parts | cut-to-length-line-uncoiler | 1× | 1 | 29 | assembly |
| 1.2.1 | Expanding Mandrel | cut-to-length-line-mandrel | 1× | 1 | · | part |
| 1.2.2 | Mandrel Expansion Cylinder | cut-to-length-line-mandrel-cylinder | 1× | 1 | · | part |
| 1.2.3 | Uncoiler Gearbox | cut-to-length-line-uncoiler-gearbox | 1× | 1 | · | part |
| 1.2.4 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 1.2.5 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 1.3 | Peeler and Threading Table 4 parts | cut-to-length-line-peeler | 1× | 1 | 4 | assembly |
| 1.3.1 | Peeler Arm | cut-to-length-line-peeler-arm | 1× | 1 | · | part |
| 1.3.2 | Peeler Pinch Roll | cut-to-length-line-peeler-roll | 1× | 1 | · | part |
| 1.3.3 | Threading Table | cut-to-length-line-threading-table | 1× | 1 | · | part |
| 1.3.4 | Pneumatic Cylinder | pneumatic-cylinder | 1× | 1 | · | part |
| 1.4 | Hold-Down and Snubber Roll 3 parts | cut-to-length-line-hold-down | 1× | 1 | 5 | assembly |
| 1.4.1 | Snubber Roll | cut-to-length-line-snubber-roll | 1× | 1 | · | part |
| 1.4.2 | Pneumatic Cylinder | pneumatic-cylinder | 2× | 2 | · | part |
| 1.4.3 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 2 | Pinch and Feed Section 4 parts | cut-to-length-line-feed-section | 1× | 1 | 38 | assembly |
| 2.1 | Entry Pinch Roll Unit 4 parts | cut-to-length-line-pinch-roll | 1× | 1 | 8 | assembly |
| 2.1.1 | Lower Pinch Roll | cut-to-length-line-pinch-roll-lower | 1× | 1 | · | part |
| 2.1.2 | Upper Pinch Roll | cut-to-length-line-pinch-roll-upper | 1× | 1 | · | part |
| 2.1.3 | Pneumatic Cylinder | pneumatic-cylinder | 2× | 2 | · | part |
| 2.1.4 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 2.2 | Strip Edge Guide 3 parts | cut-to-length-line-edge-guide | 1× | 1 | 5 | assembly |
| 2.2.1 | Guide Roll | cut-to-length-line-guide-roll | 2× | 2 | · | part |
| 2.2.2 | Edge Position Sensor | cut-to-length-line-edge-sensor | 2× | 2 | · | part |
| 2.2.3 | Guide Positioning Actuator | cut-to-length-line-guide-actuator | 1× | 1 | · | part |
| 2.3 | Feed Gearbox | cut-to-length-line-feed-gearbox | 1× | 1 | · | part |
| 2.4 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 2.4.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 2.4.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 2.4.3 | Encoder | encoder | 1× | 1 | · | part |
| 2.4.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 3 | Roller Leveler 5 parts | cut-to-length-line-leveler | 1× | 1 | 150 | assembly |
| 3.1 | Leveler Roll Cassette 4 parts | cut-to-length-line-leveler-cassette | 1× | 1 | 54 | assembly |
| 3.1.1 | Leveling Work Roll | cut-to-length-line-work-roll | 11× | 11 | · | part |
| 3.1.2 | Backup Roll | cut-to-length-line-backup-roll | 20× | 20 | · | part |
| 3.1.3 | Cassette Frame | cut-to-length-line-cassette-frame | 1× | 1 | · | part |
| 3.1.4 | Ball Bearing | ball-bearing | 22× | 22 | · | part |
| 3.2 | Intermesh Adjustment Actuator 4 parts | cut-to-length-line-intermesh-actuator | 2× | 2 | 35 | assembly |
| 3.2.1 | Intermesh Adjusting Screw | cut-to-length-line-intermesh-screw | 1× | 2 | · | part |
| 3.2.2 | Roll Position Transducer | cut-to-length-line-position-transducer | 1× | 2 | · | part |
| 3.2.3 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 2 | 24 | assembly |
| 3.2.4 | Helical Gearbox 4 parts + deeper › | gearbox | 1× | 2 | 9 | assembly |
| 3.3 | Leveler Gearbox | cut-to-length-line-leveler-gearbox | 1× | 1 | · | part |
| 3.4 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 3.4.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 3.4.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 3.4.3 | Encoder | encoder | 1× | 1 | · | part |
| 3.4.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 3.5 | Cassette Change Cradle | cut-to-length-line-cassette-changer | 1× | 1 | · | part |
| 4 | Loop Pit 3 parts | cut-to-length-line-loop-pit | 1× | 1 | 5 | assembly |
| 4.1 | Loop Deflector Roll | cut-to-length-line-loop-roll | 2× | 2 | · | part |
| 4.2 | Loop Height Sensor | cut-to-length-line-loop-sensor | 2× | 2 | · | part |
| 4.3 | Pit Liner | cut-to-length-line-pit-liner | 1× | 1 | · | part |
| 5 | Servo Roll Feeder 5 parts | cut-to-length-line-roll-feeder | 1× | 1 | 31 | assembly |
| 5.1 | Feed Roll | cut-to-length-line-feeder-roll | 2× | 2 | · | part |
| 5.2 | Feeder Release Clamp | cut-to-length-line-feeder-clamp | 1× | 1 | · | part |
| 5.3 | Measuring Roll 2 parts | cut-to-length-line-measuring-roll | 1× | 1 | 3 | assembly |
| 5.3.1 | Length Encoder | cut-to-length-line-encoder | 1× | 1 | · | part |
| 5.3.2 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 5.4 | Feeder Gearbox | cut-to-length-line-feeder-gearbox | 1× | 1 | · | part |
| 5.5 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 5.5.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 5.5.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 5.5.3 | Encoder | encoder | 1× | 1 | · | part |
| 5.5.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 6 | Flying Shear 7 parts | cut-to-length-line-shear | 1× | 1 | 41 | assembly |
| 6.1 | Shear Frame | cut-to-length-line-shear-frame | 1× | 1 | · | part |
| 6.2 | Upper Shear Blade | cut-to-length-line-upper-blade | 1× | 1 | · | part |
| 6.3 | Lower Shear Blade | cut-to-length-line-lower-blade | 1× | 1 | · | part |
| 6.4 | Blade Gap Adjuster 2 parts | cut-to-length-line-blade-gap-adjuster | 1× | 1 | 3 | assembly |
| 6.4.1 | Gap Adjustment Wedge | cut-to-length-line-gap-wedge | 1× | 1 | · | part |
| 6.4.2 | Gap Adjusting Screw | cut-to-length-line-gap-screw | 2× | 2 | · | part |
| 6.5 | Shear Cutting Cylinder | cut-to-length-line-shear-cylinder | 2× | 2 | · | part |
| 6.6 | Shear Carriage 4 parts | cut-to-length-line-shear-carriage | 1× | 1 | 29 | assembly |
| 6.6.1 | Carriage Rail | cut-to-length-line-carriage-rail | 2× | 2 | · | part |
| 6.6.2 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 6.6.3 | Ball Screw | ball-screw | 1× | 1 | · | part |
| 6.6.4 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 6.7 | Shear Hold-Down Clamp 2 parts | cut-to-length-line-hold-down-clamp | 1× | 1 | 4 | assembly |
| 6.7.1 | Clamp Pad | cut-to-length-line-clamp-pad | 2× | 2 | · | part |
| 6.7.2 | Pneumatic Cylinder | pneumatic-cylinder | 2× | 2 | · | part |
| 7 | Stacker and Exit Conveyor 4 parts | cut-to-length-line-stacker | 1× | 1 | 48 | assembly |
| 7.1 | Magnetic Belt Conveyor 4 parts | cut-to-length-line-magnetic-conveyor | 1× | 1 | 36 | assembly |
| 7.1.1 | Conveyor Belt | cut-to-length-line-conveyor-belt | 2× | 2 | · | part |
| 7.1.2 | Magnet Bar | cut-to-length-line-magnet-bar | 6× | 6 | · | part |
| 7.1.3 | Conveyor Roller | cut-to-length-line-conveyor-roller | 4× | 4 | · | part |
| 7.1.4 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 7.2 | Drop Stacker 3 parts | cut-to-length-line-drop-stacker | 1× | 1 | 4 | assembly |
| 7.2.1 | Drop Gate | cut-to-length-line-drop-gate | 1× | 1 | · | part |
| 7.2.2 | Front Stop | cut-to-length-line-front-stop | 1× | 1 | · | part |
| 7.2.3 | Pneumatic Cylinder | pneumatic-cylinder | 2× | 2 | · | part |
| 7.3 | Stacking Table 4 parts | cut-to-length-line-stack-table | 1× | 1 | 6 | assembly |
| 7.3.1 | Lift Table | cut-to-length-line-lift-table | 1× | 1 | · | part |
| 7.3.2 | Side Gauge | cut-to-length-line-side-gauge | 2× | 2 | · | part |
| 7.3.3 | Back Gauge | cut-to-length-line-back-gauge | 1× | 1 | · | part |
| 7.3.4 | Table Lift Cylinder | cut-to-length-line-lift-cylinder | 2× | 2 | · | part |
| 7.4 | Scrap Ejector 2 parts | cut-to-length-line-scrap-ejector | 1× | 1 | 2 | assembly |
| 7.4.1 | Ejector Flap | cut-to-length-line-ejector-flap | 1× | 1 | · | part |
| 7.4.2 | Pneumatic Cylinder | pneumatic-cylinder | 1× | 1 | · | part |
| 8 | Hydraulic Power Unit 6 parts | cut-to-length-line-hydraulic-unit | 1× | 1 | 44 | assembly |
| 8.1 | Hydraulic Pump 3 parts | cut-to-length-line-hydraulic-pump | 1× | 1 | 26 | assembly |
| 8.1.1 | Axial Piston Pump | cut-to-length-line-piston-pump | 1× | 1 | · | part |
| 8.1.2 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 8.1.3 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 8.2 | Hydraulic Reservoir 3 parts | cut-to-length-line-hydraulic-tank | 1× | 1 | 3 | assembly |
| 8.2.1 | Reservoir Shell | cut-to-length-line-tank-shell | 1× | 1 | · | part |
| 8.2.2 | Return Line Filter | cut-to-length-line-return-filter | 1× | 1 | · | part |
| 8.2.3 | Oil Level Switch | cut-to-length-line-level-switch | 1× | 1 | · | part |
| 8.3 | Valve Manifold 3 parts | cut-to-length-line-valve-manifold | 1× | 1 | 9 | assembly |
| 8.3.1 | Directional Valve | cut-to-length-line-directional-valve | 4× | 4 | · | part |
| 8.3.2 | Check Valve | cut-to-length-line-check-valve | 4× | 4 | · | part |
| 8.3.3 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 8.4 | Bladder Accumulator | cut-to-length-line-accumulator | 2× | 2 | · | part |
| 8.5 | Oil Cooler | cut-to-length-line-oil-cooler | 1× | 1 | · | part |
| 8.6 | Pressure Sensor | pressure-sensor | 3× | 3 | · | part |
| 9 | Drive and Control System 6 parts | cut-to-length-line-control-system | 1× | 1 | 78 | assembly |
| 9.1 | Servo Drive 4 parts | cut-to-length-line-servo-drive | 4× | 4 | 12 | assembly |
| 9.1.1 | Bare PCB | pcb-bare | 1× | 4 | · | part |
| 9.1.2 | IGBT Power Module | igbt-module | 6× | 24 | · | part |
| 9.1.3 | DC-Link Capacitor | dc-link-cap | 4× | 16 | · | part |
| 9.1.4 | Microcontroller | mcu | 1× | 4 | · | part |
| 9.2 | Line PLC 4 parts | cut-to-length-line-plc | 1× | 1 | 8 | assembly |
| 9.2.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 9.2.2 | Microcontroller | mcu | 2× | 2 | · | part |
| 9.2.3 | PLC I/O Module | cut-to-length-line-io-module | 4× | 4 | · | part |
| 9.2.4 | Power Supply | power-supply | 1× | 1 | · | part |
| 9.3 | Operator HMI 3 parts | cut-to-length-line-hmi | 1× | 1 | 3 | assembly |
| 9.3.1 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 9.3.2 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 9.3.3 | Microcontroller | mcu | 1× | 1 | · | part |
| 9.4 | Length Cut Controller 4 parts | cut-to-length-line-cut-controller | 1× | 1 | 8 | assembly |
| 9.4.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 9.4.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 9.4.3 | Relay | relay | 2× | 2 | · | part |
| 9.4.4 | Connector | connector | 4× | 4 | · | part |
| 9.5 | Drive Cabinet 4 parts | cut-to-length-line-drive-cabinet | 1× | 1 | 10 | assembly |
| 9.5.1 | Sheet Metal Panel | sheet-panel | 6× | 6 | · | part |
| 9.5.2 | Power Supply | power-supply | 1× | 1 | · | part |
| 9.5.3 | Cabinet Cooling Fan | cut-to-length-line-cabinet-fan | 2× | 2 | · | part |
| 9.5.4 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 9.6 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 10 | Machine Frame 5 parts | cut-to-length-line-frame | 1× | 1 | 20 | assembly |
| 10.1 | Base Frame | cut-to-length-line-base-frame | 1× | 1 | · | part |
| 10.2 | Leveler Stand Housing | cut-to-length-line-leveler-housing | 1× | 1 | · | part |
| 10.3 | Safety Guard Panel | cut-to-length-line-guard-panel | 8× | 8 | · | part |
| 10.4 | Maintenance Walkway | cut-to-length-line-walkway | 2× | 2 | · | part |
| 10.5 | Leveling Foot | cut-to-length-line-leveling-foot | 8× | 8 | · | part |
Related products
same domain, ranked by shared parts Compression Spring Coiler
1,167 parts · shares 9 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
959-word article