Vertical Honing Machine
ProductOverview
Honing is the finishing step that gives a bore its final size, its roundness and its surface texture. A tool carrying several abrasive stones rotates inside the bore while it strokes up and down, and the stones are pressed outward against the wall as they cut. The two motions together lay a crosshatch of fine scratches across the surface, and because the tool floats and rides on its own stones rather than on a fixed spindle, it averages out the errors a previous boring or grinding operation left behind. Honing corrects taper, barrel shape and out-of-round, holds size to a couple of microns, and leaves the controlled crosshatch that an engine cylinder needs to hold an oil film. It is the standard finish for cylinder bores, hydraulic cylinders, gears, bearing races and gun barrels.
This is a single-spindle vertical machine. The part sits in a Floating Fixture on the Worktable & Fixture, and the Rotating Spindle Head lowers the Honing Tool & Stones into the bore, turns it and strokes it through while expanding the stones against the wall.
How it works
Three motions combine. The Spindle Motor turns the tool, the Stroking Drive raises and lowers it, and the Stone Feed Mechanism expands the stones outward as they cut and wear. The ratio of rotation speed to stroke speed sets the crosshatch angle, a shallow angle for a fine sealing surface and a steeper one to hold more oil. The stroke is set so the stones overrun a little at each end of the bore, which is what keeps the bore straight instead of bell-mouthed. Because the Universal Driveshaft floats on universal joints, the tool centres itself in the bore and the Guide Shoe keeps it round, so the finished bore takes its axis from the hone, not from the machine spindle.
Pressing the stones is done one of two ways. Force feed holds a set radial pressure through the Feed Force Sensor, letting the stones cut at a steady rate as they wear; size feed advances the Expansion Cone to a set diameter through the Feed Servo. Most precision work uses size feed closed against an in-process gauge.
The tool and stones
The Honing Tool & Stones is a slotted body holding four to eight Abrasive Stone sticks around its circumference in carriers that ride the expansion cone. Vitrified aluminium-oxide or silicon-carbide stones suit cast iron and steel; diamond and CBN stones hone hardened steel and carbide and last far longer. As a stone wears, its Stone Shoe is pushed further out by the cone so the bearing pressure stays even. Selecting grit and bond is how the operator trades stock removal against final finish: a coarse stone roughs the bore to size, a fine stone follows to bring up the surface and refine the crosshatch.
Sizing and gauging
What makes honing repeatable is measuring the bore while it is being cut. The In-Process Gauging system uses an air plug whose back-pressure changes with the bore diameter, read by the Gauge Amplifier. As the bore opens up the signal climbs, and the moment it reaches the target the control tells the feed to retract and the cycle to end. With gauging in the loop a machine holds size to about two microns part after part, which no timed or open-loop hone can manage because stone wear and material variation would let the size drift.
Coolant and swarf
Honing makes a lot of fine swarf and abrasive fines that must be flushed away or they would scratch the bore and glaze the stones. The Coolant System floods the bore with honing oil through the Flush Nozzle jets, and the returning oil passes through a Fine Filter fine enough to take out the fines before the oil is used again. Clean oil keeps the stones cutting freely and protects the finish.
Use and variants
A typical job is finishing a hydraulic cylinder bore to a precise diameter with a crosshatch that holds the rod seal's oil film. The operator loads the part, picks the tool and recipe, sets the gauge target, and the machine roughs and finishes the bore to size on its own. Single-spindle machines like this one suit a wide range of parts; multi-spindle machines hone several bores at once for engine-block production, and horizontal machines handle long bores like gun barrels and hydraulic tubes. Across the family the principle is the same: a floating, stroking abrasive tool that finishes a bore to size, roundness and a controlled texture in one operation.
Control and safety
The Control coordinates speed, stroke and feed, sets the crosshatch angle and ends the cycle on the gauge signal, with the Operator Display showing size, stroke and stone load. The Enclosure & Guards contains the oil mist and guards the stroke zone, the Interlock Switch stops motion when a guard opens, the Mist Extractor clears the mist the spinning tool throws, and the Emergency Stop halts everything at once.
Vertical Honing Machine parts and their functions
10 top-level parts · 428 parts in total · full bill of materials below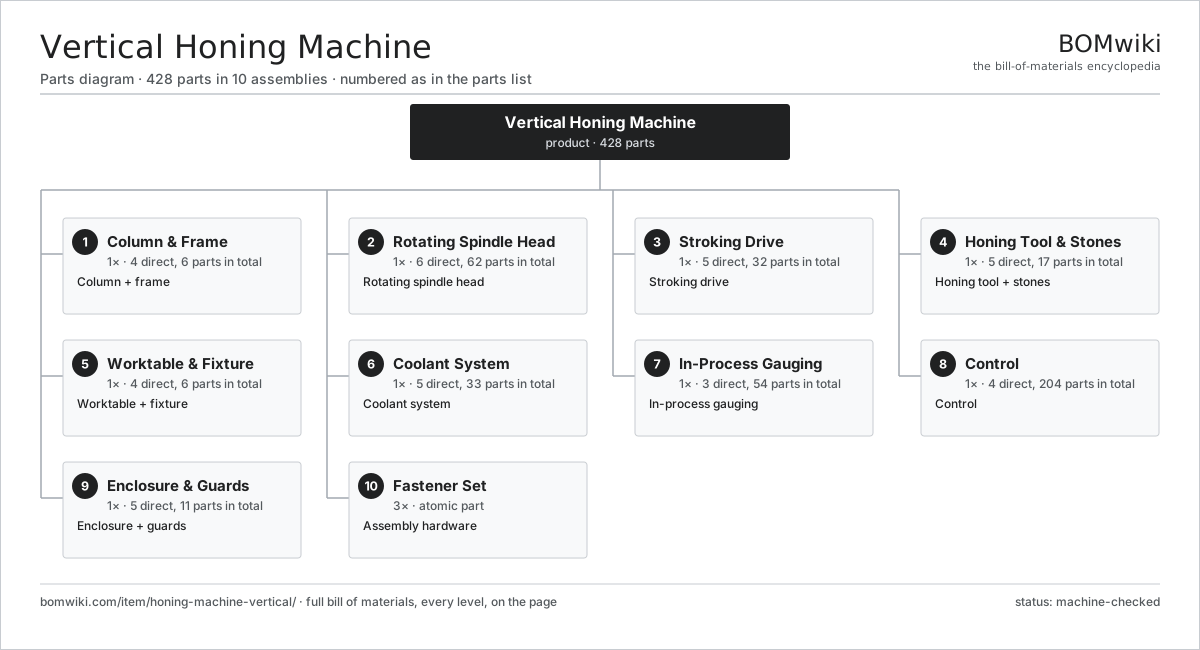
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Column & Frame 4 parts | 1× | Column + frame |
| 2 | Rotating Spindle Head 6 parts | 1× | Rotating spindle head |
| 3 | Stroking Drive 5 parts | 1× | Stroking drive |
| 4 | Honing Tool & Stones 5 parts | 1× | Honing tool + stones |
| 5 | Worktable & Fixture 4 parts | 1× | Worktable + fixture |
| 6 | Coolant System 5 parts | 1× | Coolant system |
| 7 | In-Process Gauging 3 parts | 1× | In-process gauging |
| 8 | Control 4 parts | 1× | Control |
| 9 | Enclosure & Guards 5 parts | 1× | Enclosure + guards |
| 10 | Fastener Set | 3× | Assembly hardware |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Vertical Honing Machine
10 top-level lines · 81 rows shown · 428 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Column & Frame 4 parts | honing-frame | 1× | 1 | 6 | assembly |
| 1.1 | Base | honing-base | 1× | 1 | · | part |
| 1.2 | Column | honing-column | 1× | 1 | · | part |
| 1.3 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 1.4 | Fastener Set | fastener-set | 2× | 2 | · | part |
| 2 | Rotating Spindle Head 6 parts | honing-spindle-head | 1× | 1 | 62 | assembly |
| 2.1 | Spindle Motor 5 parts | honing-spindle-motor | 1× | 1 | 26 | assembly |
| 2.1.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 2.1.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 2.1.3 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 2.1.4 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 2.1.5 | Encoder | encoder | 1× | 1 | · | part |
| 2.2 | Hone Spindle | honing-spindle | 1× | 1 | · | part |
| 2.3 | Stone Feed Mechanism 4 parts | honing-feed-mechanism | 1× | 1 | 28 | assembly |
| 2.3.1 | Feed Servo 4 parts + deeper › | honing-feed-servo | 1× | 1 | 25 | assembly |
| 2.3.2 | Expansion Feed Rod | honing-feed-rod | 1× | 1 | · | part |
| 2.3.3 | Expansion Cone | honing-feed-cone | 1× | 1 | · | part |
| 2.3.4 | Feed Force Sensor | honing-force-sensor | 1× | 1 | · | part |
| 2.4 | Universal Driveshaft | honing-driveshaft | 1× | 1 | · | part |
| 2.5 | Angular Contact Bearing | angular-bearing | 4× | 4 | · | part |
| 2.6 | Oil Seal | oil-seal | 2× | 2 | · | part |
| 3 | Stroking Drive 5 parts | honing-stroke-drive | 1× | 1 | 32 | assembly |
| 3.1 | Stroke Servo 5 parts | honing-stroke-servo | 1× | 1 | 26 | assembly |
| 3.1.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 3.1.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 3.1.3 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 3.1.4 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 3.1.5 | Encoder | encoder | 1× | 1 | · | part |
| 3.2 | Ball Screw | ball-screw | 1× | 1 | · | part |
| 3.3 | Head Slide | honing-slide | 1× | 1 | · | part |
| 3.4 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 3.5 | Limit Switch | limit-switch | 2× | 2 | · | part |
| 4 | Honing Tool & Stones 5 parts | honing-tool | 1× | 1 | 17 | assembly |
| 4.1 | Tool Body | honing-tool-body | 1× | 1 | · | part |
| 4.2 | Abrasive Stone | honing-stone | 6× | 6 | · | part |
| 4.3 | Stone Shoe | honing-stone-shoe | 6× | 6 | · | part |
| 4.4 | Guide Shoe | honing-guide-shoe | 2× | 2 | · | part |
| 4.5 | Coil Spring | coil-spring | 2× | 2 | · | part |
| 5 | Worktable & Fixture 4 parts | honing-worktable | 1× | 1 | 6 | assembly |
| 5.1 | Worktable | honing-table | 1× | 1 | · | part |
| 5.2 | Floating Fixture | honing-float-fixture | 1× | 1 | · | part |
| 5.3 | Locator | honing-locator | 2× | 2 | · | part |
| 5.4 | Light Clamp | honing-clamp | 2× | 2 | · | part |
| 6 | Coolant System 5 parts | honing-coolant-system | 1× | 1 | 33 | assembly |
| 6.1 | Coolant Pump 5 parts | honing-coolant-pump | 1× | 1 | 26 | assembly |
| 6.1.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 6.1.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 6.1.3 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 6.1.4 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 6.1.5 | Oil Seal | oil-seal | 1× | 1 | · | part |
| 6.2 | Oil Tank | honing-coolant-tank | 1× | 1 | · | part |
| 6.3 | Fine Filter | honing-coolant-filter | 1× | 1 | · | part |
| 6.4 | Flush Nozzle | honing-coolant-nozzle | 2× | 2 | · | part |
| 6.5 | Coolant Hose | honing-coolant-hose | 3× | 3 | · | part |
| 7 | In-Process Gauging 3 parts | honing-gauging | 1× | 1 | 54 | assembly |
| 7.1 | Air Plug Gauge | honing-air-gauge | 1× | 1 | · | part |
| 7.2 | Gauge Amplifier 3 parts | honing-gauge-amplifier | 1× | 1 | 52 | assembly |
| 7.2.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 7.2.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 7.2.3 | SMD Passive (R/C/L) | smd-passives | 50× | 50 | · | part |
| 7.3 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 8 | Control 4 parts | honing-control | 1× | 1 | 204 | assembly |
| 8.1 | CNC Controller 4 parts | honing-controller | 1× | 1 | 148 | assembly |
| 8.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.1.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 8.1.3 | Relay | relay | 6× | 6 | · | part |
| 8.1.4 | SMD Passive (R/C/L) | smd-passives | 140× | 140 | · | part |
| 8.2 | Operator Display 4 parts | honing-display | 1× | 1 | 43 | assembly |
| 8.2.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.2.2 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 8.2.3 | Touch Digitizer | touch-digitizer | 1× | 1 | · | part |
| 8.2.4 | SMD Passive (R/C/L) | smd-passives | 40× | 40 | · | part |
| 8.3 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 8.4 | Connector | connector | 12× | 12 | · | part |
| 9 | Enclosure & Guards 5 parts | honing-enclosure | 1× | 1 | 11 | assembly |
| 9.1 | Sheet Metal Panel | sheet-panel | 6× | 6 | · | part |
| 9.2 | Access Door | honing-access-door | 1× | 1 | · | part |
| 9.3 | Interlock Switch | honing-interlock-switch | 2× | 2 | · | part |
| 9.4 | Emergency Stop | honing-estop | 1× | 1 | · | part |
| 9.5 | Mist Extractor | honing-mist-extractor | 1× | 1 | · | part |
| 10 | Fastener Set | fastener-set | 3× | 3 | · | part |
Related products
same domain, ranked by shared parts Honing Machine
325 parts · shares 24 with this page
 CNC Milling Machine
400 parts · shares 5 with this page
 CNC Lathe
511 parts · shares 4 with this page
CNC Metal Spinning Machine
768 parts · shares 6 with this page
Electrochemical Grinder
425 parts · shares 6 with this page
Vertical Broaching Machine
220 parts · shares 3 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
848-word article