Waterjet Cutter
ProductAlso known as: Waterjet Cutting Machine
Overview
An abrasive waterjet cutting machine cuts material by firing a thin stream of water mixed with hard abrasive grit at the workpiece. Water is pressurised to about 4150 bar, forced through a tiny jewel orifice to make a fast coherent jet, and that jet pulls garnet grit into itself before leaving a focusing tube. The result is a stream moving near three times the speed of sound that erodes a narrow slot through almost any material. The cut is cold, so there is no heat-affected zone, no melting, and no hardening at the edge, which sets it apart from plasma, laser, and abrasive saws. It cuts steel, titanium, stone, glass, composites, rubber, and stacked sheets with the same head, and it leaves a clean matte edge that often needs no second operation.
The machine has nine main parts. The Intensifier Pump makes the pressure, the High-Pressure Plumbing carries it to the moving Cutting Head, and the Abrasive Delivery feeds garnet to that head. The Gantry Motion moves the head over the Catcher Tank and Table, which stops the spent jet, while the Water Treatment conditions the feed water and the CNC Controller runs the toolpath. The Enclosure and Safety contains spray and stops the machine in an emergency.
The high-pressure pump
Almost everything depends on the Intensifier Pump, because the jet has no cutting power without pressure. The common design is the intensifier. A Drive Motor of 30 to 75 kW, built from a Stator Assembly and Rotor Assembly on Ball Bearing supports, drives a Hydraulic Power Unit. That unit uses a Hydraulic Pump to send oil at around 200 bar from a Oil Reservoir through a Directional Valve, with a Oil Cooler and Hydraulic Filter keeping the oil cool and clean.
The oil drives the Intensifier. Here a large Hydraulic Piston pushes a much smaller Plunger inside a High-Pressure Cylinder. Because the piston area is roughly twenty times the plunger area, the water leaves at twenty times the oil pressure, which is how 200 bar of oil becomes 4150 bar of water. The Check Valve set admits low-pressure water on the back stroke and seals it on the forward stroke, and High-Pressure Seal rings hold the pressure around the plunger. The intensifier is double-acting, so it reverses at the end of each stroke, which makes the pressure dip briefly. A Attenuator stores compressed water and releases it during the reversal so the jet stays steady. A Inlet Filter protects the check valves from grit.
The cutting head
The Cutting Head turns pressure into a usable cut. A pneumatic On/Off Valve starts and stops the jet in a few milliseconds. Just below it sits the Jewel Orifice, a sapphire, ruby, or diamond disc with a hole of 0.25 to 0.40 mm. Forcing water through that hole converts the stored pressure into velocity, giving a coherent jet faster than 800 m/s. Plain water alone will cut soft material, but the cutting power comes from grit. The fast jet enters the Mixing Chamber, where its speed creates suction that pulls garnet in through the Abrasive Inlet. Water and grit then pass through the Focusing Tube, a carbide tube with a bore near 0.76 mm that aligns everything into one stream. The Head Body holds these parts in tight alignment, because a small misalignment between orifice and focusing tube wrecks the cut. The orifice and focusing tube are wear items: garnet slowly erodes the tube bore and a chipped orifice splits the jet, so both are replaced regularly.
Abrasive delivery
The Abrasive Delivery must deliver a steady garnet flow, since a surge or a gap changes the cut depth. Bulk Garnet Abrasive, usually 80 mesh, sits in a Abrasive Hopper and is fed to a Metering Mini-Hopper mounted on the gantry near the head. A Metering Valve sets the flow, typically 200 to 600 g/min, and the Abrasive Feed Line carries dry grit to the abrasive inlet. Too little garnet leaves an unfinished cut, and too much chokes the stream, so the rate is matched to material and thickness in the program.
Motion and catcher tank
The Gantry Motion moves the head over the work. A Bridge spans the table on X Axis rails, a Y Axis carriage rides across it, and a Z Axis sets the standoff at about 1 mm. Each axis uses a Servo Motor driving a Ball Screw on Linear Guide Rail rails, and a Energy Chain carries the high-pressure tube and abrasive line as the bridge travels. Many machines add a Taper-Compensation Wrist, a tilting wrist driven by two Servo Motor units through Helical Gear Pair reductions, that angles the head a few degrees to cancel the natural taper of the kerf so the walls come out square.
After the jet cuts through, it still carries energy and must be stopped. The Catcher Tank and Table does this with a steel Catcher Tank holding 150 to 300 mm of water that absorbs the jet. The part rests on Support Slat supports set on edge in a Slat Frame, which back the work with minimal contact. A Drain and Overflow keeps the level constant and a Sludge Removal system clears spent garnet from the floor.
Controls and water supply
The CNC Controller runs the cut. A Controller Board built around an Microcontroller commands the Servo Drive units, an I/O Module with a Pressure Sensor switches the jet and abrasive, and an LCD Panel gives the operator the toolpath, pressure, and abrasive settings. Feed water passes a Water Treatment stage first: a Booster Pump keeps the intensifier supplied, a Water Filter removes fine particles, and a Water Softener lowers hardness so scale does not foul the orifice and seals.
Use and limits
Abrasive waterjet machines suit shops that cut a wide mix of materials and thicknesses without changing tools. They cut metal up to 150 mm and more, stone, glass, ceramic, and laminates, holding about plus or minus 0.05 mm, all with a cold edge that needs no deburring on many jobs. The limits are running cost and speed: garnet, orifices, focusing tubes, and high-pressure seals are consumables, and the cut is slower than laser-cutting-machine on thin steel. For high volume in one thin material a laser or plasma is cheaper per part, but for thick, hard, heat-sensitive, or mixed work the waterjet covers ground no thermal process can reach.
Waterjet Cutter parts and their functions
9 top-level parts · 303 parts in total · full bill of materials below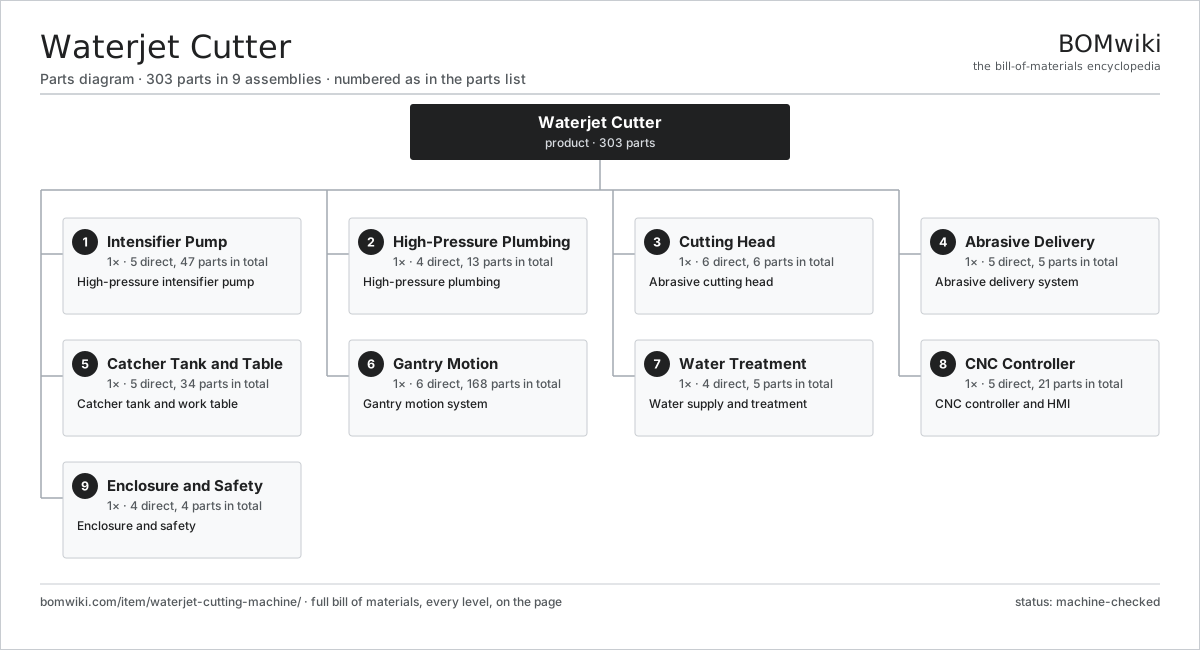
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Intensifier Pump 5 parts | 1× | High-pressure intensifier pump |
| 2 | High-Pressure Plumbing 4 parts | 1× | High-pressure plumbing |
| 3 | Cutting Head 6 parts | 1× | Abrasive cutting head |
| 4 | Abrasive Delivery 5 parts | 1× | Abrasive delivery system |
| 5 | Catcher Tank and Table 5 parts | 1× | Catcher tank and work table |
| 6 | Gantry Motion 6 parts | 1× | Gantry motion system |
| 7 | Water Treatment 4 parts | 1× | Water supply and treatment |
| 8 | CNC Controller 5 parts | 1× | CNC controller and HMI |
| 9 | Enclosure and Safety 4 parts | 1× | Enclosure and safety |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Waterjet Cutter
9 top-level lines · 89 rows shown · 303 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Intensifier Pump 5 parts | waterjet-cutting-machine-pump | 1× | 1 | 47 | assembly |
| 1.1 | Drive Motor 4 parts | waterjet-cutting-machine-drive-motor | 1× | 1 | 25 | assembly |
| 1.1.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 1.1.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 1.1.3 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 1.1.4 | Motor Cooling Fan | waterjet-cutting-machine-motor-fan | 1× | 1 | · | part |
| 1.2 | Hydraulic Power Unit 6 parts | waterjet-cutting-machine-hpu | 1× | 1 | 7 | assembly |
| 1.2.1 | Hydraulic Pump | waterjet-cutting-machine-hyd-pump | 1× | 1 | · | part |
| 1.2.2 | Oil Reservoir | waterjet-cutting-machine-reservoir | 1× | 1 | · | part |
| 1.2.3 | Directional Valve | waterjet-cutting-machine-directional-valve | 1× | 1 | · | part |
| 1.2.4 | Oil Cooler | waterjet-cutting-machine-oil-cooler | 1× | 1 | · | part |
| 1.2.5 | Hydraulic Filter | waterjet-cutting-machine-hyd-filter | 1× | 1 | · | part |
| 1.2.6 | Oil Seal | oil-seal | 2× | 2 | · | part |
| 1.3 | Intensifier 5 parts | waterjet-cutting-machine-intensifier | 1× | 1 | 13 | assembly |
| 1.3.1 | Hydraulic Piston | waterjet-cutting-machine-hyd-piston | 1× | 1 | · | part |
| 1.3.2 | Plunger | waterjet-cutting-machine-plunger | 2× | 2 | · | part |
| 1.3.3 | High-Pressure Cylinder | waterjet-cutting-machine-hp-cylinder | 2× | 2 | · | part |
| 1.3.4 | Check Valve | waterjet-cutting-machine-check-valve | 4× | 4 | · | part |
| 1.3.5 | High-Pressure Seal | waterjet-cutting-machine-hp-seal | 4× | 4 | · | part |
| 1.4 | Attenuator | waterjet-cutting-machine-attenuator | 1× | 1 | · | part |
| 1.5 | Inlet Filter | waterjet-cutting-machine-inlet-filter | 1× | 1 | · | part |
| 2 | High-Pressure Plumbing 4 parts | waterjet-cutting-machine-hp-plumbing | 1× | 1 | 13 | assembly |
| 2.1 | High-Pressure Tubing | waterjet-cutting-machine-hp-tubing | 1× | 1 | · | part |
| 2.2 | Swivel Joint | waterjet-cutting-machine-swivel-joint | 3× | 3 | · | part |
| 2.3 | High-Pressure Fitting | waterjet-cutting-machine-hp-fitting | 8× | 8 | · | part |
| 2.4 | Bleed-Down Valve | waterjet-cutting-machine-bleed-valve | 1× | 1 | · | part |
| 3 | Cutting Head 6 parts | waterjet-cutting-machine-cutting-head | 1× | 1 | 6 | assembly |
| 3.1 | On/Off Valve | waterjet-cutting-machine-onoff-valve | 1× | 1 | · | part |
| 3.2 | Jewel Orifice | waterjet-cutting-machine-orifice | 1× | 1 | · | part |
| 3.3 | Mixing Chamber | waterjet-cutting-machine-mixing-chamber | 1× | 1 | · | part |
| 3.4 | Focusing Tube | waterjet-cutting-machine-focusing-tube | 1× | 1 | · | part |
| 3.5 | Abrasive Inlet | waterjet-cutting-machine-abrasive-inlet | 1× | 1 | · | part |
| 3.6 | Head Body | waterjet-cutting-machine-head-body | 1× | 1 | · | part |
| 4 | Abrasive Delivery 5 parts | waterjet-cutting-machine-abrasive-system | 1× | 1 | 5 | assembly |
| 4.1 | Abrasive Hopper | waterjet-cutting-machine-hopper | 1× | 1 | · | part |
| 4.2 | Metering Mini-Hopper | waterjet-cutting-machine-mini-hopper | 1× | 1 | · | part |
| 4.3 | Metering Valve | waterjet-cutting-machine-metering-valve | 1× | 1 | · | part |
| 4.4 | Abrasive Feed Line | waterjet-cutting-machine-feed-line | 1× | 1 | · | part |
| 4.5 | Garnet Abrasive | waterjet-cutting-machine-garnet | 1× | 1 | · | part |
| 5 | Catcher Tank and Table 5 parts | waterjet-cutting-machine-tank-table | 1× | 1 | 34 | assembly |
| 5.1 | Catcher Tank | waterjet-cutting-machine-tank | 1× | 1 | · | part |
| 5.2 | Support Slat | waterjet-cutting-machine-slat | 30× | 30 | · | part |
| 5.3 | Slat Frame | waterjet-cutting-machine-slat-frame | 1× | 1 | · | part |
| 5.4 | Drain and Overflow | waterjet-cutting-machine-drain | 1× | 1 | · | part |
| 5.5 | Sludge Removal | waterjet-cutting-machine-sludge-removal | 1× | 1 | · | part |
| 6 | Gantry Motion 6 parts | waterjet-cutting-machine-gantry | 1× | 1 | 168 | assembly |
| 6.1 | Bridge 2 parts | waterjet-cutting-machine-bridge | 1× | 1 | 3 | assembly |
| 6.1.1 | Sheet Metal Panel | sheet-panel | 2× | 2 | · | part |
| 6.1.2 | Energy Chain | waterjet-cutting-machine-cable-track | 1× | 1 | · | part |
| 6.2 | X Axis 3 parts | waterjet-cutting-machine-x-axis | 1× | 1 | 52 | assembly |
| 6.2.1 | Servo Motor 4 parts + deeper › | servo-motor | 2× | 2 | 24 | assembly |
| 6.2.2 | Ball Screw | ball-screw | 2× | 2 | · | part |
| 6.2.3 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 6.3 | Y Axis 3 parts | waterjet-cutting-machine-y-axis | 1× | 1 | 27 | assembly |
| 6.3.1 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 6.3.2 | Ball Screw | ball-screw | 1× | 1 | · | part |
| 6.3.3 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 6.4 | Z Axis 3 parts | waterjet-cutting-machine-z-axis | 1× | 1 | 26 | assembly |
| 6.4.1 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 6.4.2 | Ball Screw | ball-screw | 1× | 1 | · | part |
| 6.4.3 | Standoff Sensor | waterjet-cutting-machine-standoff-sensor | 1× | 1 | · | part |
| 6.5 | Taper-Compensation Wrist 3 parts | waterjet-cutting-machine-taper-head | 1× | 1 | 54 | assembly |
| 6.5.1 | Servo Motor 4 parts + deeper › | servo-motor | 2× | 2 | 24 | assembly |
| 6.5.2 | Helical Gear Pair | gear-pair | 2× | 2 | · | part |
| 6.5.3 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 6.6 | Linear Guide Rail | linear-guide | 6× | 6 | · | part |
| 7 | Water Treatment 4 parts | waterjet-cutting-machine-water-treatment | 1× | 1 | 5 | assembly |
| 7.1 | Booster Pump | waterjet-cutting-machine-booster-pump | 1× | 1 | · | part |
| 7.2 | Water Filter | waterjet-cutting-machine-water-filter | 2× | 2 | · | part |
| 7.3 | Water Softener | waterjet-cutting-machine-softener | 1× | 1 | · | part |
| 7.4 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 8 | CNC Controller 5 parts | waterjet-cutting-machine-controller | 1× | 1 | 21 | assembly |
| 8.1 | Controller Board 4 parts | waterjet-cutting-machine-controller-pcb | 1× | 1 | 9 | assembly |
| 8.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.1.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 8.1.3 | SMD Passive (R/C/L) | smd-passives | 1× | 1 | · | part |
| 8.1.4 | Connector | connector | 6× | 6 | · | part |
| 8.2 | Servo Drive | waterjet-cutting-machine-servo-drive | 4× | 4 | · | part |
| 8.3 | I/O Module 3 parts | waterjet-cutting-machine-io-module | 1× | 1 | 6 | assembly |
| 8.3.1 | Relay | relay | 4× | 4 | · | part |
| 8.3.2 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 8.3.3 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 8.4 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 8.5 | Power Supply | power-supply | 1× | 1 | · | part |
| 9 | Enclosure and Safety 4 parts | waterjet-cutting-machine-enclosure | 1× | 1 | 4 | assembly |
| 9.1 | Splash Guard | waterjet-cutting-machine-splash-guard | 1× | 1 | · | part |
| 9.2 | Emergency Stop | waterjet-cutting-machine-estop | 1× | 1 | · | part |
| 9.3 | Light Curtain | waterjet-cutting-machine-light-curtain | 1× | 1 | · | part |
| 9.4 | Fastener Set | fastener-set | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Crankshaft Grinder
511 parts · shares 7 with this page
 Creep-Feed Grinder
571 parts · shares 7 with this page
Cut-to-Length Line
500 parts · shares 7 with this page
Drag Finishing Machine
735 parts · shares 7 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
1,227-word article