Seamless Pipe Piercing Mill
ProductOverview
A seamless pipe piercing mill turns a solid hot steel billet into a thick-walled hollow shell without any welded seam. It is the first hot-forming step in the seamless tube route: a round billet is heated to about 1200 to 1280 degrees, charged into the mill, and forced between two driven rolls that grip it, spin it, and drive it onto a fixed piercing point that opens a bore down the center. The shell that leaves the mill is later rolled and sized in separate stands to reach the final pipe wall and diameter, but the bore itself is made here. Because the hole is formed by deformation rather than drilling, the mill works the metal hot and fast, and one bite produces the full length of the shell.
The machine is built around the Piercing Roll Set, fed by the Entry Table and Billet Charging and worked against the Plug and Mandrel Bar. The Guide Shoes and Diescher Discs closes the sides of the pass, the Main Drive Train turns the rolls, the Hydraulic Adjustment System sets their position, and the Water Cooling System keeps the tooling from softening. All of it is framed by the Mill Housing and Stand and sequenced from the Electrical and Control Room.
The Mannesmann effect
The mill exploits a behavior of metal under cross-roll loading that the Mannesmann brothers found in the 1880s. The two work rolls are not parallel: each is tilted to a feed angle and set at a cross angle so that, as they turn, they both rotate the billet and screw it forward along the mill axis. The rolls bite the surface hard, but the surface and the core do not see the same stress. Near the center the material is pulled in alternating tension as the billet rotates under the squeeze, and after a few turns this cyclic tensile stress tears open a small cavity along the axis. That cavity is the start of the bore. The Piercing Plug is held on the axis just behind the point where the cavity forms, so the metal opens onto the plug and is shaped into a round, smooth bore rather than a ragged crack. The art of piercing is timing the roll geometry so the cavity opens exactly at the plug nose and not before, since a cavity that runs ahead of the plug leaves a rough inner surface.
How the mill works
A heated billet rolls down the Driven Roller Table to the Billet Stop, where the Centering Guides line it up with the roll gap. The Charging Pusher then drives the billet into the bite. The two Barrel Work Rolls, each a barrel with an entry cone, a central gorge, and an exit cone, grip the billet and spin it while feeding it onto the Piercing Plug. The plug sits on the Mandrel Bar, which is held back by the Thrust Block against the heavy axial force of piercing. The Guide Shoes or driven Diescher Discs back the shell on the two sides the rolls do not touch, keeping it round. The shell screws over the plug and off the back of the bar in one pass.
Major subsystems
The Piercing Roll Set carries the rolls in Roll Chocks on tapered Roll-Neck Bearings, with a Roll Tilt Drive to set the feed angle and a Roll Skew Drive to set the cross angle. The Main Drive Train runs from a large Main Drive Motor through a Pinion Gearbox that splits torque to both rolls, then through Drive Couplings and Universal Spindles that reach the roll necks across the tilt and skew range. The Hydraulic Adjustment System uses a Hydraulic Power Pack, a Valve Block of Servo Valves, and Adjustment Cylinders to set the roll gap and hold it under load. Water from the Water Cooling System floods the rolls through Spray Nozzles and runs through the bar to cool the plug. The Electrical and Control Room runs the Mill PLC and the Drive Cabinet that hold every set point.
Materials
The tooling lives in a brutal place: it is squeezing steel near its forging temperature while abrading against scale. The Barrel Work Rolls are forged hot-work steel ground to the cone profile, washed continuously to limit thermal fatigue. The Piercing Plug is a chromium-nickel-molybdenum cast steel run with a controlled oxide layer that acts as a thermal barrier, and it is cooled between billets through the Mandrel Bar because its nose can reach the billet temperature. The Housing Posts and Tie Rods are sized for the large separating force, since piercing pushes the rolls apart with great load. The Universal Spindles and Pinion Shafts are case-hardened alloy steel to carry the drive torque through the universal joints.
Use
Piercing mills sit at the head of seamless tube plants that supply line pipe, casing and tubing for wells, boiler and pressure tube, and mechanical and bearing tube. The shell from this mill goes on to a plug mill, a mandrel mill, or a pilger mill to reach the wall, then to a stretch-reducing or sizing mill for the final diameter. The seamless route is chosen where a welded seam is a liability: high pressure, fatigue loading, or sour service. A Piercing Plug and roll pass are changed to suit each billet size and grade, so the mill is set up by recipe for each campaign.
Seamless Pipe Piercing Mill parts and their functions
9 top-level parts · 301 parts in total · full bill of materials below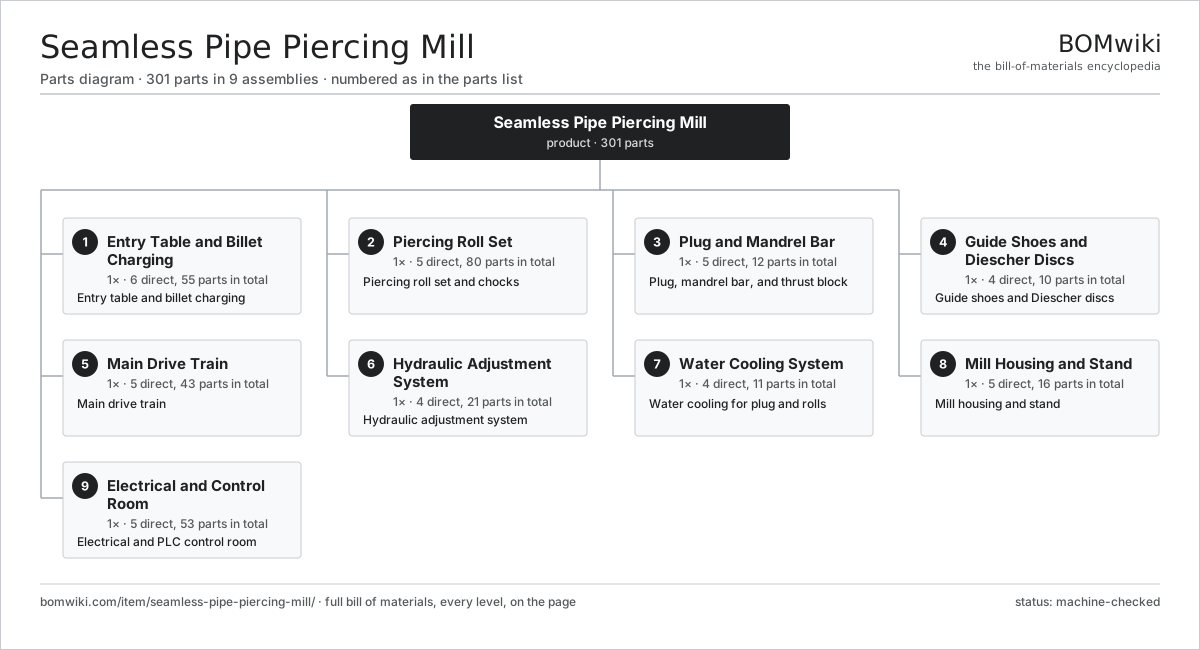
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Entry Table and Billet Charging 6 parts | 1× | Entry table and billet charging |
| 2 | Piercing Roll Set 5 parts | 1× | Piercing roll set and chocks |
| 3 | Plug and Mandrel Bar 5 parts | 1× | Plug, mandrel bar, and thrust block |
| 4 | Guide Shoes and Diescher Discs 4 parts | 1× | Guide shoes and Diescher discs |
| 5 | Main Drive Train 5 parts | 1× | Main drive train |
| 6 | Hydraulic Adjustment System 4 parts | 1× | Hydraulic adjustment system |
| 7 | Water Cooling System 4 parts | 1× | Water cooling for plug and rolls |
| 8 | Mill Housing and Stand 5 parts | 1× | Mill housing and stand |
| 9 | Electrical and Control Room 5 parts | 1× | Electrical and PLC control room |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Seamless Pipe Piercing Mill
9 top-level lines · 105 rows shown · 301 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Entry Table and Billet Charging 6 parts | seamless-pipe-piercing-mill-entry-table | 1× | 1 | 55 | assembly |
| 1.1 | Driven Roller Table 5 parts | seamless-pipe-piercing-mill-roller-table | 1× | 1 | 31 | assembly |
| 1.1.1 | Table Frame | seamless-pipe-piercing-mill-table-frame | 1× | 1 | · | part |
| 1.1.2 | Table Roller | seamless-pipe-piercing-mill-table-roller | 8× | 8 | · | part |
| 1.1.3 | Table Drive Motor | seamless-pipe-piercing-mill-table-motor | 2× | 2 | · | part |
| 1.1.4 | Helical Gear Pair | gear-pair | 4× | 4 | · | part |
| 1.1.5 | Ball Bearing | ball-bearing | 16× | 16 | · | part |
| 1.2 | Table Roller | seamless-pipe-piercing-mill-table-roller | 14× | 14 | · | part |
| 1.3 | Billet Stop | seamless-pipe-piercing-mill-billet-stop | 1× | 1 | · | part |
| 1.4 | Centering Guide | seamless-pipe-piercing-mill-centering-guide | 2× | 2 | · | part |
| 1.5 | Charging Pusher 3 parts | seamless-pipe-piercing-mill-charging-pusher | 1× | 1 | 3 | assembly |
| 1.5.1 | Pusher Cylinder | seamless-pipe-piercing-mill-pusher-cylinder | 1× | 1 | · | part |
| 1.5.2 | Pusher Head | seamless-pipe-piercing-mill-pusher-head | 1× | 1 | · | part |
| 1.5.3 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 1.6 | Fastener Set | fastener-set | 4× | 4 | · | part |
| 2 | Piercing Roll Set 5 parts | seamless-pipe-piercing-mill-roll-set | 1× | 1 | 80 | assembly |
| 2.1 | Barrel Work Roll | seamless-pipe-piercing-mill-work-roll | 2× | 2 | · | part |
| 2.2 | Roll Chock 3 parts | seamless-pipe-piercing-mill-roll-chock | 4× | 4 | 4 | assembly |
| 2.2.1 | Chock Body | seamless-pipe-piercing-mill-chock-body | 1× | 4 | · | part |
| 2.2.2 | Roll-Neck Bearing | seamless-pipe-piercing-mill-roll-bearing | 1× | 4 | · | part |
| 2.2.3 | Oil Seal | oil-seal | 2× | 8 | · | part |
| 2.3 | Roll Tilt Drive 3 parts | seamless-pipe-piercing-mill-roll-tilt | 2× | 2 | 26 | assembly |
| 2.3.1 | Tilt Screw | seamless-pipe-piercing-mill-tilt-screw | 1× | 2 | · | part |
| 2.3.2 | Tilt Worm Gear | seamless-pipe-piercing-mill-tilt-worm | 1× | 2 | · | part |
| 2.3.3 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 2 | 24 | assembly |
| 2.4 | Roll Skew Drive 3 parts | seamless-pipe-piercing-mill-roll-skew | 2× | 2 | 3 | assembly |
| 2.4.1 | Skew Cylinder | seamless-pipe-piercing-mill-skew-cylinder | 1× | 2 | · | part |
| 2.4.2 | Skew Bracket | seamless-pipe-piercing-mill-skew-bracket | 1× | 2 | · | part |
| 2.4.3 | Pressure Sensor | pressure-sensor | 1× | 2 | · | part |
| 2.5 | Roll-Neck Bearing | seamless-pipe-piercing-mill-roll-bearing | 4× | 4 | · | part |
| 3 | Plug and Mandrel Bar 5 parts | seamless-pipe-piercing-mill-mandrel-assembly | 1× | 1 | 12 | assembly |
| 3.1 | Piercing Plug | seamless-pipe-piercing-mill-piercing-plug | 1× | 1 | · | part |
| 3.2 | Mandrel Bar | seamless-pipe-piercing-mill-mandrel-bar | 1× | 1 | · | part |
| 3.3 | Thrust Block 3 parts | seamless-pipe-piercing-mill-thrust-block | 1× | 1 | 4 | assembly |
| 3.3.1 | Thrust Housing | seamless-pipe-piercing-mill-thrust-housing | 1× | 1 | · | part |
| 3.3.2 | Thrust Bearing | seamless-pipe-piercing-mill-thrust-bearing | 1× | 1 | · | part |
| 3.3.3 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 3.4 | Bar-Retaining Gear 3 parts | seamless-pipe-piercing-mill-bar-retainer | 1× | 1 | 5 | assembly |
| 3.4.1 | Helical Gear Pair | gear-pair | 1× | 1 | · | part |
| 3.4.2 | Bar Clamp | seamless-pipe-piercing-mill-retainer-clamp | 2× | 2 | · | part |
| 3.4.3 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 3.5 | Bar Cooling Line | seamless-pipe-piercing-mill-bar-cooling-line | 1× | 1 | · | part |
| 4 | Guide Shoes and Diescher Discs 4 parts | seamless-pipe-piercing-mill-guide-set | 1× | 1 | 10 | assembly |
| 4.1 | Guide Shoe | seamless-pipe-piercing-mill-guide-shoe | 2× | 2 | · | part |
| 4.2 | Diescher Disc | seamless-pipe-piercing-mill-diescher-disc | 2× | 2 | · | part |
| 4.3 | Disc Drive Motor | seamless-pipe-piercing-mill-disc-motor | 2× | 2 | · | part |
| 4.4 | Disc Bearing | seamless-pipe-piercing-mill-disc-bearing | 4× | 4 | · | part |
| 5 | Main Drive Train 5 parts | seamless-pipe-piercing-mill-main-drive | 1× | 1 | 43 | assembly |
| 5.1 | Main Drive Motor 4 parts | seamless-pipe-piercing-mill-main-motor | 1× | 1 | 25 | assembly |
| 5.1.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 5.1.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 5.1.3 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 5.1.4 | Motor Terminal Box | seamless-pipe-piercing-mill-motor-terminal-box | 1× | 1 | · | part |
| 5.2 | Pinion Gearbox 5 parts | seamless-pipe-piercing-mill-pinion-gearbox | 1× | 1 | 13 | assembly |
| 5.2.1 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 5.2.2 | Helical Gear Pair | gear-pair | 2× | 2 | · | part |
| 5.2.3 | Pinion Shaft | seamless-pipe-piercing-mill-pinion-shaft | 2× | 2 | · | part |
| 5.2.4 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 5.2.5 | Oil Seal | oil-seal | 4× | 4 | · | part |
| 5.3 | Drive Coupling | seamless-pipe-piercing-mill-coupling | 2× | 2 | · | part |
| 5.4 | Universal Spindle | seamless-pipe-piercing-mill-spindle | 2× | 2 | · | part |
| 5.5 | Flywheel | seamless-pipe-piercing-mill-flywheel | 1× | 1 | · | part |
| 6 | Hydraulic Adjustment System 4 parts | seamless-pipe-piercing-mill-hydraulic-system | 1× | 1 | 21 | assembly |
| 6.1 | Hydraulic Power Pack 5 parts | seamless-pipe-piercing-mill-power-pack | 1× | 1 | 6 | assembly |
| 6.1.1 | Hydraulic Pump | seamless-pipe-piercing-mill-hyd-pump | 1× | 1 | · | part |
| 6.1.2 | Pump Motor | seamless-pipe-piercing-mill-hyd-motor | 1× | 1 | · | part |
| 6.1.3 | Oil Tank | seamless-pipe-piercing-mill-hyd-tank | 1× | 1 | · | part |
| 6.1.4 | Oil Filter | seamless-pipe-piercing-mill-hyd-filter | 2× | 2 | · | part |
| 6.1.5 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 6.2 | Adjustment Cylinder | seamless-pipe-piercing-mill-adjust-cylinder | 4× | 4 | · | part |
| 6.3 | Valve Block 3 parts | seamless-pipe-piercing-mill-valve-block | 1× | 1 | 9 | assembly |
| 6.3.1 | Servo Valve | seamless-pipe-piercing-mill-servo-valve | 4× | 4 | · | part |
| 6.3.2 | Manifold Body | seamless-pipe-piercing-mill-manifold | 1× | 1 | · | part |
| 6.3.3 | Pressure Sensor | pressure-sensor | 4× | 4 | · | part |
| 6.4 | Accumulator | seamless-pipe-piercing-mill-accumulator | 2× | 2 | · | part |
| 7 | Water Cooling System 4 parts | seamless-pipe-piercing-mill-cooling-system | 1× | 1 | 11 | assembly |
| 7.1 | Cooling Water Pump | seamless-pipe-piercing-mill-water-pump | 1× | 1 | · | part |
| 7.2 | Water Manifold | seamless-pipe-piercing-mill-water-manifold | 1× | 1 | · | part |
| 7.3 | Spray Nozzle | seamless-pipe-piercing-mill-spray-nozzle | 8× | 8 | · | part |
| 7.4 | Plug Cooling Header | seamless-pipe-piercing-mill-plug-cooler | 1× | 1 | · | part |
| 8 | Mill Housing and Stand 5 parts | seamless-pipe-piercing-mill-housing | 1× | 1 | 16 | assembly |
| 8.1 | Housing Post | seamless-pipe-piercing-mill-housing-post | 2× | 2 | · | part |
| 8.2 | Housing Cap | seamless-pipe-piercing-mill-cap | 1× | 1 | · | part |
| 8.3 | Tie Rod | seamless-pipe-piercing-mill-tie-rod | 4× | 4 | · | part |
| 8.4 | Foundation Base Plate | seamless-pipe-piercing-mill-base-plate | 1× | 1 | · | part |
| 8.5 | Fastener Set | fastener-set | 8× | 8 | · | part |
| 9 | Electrical and Control Room 5 parts | seamless-pipe-piercing-mill-control-room | 1× | 1 | 53 | assembly |
| 9.1 | Mill PLC 5 parts | seamless-pipe-piercing-mill-plc | 1× | 1 | 24 | assembly |
| 9.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 9.1.2 | Microcontroller | mcu | 2× | 2 | · | part |
| 9.1.3 | SMD Passive (R/C/L) | smd-passives | 1× | 1 | · | part |
| 9.1.4 | Relay | relay | 8× | 8 | · | part |
| 9.1.5 | Connector | connector | 12× | 12 | · | part |
| 9.2 | Drive Cabinet 4 parts | seamless-pipe-piercing-mill-drive-cabinet | 1× | 1 | 15 | assembly |
| 9.2.1 | Power Supply | power-supply | 2× | 2 | · | part |
| 9.2.2 | Variable-Speed Drive | seamless-pipe-piercing-mill-vsd | 3× | 3 | · | part |
| 9.2.3 | Motor Contactor | seamless-pipe-piercing-mill-contactor | 6× | 6 | · | part |
| 9.2.4 | Wire Bundle | wire-bundle | 4× | 4 | · | part |
| 9.3 | Operator Desk | seamless-pipe-piercing-mill-operator-desk | 1× | 1 | · | part |
| 9.4 | HMI Station 4 parts | seamless-pipe-piercing-mill-hmi | 1× | 1 | 7 | assembly |
| 9.4.1 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 9.4.2 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 9.4.3 | SMD Passive (R/C/L) | smd-passives | 1× | 1 | · | part |
| 9.4.4 | Connector | connector | 4× | 4 | · | part |
| 9.5 | Wire Bundle | wire-bundle | 6× | 6 | · | part |
Related products
same domain, ranked by shared parts Bed-Type Milling Machine
151 parts · shares 5 with this page
 Bevel Gear Generator
201 parts · shares 5 with this page
Centering and Facing Machine
1,419 parts · shares 5 with this page
 Creep-Feed Grinder
571 parts · shares 5 with this page
Cut-to-Length Line
500 parts · shares 5 with this page
Downpipe Rollforming Machine
414 parts · shares 5 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
1,079-word article