Vertical Broaching Machine
ProductOverview
A vertical broaching machine drives a toothed broach straight up or down through a part to cut an internal shape: a keyway, a spline, a square or hexagon hole, or a profiled bore. The broach is a long bar whose teeth rise in height tooth by tooth, so a single stroke takes the bore from its drilled starting size to the finished shape and size. Standing the stroke vertical keeps the machine compact on the floor, makes loading parts onto a horizontal table easy, and lets gravity help return the broach. The same machine cuts keyways in pulley and gear hubs, internal splines in clutch and gearbox parts, and shaped holes in stamped and forged blanks.
The frame is a Column & Base standing on a cast base. A Vertical Slide travels up and down the column carrying the Puller / Pusher Head head, and the Slide Drive moves it through the cut. The part sits on the Work Table, and the Broach Tooling is the tool that does the cutting. A Hydraulic Power Unit unit powers the motion and the clamps.
Pull-down and push-up action
Vertical machines work in two ways. In a pull-down machine the operator threads the broach front pilot up through the part from below, the Puller / Pusher Head grips the broach pull end at the top, and the slide pulls the broach down through the part. In a push-up machine a short, rigid broach is pushed straight up through the part by a ram; this suits shallow keyways but a long broach would buckle, so deep cuts use pulling. The Gripping Jaw pair in the puller clamps the pull end firmly, because the entire cutting force runs through that grip. After the stroke the Broach Elevator lifts the broach back to the top so the next part can be loaded.
Slide and drive
The Vertical Slide runs on hardened Vertical Way surfaces and Linear Guide Rail blocks, with the Adjustable Gib set to take out any play so the broach pulls truly vertical. The Slide Drive is a long hydraulic Main Cylinder fed through a Servo Valve that holds a steady cutting speed even as the engaged tooth count changes through the cut. The Linear Scale reads slide height so the control sets the stroke limits and the dwell at the end of the cut, then commands the fast return.
Workholding and tooling
The Work Table carries a Table Plate with a clearance hole for the broach, a Part Fixture that nests the part, and a Guide Bushing that steadies the broach front pilot as it enters. Hold-Down Clamp hold-downs pin the part against the pulling load. The Broach Bar carries the cutting teeth between a Front Pilot that centres it in the starting hole and a Rear Pilot that keeps it aligned as the last teeth finish the bore. Because the teeth set the final size, the broach is matched to the part and reground as a set.
Hydraulics and coolant
The Hydraulic Power Unit is the machine's power source. A variable-displacement Main Pump feeds the slide cylinder, the hold-down clamps and the puller jaws. A Accumulator smooths the pressure as the cutting load changes, and a Oil Cooler keeps the oil at a steady temperature so the cutting speed does not drift. A Pressure Sensor on the cylinder confirms grip and watches for overload. The Coolant System system floods the broach with cutting oil through a Flood Nozzle to wash chips out of the tooth gullets, which is the main thing that keeps a broach cutting cleanly stroke after stroke.
Control, safety and use
The Machine Control runs the cycle from a PLC: load and clamp, grip the broach, pull the stroke, dwell, return and reset. The operator sets stroke and speed at the HMI Panel. The Guarding encloses the moving slide and a Light Curtain stops the stroke if the load zone is breached. Vertical broaching machines are a staple of gear, automotive and fastener plants for internal keyways, splines and shaped holes. Surface broaches can also be fitted to cut external flats. Cutting speed is kept modest, typically a few metres a minute, because the teeth shear hard against the bore wall and run hot; the slow speed and flood oil are what give the bore its clean, straight finish. Setting up a job means matching the broach to the bore size, fitting the right bushing and front pilot, and dialling the stroke so the broach clears the part before the return. Variants include dual-ram machines that broach two parts on alternate strokes, tandem machines that share one hydraulic unit across two slides for higher output, and pull-up designs that pull the broach upward through the part for easier chip fall and faster loading.
Vertical Broaching Machine parts and their functions
11 top-level parts · 220 parts in total · full bill of materials below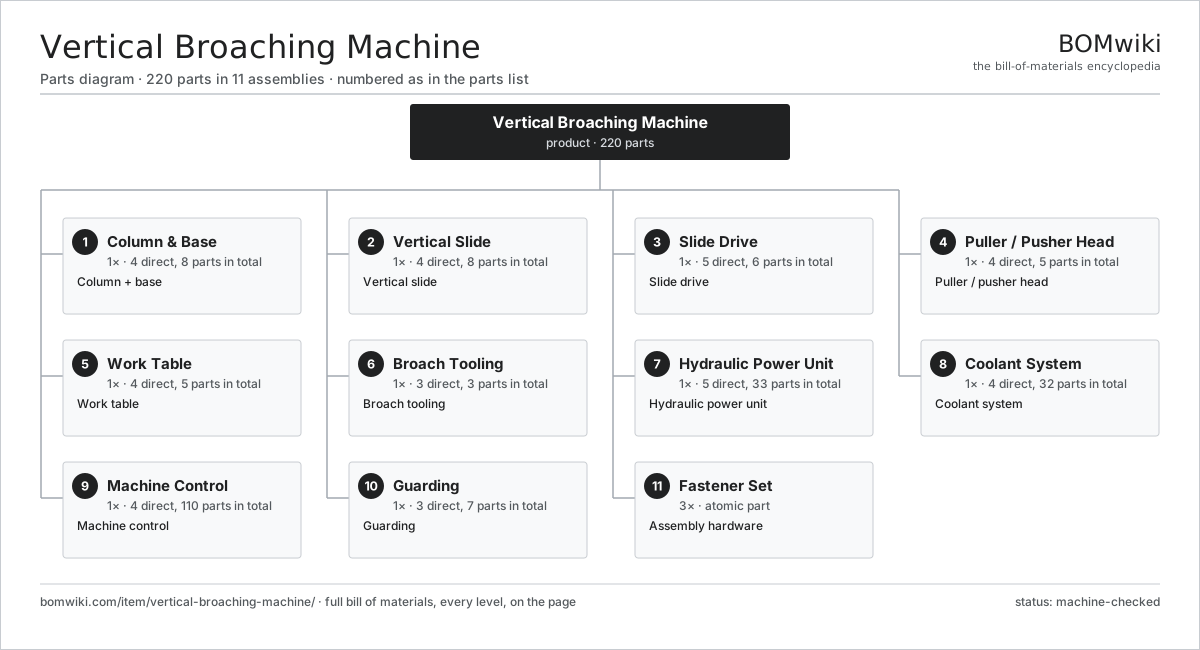
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Column & Base 4 parts | 1× | Column + base |
| 2 | Vertical Slide 4 parts | 1× | Vertical slide |
| 3 | Slide Drive 5 parts | 1× | Slide drive |
| 4 | Puller / Pusher Head 4 parts | 1× | Puller / pusher head |
| 5 | Work Table 4 parts | 1× | Work table |
| 6 | Broach Tooling 3 parts | 1× | Broach tooling |
| 7 | Hydraulic Power Unit 5 parts | 1× | Hydraulic power unit |
| 8 | Coolant System 4 parts | 1× | Coolant system |
| 9 | Machine Control 4 parts | 1× | Machine control |
| 10 | Guarding 3 parts | 1× | Guarding |
| 11 | Fastener Set | 3× | Assembly hardware |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Vertical Broaching Machine
11 top-level lines · 65 rows shown · 220 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Column & Base 4 parts | vertical-broaching-machine-column | 1× | 1 | 8 | assembly |
| 1.1 | Base Casting | vertical-broaching-machine-base-casting | 1× | 1 | · | part |
| 1.2 | Column Casting | vertical-broaching-machine-column-casting | 1× | 1 | · | part |
| 1.3 | Vertical Way | vertical-broaching-machine-way | 4× | 4 | · | part |
| 1.4 | Fastener Set | fastener-set | 2× | 2 | · | part |
| 2 | Vertical Slide 4 parts | vertical-broaching-machine-slide | 1× | 1 | 8 | assembly |
| 2.1 | Slide Body | vertical-broaching-machine-slide-body | 1× | 1 | · | part |
| 2.2 | Adjustable Gib | vertical-broaching-machine-gib | 4× | 4 | · | part |
| 2.3 | Linear Scale | vertical-broaching-machine-scale | 1× | 1 | · | part |
| 2.4 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 3 | Slide Drive 5 parts | vertical-broaching-machine-drive | 1× | 1 | 6 | assembly |
| 3.1 | Main Cylinder | vertical-broaching-machine-cylinder | 1× | 1 | · | part |
| 3.2 | Piston Rod | piston-rod | 1× | 1 | · | part |
| 3.3 | Servo Valve | vertical-broaching-machine-servo-valve | 1× | 1 | · | part |
| 3.4 | Pressure Sensor | pressure-sensor | 2× | 2 | · | part |
| 3.5 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 4 | Puller / Pusher Head 4 parts | vertical-broaching-machine-puller | 1× | 1 | 5 | assembly |
| 4.1 | Puller Body | vertical-broaching-machine-puller-body | 1× | 1 | · | part |
| 4.2 | Gripping Jaw | vertical-broaching-machine-jaw | 2× | 2 | · | part |
| 4.3 | Broach Elevator | vertical-broaching-machine-elevator | 1× | 1 | · | part |
| 4.4 | Pneumatic Cylinder | pneumatic-cylinder | 1× | 1 | · | part |
| 5 | Work Table 4 parts | vertical-broaching-machine-worktable | 1× | 1 | 5 | assembly |
| 5.1 | Table Plate | vertical-broaching-machine-table-plate | 1× | 1 | · | part |
| 5.2 | Part Fixture | vertical-broaching-machine-fixture | 1× | 1 | · | part |
| 5.3 | Hold-Down Clamp | vertical-broaching-machine-clamp | 2× | 2 | · | part |
| 5.4 | Guide Bushing | vertical-broaching-machine-bushing | 1× | 1 | · | part |
| 6 | Broach Tooling 3 parts | vertical-broaching-machine-broach | 1× | 1 | 3 | assembly |
| 6.1 | Broach Bar | vertical-broaching-machine-broach-bar | 1× | 1 | · | part |
| 6.2 | Front Pilot | vertical-broaching-machine-front-pilot | 1× | 1 | · | part |
| 6.3 | Rear Pilot | vertical-broaching-machine-rear-pilot | 1× | 1 | · | part |
| 7 | Hydraulic Power Unit 5 parts | vertical-broaching-machine-hydraulics | 1× | 1 | 33 | assembly |
| 7.1 | Main Pump 5 parts | vertical-broaching-machine-hyd-pump | 1× | 1 | 26 | assembly |
| 7.1.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 7.1.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 7.1.3 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 7.1.4 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 7.1.5 | Oil Seal | oil-seal | 1× | 1 | · | part |
| 7.2 | Oil Tank | vertical-broaching-machine-tank | 1× | 1 | · | part |
| 7.3 | Accumulator | vertical-broaching-machine-accumulator | 1× | 1 | · | part |
| 7.4 | Oil Cooler | vertical-broaching-machine-cooler | 1× | 1 | · | part |
| 7.5 | Relay | relay | 4× | 4 | · | part |
| 8 | Coolant System 4 parts | vertical-broaching-machine-coolant | 1× | 1 | 32 | assembly |
| 8.1 | Coolant Pump 5 parts | vertical-broaching-machine-coolant-pump | 1× | 1 | 26 | assembly |
| 8.1.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 8.1.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 8.1.3 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 8.1.4 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 8.1.5 | Oil Seal | oil-seal | 1× | 1 | · | part |
| 8.2 | Coolant Tank | coolant-tank | 1× | 1 | · | part |
| 8.3 | Flood Nozzle | vertical-broaching-machine-nozzle | 2× | 2 | · | part |
| 8.4 | Coolant Hose | coolant-hose | 3× | 3 | · | part |
| 9 | Machine Control 4 parts | vertical-broaching-machine-control | 1× | 1 | 110 | assembly |
| 9.1 | PLC 4 parts | vertical-broaching-machine-plc | 1× | 1 | 98 | assembly |
| 9.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 9.1.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 9.1.3 | Relay | relay | 6× | 6 | · | part |
| 9.1.4 | SMD Passive (R/C/L) | smd-passives | 90× | 90 | · | part |
| 9.2 | HMI Panel | hmi-panel | 1× | 1 | · | part |
| 9.3 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 9.4 | Connector | connector | 10× | 10 | · | part |
| 10 | Guarding 3 parts | vertical-broaching-machine-guard | 1× | 1 | 7 | assembly |
| 10.1 | Sheet Metal Panel | sheet-panel | 4× | 4 | · | part |
| 10.2 | Light Curtain | vertical-broaching-machine-light-curtain | 1× | 1 | · | part |
| 10.3 | Limit Switch | limit-switch | 2× | 2 | · | part |
| 11 | Fastener Set | fastener-set | 3× | 3 | · | part |
Related products
same domain, ranked by shared parts Surface Broaching Machine
219 parts · shares 8 with this page
Keyway Broaching Machine
179 parts · shares 5 with this page
 CNC Milling Machine
400 parts · shares 7 with this page
Gear Shaving Machine
240 parts · shares 5 with this page
 Vertical Boring Mill
265 parts · shares 5 with this page
 CNC Lathe
511 parts · shares 6 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
877-word article