Sendzimir Cluster Mill
ProductThe Sendzimir Cluster Mill is a cold rolling mill built to reduce hard, thin metal strip that ordinary four-high mills cannot handle. Its defining feature is a very small work roll, often 50 to 90 mm in diameter, supported by a cluster of progressively larger rolls. A small work roll lowers the contact area and the required separating force, so the mill can reduce stainless steel, silicon electrical steel and titanium strip down to a few hundredths of a millimetre. A small roll on its own would deflect and bend, so the 20-high roll cluster braces it from every side and passes the rolling load outward into the frame.
What a cluster mill rolls and why
Hard alloys work-harden quickly and need high reduction per coil, which drives up rolling force. On a conventional mill that force bends large work rolls and ruins gauge and flatness. The cluster arrangement breaks the problem into stages. The work roll only touches the strip; everything behind it exists to keep that roll straight and rigid. Because the work roll is small and replaceable, the mill rolls thin gauges, including foil, at high tension and high reduction without the roll deflection that limits a four-high stand.
The monobloc housing
The monobloc housing is the structural reason the cluster works. Instead of separate posts and caps bolted together, the frame is a single steel casting, the monobloc frame casting, with the backing saddle seats bored directly into it. The one-piece body is far stiffer than a built-up housing, so under 8 to 20 MN of rolling force the bores stay round and the roll axes stay parallel. End plates close the drive and operator ends, a housing cover retains the cluster, and the whole frame sits on the mill base plate. This rigidity is what lets the tiny work rolls survive the load.
The 20-high roll cluster
Loads pass from the strip outward through five rows. The two work rolls, usually tungsten carbide or hardened tool steel, sit against the strip. Behind them, four first intermediate rolls are driven and axially shiftable, the As-U rolls that set the broad crown. Six second intermediate rolls, some of them driven, carry the torque inward from the spindles. The outermost row is the eight backing bearing assemblies. Each is a backing bearing shaft riding on a row of bearing races separated by eccentric backing saddles, seated in the bored housing. The backing assemblies transmit the full rolling force into the frame over a wide footprint, which is how a 70 mm work roll can carry millions of newtons without bending. The cluster is the heart of the machine.
As-U-Roll crown and flatness control
Strip flatness depends on the shape of the roll gap across the width. The As-U-Roll crown system controls it by bending the backing shafts. Each backing shaft carries eccentric crown racks that rotate the backing saddles through crown adjustment shafts driven by individual crown servo motors. Rotating a saddle raises or lowers the shaft locally, bowing the backing assembly and changing the gap profile. The loop reads its target from the flatness measuring roll, a segmented roll whose shapemeter segments and pressure sensors measure strip tension across the width. The As-U controller compares that profile to target and adjusts the crown servos, giving the automatic flatness control that makes these mills suited to electrical steel and precision stainless.
Drive and high-tension coil handling
Torque enters through the drive train. The main drive motor, built from a stator assembly, rotor assembly and copper winding in a motor housing, feeds the gear distributor, which splits torque through gear pairs to four drive spindles turning the driven second intermediate rolls. Because Sendzimir mills are reversing, the coil handling line uses two tension reels, one each side, each with an expanding reel mandrel and a reel drive motor. The strip runs over deflector and bridle rolls under high tension, threaded by strip guides and monitored by a tensiometer. High strip tension reduces the rolling force needed for a given reduction, so tension control is part of the gauge strategy.
Coolant, hydraulics and control
The cluster runs flooded in low-viscosity rolling oil. The rolling oil system uses oil pumps, an oil tank, filters, spray headers with many nozzles, an oil cooler and a mist extractor. The roll gap is set by the hydraulic screwdown system, where gap cylinders driven through servo valves react against rolling force load cells and position sensors for automatic gauge control. Oil for the cylinders, crown system and reels comes from the hydraulic power unit, with its pumps, accumulators and valve manifold. The control system ties it together through the AGC board, the AFC loop, the drive control and the operator panel, reading encoders and pressure sensors across the mill.
Use and variants
Sendzimir mills dominate cold rolling of stainless steel sheet and strip, where the combination of small work rolls and tight flatness control gives consistent gauge on a hard material. They are the standard mill for grain-oriented and non-oriented silicon electrical steel, where flatness and thickness uniformity affect core loss. Narrow versions roll titanium and specialty alloys, and the thinnest gauges produce foil. Variants differ in width, number of stands and whether they run as standalone reversing mills or in tandem lines, but the 20-high cluster and monobloc frame remain the common pattern.
Sendzimir Cluster Mill parts and their functions
9 top-level parts · 1,344 parts in total · full bill of materials below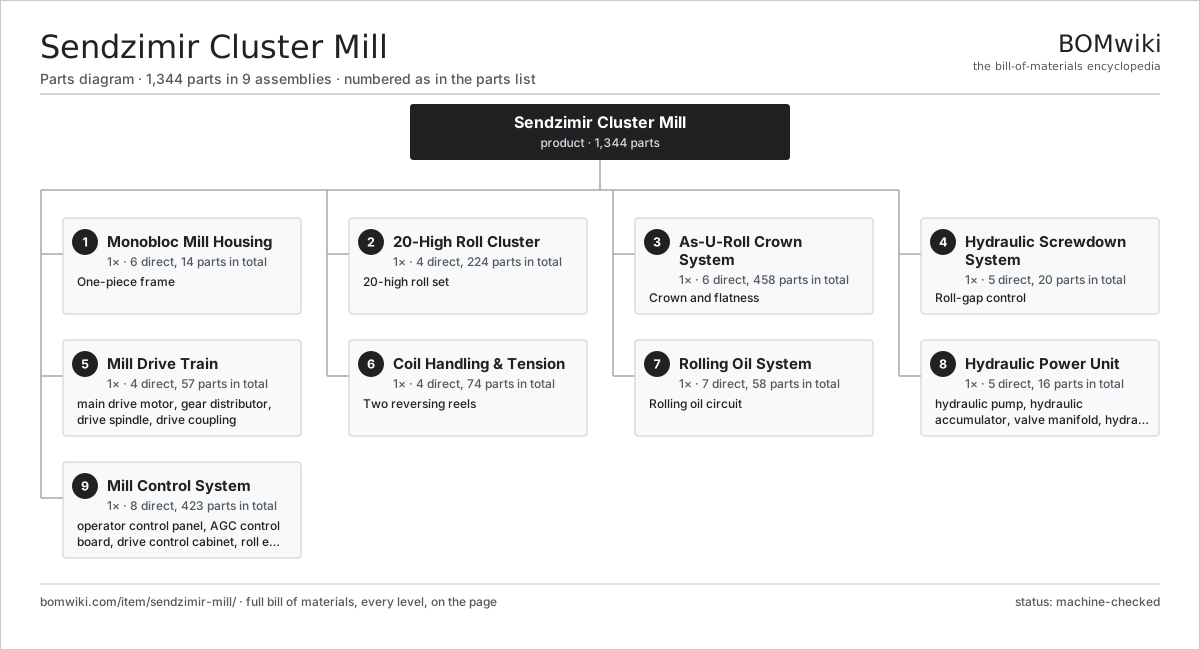
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Monobloc Mill Housing 6 parts | 1× | One-piece frame |
| 2 | 20-High Roll Cluster 4 parts | 1× | 20-high roll set |
| 3 | As-U-Roll Crown System 6 parts | 1× | Crown and flatness |
| 4 | Hydraulic Screwdown System 5 parts | 1× | Roll-gap control |
| 5 | Mill Drive Train 4 parts | 1× | Drives the second-intermediate rolls through spindles and a gear distributor. |
| 6 | Coil Handling & Tension 4 parts | 1× | Two reversing reels |
| 7 | Rolling Oil System 7 parts | 1× | Rolling oil circuit |
| 8 | Hydraulic Power Unit 5 parts | 1× | Supplies pressurised oil to the screwdown, crown and reel circuits. |
| 9 | Mill Control System 8 parts | 1× | AGC, AFC, drive control and operator interface. |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Sendzimir Cluster Mill
9 top-level lines · 118 rows shown · 1,344 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Monobloc Mill Housing 6 parts | sendzimir-mill-monobloc-housing | 1× | 1 | 14 | assembly |
| 1.1 | Monobloc Frame Casting | sendzimir-mill-monobloc-frame | 1× | 1 | · | part |
| 1.2 | Backing Saddle Seat | sendzimir-mill-saddle-seat | 8× | 8 | · | part |
| 1.3 | Housing Cover | sendzimir-mill-housing-cover | 1× | 1 | · | part |
| 1.4 | Housing End Plate | sendzimir-mill-end-plate | 2× | 2 | · | part |
| 1.5 | Mill Base Plate | sendzimir-mill-mill-base | 1× | 1 | · | part |
| 1.6 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 2 | 20-High Roll Cluster 4 parts | sendzimir-mill-roll-cluster | 1× | 1 | 224 | assembly |
| 2.1 | Work Roll | sendzimir-mill-work-roll | 2× | 2 | · | part |
| 2.2 | First Intermediate Roll 2 parts | sendzimir-mill-first-intermediate-roll | 4× | 4 | 3 | assembly |
| 2.2.1 | Roll Body | sendzimir-mill-roll-body | 1× | 4 | · | part |
| 2.2.2 | Roll Neck Bearing | sendzimir-mill-roll-neck-bearing | 2× | 8 | · | part |
| 2.3 | Second Intermediate Roll 2 parts | sendzimir-mill-second-intermediate-roll | 6× | 6 | 3 | assembly |
| 2.3.1 | Roll Body | sendzimir-mill-roll-body | 1× | 6 | · | part |
| 2.3.2 | Roll Neck Bearing | sendzimir-mill-roll-neck-bearing | 2× | 12 | · | part |
| 2.4 | Backing Bearing Assembly 5 parts | sendzimir-mill-backing-assembly | 8× | 8 | 24 | assembly |
| 2.4.1 | Backing Bearing Shaft | sendzimir-mill-backing-shaft | 1× | 8 | · | part |
| 2.4.2 | Ball Bearing | ball-bearing | 7× | 56 | · | part |
| 2.4.3 | Eccentric Backing Saddle | sendzimir-mill-backing-saddle | 6× | 48 | · | part |
| 2.4.4 | Backing Shaft Spacer | sendzimir-mill-shaft-spacer | 8× | 64 | · | part |
| 2.4.5 | O-Ring Set | oring-set | 2× | 16 | · | part |
| 3 | As-U-Roll Crown System 6 parts | sendzimir-mill-asu-crown-system | 1× | 1 | 458 | assembly |
| 3.1 | Eccentric Crown Rack | sendzimir-mill-crown-rack | 8× | 8 | · | part |
| 3.2 | Crown Adjustment Shaft | sendzimir-mill-crown-shaft | 8× | 8 | · | part |
| 3.3 | Servo Motor 4 parts | servo-motor | 8× | 8 | 24 | assembly |
| 3.3.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 8 | 3 | assembly |
| 3.3.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 8 | 19 | assembly |
| 3.3.3 | Encoder | encoder | 1× | 8 | · | part |
| 3.3.4 | Motor Housing | motor-housing | 1× | 8 | · | part |
| 3.4 | Flatness Measuring Roll 4 parts | sendzimir-mill-flatness-roll | 1× | 1 | 67 | assembly |
| 3.4.1 | Shapemeter Segment | sendzimir-mill-shapemeter-segment | 32× | 32 | · | part |
| 3.4.2 | Pressure Sensor | pressure-sensor | 32× | 32 | · | part |
| 3.4.3 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 3.4.4 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 3.5 | Helical Gear Pair | gear-pair | 8× | 8 | · | part |
| 3.6 | As-U / AFC Controller 4 parts | sendzimir-mill-asu-controller | 1× | 1 | 175 | assembly |
| 3.6.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 3.6.2 | Microcontroller | mcu | 2× | 2 | · | part |
| 3.6.3 | Connector | connector | 12× | 12 | · | part |
| 3.6.4 | SMD Passive (R/C/L) | smd-passives | 160× | 160 | · | part |
| 4 | Hydraulic Screwdown System 5 parts | sendzimir-mill-screwdown-system | 1× | 1 | 20 | assembly |
| 4.1 | Roll-Gap Cylinder 4 parts | sendzimir-mill-gap-cylinder | 2× | 2 | 5 | assembly |
| 4.1.1 | Cylinder Body | sendzimir-mill-cylinder-body | 1× | 2 | · | part |
| 4.1.2 | Cylinder Piston | sendzimir-mill-cylinder-piston | 1× | 2 | · | part |
| 4.1.3 | Oil Seal | oil-seal | 2× | 4 | · | part |
| 4.1.4 | O-Ring Set | oring-set | 1× | 2 | · | part |
| 4.2 | Servo Valve | sendzimir-mill-servo-valve | 2× | 2 | · | part |
| 4.3 | Gap Position Sensor | sendzimir-mill-position-sensor | 2× | 2 | · | part |
| 4.4 | Rolling Force Load Cell | sendzimir-mill-load-cell | 2× | 2 | · | part |
| 4.5 | O-Ring Set | oring-set | 4× | 4 | · | part |
| 5 | Mill Drive Train 4 parts | sendzimir-mill-drive-train | 1× | 1 | 57 | assembly |
| 5.1 | Main Drive Motor 5 parts | sendzimir-mill-main-motor | 1× | 1 | 26 | assembly |
| 5.1.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 5.1.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 5.1.3 | Copper Winding | copper-winding | 1× | 1 | · | part |
| 5.1.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 5.1.5 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 5.2 | Gear Distributor 4 parts | sendzimir-mill-gear-distributor | 1× | 1 | 17 | assembly |
| 5.2.1 | Helical Gear Pair | gear-pair | 4× | 4 | · | part |
| 5.2.2 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 5.2.3 | Ball Bearing | ball-bearing | 8× | 8 | · | part |
| 5.2.4 | Oil Seal | oil-seal | 4× | 4 | · | part |
| 5.3 | Drive Spindle 2 parts | sendzimir-mill-drive-spindle | 4× | 4 | 3 | assembly |
| 5.3.1 | Spindle Shaft | sendzimir-mill-spindle-shaft | 1× | 4 | · | part |
| 5.3.2 | Universal Joint | sendzimir-mill-universal-joint | 2× | 8 | · | part |
| 5.4 | Drive Coupling | sendzimir-mill-coupling | 2× | 2 | · | part |
| 6 | Coil Handling & Tension 4 parts | sendzimir-mill-coil-handling | 1× | 1 | 74 | assembly |
| 6.1 | Tension Reel 4 parts | sendzimir-mill-tension-reel | 2× | 2 | 29 | assembly |
| 6.1.1 | Reel Mandrel | sendzimir-mill-reel-mandrel | 1× | 2 | · | part |
| 6.1.2 | Reel Drive Motor 4 parts + deeper › | sendzimir-mill-reel-motor | 1× | 2 | 25 | assembly |
| 6.1.3 | Ball Bearing | ball-bearing | 2× | 4 | · | part |
| 6.1.4 | Helical Gear Pair | gear-pair | 1× | 2 | · | part |
| 6.2 | Deflector / Bridle Roll 2 parts | sendzimir-mill-deflector-roll | 4× | 4 | 3 | assembly |
| 6.2.1 | Roll Body | sendzimir-mill-roll-body | 1× | 4 | · | part |
| 6.2.2 | Ball Bearing | ball-bearing | 2× | 8 | · | part |
| 6.3 | Strip Threading Guide | sendzimir-mill-strip-guide | 2× | 2 | · | part |
| 6.4 | Strip Tensiometer | sendzimir-mill-tensiometer | 2× | 2 | · | part |
| 7 | Rolling Oil System 7 parts | sendzimir-mill-coolant-system | 1× | 1 | 58 | assembly |
| 7.1 | Rolling Oil Pump | sendzimir-mill-oil-pump | 2× | 2 | · | part |
| 7.2 | Rolling Oil Tank | sendzimir-mill-oil-tank | 1× | 1 | · | part |
| 7.3 | Rolling Oil Filter | sendzimir-mill-oil-filter | 2× | 2 | · | part |
| 7.4 | Oil Spray Header 2 parts | sendzimir-mill-spray-header | 2× | 2 | 25 | assembly |
| 7.4.1 | Header Pipe | sendzimir-mill-header-pipe | 1× | 2 | · | part |
| 7.4.2 | Oil Spray Nozzle | sendzimir-mill-spray-nozzle | 24× | 48 | · | part |
| 7.5 | Oil Cooler | sendzimir-mill-oil-cooler | 1× | 1 | · | part |
| 7.6 | Oil Mist Extractor | sendzimir-mill-mist-extractor | 1× | 1 | · | part |
| 7.7 | Rolling Oil | sendzimir-mill-rolling-oil | 1× | 1 | · | part |
| 8 | Hydraulic Power Unit 5 parts | sendzimir-mill-hydraulic-power-unit | 1× | 1 | 16 | assembly |
| 8.1 | Hydraulic Pump | sendzimir-mill-hydraulic-pump | 2× | 2 | · | part |
| 8.2 | Hydraulic Accumulator | sendzimir-mill-accumulator | 2× | 2 | · | part |
| 8.3 | Valve Manifold 3 parts | sendzimir-mill-valve-manifold | 1× | 1 | 9 | assembly |
| 8.3.1 | Manifold Block | sendzimir-mill-manifold-block | 1× | 1 | · | part |
| 8.3.2 | Control Valve | sendzimir-mill-control-valve | 6× | 6 | · | part |
| 8.3.3 | O-Ring Set | oring-set | 2× | 2 | · | part |
| 8.4 | Hydraulic Reservoir | sendzimir-mill-reservoir | 1× | 1 | · | part |
| 8.5 | Hydraulic Filter | sendzimir-mill-hpu-filter | 2× | 2 | · | part |
| 9 | Mill Control System 8 parts | sendzimir-mill-control-system | 1× | 1 | 423 | assembly |
| 9.1 | Operator Control Panel 4 parts | sendzimir-mill-control-panel | 1× | 1 | 166 | assembly |
| 9.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 9.1.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 9.1.3 | Connector | connector | 24× | 24 | · | part |
| 9.1.4 | SMD Passive (R/C/L) | smd-passives | 140× | 140 | · | part |
| 9.2 | AGC Control Board 4 parts | sendzimir-mill-agc-board | 1× | 1 | 199 | assembly |
| 9.2.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 9.2.2 | Microcontroller | mcu | 2× | 2 | · | part |
| 9.2.3 | Connector | connector | 16× | 16 | · | part |
| 9.2.4 | SMD Passive (R/C/L) | smd-passives | 180× | 180 | · | part |
| 9.3 | Drive Control Cabinet 5 parts | sendzimir-mill-drive-control | 1× | 1 | 31 | assembly |
| 9.3.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 9.3.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 9.3.3 | Relay | relay | 8× | 8 | · | part |
| 9.3.4 | Power Supply | power-supply | 1× | 1 | · | part |
| 9.3.5 | Connector | connector | 20× | 20 | · | part |
| 9.4 | Roll Encoder | sendzimir-mill-encoder | 4× | 4 | · | part |
| 9.5 | Pressure Sensor | pressure-sensor | 4× | 4 | · | part |
| 9.6 | Relay | relay | 16× | 16 | · | part |
| 9.7 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 9.8 | Power Supply | power-supply | 2× | 2 | · | part |
Related products
same domain, ranked by shared parts Bed-Type Milling Machine
151 parts · shares 4 with this page
 Bevel Gear Generator
201 parts · shares 4 with this page
Centering and Facing Machine
1,419 parts · shares 4 with this page
Cold Rolling Mill
991 parts · shares 4 with this page
 Creep-Feed Grinder
571 parts · shares 4 with this page
Cut-to-Length Line
500 parts · shares 4 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
1,152-word article