Stud and Track Rollformer
ProductOverview
A stud and track rollformer makes the light-gauge steel framing used for interior walls, partitions, ceilings, and load-bearing cold-formed buildings. It roll forms two matching sections from galvanized steel coil: the C-shaped stud that stands vertically and the U-shaped track that caps the wall top and bottom and receives the stud ends. The strip passes through a row of roller stands that bend it gradually into the section, with the service knockouts and notches punched into the flat strip before forming and each piece cut to length on the move. The output is bundles of studs and tracks cut to a job's cutting list, ready to ship to a building site.
Coil feeds from the Strip Decoiler through the Feed and Guide to the Pre-Punch Station station, then into the Roll Forming Line driven by the Forming Line Drive. The Profile Change System system resets the rolls between profiles, the Flying Cutoff Press cuts sections to length, and the Runout and Stacker bundles them. The Control System holds the cut list and times everything.
Pre-punching before forming
Studs and tracks need features that are far easier to punch in flat strip than in a formed section. The Pre-Punch Station station does this work first. The Service Knockout Die punches the service knockouts in the stud web through which cables and pipes later run, and the End Notch Die notches the flange ends so a stud seats cleanly into a track. Both are driven by the Punch Press Unit unit, whose Punch Ram and Punch Cylinder strike on the moving strip, with slugs dropping into the Slug Tray. Punching flat means the holes are accurately placed and the punch tooling is simple.
Roll forming the section
The Roll Forming Line forms the section the same way any rollformer does, by bending in small steps across many stands. Each Forming Stand holds a pair of profiled Form Roll rolls on driven Roll Shaft shafts, and the stand sequence first turns the flange returns up, then forms the web-to-flange corners, then sets the final flange angle and the small return lips that stiffen a C-stud. Side Forming Roll vertical rolls square the flanges. All stands sit on a machined Base Rail for a true pass line, and a Width Adjust Screw at each stand trims roll position.
The rolls are hardened tool steel, since they form galvanized steel continuously and must keep the zinc coating intact, because a scratched coating is where framing later rusts. Section depth and flange size are set by the roll profile, so the depth range a machine covers is built into its roll set.
Driving the line and changing profile
The Forming Line Drive turns all stands together so the strip is pulled through evenly. A Servo Motor feeds the Line Gearbox that sets line speed, and a Line Drive Shaft with a Drive Chain Set distributes drive to every stand through Drive Coupling couplings, keeping all roll surface speeds matched.
What distinguishes a modern framing rollformer is fast width change. The Profile Change System system moves rolls on their shafts by powered Ball Screw spacing screws driven from a Width Actuator, with Roll Position Encoder feedback, so the machine can switch from one stud width to another, or from stud to track, in minutes without a manual roll change. This lets one line serve a whole framing job from a single program.
Cutting to length and bundling
Framing is cut to a precise length per piece, and the line does not stop to cut. The Flying Cutoff Press is a flying die press: the Flying Carriage accelerates to match line speed, the Press Cylinder drives a profiled Profile Cutoff Die through the running section for a clean square cut, then the carriage returns, all triggered by the Encoder Wheel. The die is shaped to the section so it cuts web and flanges in one stroke. Cut pieces run onto the Runout and Stacker table where the Section Stacker nests them into bundles by type and length.
Materials, variants, and use
Strip is galvanized steel, typically 0.5 to 2.0 mm, in the zinc coating weight the building code calls for, since heavier coatings go into exterior and structural framing. Light non-structural lines make partition studs and tracks at high speed in thin gauge, while structural cold-formed steel lines run thicker gauge for load-bearing walls, floor joists, and roof trusses, often with extra stiffening lips and bridging holes. A line is built around a section family and depth range; the roll set defines the profile while length and the cut list are fully programmable. The studs and tracks these lines make frame the interior walls of nearly all commercial buildings and a growing share of houses built in cold-formed steel.
Control and the cut list
The Control System runs the job. A PLC holds the cut list, the schedule of section type, width, length, and quantity, and works through it automatically: setting line speed through the Line Drive VFD, firing the Pre-Punch Station dies and the flying Flying Cutoff Press at the right positions from the Encoder Wheel, and driving the Profile Change System system to switch width between batches. Operators import or enter the cut list at the LCD Panel and the line produces a whole framing package labelled and bundled, which is why these machines are run both in framing factories and on portable trailers at large construction sites.
Stud and Track Rollformer parts and their functions
9 top-level parts · 517 parts in total · full bill of materials below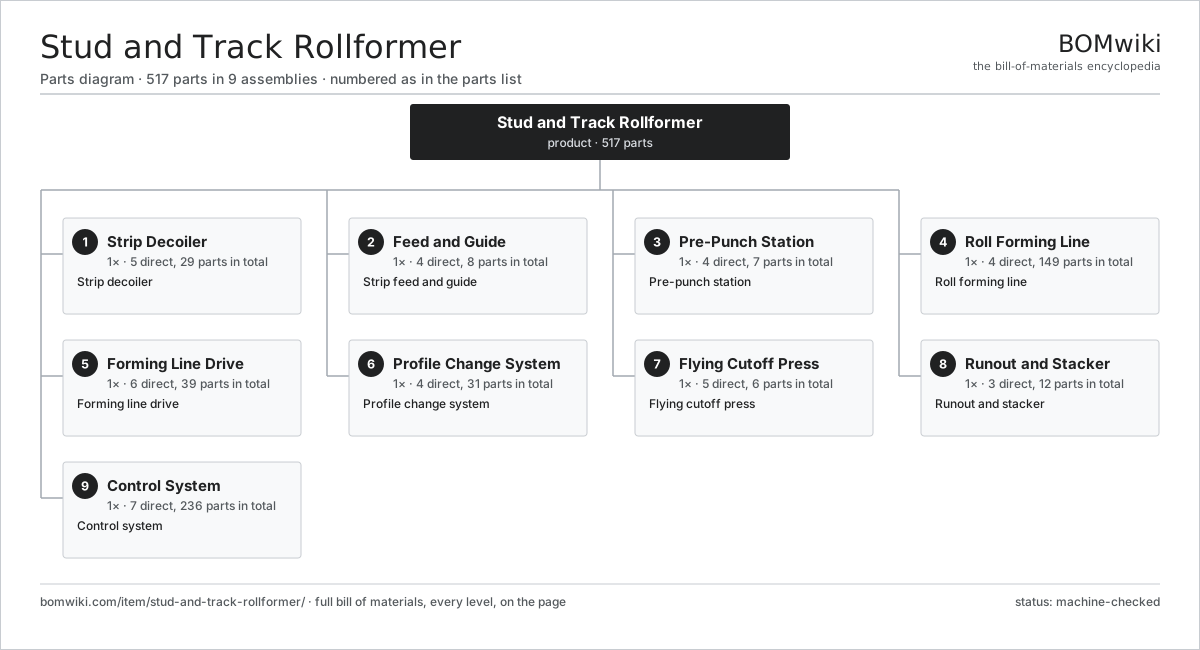
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Strip Decoiler 5 parts | 1× | Strip decoiler |
| 2 | Feed and Guide 4 parts | 1× | Strip feed and guide |
| 3 | Pre-Punch Station 4 parts | 1× | Pre-punch station |
| 4 | Roll Forming Line 4 parts | 1× | Roll forming line |
| 5 | Forming Line Drive 6 parts | 1× | Forming line drive |
| 6 | Profile Change System 4 parts | 1× | Profile change system |
| 7 | Flying Cutoff Press 5 parts | 1× | Flying cutoff press |
| 8 | Runout and Stacker 3 parts | 1× | Runout and stacker |
| 9 | Control System 7 parts | 1× | Control system |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Stud and Track Rollformer
9 top-level lines · 82 rows shown · 517 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Strip Decoiler 5 parts | stud-and-track-rollformer-decoiler | 1× | 1 | 29 | assembly |
| 1.1 | Expanding Mandrel | stud-and-track-rollformer-mandrel | 1× | 1 | · | part |
| 1.2 | Decoiler Brake | stud-and-track-rollformer-brake | 1× | 1 | · | part |
| 1.3 | Coil Car | stud-and-track-rollformer-coil-car | 1× | 1 | · | part |
| 1.4 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 1.5 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 1.5.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 1.5.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 1.5.3 | Encoder | encoder | 1× | 1 | · | part |
| 1.5.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 2 | Feed and Guide 4 parts | stud-and-track-rollformer-feed | 1× | 1 | 8 | assembly |
| 2.1 | Entry Edge Guide | stud-and-track-rollformer-entry-guide | 1× | 1 | · | part |
| 2.2 | Feed Roll | stud-and-track-rollformer-feed-rolls | 2× | 2 | · | part |
| 2.3 | Strip Sensor | stud-and-track-rollformer-strip-sensor | 1× | 1 | · | part |
| 2.4 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 3 | Pre-Punch Station 4 parts | stud-and-track-rollformer-prepunch | 1× | 1 | 7 | assembly |
| 3.1 | Service Knockout Die | stud-and-track-rollformer-knockout-die | 1× | 1 | · | part |
| 3.2 | End Notch Die | stud-and-track-rollformer-notch-die | 1× | 1 | · | part |
| 3.3 | Punch Press Unit 3 parts | stud-and-track-rollformer-punch-press | 1× | 1 | 4 | assembly |
| 3.3.1 | Punch Ram | stud-and-track-rollformer-punch-ram | 1× | 1 | · | part |
| 3.3.2 | Punch Cylinder | stud-and-track-rollformer-punch-cylinder | 1× | 1 | · | part |
| 3.3.3 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 3.4 | Slug Tray | stud-and-track-rollformer-slug-tray | 1× | 1 | · | part |
| 4 | Roll Forming Line 4 parts | stud-and-track-rollformer-roll-line | 1× | 1 | 149 | assembly |
| 4.1 | Forming Stand 5 parts | stud-and-track-rollformer-roll-stand | 12× | 12 | 11 | assembly |
| 4.1.1 | Form Roll | stud-and-track-rollformer-form-roll | 2× | 24 | · | part |
| 4.1.2 | Roll Shaft | stud-and-track-rollformer-roll-shaft | 2× | 24 | · | part |
| 4.1.3 | Stand Frame | stud-and-track-rollformer-stand-frame | 1× | 12 | · | part |
| 4.1.4 | Width Adjust Screw | stud-and-track-rollformer-adjust-screw | 2× | 24 | · | part |
| 4.1.5 | Ball Bearing | ball-bearing | 4× | 48 | · | part |
| 4.2 | Base Rail | stud-and-track-rollformer-base-rail | 1× | 1 | · | part |
| 4.3 | Side Forming Roll | stud-and-track-rollformer-side-roll | 4× | 4 | · | part |
| 4.4 | Drive Coupling | stud-and-track-rollformer-shaft-coupling | 12× | 12 | · | part |
| 5 | Forming Line Drive 6 parts | stud-and-track-rollformer-drive | 1× | 1 | 39 | assembly |
| 5.1 | Line Gearbox 3 parts | stud-and-track-rollformer-gearbox | 1× | 1 | 8 | assembly |
| 5.1.1 | Helical Gear Pair | gear-pair | 2× | 2 | · | part |
| 5.1.2 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 5.1.3 | Oil Seal | oil-seal | 2× | 2 | · | part |
| 5.2 | Line Drive Shaft | stud-and-track-rollformer-drive-shaft | 1× | 1 | · | part |
| 5.3 | Drive Chain Set | stud-and-track-rollformer-chain-set | 1× | 1 | · | part |
| 5.4 | Helical Gear Pair | gear-pair | 4× | 4 | · | part |
| 5.5 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 5.5.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 5.5.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 5.5.3 | Encoder | encoder | 1× | 1 | · | part |
| 5.5.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 5.6 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 6 | Profile Change System 4 parts | stud-and-track-rollformer-profile-change | 1× | 1 | 31 | assembly |
| 6.1 | Width Actuator | stud-and-track-rollformer-width-actuator | 1× | 1 | · | part |
| 6.2 | Roll Position Encoder | stud-and-track-rollformer-position-encoder | 4× | 4 | · | part |
| 6.3 | Ball Screw | ball-screw | 2× | 2 | · | part |
| 6.4 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 6.4.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 6.4.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 6.4.3 | Encoder | encoder | 1× | 1 | · | part |
| 6.4.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 7 | Flying Cutoff Press 5 parts | stud-and-track-rollformer-cutoff | 1× | 1 | 6 | assembly |
| 7.1 | Profile Cutoff Die | stud-and-track-rollformer-cutoff-die | 1× | 1 | · | part |
| 7.2 | Flying Carriage | stud-and-track-rollformer-cutoff-carriage | 1× | 1 | · | part |
| 7.3 | Press Cylinder | stud-and-track-rollformer-cutoff-cylinder | 1× | 1 | · | part |
| 7.4 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 7.5 | Encoder Wheel | stud-and-track-rollformer-encoder-wheel | 1× | 1 | · | part |
| 8 | Runout and Stacker 3 parts | stud-and-track-rollformer-runout | 1× | 1 | 12 | assembly |
| 8.1 | Runout Roller | stud-and-track-rollformer-runout-roller | 10× | 10 | · | part |
| 8.2 | Section Stacker | stud-and-track-rollformer-stacker | 1× | 1 | · | part |
| 8.3 | Runout Frame | stud-and-track-rollformer-runout-frame | 1× | 1 | · | part |
| 9 | Control System 7 parts | stud-and-track-rollformer-control | 1× | 1 | 236 | assembly |
| 9.1 | PLC 3 parts | stud-and-track-rollformer-plc | 1× | 1 | 122 | assembly |
| 9.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 9.1.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 9.1.3 | SMD Passive (R/C/L) | smd-passives | 120× | 120 | · | part |
| 9.2 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 9.3 | Line Drive VFD 5 parts | stud-and-track-rollformer-vfd | 1× | 1 | 89 | assembly |
| 9.3.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 9.3.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 9.3.3 | Power MOSFET | mosfet | 6× | 6 | · | part |
| 9.3.4 | Gate Driver IC | gate-driver-ic | 1× | 1 | · | part |
| 9.3.5 | SMD Passive (R/C/L) | smd-passives | 80× | 80 | · | part |
| 9.4 | Power Supply | power-supply | 1× | 1 | · | part |
| 9.5 | Relay | relay | 8× | 8 | · | part |
| 9.6 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 9.7 | Connector | connector | 14× | 14 | · | part |
Related products
same domain, ranked by shared parts Servo Stamping Press
633 parts · shares 4 with this page
 Industrial TIG Welder
492 parts · shares 3 with this page
 Railway Wheel Lathe
1,201 parts · shares 7 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
1,059-word article