Shot Peening Machine
ProductOverview
A shot peening machine bombards the surface of a metal part with a controlled stream of small round shot to leave it in compression. Each piece of shot is a tiny ball travelling fast enough to dent the surface, and each dent stretches the skin of the metal a little. The layer underneath resists that stretch, so once the whole surface is covered in overlapping dimples it is locked into compressive residual stress, typically a few tenths of a millimetre deep. Fatigue cracks start at the surface and only grow under tension, so a surface held in compression has to be pulled into tension before a crack can open. That delay is the whole point: a peened part survives many more load cycles than the same part untreated. The process is used where fatigue decides service life, on gears, valve springs and suspension springs, aircraft landing gear, and turbine disks and blades.
This machine is the air-blast type. Compressed air carries the shot through a Blast Nozzle and accelerates it onto the part, with shot velocity set by air pressure and shot mass flow set by a metering valve. The work sits inside a Blast Cabinet on a Rotary Table, the nozzles ride a Nozzle Manipulator, and the spent shot is gathered, cleaned and fed back so the same charge of media recirculates for a long time.
How peening works
Removal is not the goal here, deformation is. When a hard ball strikes the surface at speed it makes a small permanent dimple and yields a thin skin of metal outward. The bulk beneath stays elastic and pulls that skin back, which leaves the skin in compression and the substrate in a balancing tension deeper down. Build enough overlapping dimples and the surface carries a uniform compressive layer. Because cracks need tension to propagate, the part now has to spend part of every load cycle just overcoming the built-in compression before the surface sees any net tension. The benefit is largest on parts that fail by high-cycle fatigue and on surfaces left rough or with tensile residual stress by grinding, machining or heat treatment.
Almen intensity and coverage
Two numbers control the result: intensity and coverage. Intensity is measured with an Almen strip, a standard steel coupon clamped flat and exposed to the same blast as the part. The strip arcs because only one face is peened, and the arc height read on an Almen gauge is the intensity, quoted as a value such as 12 A on the A-scale strip. A given intensity comes from a specific combination of shot size, air pressure, media flow, standoff and dwell, and the Almen Flow Monitor watches the live pressure from the Air Supply + Prep and the live shot flow from the Media Flow Monitor so the machine stays on the settings that produced the qualified value. Coverage is the fraction of the surface actually dimpled, driven past full coverage to be sure no bare metal is left, and it is set by how long each area is exposed, which on this machine is the table speed and the manipulator path.
Holding intensity steady is why media classification matters. Shot wears, cracks and shatters as it recirculates, and broken or undersized shot peens softer and less predictably than full-size round shot. The Media Classifier removes the bad media every pass: a Air-Wash Separator blows out dust and fines, a Spiral Separator rolls round shot away from broken fragments, and a Classifier Screen holds the working size band. Without that, the size distribution drifts and the Almen intensity drifts with it.
Subsystems
Clean shot is held in the Clean Shot Hopper and metered into the air line by the Shot Delivery system, where a Pressure Pot forces shot through the Media Metering Valve into the air stream. The nozzles are carried by the manipulator on three servo axes built around a Ball Screw and Linear Guide Rail rails and driven by a Servo Motor, while the part turns on the rotary table through a Table Reducer. After impact the shot falls to the cabinet floor and the Shot Recovery + Reclaim system, a Screw Conveyor feeding a Bucket Elevator, lifts it back to the classifier. Dust and fines pulled off the cabinet and the air-wash are captured by the Dust Collector through pleated cartridges and an exhaust fan. The whole sequence is run from the Control + Almen Monitoring cabinet, which drives the Servo Drive units and shows status on the Operator HMI.
Materials
The parts in the shot path wear fast and are chosen for it. The Blast Nozzle and the Media Metering Valve use tungsten carbide so the bore holds its shape, because a worn bore widens the stream and quietly lowers intensity. The cabinet is lined with Wear Liner panels in manganese steel, which work-hardens under the constant impact instead of simply abrading away. The Conveyor Auger and other transport surfaces use abrasion-resistant steel. The shot itself is cast steel for most work, ceramic where a harder finer finish is wanted, or glass bead where iron contamination of the surface must be avoided, for example on stainless and aluminium.
Air-blast versus wheel-blast
This machine throws shot with compressed air. The other common family is wheel-blast, where a spinning bladed wheel flings shot by centrifugal force at high mass flow. Wheel machines move far more shot per minute and suit large flat or bulk parts where throughput matters, but the stream is broad and harder to aim. Air-blast machines move less shot but place it precisely through a small nozzle, reach into bores, fillets and gear roots, and let a CNC manipulator follow a complex path, which is why air-blast is used for controlled peening of critical parts. The trade is rate against precision and reach.
Use cases
The work that justifies controlled peening is fatigue-critical and often expensive. Gears are peened in the tooth root and flank, where bending fatigue starts. Valve and suspension springs are peened to add cycles to a part that flexes millions of times. Aircraft landing gear, machined from high-strength steel and loaded hard, is peened on every fatigue-sensitive surface and the result is certified by Almen strip records. Turbine disks and blades are peened to resist the combination of high stress and high cycle count they see in service. In all of these the value comes from a peen that is measured and repeatable, which is why the Media Classifier and the Almen Flow Monitor are as central to the machine as the nozzles themselves.
Shot Peening Machine parts and their functions
10 top-level parts · 586 parts in total · full bill of materials below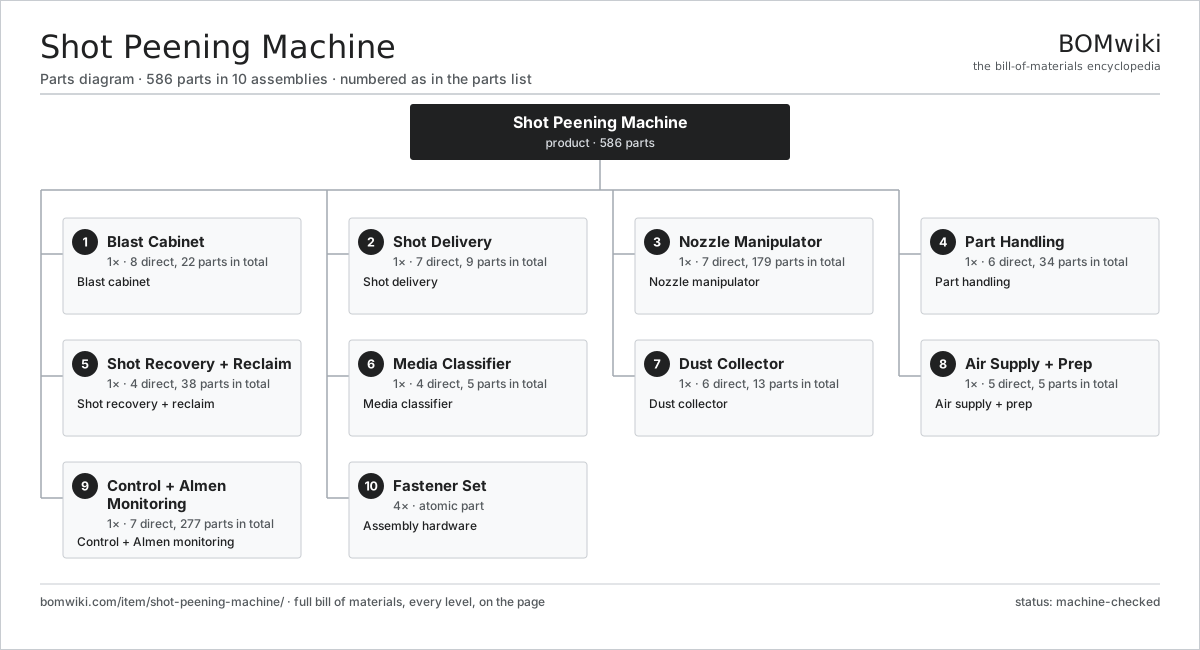
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Blast Cabinet 8 parts | 1× | Blast cabinet |
| 2 | Shot Delivery 7 parts | 1× | Shot delivery |
| 3 | Nozzle Manipulator 7 parts | 1× | Nozzle manipulator |
| 4 | Part Handling 6 parts | 1× | Part handling |
| 5 | Shot Recovery + Reclaim 4 parts | 1× | Shot recovery + reclaim |
| 6 | Media Classifier 4 parts | 1× | Media classifier |
| 7 | Dust Collector 6 parts | 1× | Dust collector |
| 8 | Air Supply + Prep 5 parts | 1× | Air supply + prep |
| 9 | Control + Almen Monitoring 7 parts | 1× | Control + Almen monitoring |
| 10 | Fastener Set | 4× | Assembly hardware |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Shot Peening Machine
10 top-level lines · 100 rows shown · 586 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Blast Cabinet 8 parts | shot-peening-machine-cabinet | 1× | 1 | 22 | assembly |
| 1.1 | Cabinet Frame | shot-peening-machine-cabinet-frame | 1× | 1 | · | part |
| 1.2 | Sheet Metal Panel | sheet-panel | 8× | 8 | · | part |
| 1.3 | Wear Liner | shot-peening-machine-liner | 6× | 6 | · | part |
| 1.4 | View Window | shot-peening-machine-view-window | 1× | 1 | · | part |
| 1.5 | Access Door | shot-peening-machine-door | 1× | 1 | · | part |
| 1.6 | Door Interlock | shot-peening-machine-interlock | 2× | 2 | · | part |
| 1.7 | Collection Hopper | shot-peening-machine-hopper | 1× | 1 | · | part |
| 1.8 | Fastener Set | fastener-set | 2× | 2 | · | part |
| 2 | Shot Delivery 7 parts | shot-peening-machine-delivery | 1× | 1 | 9 | assembly |
| 2.1 | Pressure Pot | shot-peening-machine-pressure-pot | 1× | 1 | · | part |
| 2.2 | Media Metering Valve | shot-peening-machine-media-valve | 1× | 1 | · | part |
| 2.3 | Media Flow Monitor | shot-peening-machine-flow-sensor | 1× | 1 | · | part |
| 2.4 | Air/Media Mixing Tee | shot-peening-machine-mixing-tee | 1× | 1 | · | part |
| 2.5 | Abrasive Delivery Hose | shot-peening-machine-delivery-hose | 2× | 2 | · | part |
| 2.6 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 2.7 | O-Ring Set | oring-set | 2× | 2 | · | part |
| 3 | Nozzle Manipulator 7 parts | shot-peening-machine-nozzle-manipulator | 1× | 1 | 179 | assembly |
| 3.1 | Blast Nozzle | shot-peening-machine-nozzle | 2× | 2 | · | part |
| 3.2 | Nozzle Holder | shot-peening-machine-nozzle-holder | 2× | 2 | · | part |
| 3.3 | Manipulator Axis 5 parts | shot-peening-machine-manip-axis | 3× | 3 | 31 | assembly |
| 3.3.1 | Ball Screw | ball-screw | 1× | 3 | · | part |
| 3.3.2 | Linear Guide Rail | linear-guide | 2× | 6 | · | part |
| 3.3.3 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 3 | 24 | assembly |
| 3.3.4 | Ball Bearing | ball-bearing | 2× | 6 | · | part |
| 3.3.5 | Limit Switch | shot-peening-machine-limit-switch | 2× | 6 | · | part |
| 3.4 | Servo Motor 4 parts | servo-motor | 3× | 3 | 24 | assembly |
| 3.4.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 3 | 3 | assembly |
| 3.4.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 3 | 19 | assembly |
| 3.4.3 | Encoder | encoder | 1× | 3 | · | part |
| 3.4.4 | Motor Housing | motor-housing | 1× | 3 | · | part |
| 3.5 | Ball Screw | ball-screw | 3× | 3 | · | part |
| 3.6 | Linear Guide Rail | linear-guide | 6× | 6 | · | part |
| 3.7 | Nozzle Oscillator | shot-peening-machine-oscillator | 1× | 1 | · | part |
| 4 | Part Handling 6 parts | shot-peening-machine-part-handling | 1× | 1 | 34 | assembly |
| 4.1 | Rotary Table | shot-peening-machine-rotary-table | 1× | 1 | · | part |
| 4.2 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 4.2.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 4.2.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 4.2.3 | Encoder | encoder | 1× | 1 | · | part |
| 4.2.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 4.3 | Table Reducer 4 parts | shot-peening-machine-table-reducer | 1× | 1 | 5 | assembly |
| 4.3.1 | Helical Gear Pair | gear-pair | 1× | 1 | · | part |
| 4.3.2 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 4.3.3 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 4.3.4 | Oil Seal | oil-seal | 1× | 1 | · | part |
| 4.4 | Part Fixture | shot-peening-machine-fixture | 1× | 1 | · | part |
| 4.5 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 4.6 | Oil Seal | oil-seal | 1× | 1 | · | part |
| 5 | Shot Recovery + Reclaim 4 parts | shot-peening-machine-reclaim | 1× | 1 | 38 | assembly |
| 5.1 | Screw Conveyor 4 parts | shot-peening-machine-screw-conveyor | 1× | 1 | 6 | assembly |
| 5.1.1 | Conveyor Auger | shot-peening-machine-auger | 1× | 1 | · | part |
| 5.1.2 | Conveyor Motor | shot-peening-machine-conveyor-motor | 1× | 1 | · | part |
| 5.1.3 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 5.1.4 | Oil Seal | oil-seal | 2× | 2 | · | part |
| 5.2 | Bucket Elevator 4 parts | shot-peening-machine-bucket-elevator | 1× | 1 | 30 | assembly |
| 5.2.1 | Drive Belt | drive-belt | 1× | 1 | · | part |
| 5.2.2 | Elevator Bucket | shot-peening-machine-bucket | 24× | 24 | · | part |
| 5.2.3 | Elevator Motor | shot-peening-machine-elevator-motor | 1× | 1 | · | part |
| 5.2.4 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 5.3 | Clean Shot Hopper | shot-peening-machine-storage-hopper | 1× | 1 | · | part |
| 5.4 | Drive Belt | drive-belt | 1× | 1 | · | part |
| 6 | Media Classifier 4 parts | shot-peening-machine-classifier | 1× | 1 | 5 | assembly |
| 6.1 | Air-Wash Separator | shot-peening-machine-air-wash | 1× | 1 | · | part |
| 6.2 | Classifier Screen | shot-peening-machine-classifier-screen | 2× | 2 | · | part |
| 6.3 | Spiral Separator | shot-peening-machine-spiral-separator | 1× | 1 | · | part |
| 6.4 | Reject Chute | shot-peening-machine-reject-chute | 1× | 1 | · | part |
| 7 | Dust Collector 6 parts | shot-peening-machine-dust-collector | 1× | 1 | 13 | assembly |
| 7.1 | Filter Cartridge | shot-peening-machine-filter-cartridge | 4× | 4 | · | part |
| 7.2 | Exhaust Fan | shot-peening-machine-collector-fan | 1× | 1 | · | part |
| 7.3 | Pulse-Clean Valve | shot-peening-machine-pulse-valve | 4× | 4 | · | part |
| 7.4 | Dust Bin | shot-peening-machine-dust-bin | 1× | 1 | · | part |
| 7.5 | Drive Belt | drive-belt | 1× | 1 | · | part |
| 7.6 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 8 | Air Supply + Prep 5 parts | shot-peening-machine-air-supply | 1× | 1 | 5 | assembly |
| 8.1 | Air Dryer | shot-peening-machine-air-dryer | 1× | 1 | · | part |
| 8.2 | Pressure Regulator | shot-peening-machine-air-regulator | 1× | 1 | · | part |
| 8.3 | Air Filter/Separator | shot-peening-machine-air-filter | 1× | 1 | · | part |
| 8.4 | Air Receiver | shot-peening-machine-air-receiver | 1× | 1 | · | part |
| 8.5 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 9 | Control + Almen Monitoring 7 parts | shot-peening-machine-control | 1× | 1 | 277 | assembly |
| 9.1 | PLC Controller 4 parts | shot-peening-machine-plc | 1× | 1 | 150 | assembly |
| 9.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 9.1.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 9.1.3 | Relay | relay | 8× | 8 | · | part |
| 9.1.4 | SMD Passive (R/C/L) | smd-passives | 140× | 140 | · | part |
| 9.2 | Operator HMI 3 parts | shot-peening-machine-hmi | 1× | 1 | 42 | assembly |
| 9.2.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 9.2.2 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 9.2.3 | SMD Passive (R/C/L) | smd-passives | 40× | 40 | · | part |
| 9.3 | Almen Flow Monitor 4 parts | shot-peening-machine-almen-monitor | 1× | 1 | 63 | assembly |
| 9.3.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 9.3.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 9.3.3 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 9.3.4 | SMD Passive (R/C/L) | smd-passives | 60× | 60 | · | part |
| 9.4 | Servo Drive | shot-peening-machine-servo-drive | 4× | 4 | · | part |
| 9.5 | Power Supply | power-supply | 1× | 1 | · | part |
| 9.6 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 9.7 | Connector | connector | 16× | 16 | · | part |
| 10 | Fastener Set | fastener-set | 4× | 4 | · | part |
Related products
same domain, ranked by shared parts Creep-Feed Grinder
571 parts · shares 9 with this page
Drag Finishing Machine
735 parts · shares 9 with this page
 Railway Wheel Lathe
1,201 parts · shares 9 with this page
 Rotary-Table Surface Grinder
172 parts · shares 9 with this page
Spring End Grinding Machine
1,048 parts · shares 9 with this page
Strip Edge Trimming Machine
491 parts · shares 9 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
1,171-word article