Metal Deck Rollformer
ProductOverview
A metal deck rollformer turns a flat coil of galvanised steel into long corrugated panels that become the structural deck of floors and roofs. The strip never stops moving: it pays off a coil at one end, passes through a row of shaped rollers that bend it a little more at each pass, and comes out the far end as a finished profile that is sheared to length and stacked. Because the shape is made by rolling rather than pressing, one machine can run thousands of metres of identical deck in a shift, and the only limit on panel length is how the panels are handled after the cut.
The line is built around nine subsystems. The Hydraulic Decoiler holds the coil and feeds strip under tension. The Entry Guide and Leveller squares the strip and flattens it. The Roll-Forming Station Bank does the shaping. The Drive System turns every roll at the same speed. The Hydraulic Shear Press cuts each panel to length. The Run-Out Table and Stacker catches and stacks the panels. The PLC Control Panel runs the sequence, the Centralized Lubrication Unit keeps the bearings fed, and the Baseplate and Frame holds everything to a common pass line.
How it works
Forming happens in small steps. A flat strip cannot be folded into a deep corrugation in one move without splitting or buckling, so the profile is built up across many passes, each adding a few degrees of bend. The strip enters flat, picks up its first shallow ribs, and leaves the last stand as the full deck section. This gradual approach is why a deck line has 14 to 20 stations rather than one heavy press. The strip is pushed through by the rolls themselves, which all turn at one matched speed so the metal is neither stretched nor bunched between stands.
The decoiler runs the line from the back. Its Expanding Mandrel expands inside the coil bore through four Mandrel Jaw Segment shoes driven by the Mandrel Expansion Cylinder, so the coil is gripped from the inside and spins on the Decoiler Bearing Stand. A Friction Tension Brake drags on the hub to keep back-tension, and a Coil Hold-Down Arm stops the wrap springing loose. The strip then runs into the Seven-Roll Leveller, where seven staggered Leveller Work Roll rolls flex it past yield in alternating directions to take out the curve set by the coil. Without this step the finished panel would bow.
The forming stations
Each Forming Roll Stand is one pass of the profile. A Upper Roll Shaft and a Lower Roll Shaft carry a matched pair of Profiled Forming Roll rolls, positioned along the shaft by Shaft Spacer Ring rings to set the rib pitch. The shafts run in Ball Bearing bearings inside two Stand Side Housing side plates, and a Top Shaft Screw-Down sets the gap between the rolls. The forming rolls are tool steel hardened to about HRC 60 because they carry the full forming load on every metre of strip, and the whole roll set changes when the line switches to a different deck shape. Toward the end of the line a few Edge Side-Roll Stand stands carry vertical Vertical Side Roll rolls that turn up the panel edges to form the side lap by which one panel hooks to the next on site.
Drive, cutting, and control
Every lower shaft is driven, not idle. The Drive System takes a Servo Motor through a Helical Gearbox and a single Roller Drive Chain running over a Shaft Drive Sprocket on each shaft, with Chain Tensioner idlers keeping it tight. Driving all shafts together is what keeps the line speed matched across the profile.
Cutting is done after forming, not before, because a flat strip is easy to cut but a formed panel needs a shaped tool. The Length-Measuring Encoder counts panel length and tells the PLC when to fire. The Cutting Cylinder cylinders then drive the Hardened Cutting Blade down through the panel against the Profiled Shear Die, which is profiled to support the full section so the cut stays square. Oil comes from the Hydraulic Power Unit, where a Gear Pump feeds the Directional Control Valve under guard of a Pressure Relief Valve. The PLC Control Panel holds the PLC, the Line Drive VFD that ramps line speed, and the Touchscreen Operator Panel where the operator sets length, quantity, and profile.
Materials and roll sets
Deck is rolled from structural galvanised steel in grades from G350 up to G550, in thicknesses of 0.7 to 1.5 mm. The zinc coat means the line must not scuff the surface, so the Run-Out Roller rollers are free-turning and the rolls are kept clean. Higher grades spring back more after each bend, so a line set for G550 uses slightly tighter roll gaps to land on the same final shape. The profile itself is fixed by the forming rolls, so changing from a 38 mm floor deck to a deeper roof deck means swapping the full roll set and resetting the Vertical Side Roll positions.
Use
Deck rollformers sit in steel-building plants and at large precast yards. They run long, repetitive orders where panel length is set by the building bay, often 6 to 12 m, and where every panel must match so the deck lays flat and the side laps engage. Floor deck carries wet concrete until it cures and then acts as permanent formwork and tension reinforcement; roof deck spans purlins and carries insulation and membrane above. The Run-Out Table and Stacker drops finished panels into neat bundles for banding and shipping, and the line is ready for the next length without changing tools as long as the profile stays the same.
Metal Deck Rollformer parts and their functions
9 top-level parts · 607 parts in total · full bill of materials below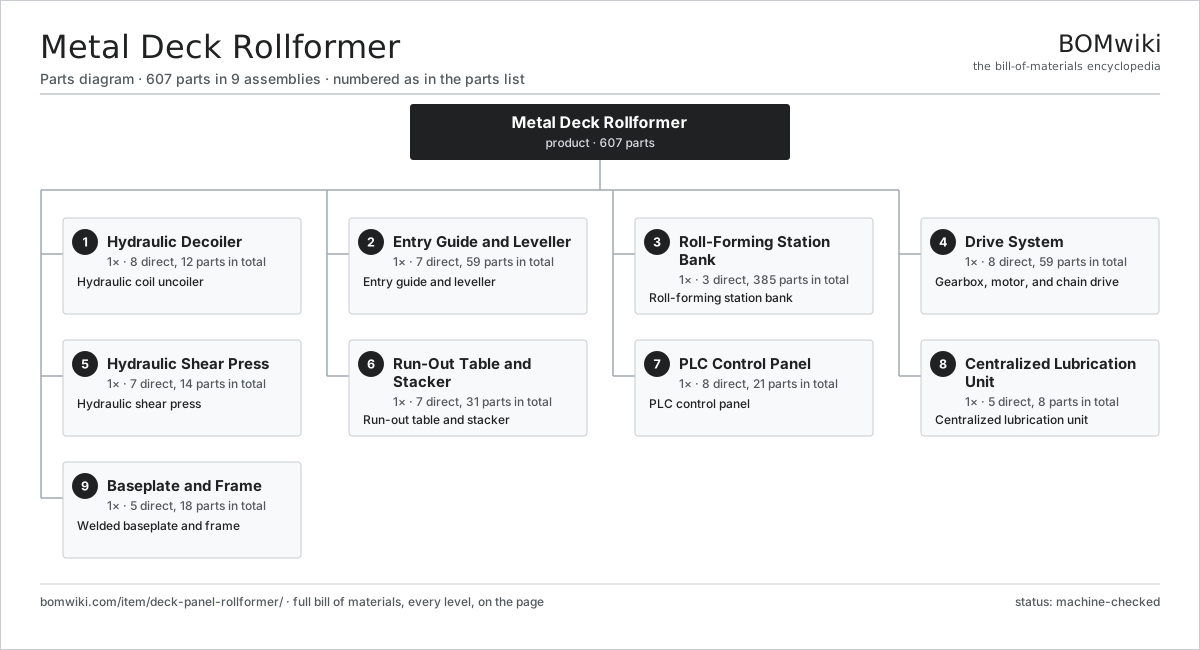
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Hydraulic Decoiler 8 parts | 1× | Hydraulic coil uncoiler |
| 2 | Entry Guide and Leveller 7 parts | 1× | Entry guide and leveller |
| 3 | Roll-Forming Station Bank 3 parts | 1× | Roll-forming station bank |
| 4 | Drive System 8 parts | 1× | Gearbox, motor, and chain drive |
| 5 | Hydraulic Shear Press 7 parts | 1× | Hydraulic shear press |
| 6 | Run-Out Table and Stacker 7 parts | 1× | Run-out table and stacker |
| 7 | PLC Control Panel 8 parts | 1× | PLC control panel |
| 8 | Centralized Lubrication Unit 5 parts | 1× | Centralized lubrication unit |
| 9 | Baseplate and Frame 5 parts | 1× | Welded baseplate and frame |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Metal Deck Rollformer
9 top-level lines · 99 rows shown · 607 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Hydraulic Decoiler 8 parts | deck-panel-rollformer-decoiler | 1× | 1 | 12 | assembly |
| 1.1 | Expanding Mandrel | deck-panel-rollformer-mandrel | 1× | 1 | · | part |
| 1.2 | Mandrel Jaw Segment | deck-panel-rollformer-mandrel-segment | 4× | 4 | · | part |
| 1.3 | Mandrel Expansion Cylinder | deck-panel-rollformer-expansion-cylinder | 1× | 1 | · | part |
| 1.4 | Decoiler Bearing Stand | deck-panel-rollformer-decoiler-stand | 1× | 1 | · | part |
| 1.5 | Friction Tension Brake | deck-panel-rollformer-brake-band | 1× | 1 | · | part |
| 1.6 | Coil Hold-Down Arm | deck-panel-rollformer-pressure-arm | 1× | 1 | · | part |
| 1.7 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 1.8 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 2 | Entry Guide and Leveller 7 parts | deck-panel-rollformer-entry-section | 1× | 1 | 59 | assembly |
| 2.1 | Adjustable Edge Guide | deck-panel-rollformer-entry-guide | 1× | 1 | · | part |
| 2.2 | Vertical Guide Roller | deck-panel-rollformer-guide-roller | 4× | 4 | · | part |
| 2.3 | Seven-Roll Leveller 4 parts | deck-panel-rollformer-leveller | 1× | 1 | 26 | assembly |
| 2.3.1 | Leveller Work Roll | deck-panel-rollformer-leveller-roll | 7× | 7 | · | part |
| 2.3.2 | Leveller Cassette Frame | deck-panel-rollformer-leveller-frame | 1× | 1 | · | part |
| 2.3.3 | Roll Gap Screw | deck-panel-rollformer-adjust-screw | 4× | 4 | · | part |
| 2.3.4 | Ball Bearing | ball-bearing | 14× | 14 | · | part |
| 2.4 | Leveller Work Roll | deck-panel-rollformer-leveller-roll | 7× | 7 | · | part |
| 2.5 | Feed Pinch Roll | deck-panel-rollformer-pinch-roll | 2× | 2 | · | part |
| 2.6 | Ball Bearing | ball-bearing | 18× | 18 | · | part |
| 2.7 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 3 | Roll-Forming Station Bank 3 parts | deck-panel-rollformer-forming-line | 1× | 1 | 385 | assembly |
| 3.1 | Forming Roll Stand 9 parts | deck-panel-rollformer-forming-station | 16× | 16 | 22 | assembly |
| 3.1.1 | Upper Roll Shaft | deck-panel-rollformer-top-shaft | 1× | 16 | · | part |
| 3.1.2 | Lower Roll Shaft | deck-panel-rollformer-bottom-shaft | 1× | 16 | · | part |
| 3.1.3 | Profiled Forming Roll | deck-panel-rollformer-forming-roll | 2× | 32 | · | part |
| 3.1.4 | Shaft Spacer Ring | deck-panel-rollformer-roll-spacer | 6× | 96 | · | part |
| 3.1.5 | Stand Side Housing | deck-panel-rollformer-stand-housing | 2× | 32 | · | part |
| 3.1.6 | Top Shaft Screw-Down | deck-panel-rollformer-screw-down | 1× | 16 | · | part |
| 3.1.7 | Ball Bearing | ball-bearing | 4× | 64 | · | part |
| 3.1.8 | Oil Seal | oil-seal | 4× | 64 | · | part |
| 3.1.9 | Fastener Set | fastener-set | 1× | 16 | · | part |
| 3.2 | Edge Side-Roll Stand 4 parts | deck-panel-rollformer-side-roll-stand | 4× | 4 | 8 | assembly |
| 3.2.1 | Vertical Side Roll | deck-panel-rollformer-side-roll | 2× | 8 | · | part |
| 3.2.2 | Side-Roll Mounting Bracket | deck-panel-rollformer-side-roll-bracket | 1× | 4 | · | part |
| 3.2.3 | Ball Bearing | ball-bearing | 4× | 16 | · | part |
| 3.2.4 | Fastener Set | fastener-set | 1× | 4 | · | part |
| 3.3 | Common Stand Baseplate | deck-panel-rollformer-stand-base | 1× | 1 | · | part |
| 4 | Drive System 8 parts | deck-panel-rollformer-drive-system | 1× | 1 | 59 | assembly |
| 4.1 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 4.1.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 4.1.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 4.1.3 | Encoder | encoder | 1× | 1 | · | part |
| 4.1.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 4.2 | Reduction Gearbox 4 parts | deck-panel-rollformer-gearbox | 1× | 1 | 9 | assembly |
| 4.2.1 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 4.2.2 | Helical Gear Pair | gear-pair | 2× | 2 | · | part |
| 4.2.3 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 4.2.4 | Oil Seal | oil-seal | 2× | 2 | · | part |
| 4.3 | Shaft Drive Sprocket | deck-panel-rollformer-drive-sprocket | 18× | 18 | · | part |
| 4.4 | Roller Drive Chain | deck-panel-rollformer-drive-chain | 1× | 1 | · | part |
| 4.5 | Chain Tensioner | deck-panel-rollformer-chain-tensioner | 4× | 4 | · | part |
| 4.6 | Motor-Gearbox Coupling | deck-panel-rollformer-coupling | 1× | 1 | · | part |
| 4.7 | Chain Guard Cover | deck-panel-rollformer-chain-guard | 1× | 1 | · | part |
| 4.8 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 5 | Hydraulic Shear Press 7 parts | deck-panel-rollformer-cutting-press | 1× | 1 | 14 | assembly |
| 5.1 | Welded Press Frame | deck-panel-rollformer-press-frame | 1× | 1 | · | part |
| 5.2 | Profiled Shear Die | deck-panel-rollformer-cut-die | 1× | 1 | · | part |
| 5.3 | Hardened Cutting Blade | deck-panel-rollformer-cut-blade | 1× | 1 | · | part |
| 5.4 | Cutting Cylinder | deck-panel-rollformer-cut-cylinder | 2× | 2 | · | part |
| 5.5 | Hydraulic Power Unit 7 parts | deck-panel-rollformer-hydraulic-power-unit | 1× | 1 | 7 | assembly |
| 5.5.1 | Gear Pump | deck-panel-rollformer-hydraulic-pump | 1× | 1 | · | part |
| 5.5.2 | Pump Drive Motor | deck-panel-rollformer-hydraulic-motor | 1× | 1 | · | part |
| 5.5.3 | Oil Reservoir | deck-panel-rollformer-hydraulic-tank | 1× | 1 | · | part |
| 5.5.4 | Directional Control Valve | deck-panel-rollformer-directional-valve | 1× | 1 | · | part |
| 5.5.5 | Pressure Relief Valve | deck-panel-rollformer-relief-valve | 1× | 1 | · | part |
| 5.5.6 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 5.5.7 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 5.6 | Length-Measuring Encoder | deck-panel-rollformer-cut-encoder | 1× | 1 | · | part |
| 5.7 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 6 | Run-Out Table and Stacker 7 parts | deck-panel-rollformer-runout-stacker | 1× | 1 | 31 | assembly |
| 6.1 | Run-Out Roller Table | deck-panel-rollformer-runout-table | 1× | 1 | · | part |
| 6.2 | Run-Out Roller | deck-panel-rollformer-runout-roller | 8× | 8 | · | part |
| 6.3 | Drop-Stack Arm | deck-panel-rollformer-stacker-arm | 2× | 2 | · | part |
| 6.4 | Stacker Arm Cylinder | deck-panel-rollformer-stack-cylinder | 2× | 2 | · | part |
| 6.5 | Adjustable Length Stop | deck-panel-rollformer-panel-stop | 1× | 1 | · | part |
| 6.6 | Ball Bearing | ball-bearing | 16× | 16 | · | part |
| 6.7 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 7 | PLC Control Panel 8 parts | deck-panel-rollformer-control-panel | 1× | 1 | 21 | assembly |
| 7.1 | Programmable Logic Controller | deck-panel-rollformer-plc | 1× | 1 | · | part |
| 7.2 | Touchscreen Operator Panel | deck-panel-rollformer-hmi | 1× | 1 | · | part |
| 7.3 | Line Drive VFD | deck-panel-rollformer-vfd | 1× | 1 | · | part |
| 7.4 | Power Supply | power-supply | 1× | 1 | · | part |
| 7.5 | Relay | relay | 8× | 8 | · | part |
| 7.6 | Connector | connector | 6× | 6 | · | part |
| 7.7 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 7.8 | Emergency Stop Button | deck-panel-rollformer-estop | 2× | 2 | · | part |
| 8 | Centralized Lubrication Unit 5 parts | deck-panel-rollformer-lubrication | 1× | 1 | 8 | assembly |
| 8.1 | Lubrication Pump | deck-panel-rollformer-lube-pump | 1× | 1 | · | part |
| 8.2 | Lubricant Reservoir | deck-panel-rollformer-lube-reservoir | 1× | 1 | · | part |
| 8.3 | Progressive Metering Block | deck-panel-rollformer-metering-block | 4× | 4 | · | part |
| 8.4 | Distribution Tubing Set | deck-panel-rollformer-lube-line | 1× | 1 | · | part |
| 8.5 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 9 | Baseplate and Frame 5 parts | deck-panel-rollformer-mainframe | 1× | 1 | 18 | assembly |
| 9.1 | Longitudinal Base Rail | deck-panel-rollformer-base-rail | 2× | 2 | · | part |
| 9.2 | Cross Member | deck-panel-rollformer-cross-member | 6× | 6 | · | part |
| 9.3 | Levelling Foot | deck-panel-rollformer-levelling-foot | 8× | 8 | · | part |
| 9.4 | Perimeter Guard Rail | deck-panel-rollformer-guard-rail | 1× | 1 | · | part |
| 9.5 | Fastener Set | fastener-set | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Bed-Type Milling Machine
151 parts · shares 4 with this page
 Bevel Gear Generator
201 parts · shares 4 with this page
Centering and Facing Machine
1,419 parts · shares 4 with this page
Cold Rolling Mill
991 parts · shares 4 with this page
 Creep-Feed Grinder
571 parts · shares 4 with this page
Cut-to-Length Line
500 parts · shares 4 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
1,047-word article