Aluminum Extrusion Press
ProductOverview
An aluminium extrusion press shapes long profiles by pushing a softened, heated billet through a steel die, the way toothpaste takes the shape of the tube opening. The aluminium is not melted: it is heated to around 450 degrees C, where it flows under pressure but stays solid. A hydraulic ram drives the billet, held in a heated Container, against the Die Stack, and the metal squeezes through the die aperture as a continuous profile of that cross-section. Almost every aluminium window frame, heat sink, ladder rail, and structural channel is made this way. The Main Cylinder supplies the force, the Platen Frame carries it, the Billet Loader feeds each log, the Butt Shear crops the discard, and the Run-Out Table cools and straightens the result, all under the Press Control and powered by the Hydraulic System.
Frame and force loop
Extrusion needs thousands of tonnes of steady push, so the press is built as a closed load loop. The Front Platen holds the die and the Cylinder Platen holds the main cylinder; four Tie Rod rods pre-tensioned by Tie Rod Nut nuts tie them together so the force circulates inside the frame rather than into the foundation. The Moving Crosshead carries the stem and rides the tie rods as it advances. Pretension matters: it keeps the rods always in tension so they never see the fatigue of load reversal.
The main cylinder
The Main Cylinder turns oil pressure into ram force. Its Cylinder Body is a forged bore that holds the Main Ram, sealed by a stack of High-Pressure Packing. The ram pushes the Extrusion Stem, a hardened nose that bears on the billet through the Dummy Block. That dummy block is a sacrificial disc the diameter of the container bore: it wipes the bore clean on each stroke and is left behind with the discard butt when the cycle ends. Force is the product of oil pressure and ram area, which is why these cylinders are so large; a 4,000-tonne press runs a ram close to a metre across.
Container and die
The Container is a heated cylinder that holds the billet during upset and extrusion. Its hardened Container Liner is shrink-fitted inside a Container Mantle that pre-stresses it against the internal pressure, and Container Heater elements with Container Thermocouple feedback hold it at temperature so the billet does not chill at the wall. A Container Shift Cylinder cylinder seals the container against the die and opens it to clear the butt.
Shape comes from the Die Stack. The Profile Die carries the profile aperture; behind it a Backer and Bolster spread the bending load into the platen, all held in a Die Ring cartridge. Because dies change often, a Die Slide driven by a Slide Cylinder shuttles cartridges in and out and a Die Clamp seats the chosen die against the platen.
The extrusion cycle
The Billet Loader takes a hot log from the furnace on its Billet Cradle, a Billet Lubricator coats the end, and the Loader Arm raises it to the container bore. The ram advances, upsets the billet to fill the bore, then pushes it through the die. As profile emerges, the Profile Puller grips the nose and tracks it down the run-out to keep tension steady and stop it whipping. When the billet is nearly spent, the press stops short to leave a discard butt, the Butt Shear drives its Shear Blade across the die face to crop the profile free, and the container opens to eject the butt with the dummy block. A new billet loads and the cycle repeats.
Cooling, stretching, and control
Fresh profile leaves the die soft and must be cooled at a controlled rate to set its temper. The Run-Out Table carries it on a Run-Out Belt through the Quench Section where Cooling Fan fans or water spray solidify the alloy structure. Cooling leaves the profile with twist and slight bow, so the Stretcher grips both ends in Stretch Head jaws and pulls it straight with a Stretch Cylinder. The Press Control runs the cycle through its Press PLC, whose isokinetic speed loop reads Ram Position Sensor feedback and slows the ram as the die heats so exit temperature stays constant. A Temperature Controller manages container and die heat, and the operator sets recipes at the Operator HMI. The high pressure comes from the Hydraulic System, where Main Pump pumps feed a Prefill Valve for fast approach, an Accumulator supplies peak flow at breakthrough, and an Oil Cooler sheds the heat of work. Die steel and the container liner are the main wear items because they run hot under abrasive metal flow, and a press of this kind feeds the building, transport, and electronics industries with the bulk of their aluminium sections.
Aluminum Extrusion Press parts and their functions
9 top-level parts · 365 parts in total · full bill of materials below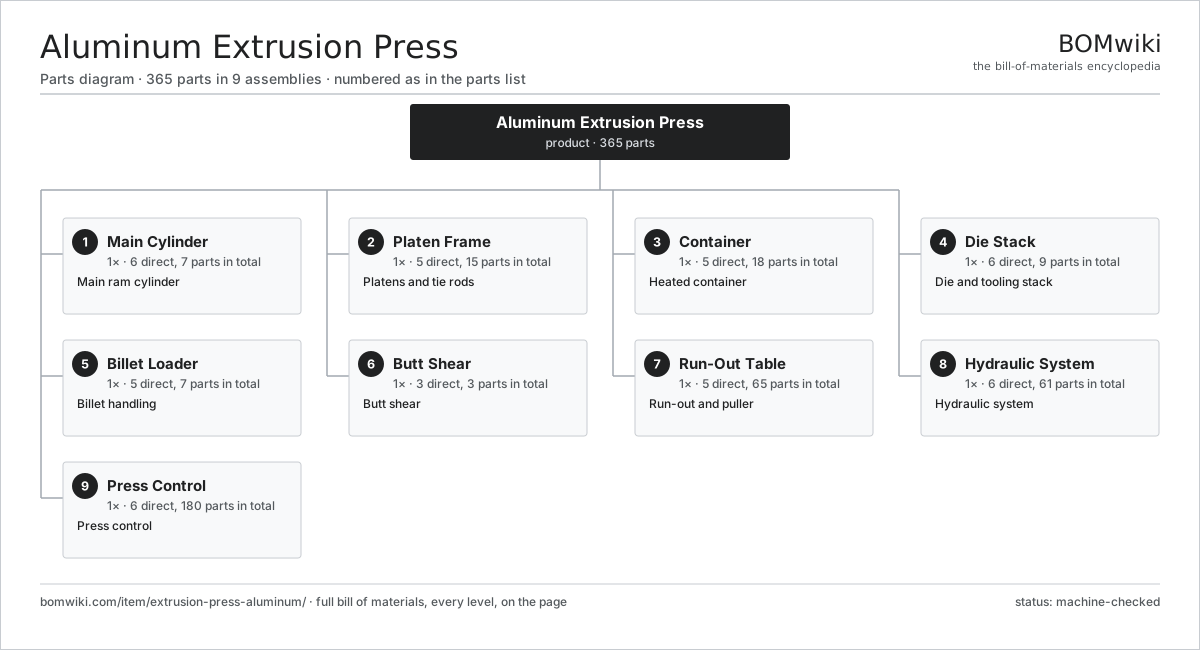
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Main Cylinder 6 parts | 1× | Main ram cylinder |
| 2 | Platen Frame 5 parts | 1× | Platens and tie rods |
| 3 | Container 5 parts | 1× | Heated container |
| 4 | Die Stack 6 parts | 1× | Die and tooling stack |
| 5 | Billet Loader 5 parts | 1× | Billet handling |
| 6 | Butt Shear 3 parts | 1× | Butt shear |
| 7 | Run-Out Table 5 parts | 1× | Run-out and puller |
| 8 | Hydraulic System 6 parts | 1× | Hydraulic system |
| 9 | Press Control 6 parts | 1× | Press control |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Aluminum Extrusion Press
9 top-level lines · 78 rows shown · 365 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Main Cylinder 6 parts | extrusion-press-aluminum-main-cylinder | 1× | 1 | 7 | assembly |
| 1.1 | Cylinder Body | extrusion-press-aluminum-cylinder-body | 1× | 1 | · | part |
| 1.2 | Main Ram | extrusion-press-aluminum-main-ram | 1× | 1 | · | part |
| 1.3 | Extrusion Stem | extrusion-press-aluminum-stem | 1× | 1 | · | part |
| 1.4 | Dummy Block | extrusion-press-aluminum-dummy-block | 1× | 1 | · | part |
| 1.5 | High-Pressure Packing | extrusion-press-aluminum-cylinder-packing | 1× | 1 | · | part |
| 1.6 | O-Ring Set | oring-set | 2× | 2 | · | part |
| 2 | Platen Frame 5 parts | extrusion-press-aluminum-platen-frame | 1× | 1 | 15 | assembly |
| 2.1 | Front Platen | extrusion-press-aluminum-front-platen | 1× | 1 | · | part |
| 2.2 | Cylinder Platen | extrusion-press-aluminum-cylinder-platen | 1× | 1 | · | part |
| 2.3 | Moving Crosshead | extrusion-press-aluminum-moving-crosshead | 1× | 1 | · | part |
| 2.4 | Tie Rod | extrusion-press-aluminum-tie-rod | 4× | 4 | · | part |
| 2.5 | Tie Rod Nut | extrusion-press-aluminum-tie-rod-nut | 8× | 8 | · | part |
| 3 | Container 5 parts | extrusion-press-aluminum-container | 1× | 1 | 18 | assembly |
| 3.1 | Container Liner | extrusion-press-aluminum-container-liner | 1× | 1 | · | part |
| 3.2 | Container Mantle | extrusion-press-aluminum-container-mantle | 1× | 1 | · | part |
| 3.3 | Container Heater 2 parts | extrusion-press-aluminum-container-heater | 1× | 1 | 12 | assembly |
| 3.3.1 | Heating Element | heating-element | 6× | 6 | · | part |
| 3.3.2 | Connector | connector | 6× | 6 | · | part |
| 3.4 | Container Shift Cylinder | extrusion-press-aluminum-container-shift | 1× | 1 | · | part |
| 3.5 | Container Thermocouple | extrusion-press-aluminum-container-thermocouple | 3× | 3 | · | part |
| 4 | Die Stack 6 parts | extrusion-press-aluminum-die-stack | 1× | 1 | 9 | assembly |
| 4.1 | Profile Die | extrusion-press-aluminum-die | 1× | 1 | · | part |
| 4.2 | Backer | extrusion-press-aluminum-backer | 1× | 1 | · | part |
| 4.3 | Bolster | extrusion-press-aluminum-bolster | 1× | 1 | · | part |
| 4.4 | Die Ring | extrusion-press-aluminum-die-ring | 1× | 1 | · | part |
| 4.5 | Die Slide 3 parts | extrusion-press-aluminum-die-slide | 1× | 1 | 4 | assembly |
| 4.5.1 | Slide Cylinder | extrusion-press-aluminum-slide-cylinder | 1× | 1 | · | part |
| 4.5.2 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 4.5.3 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 4.6 | Die Clamp | extrusion-press-aluminum-die-clamp | 1× | 1 | · | part |
| 5 | Billet Loader 5 parts | extrusion-press-aluminum-billet-loader | 1× | 1 | 7 | assembly |
| 5.1 | Billet Cradle | extrusion-press-aluminum-billet-cradle | 1× | 1 | · | part |
| 5.2 | Loader Arm | extrusion-press-aluminum-loader-arm | 1× | 1 | · | part |
| 5.3 | Billet Lubricator | extrusion-press-aluminum-billet-lube | 1× | 1 | · | part |
| 5.4 | Loader Cylinder | extrusion-press-aluminum-loader-cylinder | 2× | 2 | · | part |
| 5.5 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 6 | Butt Shear 3 parts | extrusion-press-aluminum-shear | 1× | 1 | 3 | assembly |
| 6.1 | Shear Blade | extrusion-press-aluminum-shear-blade | 1× | 1 | · | part |
| 6.2 | Shear Cylinder | extrusion-press-aluminum-shear-cylinder | 1× | 1 | · | part |
| 6.3 | Shear Guide | extrusion-press-aluminum-shear-guide | 1× | 1 | · | part |
| 7 | Run-Out Table 5 parts | extrusion-press-aluminum-runout | 1× | 1 | 65 | assembly |
| 7.1 | Run-Out Belt 3 parts | extrusion-press-aluminum-runout-belt | 1× | 1 | 30 | assembly |
| 7.1.1 | Drive Belt | drive-belt | 2× | 2 | · | part |
| 7.1.2 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 7.1.3 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 7.2 | Profile Puller 3 parts | extrusion-press-aluminum-puller | 1× | 1 | 27 | assembly |
| 7.2.1 | Puller Jaw | extrusion-press-aluminum-puller-jaw | 1× | 1 | · | part |
| 7.2.2 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 7.2.3 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 7.3 | Quench Section | extrusion-press-aluminum-quench | 1× | 1 | · | part |
| 7.4 | Stretcher 2 parts | extrusion-press-aluminum-stretcher | 1× | 1 | 3 | assembly |
| 7.4.1 | Stretch Head | extrusion-press-aluminum-stretch-head | 2× | 2 | · | part |
| 7.4.2 | Stretch Cylinder | extrusion-press-aluminum-stretch-cylinder | 1× | 1 | · | part |
| 7.5 | Cooling Fan | extrusion-press-aluminum-cooling-fan | 4× | 4 | · | part |
| 8 | Hydraulic System 6 parts | extrusion-press-aluminum-hydraulics | 1× | 1 | 61 | assembly |
| 8.1 | Main Pump 3 parts | extrusion-press-aluminum-main-pump | 2× | 2 | 27 | assembly |
| 8.1.1 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 2 | 24 | assembly |
| 8.1.2 | Pump Cartridge | extrusion-press-aluminum-pump-cartridge | 1× | 2 | · | part |
| 8.1.3 | Oil Seal | oil-seal | 2× | 4 | · | part |
| 8.2 | Oil Tank | extrusion-press-aluminum-oil-tank | 1× | 1 | · | part |
| 8.3 | Prefill Valve | extrusion-press-aluminum-prefill-valve | 1× | 1 | · | part |
| 8.4 | Accumulator | extrusion-press-aluminum-accumulator | 1× | 1 | · | part |
| 8.5 | Oil Cooler | extrusion-press-aluminum-oil-cooler | 1× | 1 | · | part |
| 8.6 | Pressure Sensor | pressure-sensor | 3× | 3 | · | part |
| 9 | Press Control 6 parts | extrusion-press-aluminum-control | 1× | 1 | 180 | assembly |
| 9.1 | Press PLC 3 parts | extrusion-press-aluminum-plc | 1× | 1 | 163 | assembly |
| 9.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 9.1.2 | Microcontroller | mcu | 2× | 2 | · | part |
| 9.1.3 | SMD Passive (R/C/L) | smd-passives | 160× | 160 | · | part |
| 9.2 | Temperature Controller | extrusion-press-aluminum-temp-controller | 1× | 1 | · | part |
| 9.3 | Operator HMI 3 parts | extrusion-press-aluminum-hmi | 1× | 1 | 3 | assembly |
| 9.3.1 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 9.3.2 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 9.3.3 | Microcontroller | mcu | 1× | 1 | · | part |
| 9.4 | Ram Position Sensor | extrusion-press-aluminum-position-sensor | 2× | 2 | · | part |
| 9.5 | Relay | relay | 10× | 10 | · | part |
| 9.6 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Crankshaft Grinder
511 parts · shares 6 with this page
 Rotary-Table Surface Grinder
172 parts · shares 6 with this page
 Heat Treatment Furnace
299 parts · shares 5 with this page
 Profile Grinding Machine
815 parts · shares 4 with this page
 Nitriding Furnace
105 parts · shares 4 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
960-word article