Oxy-Fuel Cutting Machine
ProductOverview
An oxy-fuel cutting machine severs thick steel plate by burning a narrow line through it with a high-temperature flame and a jet of pure oxygen. It is the oldest of the thermal cutting processes and still the cheapest way to cut carbon steel above roughly 25 mm, where plasma and laser lose their edge on cost. On a machine of this kind the torch does not move by hand. A motor-driven Gantry Bridge spans the plate and carries a Cross Carriage across it, so the Cutting Torch follows a programmed path while the CNC Controller runs the axes, the gases, and the standoff. The result is a repeatable cut on heavy plate that would be slow and inaccurate to mark and burn by hand.
The plate rests on a Cutting Table while a Gas Console feeds oxygen and fuel through Torch Station lifters. Power and gas reach the moving parts through Cable Management drag chains. Most machines mount more than one torch so several copies of a part can be cut in one pass.
How oxy-fuel cutting works
Oxy-fuel cutting relies on a chemical fact: iron burns in pure oxygen once it is hot enough. The Cutting Torch first lights a preheat flame from oxygen and a fuel gas, either acetylene for speed or propane for cost and safety, mixed in the Gas Mixer and metered by the Preheat Valve needles. That flame heats a spot on the plate to about 900 C, its ignition point. The operator or program then opens the Cutting-Oxygen Valve and a high-flow jet of cutting oxygen streams down the centre bore of the Cutting Tip. The hot steel oxidizes rapidly in that jet, the reaction itself adds heat, and the jet blows the molten iron oxide out of the bottom of the cut as slag. The flame only preheats; the cutting oxygen does the work, which is why its purity matters and why a tip is sized to plate thickness. Thin plate uses a small tip and low pressure, while 200 mm plate needs a large bore and a long, coherent oxygen stream.
Gantry and motion
The machine moves the torch in two axes over the plate. The long axis runs the Gantry Bridge down the length of the table on two Running Rail tracks. Each Drive Side Housing carries a Servo Motor through a Gearbox Housing and Helical Gear Pair to a Drive Pinion that climbs a Drive Rack beside the rail. Driving both sides keeps a wide gantry square, and a Squaring Cross-Shaft ties the two together so they cannot drift out of line. The End Truck at each beam end rides the rail on guide wheels. The cross axis moves the Cross Carriage along the Gantry Beam on Linear Guide Rail bearings, again with a Servo Motor and a rack and pinion. Together the two axes place the torch anywhere over the plate, and the CNC Controller coordinates them to trace straight lines, arcs, and full part outlines.
Torch lifter and height control
Cut quality depends on holding the tip a small, steady distance above the plate, so each Torch Station has its own vertical axis. The Z Lifter uses a Ball Screw turned by a Servo Motor on a Linear Guide Rail to raise and lower the Torch Holder. A Height Sensor, capacitive or ohmic, reads the gap to the plate so the lifter can hold standoff as the plate warps from heat. The sequence at each pierce is deliberate: lower to the plate, preheat, raise slightly, open cutting oxygen to pierce through, then drop to cutting height and move. If the torch hits a tipped offcut, the Breakaway Mount mount releases and trips a stop so the torch is not bent.
Gas console and safety
The Gas Console conditions and switches the gases. An Oxygen Regulator and an Fuel Regulator drop supply pressure to safe working values, with Pressure Sensor feedback so the control can confirm the lines are ready before it lights a flame. The Solenoid Valve Bank holds the Oxygen Solenoid, Fuel Solenoid, and the high-flow Cutting-Oxygen Solenoid that the program pulses for each pierce. A Spark Igniter lights the preheat without a hand torch. Because fuel gas and oxygen can flash back up a hose, a Flashback Arrestor arrestor sits in each line to stop a flame or reverse flow from reaching the supply. Acetylene in particular is limited to low pressure for this reason, and the console enforces that limit.
Cutting table and fume control
The plate sits on a Cutting Table built from rows of Support Slat bars set in a Table Frame. The slats hold the plate up while leaving gaps for slag and the oxygen jet to pass through, and because the cut burns into them they are consumable and replaced when worn. Flame cutting throws a heavy plume of iron-oxide fume, so the table is a downdraft design. A Fume Blower pulls air down through the bed, and a set of Zone Damper flaps open suction only under the section of table the gantry is over, so all the airflow is spent on the live cut. Slag and small offcuts drop into Slag Pan drawers that pull out for emptying.
Controls and use
The CNC Controller turns a nested drawing into motion and gas timing. Its Controller Board runs the path with kerf offset so the cut lands on the part line, an LCD Panel shows the operator the nest and status, Drive Amplifier amplifiers drive the servos, and an I/O Board switches the solenoids, igniter, and dampers. Oxy-fuel works only on carbon and low-alloy steel, since the cut depends on the metal burning in oxygen, so stainless and aluminium need plasma or another process. Within that limit it is hard to beat on thick plate: the equipment is simple, the gases are cheap, several torches cut at once, and a clean cut on 50 to 150 mm steel comes off square and ready for the next operation.
Oxy-Fuel Cutting Machine parts and their functions
9 top-level parts · 343 parts in total · full bill of materials below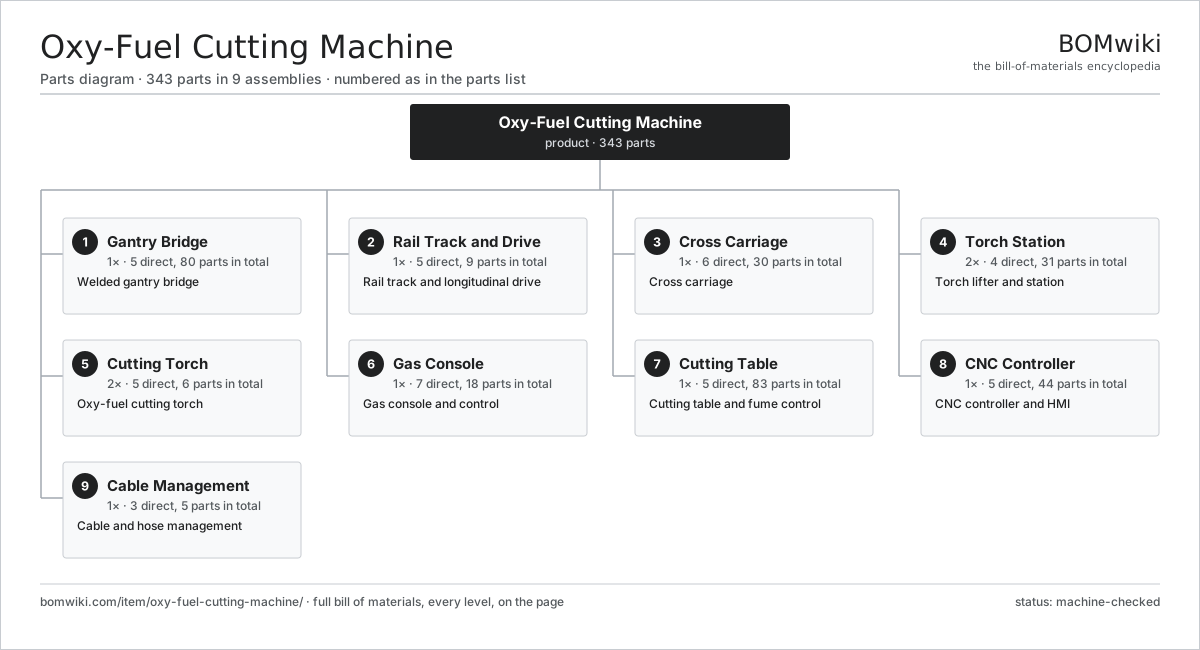
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Gantry Bridge 5 parts | 1× | Welded gantry bridge |
| 2 | Rail Track and Drive 5 parts | 1× | Rail track and longitudinal drive |
| 3 | Cross Carriage 6 parts | 1× | Cross carriage |
| 4 | Torch Station 4 parts | 2× | Torch lifter and station |
| 5 | Cutting Torch 5 parts | 2× | Oxy-fuel cutting torch |
| 6 | Gas Console 7 parts | 1× | Gas console and control |
| 7 | Cutting Table 5 parts | 1× | Cutting table and fume control |
| 8 | CNC Controller 5 parts | 1× | CNC controller and HMI |
| 9 | Cable Management 3 parts | 1× | Cable and hose management |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Oxy-Fuel Cutting Machine
9 top-level lines · 93 rows shown · 343 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Gantry Bridge 5 parts | oxy-fuel-cutting-machine-gantry | 1× | 1 | 80 | assembly |
| 1.1 | Gantry Beam | oxy-fuel-cutting-machine-gantry-beam | 1× | 1 | · | part |
| 1.2 | End Truck 3 parts | oxy-fuel-cutting-machine-end-truck | 2× | 2 | 9 | assembly |
| 1.2.1 | Truck Frame | oxy-fuel-cutting-machine-truck-frame | 1× | 2 | · | part |
| 1.2.2 | Guide Wheel | oxy-fuel-cutting-machine-guide-wheel | 4× | 8 | · | part |
| 1.2.3 | Ball Bearing | ball-bearing | 4× | 8 | · | part |
| 1.3 | Drive Side Housing 5 parts | oxy-fuel-cutting-machine-drive-side | 2× | 2 | 29 | assembly |
| 1.3.1 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 2 | 24 | assembly |
| 1.3.2 | Gearbox Housing | gearbox-housing | 1× | 2 | · | part |
| 1.3.3 | Helical Gear Pair | gear-pair | 1× | 2 | · | part |
| 1.3.4 | Drive Pinion | oxy-fuel-cutting-machine-drive-pinion | 1× | 2 | · | part |
| 1.3.5 | Ball Bearing | ball-bearing | 2× | 4 | · | part |
| 1.4 | Squaring Cross-Shaft | oxy-fuel-cutting-machine-square-link | 1× | 1 | · | part |
| 1.5 | Fastener Set | fastener-set | 2× | 2 | · | part |
| 2 | Rail Track and Drive 5 parts | oxy-fuel-cutting-machine-rail-drive | 1× | 1 | 9 | assembly |
| 2.1 | Running Rail | oxy-fuel-cutting-machine-rail | 2× | 2 | · | part |
| 2.2 | Drive Rack | oxy-fuel-cutting-machine-rack | 2× | 2 | · | part |
| 2.3 | Rail Anchor | oxy-fuel-cutting-machine-rail-anchor | 1× | 1 | · | part |
| 2.4 | Home Switch | oxy-fuel-cutting-machine-home-switch | 2× | 2 | · | part |
| 2.5 | Fastener Set | fastener-set | 2× | 2 | · | part |
| 3 | Cross Carriage 6 parts | oxy-fuel-cutting-machine-carriage | 1× | 1 | 30 | assembly |
| 3.1 | Carriage Frame | oxy-fuel-cutting-machine-carriage-frame | 1× | 1 | · | part |
| 3.2 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 3.3 | Cross-Axis Rack | oxy-fuel-cutting-machine-carriage-rack | 1× | 1 | · | part |
| 3.4 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 3.4.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 3.4.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 3.4.3 | Encoder | encoder | 1× | 1 | · | part |
| 3.4.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 3.5 | Helical Gear Pair | gear-pair | 1× | 1 | · | part |
| 3.6 | Cross-Axis Pinion | oxy-fuel-cutting-machine-carriage-pinion | 1× | 1 | · | part |
| 4 | Torch Station 4 parts | oxy-fuel-cutting-machine-torch-station | 2× | 2 | 31 | assembly |
| 4.1 | Z Lifter 4 parts | oxy-fuel-cutting-machine-lifter | 1× | 2 | 28 | assembly |
| 4.1.1 | Ball Screw | ball-screw | 1× | 2 | · | part |
| 4.1.2 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 2 | 24 | assembly |
| 4.1.3 | Linear Guide Rail | linear-guide | 1× | 2 | · | part |
| 4.1.4 | Ball Bearing | ball-bearing | 2× | 4 | · | part |
| 4.2 | Torch Holder | oxy-fuel-cutting-machine-torch-holder | 1× | 2 | · | part |
| 4.3 | Height Sensor | oxy-fuel-cutting-machine-height-sensor | 1× | 2 | · | part |
| 4.4 | Breakaway Mount | oxy-fuel-cutting-machine-breakaway | 1× | 2 | · | part |
| 5 | Cutting Torch 5 parts | oxy-fuel-cutting-machine-torch | 2× | 2 | 6 | assembly |
| 5.1 | Torch Body | oxy-fuel-cutting-machine-torch-body | 1× | 2 | · | part |
| 5.2 | Gas Mixer | oxy-fuel-cutting-machine-mixer | 1× | 2 | · | part |
| 5.3 | Cutting Tip | oxy-fuel-cutting-machine-tip | 1× | 2 | · | part |
| 5.4 | Preheat Valve | oxy-fuel-cutting-machine-preheat-valve | 2× | 4 | · | part |
| 5.5 | Cutting-Oxygen Valve | oxy-fuel-cutting-machine-cut-valve | 1× | 2 | · | part |
| 6 | Gas Console 7 parts | oxy-fuel-cutting-machine-gas-console | 1× | 1 | 18 | assembly |
| 6.1 | Oxygen Regulator | oxy-fuel-cutting-machine-oxy-regulator | 1× | 1 | · | part |
| 6.2 | Fuel Regulator | oxy-fuel-cutting-machine-fuel-regulator | 1× | 1 | · | part |
| 6.3 | Solenoid Valve Bank 4 parts | oxy-fuel-cutting-machine-solenoid-bank | 1× | 1 | 7 | assembly |
| 6.3.1 | Oxygen Solenoid | oxy-fuel-cutting-machine-oxy-solenoid | 1× | 1 | · | part |
| 6.3.2 | Fuel Solenoid | oxy-fuel-cutting-machine-fuel-solenoid | 1× | 1 | · | part |
| 6.3.3 | Cutting-Oxygen Solenoid | oxy-fuel-cutting-machine-cut-solenoid | 1× | 1 | · | part |
| 6.3.4 | Connector | connector | 4× | 4 | · | part |
| 6.4 | Flashback Arrestor | oxy-fuel-cutting-machine-flashback | 2× | 2 | · | part |
| 6.5 | Spark Igniter | oxy-fuel-cutting-machine-igniter | 1× | 1 | · | part |
| 6.6 | Gas Hose | oxy-fuel-cutting-machine-gas-hose | 4× | 4 | · | part |
| 6.7 | Pressure Sensor | pressure-sensor | 2× | 2 | · | part |
| 7 | Cutting Table 5 parts | oxy-fuel-cutting-machine-table | 1× | 1 | 83 | assembly |
| 7.1 | Table Frame | oxy-fuel-cutting-machine-table-frame | 1× | 1 | · | part |
| 7.2 | Support Slat | oxy-fuel-cutting-machine-slat | 40× | 40 | · | part |
| 7.3 | Zone Damper 3 parts | oxy-fuel-cutting-machine-zone-damper | 4× | 4 | 3 | assembly |
| 7.3.1 | Damper Flap | oxy-fuel-cutting-machine-damper-flap | 1× | 4 | · | part |
| 7.3.2 | Damper Actuator | oxy-fuel-cutting-machine-damper-actuator | 1× | 4 | · | part |
| 7.3.3 | Coil Spring | coil-spring | 1× | 4 | · | part |
| 7.4 | Fume Blower 5 parts | oxy-fuel-cutting-machine-fume-blower | 1× | 1 | 26 | assembly |
| 7.4.1 | Blower Housing | oxy-fuel-cutting-machine-blower-housing | 1× | 1 | · | part |
| 7.4.2 | Impeller | oxy-fuel-cutting-machine-impeller | 1× | 1 | · | part |
| 7.4.3 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 7.4.4 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 7.4.5 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 7.5 | Slag Pan | oxy-fuel-cutting-machine-slag-pan | 4× | 4 | · | part |
| 8 | CNC Controller 5 parts | oxy-fuel-cutting-machine-cnc | 1× | 1 | 44 | assembly |
| 8.1 | Controller Board 4 parts | oxy-fuel-cutting-machine-controller-board | 1× | 1 | 9 | assembly |
| 8.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.1.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 8.1.3 | SMD Passive (R/C/L) | smd-passives | 1× | 1 | · | part |
| 8.1.4 | Connector | connector | 6× | 6 | · | part |
| 8.2 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 8.3 | Drive Amplifier 3 parts | oxy-fuel-cutting-machine-drive-amp | 3× | 3 | 5 | assembly |
| 8.3.1 | Bare PCB | pcb-bare | 1× | 3 | · | part |
| 8.3.2 | SMD Passive (R/C/L) | smd-passives | 1× | 3 | · | part |
| 8.3.3 | Connector | connector | 3× | 9 | · | part |
| 8.4 | I/O Board 4 parts | oxy-fuel-cutting-machine-io-board | 1× | 1 | 18 | assembly |
| 8.4.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.4.2 | Relay | relay | 8× | 8 | · | part |
| 8.4.3 | SMD Passive (R/C/L) | smd-passives | 1× | 1 | · | part |
| 8.4.4 | Connector | connector | 8× | 8 | · | part |
| 8.5 | Power Supply | power-supply | 1× | 1 | · | part |
| 9 | Cable Management 3 parts | oxy-fuel-cutting-machine-cable-mgmt | 1× | 1 | 5 | assembly |
| 9.1 | Drag Chain | oxy-fuel-cutting-machine-drag-chain | 2× | 2 | · | part |
| 9.2 | Wire Bundle | wire-bundle | 2× | 2 | · | part |
| 9.3 | Hose Carrier | oxy-fuel-cutting-machine-hose-carrier | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Bevel Gear Generator
201 parts · shares 7 with this page
Centering and Facing Machine
1,419 parts · shares 7 with this page
 Creep-Feed Grinder
571 parts · shares 7 with this page
 Radial Forging Machine
288 parts · shares 7 with this page
 Railway Wheel Lathe
1,201 parts · shares 7 with this page
 Rotary Draw Bender
821 parts · shares 7 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
1,171-word article