Turret Lathe
ProductOverview
A turret lathe is built for repetition. Where an engine lathe relies on the operator to mount and set each tool by hand, a turret lathe carries a row of tools preset on an indexing turret so they can be brought to the work one after another in a fixed sequence. Once the machine is tooled and the stops are set, an operator can turn out identical parts quickly by indexing through the sequence, with much of the skill moved from running each cut into the initial setup. This made the turret lathe the workhorse of small and medium production for decades, especially for parts made from bar stock such as fittings, bushings, studs, and valve bodies.
The machine shares its foundation with an engine lathe: a Bed & Ways with hardened ways, a Geared Headstock driving the spindle, and a Cross Slide. What sets it apart is the Hexagonal Turret on the saddle, the Square Turret on the cross slide, and the Turret Stops & Trips that make every cut land at the same length.
Headstock and workholding
The Geared Headstock drives a hollow Work Spindle with a large bore so bar stock can pass through and be fed forward between parts. A Main Drive Motor turns it through a Speed Gearbox. Most production work uses the Collet Chuck rather than a jaw chuck: a Draw Tube pulls a spring Spring Collet into a taper, gripping the bar concentrically in a fraction of a second, which keeps load and unload time low. A Collet Closer works the collet by lever or air.
The hexagonal turret
The Hexagonal Turret is the heart of the machine. Its six-faced Turret Head rides the bed on the Turret Saddle, and each face is bored to hold a Turret Tool Holder: a drill, a reamer, a boring bar, a die head, or a box tool. The operator feeds the turret toward the work to make a cut, then withdraws it. On withdrawal the Indexing Mechanism automatically rotates the head to the next station and locks it. A Geneva Cam gives the intermittent rotation and a spring Index Plunger seats each face precisely, so the next tool comes up in exactly the same position every cycle.
Square turret and cross slide
The Cross Slide carries the Square Turret, a four-station turret holding turning and facing tools that work on the diameter while the hex turret works on the end and bore. A Rear Tool Post on the back of the cross slide usually holds a parting blade to cut the finished part off the bar. With tools on both turrets, several operations can overlap, the square turret turning an outside diameter while the hex turret drills the center, which is where the turret lathe gains its speed.
Stops, trips, and repeatability
Repeatability comes from the Turret Stops & Trips. A rotating Stop Drum carries one Length Stop Screw per turret station, each a micrometer screw set to the exact depth that station should reach. When the turret advances to its stop a Feed Trip disengages the feed, so the hole depth or shoulder position is the same on every part without the operator watching a dial. Setting these stops is the main skill in running the machine, and once set the cycle is largely mechanical.
Feeds, auxiliaries, and use
A Feed Train drives the turret saddle and cross slide at selected feed rates through a Feed Gearbox and Feed Rod. A Lubrication System system oils the headstock and slides, a Coolant System system floods the cut, and the Electrical Control cabinet houses the motor starters and an operator Operator Pendant. Castings are gray iron, ways and spindle are hardened, and the turret index parts are hardened and ground for long life. The Geneva cam and the index plunger seat take the most wear, so they are made oversize and replaceable, because the whole value of the machine depends on each tool returning to exactly the same place.
The turret lathe suits batch production of turned parts from bar or chucked blanks, bridging the gap between the one-off work of an engine lathe and the high volume of an automatic screw machine. Once set up, it is run by a less experienced operator who simply indexes through the sequence and reloads bar, while the skilled work is the toolmaker's job of arranging the stations and setting the stops. Common products are pipe fittings, valve bodies, spacers, threaded studs, bushings, and hydraulic adapters, often made in runs of a few hundred to a few thousand where the setup time is paid back many times over. The combination of preset tooling on two turrets, fast collet loading, and per-station length stops is what lets one machine and one operator hold close tolerances across a whole batch without re-measuring each part.
Turret Lathe parts and their functions
12 top-level parts · 230 parts in total · full bill of materials below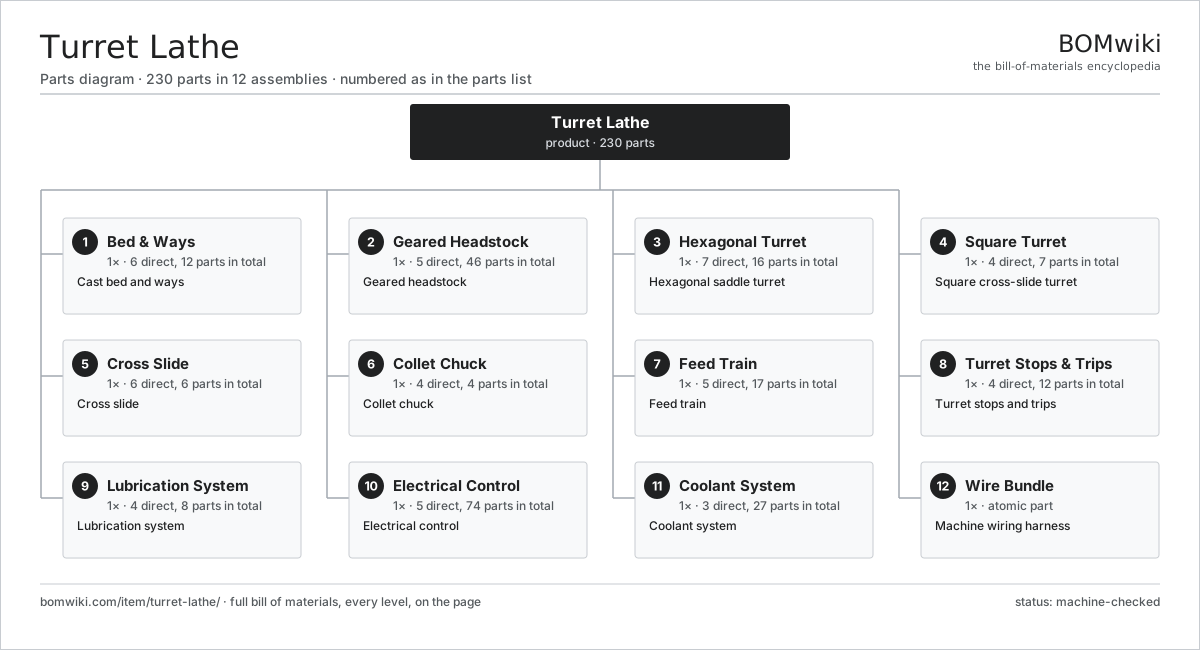
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Bed & Ways 6 parts | 1× | Cast bed and ways |
| 2 | Geared Headstock 5 parts | 1× | Geared headstock |
| 3 | Hexagonal Turret 7 parts | 1× | Hexagonal saddle turret |
| 4 | Square Turret 4 parts | 1× | Square cross-slide turret |
| 5 | Cross Slide 6 parts | 1× | Cross slide |
| 6 | Collet Chuck 4 parts | 1× | Collet chuck |
| 7 | Feed Train 5 parts | 1× | Feed train |
| 8 | Turret Stops & Trips 4 parts | 1× | Turret stops and trips |
| 9 | Lubrication System 4 parts | 1× | Lubrication system |
| 10 | Electrical Control 5 parts | 1× | Electrical control |
| 11 | Coolant System 3 parts | 1× | Coolant system |
| 12 | Wire Bundle | 1× | Machine wiring harness |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Turret Lathe
12 top-level lines · 88 rows shown · 230 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Bed & Ways 6 parts | turret-lathe-bed | 1× | 1 | 12 | assembly |
| 1.1 | Bed Casting | turret-lathe-bed-casting | 1× | 1 | · | part |
| 1.2 | Hardened V-Way | turret-lathe-v-way | 2× | 2 | · | part |
| 1.3 | Hardened Flat Way | turret-lathe-flat-way | 2× | 2 | · | part |
| 1.4 | Way Wiper | turret-lathe-way-wiper | 4× | 4 | · | part |
| 1.5 | Bed Leg & Foot | turret-lathe-bed-foot | 2× | 2 | · | part |
| 1.6 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 2 | Geared Headstock 5 parts | turret-lathe-headstock | 1× | 1 | 46 | assembly |
| 2.1 | Work Spindle | turret-lathe-spindle | 1× | 1 | · | part |
| 2.2 | Headstock Casting | turret-lathe-headstock-casting | 1× | 1 | · | part |
| 2.3 | Speed Gearbox 4 parts | turret-lathe-speed-gearbox | 1× | 1 | 16 | assembly |
| 2.3.1 | Helical Gear Pair | gear-pair | 6× | 6 | · | part |
| 2.3.2 | Shift Fork | turret-lathe-shift-fork | 3× | 3 | · | part |
| 2.3.3 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 2.3.4 | Ball Bearing | ball-bearing | 6× | 6 | · | part |
| 2.4 | Main Drive Motor 5 parts | turret-lathe-main-motor | 1× | 1 | 26 | assembly |
| 2.4.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 2.4.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 2.4.3 | Copper Winding | copper-winding | 1× | 1 | · | part |
| 2.4.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 2.4.5 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 2.5 | Spindle Bearing | turret-lathe-spindle-bearing | 2× | 2 | · | part |
| 3 | Hexagonal Turret 7 parts | turret-lathe-hex-turret | 1× | 1 | 16 | assembly |
| 3.1 | Turret Head | turret-lathe-turret-head | 1× | 1 | · | part |
| 3.2 | Turret Saddle | turret-lathe-turret-saddle | 1× | 1 | · | part |
| 3.3 | Indexing Mechanism 4 parts | turret-lathe-index-mechanism | 1× | 1 | 4 | assembly |
| 3.3.1 | Geneva Cam | turret-lathe-geneva-cam | 1× | 1 | · | part |
| 3.3.2 | Index Plunger | turret-lathe-index-plunger | 1× | 1 | · | part |
| 3.3.3 | Coil Spring | coil-spring | 1× | 1 | · | part |
| 3.3.4 | Helical Gear Pair | gear-pair | 1× | 1 | · | part |
| 3.4 | Turret Tool Holder | turret-lathe-turret-tool | 6× | 6 | · | part |
| 3.5 | Saddle Feed Screw | turret-lathe-saddle-screw | 1× | 1 | · | part |
| 3.6 | Saddle Handwheel | turret-lathe-saddle-handwheel | 1× | 1 | · | part |
| 3.7 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 4 | Square Turret 4 parts | turret-lathe-square-turret | 1× | 1 | 7 | assembly |
| 4.1 | Square Turret Body | turret-lathe-square-body | 1× | 1 | · | part |
| 4.2 | Square Index Plate | turret-lathe-square-index | 1× | 1 | · | part |
| 4.3 | Turning Tool | turret-lathe-turning-tool | 4× | 4 | · | part |
| 4.4 | Turret Clamp | turret-lathe-square-clamp | 1× | 1 | · | part |
| 5 | Cross Slide 6 parts | turret-lathe-cross-slide | 1× | 1 | 6 | assembly |
| 5.1 | Cross-Slide Casting | turret-lathe-cross-casting | 1× | 1 | · | part |
| 5.2 | Cross-Slide Screw | turret-lathe-cross-screw | 1× | 1 | · | part |
| 5.3 | Cross-Slide Nut | turret-lathe-cross-nut | 1× | 1 | · | part |
| 5.4 | Cross Handwheel | turret-lathe-cross-handwheel | 1× | 1 | · | part |
| 5.5 | Rear Tool Post | turret-lathe-rear-post | 1× | 1 | · | part |
| 5.6 | Cross-Slide Gib | turret-lathe-cross-gib | 1× | 1 | · | part |
| 6 | Collet Chuck 4 parts | turret-lathe-collet-chuck | 1× | 1 | 4 | assembly |
| 6.1 | Spring Collet | turret-lathe-collet | 1× | 1 | · | part |
| 6.2 | Draw Tube | turret-lathe-draw-tube | 1× | 1 | · | part |
| 6.3 | Collet Closer | turret-lathe-collet-closer | 1× | 1 | · | part |
| 6.4 | Chuck Nose | turret-lathe-chuck-nose | 1× | 1 | · | part |
| 7 | Feed Train 5 parts | turret-lathe-feed-train | 1× | 1 | 17 | assembly |
| 7.1 | Feed Gearbox 3 parts | turret-lathe-feed-gearbox | 1× | 1 | 9 | assembly |
| 7.1.1 | Helical Gear Pair | gear-pair | 4× | 4 | · | part |
| 7.1.2 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 7.1.3 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 7.2 | Feed Rod | turret-lathe-feed-rod | 1× | 1 | · | part |
| 7.3 | Helical Gear Pair | gear-pair | 3× | 3 | · | part |
| 7.4 | Feed Clutch | turret-lathe-feed-clutch | 2× | 2 | · | part |
| 7.5 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 8 | Turret Stops & Trips 4 parts | turret-lathe-stops | 1× | 1 | 12 | assembly |
| 8.1 | Stop Drum | turret-lathe-stop-drum | 1× | 1 | · | part |
| 8.2 | Length Stop Screw | turret-lathe-stop-screw | 6× | 6 | · | part |
| 8.3 | Trip Dog | turret-lathe-trip-dog | 4× | 4 | · | part |
| 8.4 | Feed Trip | turret-lathe-feed-trip | 1× | 1 | · | part |
| 9 | Lubrication System 4 parts | turret-lathe-lube | 1× | 1 | 8 | assembly |
| 9.1 | Lube Pump | turret-lathe-lube-pump | 1× | 1 | · | part |
| 9.2 | Metering Unit | turret-lathe-lube-meter | 5× | 5 | · | part |
| 9.3 | Distribution Tubing | turret-lathe-lube-line | 1× | 1 | · | part |
| 9.4 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 10 | Electrical Control 5 parts | turret-lathe-control | 1× | 1 | 74 | assembly |
| 10.1 | Control Board 3 parts | turret-lathe-control-board | 1× | 1 | 52 | assembly |
| 10.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 10.1.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 10.1.3 | SMD Passive (R/C/L) | smd-passives | 50× | 50 | · | part |
| 10.2 | Relay | relay | 8× | 8 | · | part |
| 10.3 | Connector | connector | 12× | 12 | · | part |
| 10.4 | Operator Pendant | turret-lathe-pendant | 1× | 1 | · | part |
| 10.5 | Control Enclosure | turret-lathe-control-enclosure | 1× | 1 | · | part |
| 11 | Coolant System 3 parts | turret-lathe-coolant | 1× | 1 | 27 | assembly |
| 11.1 | Coolant Pump 4 parts | turret-lathe-coolant-pump | 1× | 1 | 24 | assembly |
| 11.1.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 11.1.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 11.1.3 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 11.1.4 | Oil Seal | oil-seal | 1× | 1 | · | part |
| 11.2 | Coolant Tank | turret-lathe-coolant-tank | 1× | 1 | · | part |
| 11.3 | Coolant Nozzle | turret-lathe-coolant-nozzle | 2× | 2 | · | part |
| 12 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Bevel Gear Generator
201 parts · shares 4 with this page
 Capstan Lathe
197 parts · shares 4 with this page
Centering and Facing Machine
1,419 parts · shares 4 with this page
 Continuous Belt Furnace
130 parts · shares 4 with this page
 Creep-Feed Grinder
571 parts · shares 4 with this page
Forging Roll Machine
135 parts · shares 4 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
859-word article