Pipe Sizing Mill
ProductOverview
A pipe sizing mill is the last hot rolling step in a seamless or welded tube line. The tube arrives still glowing, somewhere between 850 and 1050 C, already close to its target outside diameter but not yet round or accurate enough to ship. The sizing mill passes it through a row of rolling stands that each take a small bite, and by the time the tube leaves the last stand its outside diameter holds to roughly half a percent and its cross section is a true circle. The mill does not change the wall thickness much. Its job is to set the outside diameter and the roundness, which is why the gauging head and the closed-loop control matter as much as the rolls themselves.
The line begins at the Entry Section, where driven rollers and pinch rolls catch the tube and push it into the first pass. It runs through a series of Sizing Stand units mounted on the Mill Bed, turned by the Drive Line. The Gauging Head reads the finished diameter, the Descale and Cooling System keeps scale off the tube and holds its temperature, and the Exit Run-Out Table carries the sized tube away. The Lubrication System feeds the bearings and gears, and the Control Cabinet runs the whole sequence.
How it works
Each stand carries two grooved rolls whose pass forms an oval slightly smaller than the tube coming in. The tube is squeezed in that one direction, then the next stand presents its pass turned 90 degrees and squeezes the other way. Over five to nine stands this back-and-forth working closes the section from a rough oval to a tight round and brings the outside diameter down in small steps. No single stand does much. The accuracy comes from many light passes rather than one heavy one, because a small reduction per stand keeps the tube from buckling or forming fins where the rolls meet.
The stands
The Sizing Stand is the working unit of the mill. A heavy Stand Frame holds two Sizing Roll assemblies, each a forged Roll Body carrying the Roll Groove that shapes the tube. The rolls turn on Roll Shaft shafts running in Roll Chock chocks on heavy Roll-Neck Bearing bearings that take the separating force. A Screw-Down Adjustment mechanism moves the upper chock to set the gap, and through it the finished diameter, using a self-locking Worm Gear and two Adjustment Screw screws. A Position Encoder reports the actual gap so the control knows where each stand is set, and a Guide Box aligns the tube into the pass.
Drive
Each stand has its own Stand Drive Motor, an AC motor with a Stator Assembly and Rotor Assembly and a Motor Encoder for speed feedback. The motor drives through a Coupling into a Reduction Gearbox built from a Gearbox Housing and Helical Gear Pair sets, and the torque reaches the roll shaft through a Drive Spindle with universal joints that let it follow the chock as the gap changes. Because the tube grows longer as it is reduced, every stand must run a little faster than the one before it. The Distribution Gearbox sets the base ratios, and the drives trim each speed so the tube neither piles up nor pulls tight between stands.
Gauging and control
The Gauging Head sits just past the last stand. Two Laser Scan Gauge heads scan the glowing tube edge to edge in two axes and report the diameter and the ovality many times a second. A Gauge Cooling Jacket jacket and a Air Purge keep the optics alive next to the hot tube. The Gauge Controller turns the scan into a number that the PLC compares with the target. If the tube drifts oversize or undersize, the PLC nudges the Screw-Down Adjustment screws on the finishing stands to bring it back, closing the loop on diameter while the mill runs. The Variable-Frequency Drive drives hold the stand speeds, and the operator sets the product and watches the trend on the Operator Touchscreen.
Materials and cooling
The rolls take heat, pressure, and abrasion at once, so the Roll Body is a forged alloy steel chosen to hold its hardness hot. The Descale and Cooling System runs a Descale Pump at 120 to 200 bar through a Water Manifold and rows of Spray Nozzle jets that shock the oxide scale off the tube before it can be rolled into the surface, with Pressure Sensor sensors watching the line. The same water and the Lubrication System hold the working temperatures down so the bearings and gears survive a continuous shift.
Use
Pipe sizing mills run at the finishing end of seamless and welded tube plants that make line pipe, boiler tube, mechanical tube, and structural sections. One mill covers a band of sizes by changing the rolls and resetting the screw-downs, so a plant can hold a wide product range without a separate machine for each diameter. The output feeds straight to the cooling bed, the straightener, and the cutoff, where the tube is finished to its shipping length.
Pipe Sizing Mill parts and their functions
9 top-level parts · 641 parts in total · full bill of materials below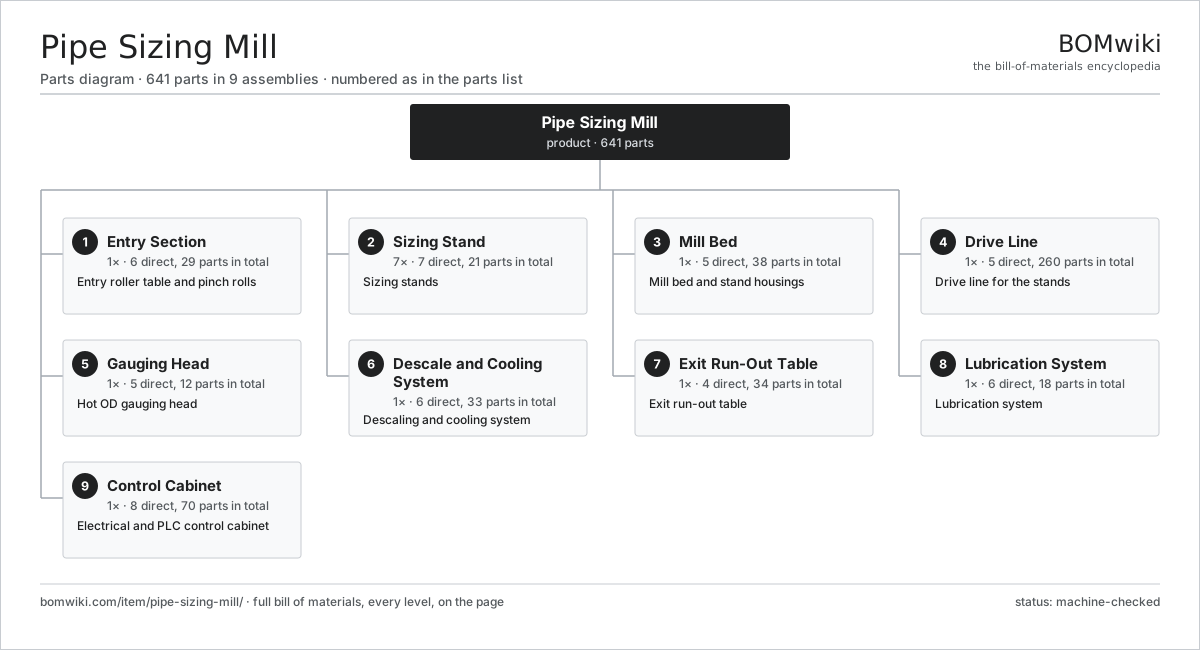
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Entry Section 6 parts | 1× | Entry roller table and pinch rolls |
| 2 | Sizing Stand 7 parts | 7× | Sizing stands |
| 3 | Mill Bed 5 parts | 1× | Mill bed and stand housings |
| 4 | Drive Line 5 parts | 1× | Drive line for the stands |
| 5 | Gauging Head 5 parts | 1× | Hot OD gauging head |
| 6 | Descale and Cooling System 6 parts | 1× | Descaling and cooling system |
| 7 | Exit Run-Out Table 4 parts | 1× | Exit run-out table |
| 8 | Lubrication System 6 parts | 1× | Lubrication system |
| 9 | Control Cabinet 8 parts | 1× | Electrical and PLC control cabinet |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Pipe Sizing Mill
9 top-level lines · 93 rows shown · 641 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Entry Section 6 parts | pipe-sizing-mill-entry-section | 1× | 1 | 29 | assembly |
| 1.1 | Entry Table Roller | pipe-sizing-mill-entry-roller | 6× | 6 | · | part |
| 1.2 | Pinch Roll | pipe-sizing-mill-pinch-roll | 2× | 2 | · | part |
| 1.3 | Side Guide | pipe-sizing-mill-side-guide | 2× | 2 | · | part |
| 1.4 | Entry Trough | pipe-sizing-mill-entry-trough | 1× | 1 | · | part |
| 1.5 | Roller Drive Motor | pipe-sizing-mill-roller-motor | 6× | 6 | · | part |
| 1.6 | Ball Bearing | ball-bearing | 12× | 12 | · | part |
| 2 | Sizing Stand 7 parts | pipe-sizing-mill-stand | 7× | 7 | 21 | assembly |
| 2.1 | Stand Frame | pipe-sizing-mill-stand-frame | 1× | 7 | · | part |
| 2.2 | Sizing Roll 2 parts | pipe-sizing-mill-sizing-roll | 2× | 14 | 2 | assembly |
| 2.2.1 | Roll Body | pipe-sizing-mill-roll-body | 1× | 14 | · | part |
| 2.2.2 | Roll Groove | pipe-sizing-mill-roll-groove | 1× | 14 | · | part |
| 2.3 | Roll Shaft | pipe-sizing-mill-roll-shaft | 2× | 14 | · | part |
| 2.4 | Roll Chock | pipe-sizing-mill-roll-chock | 4× | 28 | · | part |
| 2.5 | Roll-Neck Bearing | pipe-sizing-mill-roll-bearing | 4× | 28 | · | part |
| 2.6 | Screw-Down Adjustment 4 parts | pipe-sizing-mill-screw-adjust | 1× | 7 | 5 | assembly |
| 2.6.1 | Worm Gear | pipe-sizing-mill-worm-gear | 1× | 7 | · | part |
| 2.6.2 | Adjustment Screw | pipe-sizing-mill-adjust-screw | 2× | 14 | · | part |
| 2.6.3 | Position Encoder | pipe-sizing-mill-position-encoder | 1× | 7 | · | part |
| 2.6.4 | Handwheel | pipe-sizing-mill-handwheel | 1× | 7 | · | part |
| 2.7 | Guide Box | pipe-sizing-mill-guide-box | 1× | 7 | · | part |
| 3 | Mill Bed 5 parts | pipe-sizing-mill-mill-bed | 1× | 1 | 38 | assembly |
| 3.1 | Bed Frame | pipe-sizing-mill-bed-frame | 1× | 1 | · | part |
| 3.2 | Stand Housing | pipe-sizing-mill-stand-housing | 7× | 7 | · | part |
| 3.3 | Anchor Bolt | pipe-sizing-mill-anchor-bolt | 28× | 28 | · | part |
| 3.4 | Alignment Shim Set | pipe-sizing-mill-shim-set | 1× | 1 | · | part |
| 3.5 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 4 | Drive Line 5 parts | pipe-sizing-mill-drive-line | 1× | 1 | 260 | assembly |
| 4.1 | Stand Drive Motor 4 parts | pipe-sizing-mill-drive-motor | 7× | 7 | 25 | assembly |
| 4.1.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 7 | 3 | assembly |
| 4.1.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 7 | 19 | assembly |
| 4.1.3 | Ball Bearing | ball-bearing | 2× | 14 | · | part |
| 4.1.4 | Motor Encoder | pipe-sizing-mill-motor-encoder | 1× | 7 | · | part |
| 4.2 | Distribution Gearbox | pipe-sizing-mill-distribution-gearbox | 1× | 1 | · | part |
| 4.3 | Drive Spindle | pipe-sizing-mill-spindle | 14× | 14 | · | part |
| 4.4 | Coupling | pipe-sizing-mill-coupling | 7× | 7 | · | part |
| 4.5 | Reduction Gearbox 4 parts | pipe-sizing-mill-gearbox | 7× | 7 | 9 | assembly |
| 4.5.1 | Gearbox Housing | gearbox-housing | 1× | 7 | · | part |
| 4.5.2 | Helical Gear Pair | gear-pair | 2× | 14 | · | part |
| 4.5.3 | Ball Bearing | ball-bearing | 4× | 28 | · | part |
| 4.5.4 | Oil Seal | oil-seal | 2× | 14 | · | part |
| 5 | Gauging Head 5 parts | pipe-sizing-mill-gauging-head | 1× | 1 | 12 | assembly |
| 5.1 | Laser Scan Gauge | pipe-sizing-mill-laser-gauge | 2× | 2 | · | part |
| 5.2 | Gauge Frame | pipe-sizing-mill-gauge-frame | 1× | 1 | · | part |
| 5.3 | Air Purge | pipe-sizing-mill-air-purge | 1× | 1 | · | part |
| 5.4 | Gauge Cooling Jacket | pipe-sizing-mill-gauge-cooling | 1× | 1 | · | part |
| 5.5 | Gauge Controller 4 parts | pipe-sizing-mill-gauge-controller | 1× | 1 | 7 | assembly |
| 5.5.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 5.5.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 5.5.3 | SMD Passive (R/C/L) | smd-passives | 1× | 1 | · | part |
| 5.5.4 | Connector | connector | 4× | 4 | · | part |
| 6 | Descale and Cooling System 6 parts | pipe-sizing-mill-descale-system | 1× | 1 | 33 | assembly |
| 6.1 | Descale Pump 4 parts | pipe-sizing-mill-descale-pump | 1× | 1 | 9 | assembly |
| 6.1.1 | Pump Casing | pipe-sizing-mill-pump-casing | 1× | 1 | · | part |
| 6.1.2 | Pump Impeller | pipe-sizing-mill-pump-impeller | 4× | 4 | · | part |
| 6.1.3 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 6.1.4 | Oil Seal | oil-seal | 2× | 2 | · | part |
| 6.2 | Water Manifold | pipe-sizing-mill-water-manifold | 1× | 1 | · | part |
| 6.3 | Spray Nozzle | pipe-sizing-mill-spray-nozzle | 16× | 16 | · | part |
| 6.4 | Control Valve | pipe-sizing-mill-control-valve | 4× | 4 | · | part |
| 6.5 | Inlet Strainer | pipe-sizing-mill-strainer | 1× | 1 | · | part |
| 6.6 | Pressure Sensor | pressure-sensor | 2× | 2 | · | part |
| 7 | Exit Run-Out Table 4 parts | pipe-sizing-mill-exit-table | 1× | 1 | 34 | assembly |
| 7.1 | Exit Table Roller | pipe-sizing-mill-exit-roller | 8× | 8 | · | part |
| 7.2 | Roller Drive Motor | pipe-sizing-mill-roller-motor | 8× | 8 | · | part |
| 7.3 | Skid Rail | pipe-sizing-mill-skid-rail | 2× | 2 | · | part |
| 7.4 | Ball Bearing | ball-bearing | 16× | 16 | · | part |
| 8 | Lubrication System 6 parts | pipe-sizing-mill-lube-system | 1× | 1 | 18 | assembly |
| 8.1 | Lube Pump | pipe-sizing-mill-lube-pump | 1× | 1 | · | part |
| 8.2 | Oil Tank | pipe-sizing-mill-oil-tank | 1× | 1 | · | part |
| 8.3 | Oil Filter | pipe-sizing-mill-oil-filter | 2× | 2 | · | part |
| 8.4 | Oil Cooler | pipe-sizing-mill-oil-cooler | 1× | 1 | · | part |
| 8.5 | Lube Manifold | pipe-sizing-mill-lube-manifold | 1× | 1 | · | part |
| 8.6 | Lube Line | pipe-sizing-mill-lube-line | 12× | 12 | · | part |
| 9 | Control Cabinet 8 parts | pipe-sizing-mill-control-cabinet | 1× | 1 | 70 | assembly |
| 9.1 | PLC 4 parts | pipe-sizing-mill-plc | 1× | 1 | 7 | assembly |
| 9.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 9.1.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 9.1.3 | SMD Passive (R/C/L) | smd-passives | 1× | 1 | · | part |
| 9.1.4 | I/O Module | pipe-sizing-mill-io-module | 4× | 4 | · | part |
| 9.2 | Variable-Frequency Drive 3 parts | pipe-sizing-mill-vfd | 7× | 7 | 3 | assembly |
| 9.2.1 | Bare PCB | pcb-bare | 1× | 7 | · | part |
| 9.2.2 | SMD Passive (R/C/L) | smd-passives | 1× | 7 | · | part |
| 9.2.3 | Power Supply | power-supply | 1× | 7 | · | part |
| 9.3 | Operator Touchscreen 3 parts | pipe-sizing-mill-hmi | 1× | 1 | 3 | assembly |
| 9.3.1 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 9.3.2 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 9.3.3 | Microcontroller | mcu | 1× | 1 | · | part |
| 9.4 | Cabinet Enclosure | pipe-sizing-mill-cabinet-shell | 1× | 1 | · | part |
| 9.5 | Power Supply | power-supply | 1× | 1 | · | part |
| 9.6 | Relay | relay | 12× | 12 | · | part |
| 9.7 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 9.8 | Connector | connector | 24× | 24 | · | part |
Related products
same domain, ranked by shared parts Angle Roll Bender
100 parts · shares 3 with this page
 Bed-Type Milling Machine
151 parts · shares 3 with this page
 Bevel Gear Generator
201 parts · shares 3 with this page
Billet Heating Furnace
358 parts · shares 3 with this page
Centering and Facing Machine
1,419 parts · shares 3 with this page
Chain Link Welding Machine
440 parts · shares 3 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
965-word article