Bolt Heading Machine
ProductOverview
A bolt heading machine forms the head of a bolt or screw by upsetting wire cold, striking the end of a cut blank so the metal swells out into a head while the shank stays the wire diameter. It is the front half of how almost every bolt is made: this machine produces a headed blank, and a thread rolling machine adds the thread afterward. Cold heading is fast, runs at over a hundred parts a minute, and wastes almost no material because the head is formed by flow rather than cut from bar stock. The flowed grain also wraps around the head-to-shank fillet, which is the strongest part of a cold-headed bolt and the reason these fasteners resist fatigue better than machined ones.
The machine cuts a blank from wire and drives heading punches against its end. The Press Frame absorbs the force, the Wire Feed meters wire, the Cutoff and Transfer shears the blank and transfers it, the Die Stations grips the shank while the Header Slide upsets the head, the Flywheel Drive stores the blow energy, the Lubrication System system cools the tools, and the Control System runs and guards the cycle.
Frame and forming load
Upsetting a bolt head means stopping a moving slug of metal dead and squashing it sideways, which takes a large momentary force that the Press Frame must take without flexing. The Bed Casting casting carries the slide ways and the die block, the Die Breast backs the die against the blow, and Tie Rod pre-load keeps the whole frame in compression so it stays rigid through millions of cycles. A Forming Guard encloses the heading zone, which throws hot metal and is the chief hazard. Frame stiffness sets head consistency: any spring in the frame shows up as variation in head height.
Wire feed and cutoff
Stock arrives as a coil on the Decoiler and runs through a Straightener that takes out the coil curve, because a bent shank heads off-center. Feed Roll pairs then advance a measured length for the shank plus the metal that will become the head, set by the Feed Cam or a feed servo. The Cutoff and Transfer shears the blank with a carbide Cutoff Knife, and the Cutoff Quill delivers it square to the heading die. From there Transfer Finger grippers driven by the Transfer Cam and returned by Coil Spring move the blank to the next station on a double-blow machine.
Dies and heading slide
Heading happens between the fixed Die Stations and the moving Header Slide. The die block, a Die Case holding carbide tools, has a Grip Die that clamps the shank so only the protruding end deforms, then a Cone Die and a Finish Die that shape the preform and the final head, with Kickout Pin ejectors pushing the finished bolt out. Opposite them the slide carries a Cone Punch that gathers the metal into a cone and a Finish Punch that strikes the final hex, pan, or socket recess, both held in a Punch Holder that indexes them to the work. The Slide Body runs square on Slide Gib strips so the punches land true on the shank.
Flywheel drive
Cold heading needs a large force for a few milliseconds, so the Flywheel Drive stores energy in a heavy Flywheel kept spinning by the Main Motor through Drive Belt pairs. When a blow is called, a Clutch and Brake couples the flywheel to the Crankshaft, and the Pitman Arm converts the crank rotation into the straight slide stroke, all on Ball Bearing supports. The flywheel lets a modest motor deliver a meganewton blow several times a second, the same energy-storage principle used in the Nut Forming Machine and the Rivet Heading Machine.
Lubrication and control
The dies and slide run hot and heavily loaded, so the Lubrication System system feeds oil continuously. An Oil Pump lubricates the slide and crank bearings through an Oil Cooler, while Die Spray Nozzle nozzles cool and lubricate the tools each cycle, confirmed by a Pressure Sensor. The Control System cabinet runs the press: an Microcontroller on a Bare PCB sets stroke rate, a Power Supply feeds the logic, Relay safety chains tie in the guard and clutch, and a Tonnage Monitor tonnage monitor stops the press if forming force climbs, which signals a die jam before it breaks the tooling. The operator works from the Operator Panel.
Heads, materials, and use
A bolt header can form hex heads, socket-cap recesses, pan and flange heads, and carriage-bolt squares simply by changing the finish punch and die. It works in any metal ductile enough to flow cold, which covers most carbon and alloy steels, stainless, brass, and aluminium. The output is a headed blank with no thread yet, so it moves next to a Flat-Die Thread Roller or a cylindrical-die roller that rolls the thread, again by forming rather than cutting. Cold heading dominates fastener production for the same reason throughout this family of machines: at volume it makes a stronger part from less metal in less time than any cutting process can match.
Bolt Heading Machine parts and their functions
8 top-level parts · 102 parts in total · full bill of materials below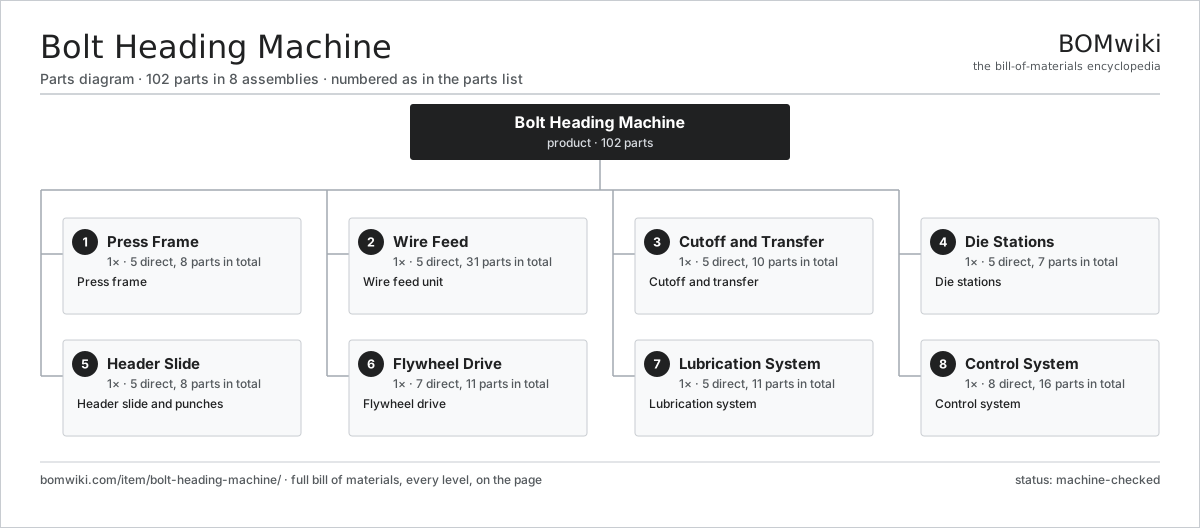
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Press Frame 5 parts | 1× | Press frame |
| 2 | Wire Feed 5 parts | 1× | Wire feed unit |
| 3 | Cutoff and Transfer 5 parts | 1× | Cutoff and transfer |
| 4 | Die Stations 5 parts | 1× | Die stations |
| 5 | Header Slide 5 parts | 1× | Header slide and punches |
| 6 | Flywheel Drive 7 parts | 1× | Flywheel drive |
| 7 | Lubrication System 5 parts | 1× | Lubrication system |
| 8 | Control System 8 parts | 1× | Control system |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Bolt Heading Machine
8 top-level lines · 57 rows shown · 102 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Press Frame 5 parts | bolt-heading-machine-frame | 1× | 1 | 8 | assembly |
| 1.1 | Bed Casting | bolt-heading-machine-bed | 1× | 1 | · | part |
| 1.2 | Die Breast | bolt-heading-machine-die-breast | 1× | 1 | · | part |
| 1.3 | Tie Rod | bolt-heading-machine-tie-rod | 4× | 4 | · | part |
| 1.4 | Forming Guard | bolt-heading-machine-guard | 1× | 1 | · | part |
| 1.5 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 2 | Wire Feed 5 parts | bolt-heading-machine-wire-feed | 1× | 1 | 31 | assembly |
| 2.1 | Feed Roll | bolt-heading-machine-feed-roll | 4× | 4 | · | part |
| 2.2 | Straightener | bolt-heading-machine-straightener | 1× | 1 | · | part |
| 2.3 | Feed Cam | bolt-heading-machine-feed-cam | 1× | 1 | · | part |
| 2.4 | Decoiler | bolt-heading-machine-decoiler | 1× | 1 | · | part |
| 2.5 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 2.5.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 2.5.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 2.5.3 | Encoder | encoder | 1× | 1 | · | part |
| 2.5.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 3 | Cutoff and Transfer 5 parts | bolt-heading-machine-cutoff | 1× | 1 | 10 | assembly |
| 3.1 | Cutoff Knife | bolt-heading-machine-cutoff-knife | 1× | 1 | · | part |
| 3.2 | Cutoff Quill | bolt-heading-machine-cutoff-quill | 1× | 1 | · | part |
| 3.3 | Transfer Finger | bolt-heading-machine-transfer-finger | 4× | 4 | · | part |
| 3.4 | Transfer Cam | bolt-heading-machine-transfer-cam | 1× | 1 | · | part |
| 3.5 | Coil Spring | coil-spring | 3× | 3 | · | part |
| 4 | Die Stations 5 parts | bolt-heading-machine-die-station | 1× | 1 | 7 | assembly |
| 4.1 | Die Case | bolt-heading-machine-die-case | 1× | 1 | · | part |
| 4.2 | Grip Die | bolt-heading-machine-grip-die | 1× | 1 | · | part |
| 4.3 | Cone Die | bolt-heading-machine-cone-die | 1× | 1 | · | part |
| 4.4 | Finish Die | bolt-heading-machine-finish-die | 1× | 1 | · | part |
| 4.5 | Kickout Pin | bolt-heading-machine-kickout-pin | 3× | 3 | · | part |
| 5 | Header Slide 5 parts | bolt-heading-machine-header-slide | 1× | 1 | 8 | assembly |
| 5.1 | Slide Body | bolt-heading-machine-slide-body | 1× | 1 | · | part |
| 5.2 | Cone Punch | bolt-heading-machine-cone-punch | 1× | 1 | · | part |
| 5.3 | Finish Punch | bolt-heading-machine-finish-punch | 1× | 1 | · | part |
| 5.4 | Punch Holder | bolt-heading-machine-punch-holder | 1× | 1 | · | part |
| 5.5 | Slide Gib | bolt-heading-machine-gib | 4× | 4 | · | part |
| 6 | Flywheel Drive 7 parts | bolt-heading-machine-drive | 1× | 1 | 11 | assembly |
| 6.1 | Main Motor | bolt-heading-machine-main-motor | 1× | 1 | · | part |
| 6.2 | Flywheel | bolt-heading-machine-flywheel | 1× | 1 | · | part |
| 6.3 | Clutch and Brake | bolt-heading-machine-clutch-brake | 1× | 1 | · | part |
| 6.4 | Crankshaft | bolt-heading-machine-crankshaft | 1× | 1 | · | part |
| 6.5 | Pitman Arm | bolt-heading-machine-pitman | 1× | 1 | · | part |
| 6.6 | Drive Belt | drive-belt | 2× | 2 | · | part |
| 6.7 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 7 | Lubrication System 5 parts | bolt-heading-machine-lube | 1× | 1 | 11 | assembly |
| 7.1 | Oil Pump | bolt-heading-machine-oil-pump | 1× | 1 | · | part |
| 7.2 | Die Spray Nozzle | bolt-heading-machine-die-spray | 4× | 4 | · | part |
| 7.3 | Oil Cooler | bolt-heading-machine-oil-cooler | 1× | 1 | · | part |
| 7.4 | Oil Seal | oil-seal | 4× | 4 | · | part |
| 7.5 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 8 | Control System 8 parts | bolt-heading-machine-control | 1× | 1 | 16 | assembly |
| 8.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 8.3 | Power Supply | power-supply | 1× | 1 | · | part |
| 8.4 | Relay | relay | 6× | 6 | · | part |
| 8.5 | Tonnage Monitor | bolt-heading-machine-load-cell | 1× | 1 | · | part |
| 8.6 | Operator Panel | bolt-heading-machine-hmi | 1× | 1 | · | part |
| 8.7 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 8.8 | Connector | connector | 4× | 4 | · | part |
Related products
same domain, ranked by shared parts Bevel Gear Generator
201 parts · shares 3 with this page
Blanking Press Line
350 parts · shares 3 with this page
Camshaft Grinder
489 parts · shares 3 with this page
 Crankshaft Grinder
511 parts · shares 3 with this page
 Creep-Feed Grinder
571 parts · shares 3 with this page
 Cylindrical Grinder
167 parts · shares 3 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
982-word article