Progressive Stamping Line
ProductOverview
A progressive stamping line turns a coil of flat strip steel into finished sheet-metal parts at a high, steady rate. The strip is pulled off a coil, flattened, and fed an exact distance into a press on each stroke. Inside the press a single multi-station tool, the progressive die, pierces holes, bends flanges, and draws shapes at successive stations as the strip steps through it, then cuts the completed part free at the last station. The skeleton of leftover metal is chopped and carried away as scrap. One line can stamp brackets, contacts, lamination blanks, clips, and chassis parts by the hundred per minute, which is why progressive stamping is the standard way to make small metal parts in volume for automotive, appliance, electrical, and electronics work.
The line runs as a chain of subsystems. The Decoiler holds the coil and pays it off, the Straightener takes the curve out of it, the Servo Roll Feed indexes it forward by one part pitch each stroke, and the Stamping Press drives the Progressive Die Set down onto it. The Scrap System clears the web, the Part Discharge moves out finished parts, the Lubrication System wets the strip, and the Control System keeps all of it in time and stops the press if anything misfeeds.
Coil handling and straightening
A coil of strip can weigh several tonnes and carries a strong curl from the way it was wound. The Decoiler grips the coil bore with an Expanding Mandrel that expands inside it, and a Reel Drive pays the strip off while a Coil Brake drags the reel so it cannot overrun and dump a loop of slack. A Coil Car lifts each new coil off the floor and aligns its bore with the mandrel, and a Keeper Arm presses on the outer wrap so the coil does not spring open when the band is cut.
Strip cannot enter a die with the coil curl still in it. The Straightener threads it through a staggered bank of small Work Roll units that bend it up and down past its yield point, relieving the set so it comes out flat. Each work roll is held against deflection by a Backup Roll, and a Flatness Screw sets how deep the upper bank presses to tune flatness for a given thickness. A short slack loop between the straightener and the feed lets the two run at slightly different rates without fighting.
Servo feed
The Servo Roll Feed is what makes the line a progressive line rather than a single-hit press. Between strokes it advances the strip exactly one part pitch through a pair of Feed Roll units driven by a Servo Motor through the Feed Gearbox. A Feed Encoder closes the loop on feed length so every advance matches the die layout to within a few hundredths of a millimeter. Just before the punches hit, the Roll Release lifts the upper feed roll under the Release Cylinder so the die pilots can pull the strip into final register. A Edge Guide keeps the strip centered as it enters.
The press
The Stamping Press supplies the force and the motion. A Main Motor spins a heavy Flywheel that stores energy between strokes, so the motor sees an even load instead of a spike at each hit. When a stroke is called the Clutch-Brake couples the flywheel to the Crankshaft, whose eccentric drives the Slide down through two Connecting Rod links. The Slide Gib strips guide the slide square so the die halves stay aligned, and a Counterbalance carries the slide and upper-die weight so it does not load the clutch. The Bolster Plate spreads the stamping reaction into the Press Frame. The clutch and brake act together: applying air engages the clutch to run, and exhausting it lets springs set the brake and stop the slide at top dead center.
The progressive die
The Progressive Die Set is the tool that gives each part its shape. An Upper Die Shoe bolted to the slide and a Lower Die Shoe clamped to the bolster are held in line by four Guide Post pillars. Each station does one operation: a Piercing Punch shears a hole into a hardened Die Button, a Forming Punch bends or draws the metal, and a spring-loaded Stripper Plate holds the strip flat and pulls it off the punches on the upstroke. Pilot Pin units enter pre-pierced holes to register the strip before the working punches land. At the last station a Cutoff Punch severs the finished part from the carrier. Die wear, clearance, and the tonnage each station draws set how long the tool runs between regrinds.
Scrap, discharge, lubrication, and control
The leftover web is cut into short lengths by the Scrap Chopper and carried off by the Scrap Conveyor, while pierced slugs fall through a Slug Chute onto the same belt. Finished parts leave on the Part Conveyor, helped clear of the die by a Blow-off Nozzle and tallied by a Part Counter. The Lubrication System wets the strip with stamping oil from a Lube Roller so the punches do not gall. Over all of it the Line PLC and the Press Control sequence the cycle, the Die Protection module watches in-die Die Sensor signals and stops the press in mid-stroke if a part fails to eject, and the Tonnage Monitor flags a dull punch or a slug stack before it cracks the tool. Light curtains guard the die opening so the slide cannot run while a hand is in the work zone. Lines vary from small high-speed presses making electrical contacts at 250 strokes a minute to heavy 600-tonne lines stamping structural brackets, all built on the same coil to finished-part flow.
Progressive Stamping Line parts and their functions
9 top-level parts · 335 parts in total · full bill of materials below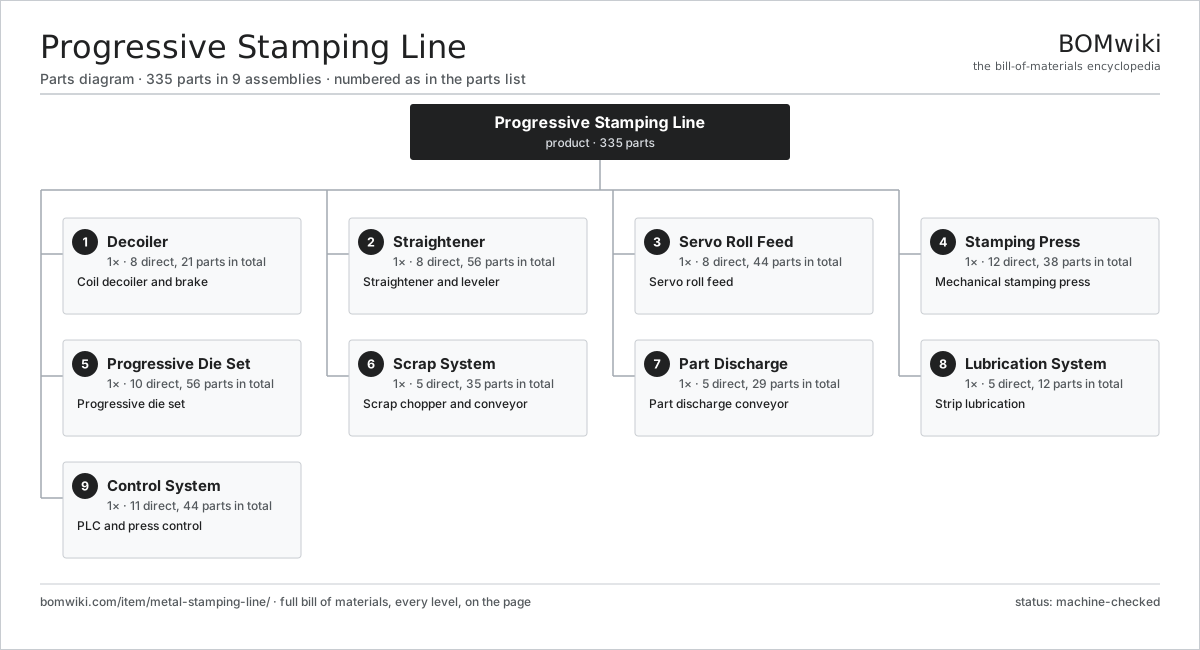
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Decoiler 8 parts | 1× | Coil decoiler and brake |
| 2 | Straightener 8 parts | 1× | Straightener and leveler |
| 3 | Servo Roll Feed 8 parts | 1× | Servo roll feed |
| 4 | Stamping Press 12 parts | 1× | Mechanical stamping press |
| 5 | Progressive Die Set 10 parts | 1× | Progressive die set |
| 6 | Scrap System 5 parts | 1× | Scrap chopper and conveyor |
| 7 | Part Discharge 5 parts | 1× | Part discharge conveyor |
| 8 | Lubrication System 5 parts | 1× | Strip lubrication |
| 9 | Control System 11 parts | 1× | PLC and press control |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Progressive Stamping Line
9 top-level lines · 115 rows shown · 335 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Decoiler 8 parts | metal-stamping-line-decoiler | 1× | 1 | 21 | assembly |
| 1.1 | Expanding Mandrel 4 parts | metal-stamping-line-mandrel | 1× | 1 | 8 | assembly |
| 1.1.1 | Mandrel Segment | metal-stamping-line-mandrel-segment | 4× | 4 | · | part |
| 1.1.2 | Expansion Screw | metal-stamping-line-expansion-screw | 1× | 1 | · | part |
| 1.1.3 | Mandrel Shaft | metal-stamping-line-mandrel-shaft | 1× | 1 | · | part |
| 1.1.4 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 1.2 | Reel Drive | metal-stamping-line-reel-drive | 1× | 1 | · | part |
| 1.3 | Coil Brake | metal-stamping-line-coil-brake | 1× | 1 | · | part |
| 1.4 | Coil Car 3 parts | metal-stamping-line-coil-car | 1× | 1 | 3 | assembly |
| 1.4.1 | Coil Cradle | metal-stamping-line-car-cradle | 1× | 1 | · | part |
| 1.4.2 | Coil Lift | metal-stamping-line-car-lift | 1× | 1 | · | part |
| 1.4.3 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 1.5 | Keeper Arm | metal-stamping-line-keeper-arm | 1× | 1 | · | part |
| 1.6 | Loop Sensor | metal-stamping-line-loop-sensor | 2× | 2 | · | part |
| 1.7 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 1.8 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 2 | Straightener 8 parts | metal-stamping-line-straightener | 1× | 1 | 56 | assembly |
| 2.1 | Work Roll | metal-stamping-line-work-roll | 11× | 11 | · | part |
| 2.2 | Pinch Roll | metal-stamping-line-pinch-roll | 2× | 2 | · | part |
| 2.3 | Backup Roll | metal-stamping-line-backup-roll | 8× | 8 | · | part |
| 2.4 | Flatness Screw | metal-stamping-line-flatness-screw | 6× | 6 | · | part |
| 2.5 | Straightener Drive | metal-stamping-line-straightener-drive | 1× | 1 | · | part |
| 2.6 | Helical Gear Pair | gear-pair | 5× | 5 | · | part |
| 2.7 | Ball Bearing | ball-bearing | 22× | 22 | · | part |
| 2.8 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 3 | Servo Roll Feed 8 parts | metal-stamping-line-feeder | 1× | 1 | 44 | assembly |
| 3.1 | Feed Roll | metal-stamping-line-feed-roll | 2× | 2 | · | part |
| 3.2 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 3.2.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 3.2.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 3.2.3 | Encoder | encoder | 1× | 1 | · | part |
| 3.2.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 3.3 | Feed Gearbox 4 parts | metal-stamping-line-feed-gearbox | 1× | 1 | 9 | assembly |
| 3.3.1 | Helical Gear Pair | gear-pair | 2× | 2 | · | part |
| 3.3.2 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 3.3.3 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 3.3.4 | Oil Seal | oil-seal | 2× | 2 | · | part |
| 3.4 | Roll Release | metal-stamping-line-roll-release | 1× | 1 | · | part |
| 3.5 | Release Cylinder | metal-stamping-line-pilot-release-cyl | 1× | 1 | · | part |
| 3.6 | Edge Guide | metal-stamping-line-edge-guide | 2× | 2 | · | part |
| 3.7 | Feed Encoder | metal-stamping-line-encoder | 1× | 1 | · | part |
| 3.8 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 4 | Stamping Press 12 parts | metal-stamping-line-press | 1× | 1 | 38 | assembly |
| 4.1 | Press Frame | metal-stamping-line-press-frame | 1× | 1 | · | part |
| 4.2 | Crankshaft | metal-stamping-line-crankshaft | 1× | 1 | · | part |
| 4.3 | Flywheel | metal-stamping-line-flywheel | 1× | 1 | · | part |
| 4.4 | Clutch-Brake 4 parts | metal-stamping-line-clutch-brake | 1× | 1 | 14 | assembly |
| 4.4.1 | Clutch Plate | metal-stamping-line-clutch-plate | 4× | 4 | · | part |
| 4.4.2 | Brake Plate | metal-stamping-line-brake-plate | 3× | 3 | · | part |
| 4.4.3 | Clutch Cylinder | metal-stamping-line-clutch-cylinder | 1× | 1 | · | part |
| 4.4.4 | Coil Spring | coil-spring | 6× | 6 | · | part |
| 4.5 | Slide | metal-stamping-line-slide | 1× | 1 | · | part |
| 4.6 | Connecting Rod | metal-stamping-line-connecting-rod | 2× | 2 | · | part |
| 4.7 | Slide Gib | metal-stamping-line-gib | 4× | 4 | · | part |
| 4.8 | Bolster Plate | metal-stamping-line-bolster | 1× | 1 | · | part |
| 4.9 | Counterbalance | metal-stamping-line-counterbalance | 2× | 2 | · | part |
| 4.10 | Main Motor | metal-stamping-line-main-motor | 1× | 1 | · | part |
| 4.11 | Drive Belt | drive-belt | 4× | 4 | · | part |
| 4.12 | Ball Bearing | ball-bearing | 6× | 6 | · | part |
| 5 | Progressive Die Set 10 parts | metal-stamping-line-die-set | 1× | 1 | 56 | assembly |
| 5.1 | Upper Die Shoe | metal-stamping-line-upper-shoe | 1× | 1 | · | part |
| 5.2 | Lower Die Shoe | metal-stamping-line-lower-shoe | 1× | 1 | · | part |
| 5.3 | Guide Post | metal-stamping-line-guide-post | 4× | 4 | · | part |
| 5.4 | Piercing Punch | metal-stamping-line-punch | 12× | 12 | · | part |
| 5.5 | Forming Punch | metal-stamping-line-form-punch | 4× | 4 | · | part |
| 5.6 | Die Button | metal-stamping-line-die-button | 12× | 12 | · | part |
| 5.7 | Stripper Plate | metal-stamping-line-stripper-plate | 1× | 1 | · | part |
| 5.8 | Pilot Pin | metal-stamping-line-pilot-pin | 4× | 4 | · | part |
| 5.9 | Coil Spring | coil-spring | 16× | 16 | · | part |
| 5.10 | Cutoff Punch | metal-stamping-line-cutoff-punch | 1× | 1 | · | part |
| 6 | Scrap System 5 parts | metal-stamping-line-scrap-system | 1× | 1 | 35 | assembly |
| 6.1 | Scrap Chopper 3 parts | metal-stamping-line-scrap-chopper | 1× | 1 | 5 | assembly |
| 6.1.1 | Chopper Blade | metal-stamping-line-chopper-blade | 2× | 2 | · | part |
| 6.1.2 | Chopper Cam | metal-stamping-line-chopper-cam | 1× | 1 | · | part |
| 6.1.3 | Coil Spring | coil-spring | 2× | 2 | · | part |
| 6.2 | Scrap Conveyor | metal-stamping-line-scrap-conveyor | 1× | 1 | · | part |
| 6.3 | Slug Chute | metal-stamping-line-slug-chute | 4× | 4 | · | part |
| 6.4 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 6.4.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 6.4.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 6.4.3 | Encoder | encoder | 1× | 1 | · | part |
| 6.4.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 6.5 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 7 | Part Discharge 5 parts | metal-stamping-line-discharge | 1× | 1 | 29 | assembly |
| 7.1 | Part Conveyor | metal-stamping-line-part-conveyor | 1× | 1 | · | part |
| 7.2 | Blow-off Nozzle | metal-stamping-line-blowoff-nozzle | 2× | 2 | · | part |
| 7.3 | Part Counter | metal-stamping-line-part-counter | 1× | 1 | · | part |
| 7.4 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 7.4.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 7.4.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 7.4.3 | Encoder | encoder | 1× | 1 | · | part |
| 7.4.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 7.5 | Drive Belt | drive-belt | 1× | 1 | · | part |
| 8 | Lubrication System 5 parts | metal-stamping-line-lube-system | 1× | 1 | 12 | assembly |
| 8.1 | Lube Pump | metal-stamping-line-lube-pump | 1× | 1 | · | part |
| 8.2 | Lube Roller | metal-stamping-line-lube-roller | 2× | 2 | · | part |
| 8.3 | Lube Tank | metal-stamping-line-lube-tank | 1× | 1 | · | part |
| 8.4 | Lube Valve | metal-stamping-line-lube-valve | 4× | 4 | · | part |
| 8.5 | Connector | connector | 4× | 4 | · | part |
| 9 | Control System 11 parts | metal-stamping-line-control-system | 1× | 1 | 44 | assembly |
| 9.1 | Line PLC | metal-stamping-line-plc | 1× | 1 | · | part |
| 9.2 | Press Control | metal-stamping-line-press-control | 1× | 1 | · | part |
| 9.3 | Servo Drive | metal-stamping-line-servo-drive | 3× | 3 | · | part |
| 9.4 | Die Protection 4 parts | metal-stamping-line-die-protection | 1× | 1 | 9 | assembly |
| 9.4.1 | Die Sensor | metal-stamping-line-die-sensor | 6× | 6 | · | part |
| 9.4.2 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 9.4.3 | Microcontroller | mcu | 1× | 1 | · | part |
| 9.4.4 | SMD Passive (R/C/L) | smd-passives | 1× | 1 | · | part |
| 9.5 | Tonnage Monitor | metal-stamping-line-tonnage-monitor | 1× | 1 | · | part |
| 9.6 | Light Curtain | metal-stamping-line-light-curtain | 2× | 2 | · | part |
| 9.7 | Operator HMI | metal-stamping-line-hmi | 1× | 1 | · | part |
| 9.8 | Power Supply | power-supply | 1× | 1 | · | part |
| 9.9 | Relay | relay | 8× | 8 | · | part |
| 9.10 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 9.11 | Connector | connector | 16× | 16 | · | part |
Related products
same domain, ranked by shared parts Bevel Gear Generator
201 parts · shares 5 with this page
Blanking Press Line
350 parts · shares 5 with this page
 Creep-Feed Grinder
571 parts · shares 5 with this page
 Railway Wheel Lathe
1,201 parts · shares 5 with this page
Roller Leveler
469 parts · shares 5 with this page
 Rotary-Table Surface Grinder
172 parts · shares 5 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
1,128-word article