Roller Shutter Slat Rollformer
ProductOverview
A roller shutter slat rollformer turns a coil of thin coated steel into the interlocking slats that make up a rolling shutter or rolling door. It does this by roll forming: the flat strip passes through a row of paired rollers, each bending it a little more, until the cumulative bends produce the curved slat profile with a hook along one long edge and an eye along the other. Successive slats hinge together at those curled edges, so a finished shutter rolls up into a small drum yet hangs as a continuous curtain when down. The machine forms the profile, curls the edges, punches the end slots, and cuts each slat to length, delivering finished slats ready to assemble into a shutter.
Strip comes off the Strip Decoiler through the Feed and Guide into the Roll Forming Stands, which form the profile under the Forming Line Drive. The Edge Curling Station rolls the interlock curls, the Slot and Vent Punch adds slots and vents, and the Flying Cutoff cuts slats to length onto the Runout Table table. The Control System sets length and quantity and times the moving operations.
Roll forming the profile
Roll forming is a gradual process, and that is its strength: bending thin strip a small amount at each of many stands avoids the cracking and springback that a single sharp bend would cause. The Roll Forming Stands hold a row of Forming Stand units, each with a pair of profiled Form Roll rolls on driven Roll Shaft shafts. The first stands put a gentle curve in the flat strip, the middle stands deepen it, and the last stands set the final slat curvature and the lead-in to the edge curls. Every stand sits on a machined Base Rail so all the passes share one straight pass line, and a Gap Adjust Screw at each stand trims the roll gap to the exact strip thickness.
The rolls are hardened tool steel because they shape coated steel continuously and must not mark the painted surface. A slat profile is defined by its set of rolls, so a different slat shape or pitch needs a different roll set, which is why these machines are dedicated to one profile family at a time.
Driving the line at matched speed
If the stands turned at different surface speeds they would stretch or buckle the strip between them, so the Forming Line Drive turns them all together. A Servo Motor feeds the Line Gearbox, which sets line speed, and a common Line Drive Shaft with a Drive Chain Set distributes that drive to every stand through Drive Coupling couplings. Keeping the surface speed of all rolls matched is what lets the strip flow through without distortion.
Curling the interlock
The feature that makes a shutter slat is the curl on each long edge. The Edge Curling Station rolls one edge into an open hook and the other into a closed eye, using Curling Roll rolls to wrap the metal and Hem Roll rolls to close the curl tight. When slats are assembled, the hook of one slat hooks into the eye of the next, so the joint hinges as the shutter rolls and stays closed when it hangs. The Curl Stand holds these rolls in precise register with the formed profile, since a curl that is too loose rattles and one too tight will not hinge.
Punching, cutting, and stacking
Shutter slats need end slots so they can be locked or clipped at the guides, and some are ventilated. The Slot and Vent Punch handles this: the Slot Punch Die, driven by the Punch Cylinder, punches the end fixing slots, and an optional Vent Die punches ventilation perforations for perforated slats, with slugs falling into the Slug Tray.
The slat must be cut to a precise length without stopping the line, so the Flying Cutoff is a flying shear. The Flying Carriage accelerates to match line speed, the Shear Cylinder drives the profiled Cutoff Blade through the moving slat for a square cut, then the carriage returns, all triggered by the Encoder Wheel that counts off the slat length. The cut slats run onto the Runout Table table where the Slat Stacker nests them into bundles for the assembly line.
Materials, variants, and use
Strip is usually galvanized steel pre-painted in the shutter colour, between 0.5 and 1.2 mm thick, or aluminium for lighter shutters. Slat profiles range from small pitches for shopfront and window shutters up to larger insulated slats for industrial doors, and insulated slats are roll formed as a skin then foam filled in a separate step. A machine is built for one profile family; the roll set in the Roll Forming Stands and curling rolls define the slat, while length is fully programmable at the Control System. The slats these lines make go into security shutters, garage and industrial rolling doors, shopfront closures, and grilles, the bulk of the rolling-shutter market.
Control and changeover
The Control System runs the line from one screen. A PLC sets line speed through the Line Drive VFD, counts slat length from the Encoder Wheel, and fires the Slot and Vent Punch and flying Flying Cutoff at the right position while the strip moves. Operators enter slat length and quantity at the LCD Panel and the line forms, slots, and cuts a batch unattended. Changeover to a new profile means swapping the roll set and curl rolls and reloading the Strip Decoiler with the right coil, after which the same length program drives the new run.
Roller Shutter Slat Rollformer parts and their functions
9 top-level parts · 524 parts in total · full bill of materials below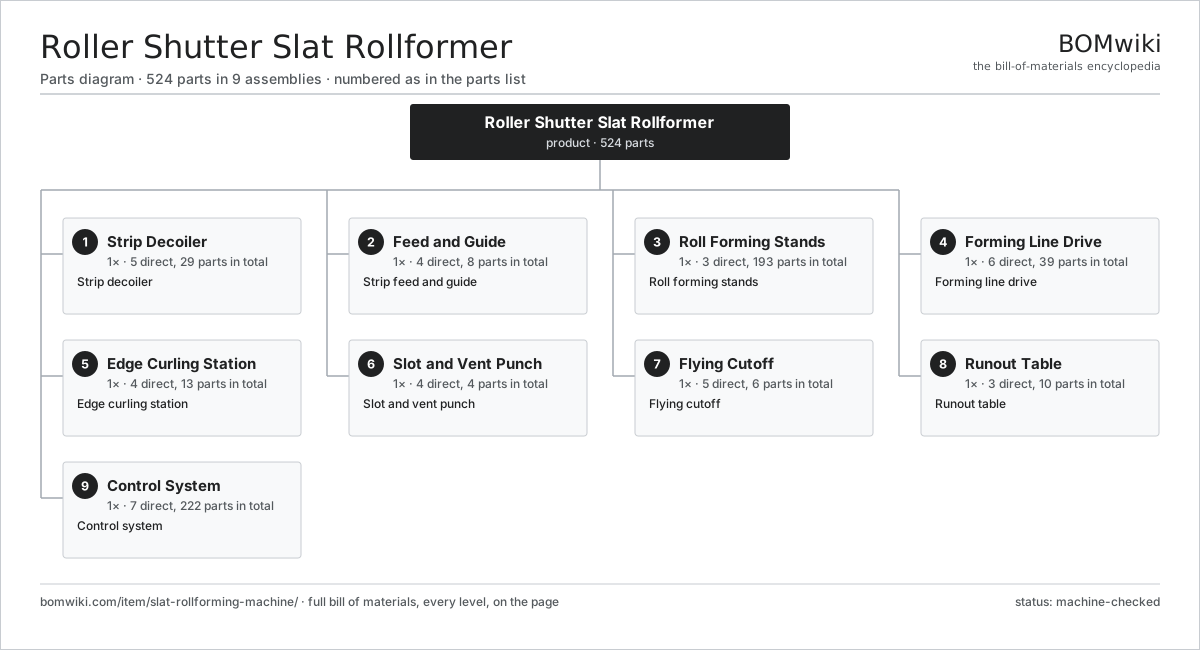
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Strip Decoiler 5 parts | 1× | Strip decoiler |
| 2 | Feed and Guide 4 parts | 1× | Strip feed and guide |
| 3 | Roll Forming Stands 3 parts | 1× | Roll forming stands |
| 4 | Forming Line Drive 6 parts | 1× | Forming line drive |
| 5 | Edge Curling Station 4 parts | 1× | Edge curling station |
| 6 | Slot and Vent Punch 4 parts | 1× | Slot and vent punch |
| 7 | Flying Cutoff 5 parts | 1× | Flying cutoff |
| 8 | Runout Table 3 parts | 1× | Runout table |
| 9 | Control System 7 parts | 1× | Control system |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Roller Shutter Slat Rollformer
9 top-level lines · 74 rows shown · 524 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Strip Decoiler 5 parts | slat-rollforming-machine-decoiler | 1× | 1 | 29 | assembly |
| 1.1 | Expanding Mandrel | slat-rollforming-machine-mandrel | 1× | 1 | · | part |
| 1.2 | Decoiler Brake | slat-rollforming-machine-brake | 1× | 1 | · | part |
| 1.3 | Coil Car | slat-rollforming-machine-coil-car | 1× | 1 | · | part |
| 1.4 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 1.5 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 1.5.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 1.5.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 1.5.3 | Encoder | encoder | 1× | 1 | · | part |
| 1.5.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 2 | Feed and Guide 4 parts | slat-rollforming-machine-feed-section | 1× | 1 | 8 | assembly |
| 2.1 | Entry Edge Guide | slat-rollforming-machine-entry-guide | 1× | 1 | · | part |
| 2.2 | Feed Roll | slat-rollforming-machine-feed-rolls | 2× | 2 | · | part |
| 2.3 | Strip Sensor | slat-rollforming-machine-strip-sensor | 1× | 1 | · | part |
| 2.4 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 3 | Roll Forming Stands 3 parts | slat-rollforming-machine-roll-stands | 1× | 1 | 193 | assembly |
| 3.1 | Forming Stand 5 parts | slat-rollforming-machine-roll-stand | 16× | 16 | 11 | assembly |
| 3.1.1 | Form Roll | slat-rollforming-machine-form-roll | 2× | 32 | · | part |
| 3.1.2 | Roll Shaft | slat-rollforming-machine-roll-shaft | 2× | 32 | · | part |
| 3.1.3 | Stand Frame | slat-rollforming-machine-stand-frame | 1× | 16 | · | part |
| 3.1.4 | Gap Adjust Screw | slat-rollforming-machine-adjust-screw | 2× | 32 | · | part |
| 3.1.5 | Ball Bearing | ball-bearing | 4× | 64 | · | part |
| 3.2 | Base Rail | slat-rollforming-machine-base-rail | 1× | 1 | · | part |
| 3.3 | Drive Coupling | slat-rollforming-machine-shaft-coupling | 16× | 16 | · | part |
| 4 | Forming Line Drive 6 parts | slat-rollforming-machine-drive | 1× | 1 | 39 | assembly |
| 4.1 | Line Gearbox 3 parts | slat-rollforming-machine-gearbox | 1× | 1 | 8 | assembly |
| 4.1.1 | Helical Gear Pair | gear-pair | 2× | 2 | · | part |
| 4.1.2 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 4.1.3 | Oil Seal | oil-seal | 2× | 2 | · | part |
| 4.2 | Line Drive Shaft | slat-rollforming-machine-drive-shaft | 1× | 1 | · | part |
| 4.3 | Drive Chain Set | slat-rollforming-machine-chain-set | 1× | 1 | · | part |
| 4.4 | Helical Gear Pair | gear-pair | 4× | 4 | · | part |
| 4.5 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 4.5.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 4.5.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 4.5.3 | Encoder | encoder | 1× | 1 | · | part |
| 4.5.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 4.6 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 5 | Edge Curling Station 4 parts | slat-rollforming-machine-curling-station | 1× | 1 | 13 | assembly |
| 5.1 | Curling Roll | slat-rollforming-machine-curl-roll | 4× | 4 | · | part |
| 5.2 | Hem Roll | slat-rollforming-machine-hem-roll | 2× | 2 | · | part |
| 5.3 | Curl Stand | slat-rollforming-machine-curl-stand | 1× | 1 | · | part |
| 5.4 | Ball Bearing | ball-bearing | 6× | 6 | · | part |
| 6 | Slot and Vent Punch 4 parts | slat-rollforming-machine-punch-unit | 1× | 1 | 4 | assembly |
| 6.1 | Slot Punch Die | slat-rollforming-machine-punch-die | 1× | 1 | · | part |
| 6.2 | Punch Cylinder | slat-rollforming-machine-punch-cylinder | 1× | 1 | · | part |
| 6.3 | Vent Die | slat-rollforming-machine-vent-die | 1× | 1 | · | part |
| 6.4 | Slug Tray | slat-rollforming-machine-slug-tray | 1× | 1 | · | part |
| 7 | Flying Cutoff 5 parts | slat-rollforming-machine-cutoff | 1× | 1 | 6 | assembly |
| 7.1 | Cutoff Blade | slat-rollforming-machine-cutoff-blade | 1× | 1 | · | part |
| 7.2 | Flying Carriage | slat-rollforming-machine-cutoff-carriage | 1× | 1 | · | part |
| 7.3 | Shear Cylinder | slat-rollforming-machine-cutoff-cylinder | 1× | 1 | · | part |
| 7.4 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 7.5 | Encoder Wheel | slat-rollforming-machine-encoder-wheel | 1× | 1 | · | part |
| 8 | Runout Table 3 parts | slat-rollforming-machine-runout | 1× | 1 | 10 | assembly |
| 8.1 | Runout Roller | slat-rollforming-machine-runout-roller | 8× | 8 | · | part |
| 8.2 | Slat Stacker | slat-rollforming-machine-stacker | 1× | 1 | · | part |
| 8.3 | Runout Frame | slat-rollforming-machine-runout-frame | 1× | 1 | · | part |
| 9 | Control System 7 parts | slat-rollforming-machine-control | 1× | 1 | 222 | assembly |
| 9.1 | PLC 3 parts | slat-rollforming-machine-plc | 1× | 1 | 112 | assembly |
| 9.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 9.1.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 9.1.3 | SMD Passive (R/C/L) | smd-passives | 110× | 110 | · | part |
| 9.2 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 9.3 | Line Drive VFD 5 parts | slat-rollforming-machine-vfd | 1× | 1 | 89 | assembly |
| 9.3.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 9.3.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 9.3.3 | Power MOSFET | mosfet | 6× | 6 | · | part |
| 9.3.4 | Gate Driver IC | gate-driver-ic | 1× | 1 | · | part |
| 9.3.5 | SMD Passive (R/C/L) | smd-passives | 80× | 80 | · | part |
| 9.4 | Power Supply | power-supply | 1× | 1 | · | part |
| 9.5 | Relay | relay | 6× | 6 | · | part |
| 9.6 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 9.7 | Connector | connector | 12× | 12 | · | part |
Related products
same domain, ranked by shared parts Servo Stamping Press
633 parts · shares 4 with this page
 Industrial TIG Welder
492 parts · shares 3 with this page
 Railway Wheel Lathe
1,201 parts · shares 6 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
1,030-word article