Nitriding Furnace
ProductOverview
A nitriding furnace case-hardens steel by diffusing nitrogen into its surface at a low temperature, between about 480 and 580 degrees Celsius. Unlike hardening by heating and quenching, nitriding adds nitrogen that forms hard iron and alloy nitrides in a thin surface layer while the core stays unchanged. Because the process runs below the temperature where steel transforms, and because there is no quench, parts come out very hard at the surface with almost no distortion. That low distortion is the main reason to nitride: gears, crankshafts, dies, extrusion screws, and valve parts can be finish-machined first and nitrided last with little need for grinding afterward. The trade is time, since the cycle runs for many hours while nitrogen slowly diffuses inward.
The furnace centers on a sealed Retort holding the charge in a controlled atmosphere. Around it the Heating System system holds the narrow process temperature, the Gas System feeds nitrogen to the steel, and on plasma machines the Plasma System drives nitrogen in by glow discharge. The Vacuum System system manages pressure and exhaust, the Cooling System system ends the cycle, the Control System system runs the recipe, and the Frame and Handling carries and loads the charge.
The retort
The Retort is the heart of the machine. Its Retort Vessel is a heat-resistant alloy can that confines the process gas and the parts, keeping the reactive atmosphere away from the heating elements outside it. The Retort Lid seals the top and carries gas, sensor, and power ports, and the Lid Seal is a water-cooled flange with a gasket that keeps the hot vessel gas-tight, backed by an O-Ring Set. Parts load in Charge Basket baskets or hang on a Fixture Tree so every surface sees the gas, since nitrogen only enters where the atmosphere can reach. Spacing the charge well is part of getting an even case.
Heating
The Heating System system holds the charge in the tight nitriding band. Banks of Heating Element elements on Element Holder supports surround the retort, wrapped in an Insulation Pack of fiber and brick. A Convection Fan inside circulates the gas so all parts reach the same temperature, which matters because case depth depends on temperature and time together. Power is metered by a SCR Controller reading a Control Thermocouple. Holding plus or minus 5 degrees across the charge keeps the case uniform from part to part.
Gas and plasma
In gas nitriding the Gas System supplies the nitrogen. Anhydrous ammonia flows through the Ammonia Line and breaks down at the hot steel surface, releasing nitrogen that diffuses in. A Nitrogen Line and Hydrogen Line let the operator dilute and tune the atmosphere, each metered by a Mass Flow Controller through Gas Valve solenoids, with a Gas Preheater warming the feed. A Dissociation Meter reads how far the ammonia has cracked, which sets the nitriding potential and so the kind of case formed. In plasma nitriding the Plasma System does the work instead: a DC Power Supply puts the charge on a Cathode Table at negative voltage against the grounded Anode Shell, striking a glow discharge that bombards the parts with nitrogen ions through HV Feedthrough bushings. A Arc Suppressor cuts power the instant an arc forms, since an arc would pit the part.
Vacuum, exhaust, and cooling
The Vacuum System system serves both plasma and gas work. A Vacuum Pump with a Pump Rotor driven by a Pump Motor on Ball Bearing supports and Oil Seal seals pulls the retort down before backfilling. Spent ammonia is hazardous, so it passes a Exhaust Burner that cracks it and a Scrubber that captures the rest before the stack, with Vacuum Valve isolation and Pressure Sensor readings. When the long soak ends, the Cooling System system circulates gas with a Cooling Fan through a Heat Exchanger cooled by a Cooling Pump and the Water Jacket, so parts come down slowly without distortion.
Control, handling, and variants
The Control System system uses an Microcontroller on a Bare PCB board with SMD Passive (R/C/L), a HMI Panel and LCD Panel, Relay outputs, and a Power Supply, wired with Wire Bundle and Connector terminals. It runs multi-step recipes that hold temperature and nitriding potential for the many hours the cycle needs. The Frame and Handling is a Base Frame with Sheet Metal Panel covers and Leveling Foot feet, and because loaded retorts are heavy the Lid Hoist uses a Ball Screw and Linear Guide Rail pair driven by a Hoist Motor to lift the Lift Frame, with a Roller Cart to bring the charge in. The three common variants differ by how nitrogen is supplied: gas nitriding through ammonia, salt-bath nitriding in molten cyanate, and plasma nitriding by glow discharge. Plasma works cleanest and on stainless that gas cannot easily treat, while gas nitriding suits large batches at lower equipment cost. The limits are the long cycle and the need for alloy steels that contain nitride-forming elements like chromium, aluminium, or vanadium to reach full hardness. Within those bounds nitriding gives a hard, wear-resistant, and fatigue-resistant surface on a tough core with almost no change in size.
Nitriding Furnace parts and their functions
8 top-level parts · 105 parts in total · full bill of materials below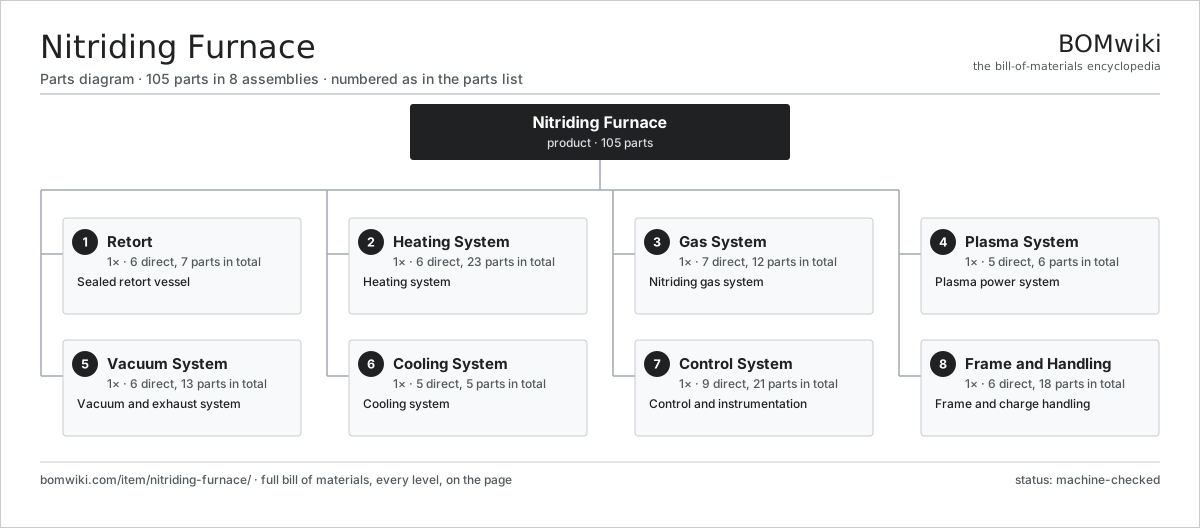
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Retort 6 parts | 1× | Sealed retort vessel |
| 2 | Heating System 6 parts | 1× | Heating system |
| 3 | Gas System 7 parts | 1× | Nitriding gas system |
| 4 | Plasma System 5 parts | 1× | Plasma power system |
| 5 | Vacuum System 6 parts | 1× | Vacuum and exhaust system |
| 6 | Cooling System 5 parts | 1× | Cooling system |
| 7 | Control System 9 parts | 1× | Control and instrumentation |
| 8 | Frame and Handling 6 parts | 1× | Frame and charge handling |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Nitriding Furnace
8 top-level lines · 66 rows shown · 105 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Retort 6 parts | nitriding-furnace-retort | 1× | 1 | 7 | assembly |
| 1.1 | Retort Vessel | nitriding-furnace-retort-vessel | 1× | 1 | · | part |
| 1.2 | Retort Lid | nitriding-furnace-retort-lid | 1× | 1 | · | part |
| 1.3 | Lid Seal | nitriding-furnace-lid-seal | 1× | 1 | · | part |
| 1.4 | Charge Basket | nitriding-furnace-charge-basket | 2× | 2 | · | part |
| 1.5 | Fixture Tree | nitriding-furnace-fixture-tree | 1× | 1 | · | part |
| 1.6 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 2 | Heating System 6 parts | nitriding-furnace-heating | 1× | 1 | 23 | assembly |
| 2.1 | Heating Element | heating-element | 8× | 8 | · | part |
| 2.2 | Element Holder | nitriding-furnace-element-holder | 8× | 8 | · | part |
| 2.3 | Insulation Pack | nitriding-furnace-insulation-pack | 1× | 1 | · | part |
| 2.4 | Convection Fan | nitriding-furnace-convection-fan | 1× | 1 | · | part |
| 2.5 | Control Thermocouple | nitriding-furnace-control-thermocouple | 3× | 3 | · | part |
| 2.6 | SCR Controller | nitriding-furnace-scr-controller | 2× | 2 | · | part |
| 3 | Gas System 7 parts | nitriding-furnace-gas-system | 1× | 1 | 12 | assembly |
| 3.1 | Ammonia Line | nitriding-furnace-ammonia-line | 1× | 1 | · | part |
| 3.2 | Nitrogen Line | nitriding-furnace-nitrogen-line | 1× | 1 | · | part |
| 3.3 | Hydrogen Line | nitriding-furnace-hydrogen-line | 1× | 1 | · | part |
| 3.4 | Mass Flow Controller | nitriding-furnace-mass-flow-controller | 3× | 3 | · | part |
| 3.5 | Gas Valve | nitriding-furnace-gas-valve | 4× | 4 | · | part |
| 3.6 | Dissociation Meter | nitriding-furnace-dissociation-meter | 1× | 1 | · | part |
| 3.7 | Gas Preheater | nitriding-furnace-gas-preheater | 1× | 1 | · | part |
| 4 | Plasma System 5 parts | nitriding-furnace-plasma-system | 1× | 1 | 6 | assembly |
| 4.1 | DC Power Supply | nitriding-furnace-dc-power-supply | 1× | 1 | · | part |
| 4.2 | Cathode Table | nitriding-furnace-cathode-table | 1× | 1 | · | part |
| 4.3 | Anode Shell | nitriding-furnace-anode-shell | 1× | 1 | · | part |
| 4.4 | HV Feedthrough | nitriding-furnace-hv-feedthrough | 2× | 2 | · | part |
| 4.5 | Arc Suppressor | nitriding-furnace-arc-suppressor | 1× | 1 | · | part |
| 5 | Vacuum System 6 parts | nitriding-furnace-vacuum | 1× | 1 | 13 | assembly |
| 5.1 | Vacuum Pump 4 parts | nitriding-furnace-vacuum-pump | 1× | 1 | 6 | assembly |
| 5.1.1 | Pump Rotor | nitriding-furnace-pump-rotor | 1× | 1 | · | part |
| 5.1.2 | Pump Motor | nitriding-furnace-pump-motor | 1× | 1 | · | part |
| 5.1.3 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 5.1.4 | Oil Seal | oil-seal | 2× | 2 | · | part |
| 5.2 | Exhaust Burner | nitriding-furnace-exhaust-burner | 1× | 1 | · | part |
| 5.3 | Scrubber | nitriding-furnace-scrubber | 1× | 1 | · | part |
| 5.4 | Vacuum Valve | nitriding-furnace-vacuum-valve | 2× | 2 | · | part |
| 5.5 | Pressure Sensor | pressure-sensor | 2× | 2 | · | part |
| 5.6 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 6 | Cooling System 5 parts | nitriding-furnace-cooling | 1× | 1 | 5 | assembly |
| 6.1 | Cooling Fan | nitriding-furnace-cooling-fan | 1× | 1 | · | part |
| 6.2 | Water Jacket | nitriding-furnace-water-jacket | 1× | 1 | · | part |
| 6.3 | Cooling Pump | nitriding-furnace-cooling-pump | 1× | 1 | · | part |
| 6.4 | Heat Exchanger | nitriding-furnace-heat-exchanger | 1× | 1 | · | part |
| 6.5 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 7 | Control System 9 parts | nitriding-furnace-control | 1× | 1 | 21 | assembly |
| 7.1 | Microcontroller | mcu | 1× | 1 | · | part |
| 7.2 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 7.3 | SMD Passive (R/C/L) | smd-passives | 1× | 1 | · | part |
| 7.4 | HMI Panel | nitriding-furnace-hmi-panel | 1× | 1 | · | part |
| 7.5 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 7.6 | Relay | relay | 6× | 6 | · | part |
| 7.7 | Power Supply | power-supply | 1× | 1 | · | part |
| 7.8 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 7.9 | Connector | connector | 8× | 8 | · | part |
| 8 | Frame and Handling 6 parts | nitriding-furnace-frame | 1× | 1 | 18 | assembly |
| 8.1 | Base Frame | nitriding-furnace-base-frame | 1× | 1 | · | part |
| 8.2 | Lid Hoist 4 parts | nitriding-furnace-lid-hoist | 1× | 1 | 5 | assembly |
| 8.2.1 | Hoist Motor | nitriding-furnace-hoist-motor | 1× | 1 | · | part |
| 8.2.2 | Ball Screw | ball-screw | 1× | 1 | · | part |
| 8.2.3 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 8.2.4 | Lift Frame | nitriding-furnace-lift-frame | 1× | 1 | · | part |
| 8.3 | Roller Cart | nitriding-furnace-roller-cart | 1× | 1 | · | part |
| 8.4 | Sheet Metal Panel | sheet-panel | 6× | 6 | · | part |
| 8.5 | Leveling Foot | nitriding-furnace-leveling-foot | 4× | 4 | · | part |
| 8.6 | Fastener Set | fastener-set | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Crankshaft Grinder
511 parts · shares 6 with this page
 Rotary-Table Surface Grinder
172 parts · shares 6 with this page
 Heat Treatment Furnace
299 parts · shares 5 with this page
 Profile Grinding Machine
815 parts · shares 4 with this page
 Aluminum Extrusion Press
365 parts · shares 4 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $10k–$1M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
|
🇩🇪DMG MORI
dmgmori.com ↗
|
Bielefeld, DE | Machine tools | 5 units | 12–20 wks |
|
🇯🇵Mazak
mazak.com ↗
|
Oguchi, JP | Machine tools | 5 units | 12–20 wks |
| haascnc.com ↗ | Oxnard, US | CNC machine tools | 5 units | 12–20 wks |
|
🇯🇵Okuma
okuma.com ↗
|
Niwa, JP | Machine tools | 5 units | 12–20 wks |
|
🇩🇪Trumpf
trumpf.com ↗
|
Ditzingen, DE | Laser & sheet-metal machines | 5 units | 12–20 wks |
958-word article