Hot Wire Foam Cutting Line
ProductOverview
A hot wire foam cutting line slices molded foam blocks into boards, sheets, and shaped parts by melting a thin path through the foam with electrically heated wire. There is no chip and no blade: a taut nichrome wire is held just above its softening temperature, and as the block feeds past it, the wire melts a narrow kerf and leaves a smooth sealed edge. The line takes the plain blocks from an EPS Block Molding Machine and converts them into the insulation board, packaging shapes, architectural mouldings, and pattern stock that customers buy. Cutting a block is faster and cleaner than sawing foam, which tears and sheds beads, and the melted edge needs no finishing.
A full line combines several cutting stations. The Line Frame and Table carries the block on a roller table, the Wire Carriage of vertical wires splits it into boards, the Horizontal Cutting Frame of horizontal wires sets sheet thickness, and a CNC Motion System gantry handles contour and tapered cuts. The Wire Power Supply heats the wires, Fume Extraction extraction cleans the air, and the Control System system runs it all.
How a hot wire cuts
The cut depends on resistance heating, not abrasion. The Cutting Wire is nichrome, an alloy chosen because its resistance stays steady as it heats and it does not oxidize away quickly. The Wire Power Supply pushes a large current through it at only a few volts, raising it to around 200 to 300 C, hot enough to melt the foam but not so hot it scorches or sags. The wire never touches solid plastic for long: it melts a thin gap just ahead of itself and glides through. Two things set the cut quality. One is wire temperature, held constant by the Current Control Board board so the wire does not cool in the cut and drag. The other is feed speed, set by the Block Feed System system: feed too fast and the wire bows and leaves a curved cut, feed too slow and the wire melts a wide kerf and wastes material.
Straight cuts: boards and sheets
Most production is plain rectangular stock. The Wire Carriage holds a bank of tensioned vertical Cutting Wire units spaced to the board width wanted, each kept taut by a Wire Tensioner and Coil Spring so it stays straight as it heats and lengthens. The block feeds through this bank and comes out split into parallel boards in one pass. The Horizontal Cutting Frame does the cross direction: a Lift Frame of horizontal Horizontal Wire units is set to a height by the Lift Screw and Lift Motor, so the same block can be sliced into sheets of any chosen thickness. Running both banks turns a block into a stack of identical sheets quickly.
Contour cutting
For shaped parts the line uses the CNC Motion System system. Here a single Contour Wire is held between two Gantry Tower towers, each driven on two axes by Servo Motor and Ball Screw hardware. Moving the two ends of the wire independently lets the line cut tapers, bevels, letters, cornice profiles, and swept shapes, because the wire can tilt and follow different paths at each end. This is how foam letters, architectural mouldings, packaging inserts, and sculpture blanks are produced. The Control System system runs the toolpath from a program, coordinating the four axes so the wire stays straight and the cut matches the drawing.
Power and fume control
Two support systems make the line work safely. The Wire Power Supply is built around a Step-Down Transformer that drops mains voltage to a few volts and a Thyristor Regulator that regulates current, with Current Sensor feedback so wire temperature holds even as a wire wears thin or the room temperature changes. The Fume Extraction system matters because melting polystyrene releases styrene vapor; a Capture Hood over the cutting zone, a Exhaust Fan, and a Carbon Filter of activated carbon capture and clean the fume before it reaches the operator.
Use and limits
Hot wire lines run in EPS and XPS plants downstream of the molding presses, in insulation board factories, in packaging converters, and in sign and display shops. Their strengths are clean sealed edges, no dust or torn beads, thin kerfs that waste little material, and the flexibility to cut both flat stock and complex contours from the same block. The limits follow from the melting cut: it only suits thermoplastic foams that melt cleanly, so it cannot cut polyurethane or mineral wool, which char or do not melt. The wire is consumable and must be re-tensioned and replaced as it thins, cut speed is modest because the wire can only melt so fast without bowing, and the fume must always be extracted. Within those limits it is the standard way to convert molded foam blocks into the finished sheets and shapes that the market actually uses.
Hot Wire Foam Cutting Line parts and their functions
8 top-level parts · 314 parts in total · full bill of materials below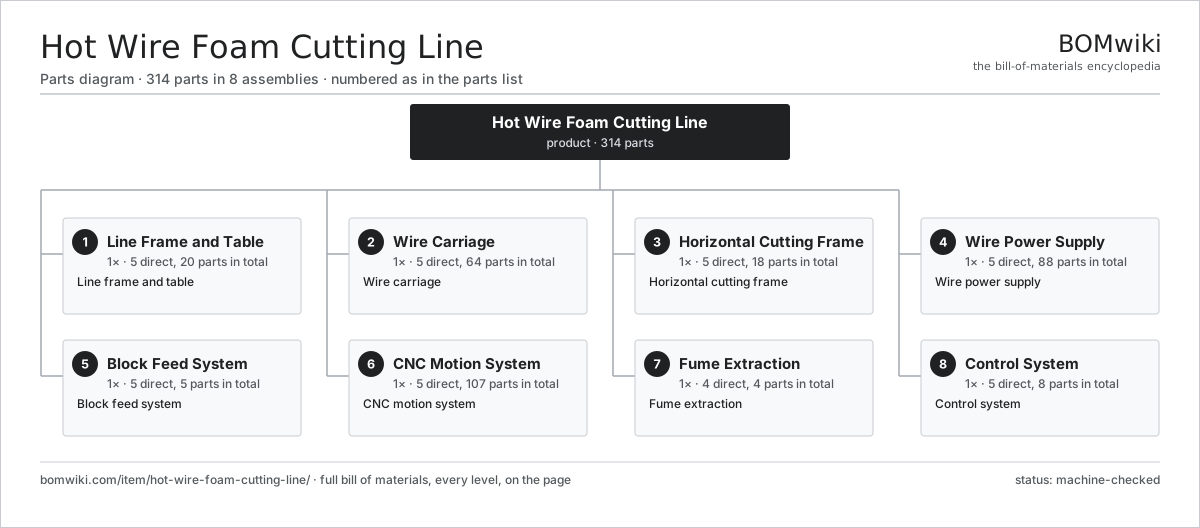
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Line Frame and Table 5 parts | 1× | Line frame and table |
| 2 | Wire Carriage 5 parts | 1× | Wire carriage |
| 3 | Horizontal Cutting Frame 5 parts | 1× | Horizontal cutting frame |
| 4 | Wire Power Supply 5 parts | 1× | Wire power supply |
| 5 | Block Feed System 5 parts | 1× | Block feed system |
| 6 | CNC Motion System 5 parts | 1× | CNC motion system |
| 7 | Fume Extraction 4 parts | 1× | Fume extraction |
| 8 | Control System 5 parts | 1× | Control system |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Hot Wire Foam Cutting Line
8 top-level lines · 54 rows shown · 314 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Line Frame and Table 5 parts | hot-wire-foam-cutting-line-frame | 1× | 1 | 20 | assembly |
| 1.1 | Base Frame | hot-wire-foam-cutting-line-base-frame | 1× | 1 | · | part |
| 1.2 | Roller Table | hot-wire-foam-cutting-line-roller-table | 1× | 1 | · | part |
| 1.3 | Side Rail | hot-wire-foam-cutting-line-side-rail | 2× | 2 | · | part |
| 1.4 | Table Roller | hot-wire-foam-cutting-line-table-roller | 12× | 12 | · | part |
| 1.5 | Fastener Set | fastener-set | 4× | 4 | · | part |
| 2 | Wire Carriage 5 parts | hot-wire-foam-cutting-line-wire-carriage | 1× | 1 | 64 | assembly |
| 2.1 | Carriage Beam | hot-wire-foam-cutting-line-carriage-beam | 2× | 2 | · | part |
| 2.2 | Cutting Wire | hot-wire-foam-cutting-line-cutting-wire | 20× | 20 | · | part |
| 2.3 | Wire Tensioner | hot-wire-foam-cutting-line-wire-tensioner | 20× | 20 | · | part |
| 2.4 | Coil Spring | coil-spring | 20× | 20 | · | part |
| 2.5 | Power Bus Bar | hot-wire-foam-cutting-line-bus-bar | 2× | 2 | · | part |
| 3 | Horizontal Cutting Frame 5 parts | hot-wire-foam-cutting-line-wire-frame | 1× | 1 | 18 | assembly |
| 3.1 | Lift Frame | hot-wire-foam-cutting-line-lift-frame | 1× | 1 | · | part |
| 3.2 | Horizontal Wire | hot-wire-foam-cutting-line-horizontal-wire | 12× | 12 | · | part |
| 3.3 | Lift Screw | hot-wire-foam-cutting-line-lift-screw | 2× | 2 | · | part |
| 3.4 | Lift Motor | hot-wire-foam-cutting-line-lift-motor | 1× | 1 | · | part |
| 3.5 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 4 | Wire Power Supply 5 parts | hot-wire-foam-cutting-line-power-supply | 1× | 1 | 88 | assembly |
| 4.1 | Step-Down Transformer | hot-wire-foam-cutting-line-transformer | 1× | 1 | · | part |
| 4.2 | Thyristor Regulator | hot-wire-foam-cutting-line-thyristor-pack | 1× | 1 | · | part |
| 4.3 | Current Control Board 3 parts | hot-wire-foam-cutting-line-current-control | 1× | 1 | 82 | assembly |
| 4.3.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 4.3.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 4.3.3 | SMD Passive (R/C/L) | smd-passives | 80× | 80 | · | part |
| 4.4 | Wire Contactor | hot-wire-foam-cutting-line-contactor | 2× | 2 | · | part |
| 4.5 | Current Sensor | current-sensor | 2× | 2 | · | part |
| 5 | Block Feed System 5 parts | hot-wire-foam-cutting-line-feed | 1× | 1 | 5 | assembly |
| 5.1 | Feed Belt | hot-wire-foam-cutting-line-feed-belt | 1× | 1 | · | part |
| 5.2 | Feed Motor | hot-wire-foam-cutting-line-feed-motor | 1× | 1 | · | part |
| 5.3 | Feed Gearbox | hot-wire-foam-cutting-line-feed-gearbox | 1× | 1 | · | part |
| 5.4 | Block Pusher | hot-wire-foam-cutting-line-pusher | 1× | 1 | · | part |
| 5.5 | Drive Belt | drive-belt | 1× | 1 | · | part |
| 6 | CNC Motion System 5 parts | hot-wire-foam-cutting-line-cnc | 1× | 1 | 107 | assembly |
| 6.1 | Gantry Tower | hot-wire-foam-cutting-line-gantry | 2× | 2 | · | part |
| 6.2 | Ball Screw | ball-screw | 4× | 4 | · | part |
| 6.3 | Servo Motor 4 parts | servo-motor | 4× | 4 | 24 | assembly |
| 6.3.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 4 | 3 | assembly |
| 6.3.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 4 | 19 | assembly |
| 6.3.3 | Encoder | encoder | 1× | 4 | · | part |
| 6.3.4 | Motor Housing | motor-housing | 1× | 4 | · | part |
| 6.4 | Linear Guide Rail | linear-guide | 4× | 4 | · | part |
| 6.5 | Contour Wire | hot-wire-foam-cutting-line-contour-wire | 1× | 1 | · | part |
| 7 | Fume Extraction 4 parts | hot-wire-foam-cutting-line-fume | 1× | 1 | 4 | assembly |
| 7.1 | Capture Hood | hot-wire-foam-cutting-line-hood | 1× | 1 | · | part |
| 7.2 | Exhaust Fan | hot-wire-foam-cutting-line-exhaust-fan | 1× | 1 | · | part |
| 7.3 | Carbon Filter | hot-wire-foam-cutting-line-filter | 1× | 1 | · | part |
| 7.4 | Ductwork | hot-wire-foam-cutting-line-duct | 1× | 1 | · | part |
| 8 | Control System 5 parts | hot-wire-foam-cutting-line-control | 1× | 1 | 8 | assembly |
| 8.1 | Motion Controller | hot-wire-foam-cutting-line-controller | 1× | 1 | · | part |
| 8.2 | Operator Panel | hot-wire-foam-cutting-line-hmi | 1× | 1 | · | part |
| 8.3 | Power Supply | power-supply | 1× | 1 | · | part |
| 8.4 | Servo Drive | hot-wire-foam-cutting-line-servo-drive | 4× | 4 | · | part |
| 8.5 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Electric Arc Furnace
1,462 parts · shares 16 with this page
 Ladle Refining Furnace
554 parts · shares 16 with this page
Automated Paint Spray Line
2,003 parts · shares 20 with this page
Powder Coating Line
5,418 parts · shares 20 with this page
 Rubber Extrusion Line
524 parts · shares 20 with this page
 Tensile Testing Machine
608 parts · shares 20 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $5k–$2M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| atlascopco.com ↗ | Stockholm, SE | Compressors & industrial | 10 units | 12–20 wks |
|
🇦🇹Andritz
andritz.com ↗
|
Graz, AT | Process plants & machinery | 10 units | 12–20 wks |
| buhlergroup.com ↗ | Uzwil, CH | Food & materials processing | 10 units | 12–20 wks |
| gea.com ↗ | Düsseldorf, DE | Process technology | 10 units | 12–20 wks |
| mhi.com ↗ | Tokyo, JP | Heavy machinery | 10 units | 12–20 wks |
944-word article