Low-Pressure Die Casting Machine
ProductOverview
A low-pressure die casting machine fills a permanent steel mould from below by gently pressurising a sealed bath of molten metal. The mould sits directly above the furnace, connected by a vertical stalk tube that dips into the melt. When low gas pressure, typically 0.2 to 1.0 bar, is applied to the sealed furnace chamber, it pushes metal up the stalk and into the die cavity against gravity. Because the metal rises slowly and smoothly rather than being shot in at high velocity, the fill is calm and free of the air entrapment that plagues high-pressure die casting. The result is dense, sound castings with good mechanical properties, which is why the process dominates production of aluminium automotive wheels, cylinder heads and structural suspension parts.
The machine is organised around the Pressurised Holding Furnace, which holds and pressurises the metal, the Die Platen and Clamp, which carries and clamps the mould, the Pressure Control System, which shapes the fill, and the Stalk and Riser stalk that links bath to die.
How low-pressure filling works
The Pressurised Holding Furnace is a sealed pressure vessel. A Furnace Lid Seal keeps gas pressure inside, and a Furnace Relief Valve valve guards against overpressure. To fill, the Pressure Control System admits inert gas through a Proportional Pressure Valve, raising chamber pressure on a programmed curve. Metal rises through the Stalk Tube and the Sprue Bush into the cavity. The pressure ramp has distinct stages: a slow rise to bring metal up the stalk, a controlled fill of the cavity, then a higher holding pressure that feeds the casting as it shrinks during solidification. Holding pressure on the liquid metal directly into the freezing cavity is what gives low-pressure castings their density, because shrinkage porosity is fed from below instead of being left as voids. When solidification is complete the Vent Valve drops chamber pressure and unfilled metal in the stalk falls back into the bath for the next cast.
Furnace and metal handling
Inside the Furnace Shell a refractory Furnace Lining holds the bath, kept at 680 to 730 degrees Celsius by Heating Element units and read by Bath Thermocouple probes. Holding temperature is critical: too cold and the metal misruns, too hot and grain structure coarsens and die life shortens. The sealed chamber also blankets the melt and suppresses oxidation. The Stalk Heater keeps the stalk metal liquid between casts so the riser never freezes shut.
Die, platen and clamp
The die mounts between a fixed Lower Platen over the furnace and a moving Upper Platen running on four Tie Bar columns. A Clamp Cylinder holds the Permanent Die Set closed against the fill pressure and the weight of metal. The die itself is a machined permanent steel mould, unlike sand casting where the mould is destroyed each time, so it produces thousands of castings with consistent dimensions. After solidification the platen opens and the Ejection System system drives an Ejector Plate and its Ejector Pin array to push the casting clear onto the Casting Takeout.
Die temperature control
Casting quality and cycle time both depend on holding the die in a stable thermal window. The Die Temperature System system runs water and oil through a Cooling Water Manifold to individual die zones, each trimmed by a Zone Flow Valve and monitored by a Die Thermocouple. Thick sections that solidify slowly get extra cooling, including Air Blast Cooling jets, so the whole casting freezes in a directional pattern from the far reaches back toward the feeding sprue. A Temperature Control Unit preheats the die at startup and holds its baseline temperature.
Control and automation
The Control Panel runs the cast cycle through its Machine PLC, storing a recipe for each part: pressure curve, hold time, die temperatures and ejection timing. Servo drives position the platen and ejector smoothly and repeatably. The operator sets up a job from a stored recipe and the machine then runs autonomously, often integrated with a downstream trim press, X-ray inspection and quench line.
Applications
Low-pressure die casting is the standard route for aluminium automotive road wheels, where it gives the strength and consistency that safety-critical parts demand, and for engine cylinder heads, intake manifolds and chassis components. Compared with gravity casting it gives higher yield and better feeding of shrinkage; compared with high-pressure die casting it gives sounder, heat-treatable castings at the cost of longer cycle time. The process suits medium-volume production of medium to large aluminium and magnesium parts where mechanical integrity outweighs raw output rate.
Low-Pressure Die Casting Machine parts and their functions
8 top-level parts · 97 parts in total · full bill of materials below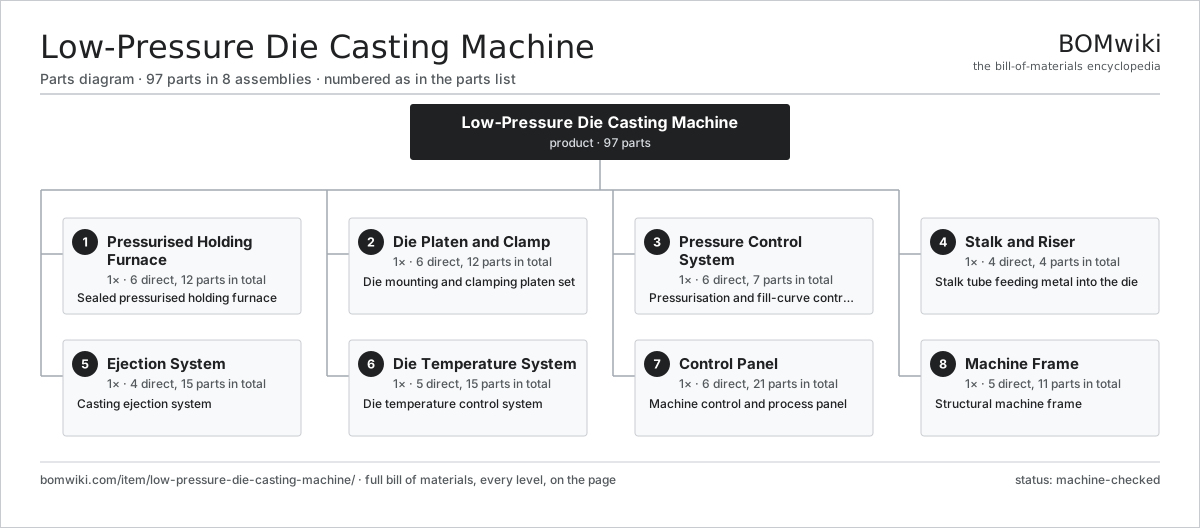
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Pressurised Holding Furnace 6 parts | 1× | Sealed pressurised holding furnace |
| 2 | Die Platen and Clamp 6 parts | 1× | Die mounting and clamping platen set |
| 3 | Pressure Control System 6 parts | 1× | Pressurisation and fill-curve control |
| 4 | Stalk and Riser 4 parts | 1× | Stalk tube feeding metal into the die |
| 5 | Ejection System 4 parts | 1× | Casting ejection system |
| 6 | Die Temperature System 5 parts | 1× | Die temperature control system |
| 7 | Control Panel 6 parts | 1× | Machine control and process panel |
| 8 | Machine Frame 5 parts | 1× | Structural machine frame |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Low-Pressure Die Casting Machine
8 top-level lines · 50 rows shown · 97 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Pressurised Holding Furnace 6 parts | low-pressure-die-casting-machine-furnace | 1× | 1 | 12 | assembly |
| 1.1 | Furnace Shell | low-pressure-die-casting-machine-furnace-shell | 1× | 1 | · | part |
| 1.2 | Furnace Lining | low-pressure-die-casting-machine-furnace-lining | 1× | 1 | · | part |
| 1.3 | Heating Element | heating-element | 6× | 6 | · | part |
| 1.4 | Furnace Lid Seal | low-pressure-die-casting-machine-furnace-lid-seal | 1× | 1 | · | part |
| 1.5 | Bath Thermocouple | low-pressure-die-casting-machine-bath-thermocouple | 2× | 2 | · | part |
| 1.6 | Furnace Relief Valve | low-pressure-die-casting-machine-furnace-relief | 1× | 1 | · | part |
| 2 | Die Platen and Clamp 6 parts | low-pressure-die-casting-machine-die-platen | 1× | 1 | 12 | assembly |
| 2.1 | Lower Platen | low-pressure-die-casting-machine-lower-platen | 1× | 1 | · | part |
| 2.2 | Upper Platen | low-pressure-die-casting-machine-upper-platen | 1× | 1 | · | part |
| 2.3 | Tie Bar | low-pressure-die-casting-machine-tie-bar | 4× | 4 | · | part |
| 2.4 | Clamp Cylinder | low-pressure-die-casting-machine-clamp-cylinder | 1× | 1 | · | part |
| 2.5 | Linear Guide Rail | linear-guide | 4× | 4 | · | part |
| 2.6 | Permanent Die Set | low-pressure-die-casting-machine-die-set | 1× | 1 | · | part |
| 3 | Pressure Control System 6 parts | low-pressure-die-casting-machine-pressure-control | 1× | 1 | 7 | assembly |
| 3.1 | Proportional Pressure Valve | low-pressure-die-casting-machine-proportional-valve | 1× | 1 | · | part |
| 3.2 | Pressure Sensor | pressure-sensor | 2× | 2 | · | part |
| 3.3 | Gas Regulator | low-pressure-die-casting-machine-gas-regulator | 1× | 1 | · | part |
| 3.4 | Vent Valve | low-pressure-die-casting-machine-vent-valve | 1× | 1 | · | part |
| 3.5 | Microcontroller | mcu | 1× | 1 | · | part |
| 3.6 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 4 | Stalk and Riser 4 parts | low-pressure-die-casting-machine-riser | 1× | 1 | 4 | assembly |
| 4.1 | Stalk Tube | low-pressure-die-casting-machine-stalk-tube | 1× | 1 | · | part |
| 4.2 | Sprue Bush | low-pressure-die-casting-machine-sprue-bush | 1× | 1 | · | part |
| 4.3 | Stalk Seal | low-pressure-die-casting-machine-stalk-seal | 1× | 1 | · | part |
| 4.4 | Stalk Heater | low-pressure-die-casting-machine-stalk-heater | 1× | 1 | · | part |
| 5 | Ejection System 4 parts | low-pressure-die-casting-machine-ejection | 1× | 1 | 15 | assembly |
| 5.1 | Ejector Plate | low-pressure-die-casting-machine-ejector-plate | 1× | 1 | · | part |
| 5.2 | Ejector Pin | low-pressure-die-casting-machine-ejector-pin | 12× | 12 | · | part |
| 5.3 | Ejector Cylinder | low-pressure-die-casting-machine-ejector-cylinder | 1× | 1 | · | part |
| 5.4 | Casting Takeout | low-pressure-die-casting-machine-takeout | 1× | 1 | · | part |
| 6 | Die Temperature System 5 parts | low-pressure-die-casting-machine-cooling | 1× | 1 | 15 | assembly |
| 6.1 | Cooling Water Manifold | low-pressure-die-casting-machine-water-manifold | 1× | 1 | · | part |
| 6.2 | Zone Flow Valve | low-pressure-die-casting-machine-flow-valve | 6× | 6 | · | part |
| 6.3 | Die Thermocouple | low-pressure-die-casting-machine-die-thermocouple | 6× | 6 | · | part |
| 6.4 | Air Blast Cooling | low-pressure-die-casting-machine-air-blast | 1× | 1 | · | part |
| 6.5 | Temperature Control Unit | low-pressure-die-casting-machine-temp-unit | 1× | 1 | · | part |
| 7 | Control Panel 6 parts | low-pressure-die-casting-machine-control-panel | 1× | 1 | 21 | assembly |
| 7.1 | Machine PLC | low-pressure-die-casting-machine-plc | 1× | 1 | · | part |
| 7.2 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 7.3 | Relay | relay | 8× | 8 | · | part |
| 7.4 | Connector | connector | 8× | 8 | · | part |
| 7.5 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 7.6 | Servo Drive | low-pressure-die-casting-machine-servo-drive | 2× | 2 | · | part |
| 8 | Machine Frame 5 parts | low-pressure-die-casting-machine-frame | 1× | 1 | 11 | assembly |
| 8.1 | Base Frame | low-pressure-die-casting-machine-base-frame | 1× | 1 | · | part |
| 8.2 | Support Column | low-pressure-die-casting-machine-column | 4× | 4 | · | part |
| 8.3 | Hydraulic Power Pack | low-pressure-die-casting-machine-hydraulic-pack | 1× | 1 | · | part |
| 8.4 | Sheet Metal Panel | sheet-panel | 4× | 4 | · | part |
| 8.5 | O-Ring Set | oring-set | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Industrial Ultrasonic Cleaner
787 parts · shares 9 with this page
Micro Injection Molding Machine
704 parts · shares 9 with this page
 Thermal Spray Coating System
866 parts · shares 9 with this page
Wax Pattern Injection Press
107 parts · shares 9 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $5k–$2M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| atlascopco.com ↗ | Stockholm, SE | Compressors & industrial | 10 units | 12–20 wks |
|
🇦🇹Andritz
andritz.com ↗
|
Graz, AT | Process plants & machinery | 10 units | 12–20 wks |
| buhlergroup.com ↗ | Uzwil, CH | Food & materials processing | 10 units | 12–20 wks |
| gea.com ↗ | Düsseldorf, DE | Process technology | 10 units | 12–20 wks |
| mhi.com ↗ | Tokyo, JP | Heavy machinery | 10 units | 12–20 wks |
905-word article