EPS Block Molding Machine
ProductOverview
An EPS block molding machine makes one large rectangular block of expanded polystyrene foam at a time, which is then aged and sliced into sheets, shapes, or custom parts on a separate cutting line. It works on the same steam principle as shape molding, but instead of forming a finished part it produces a plain block, typically about a cubic metre in cross section and several metres long. Blocks are the raw stock for insulation board, geofoam fill, lost-foam casting patterns, craft and display shapes, and packaging that is cut to order. Making one big block and cutting it is cheaper per cubic metre than molding each part, so block plants feed the volume end of the EPS market.
The cycle is fill, steam, vacuum, cool, and discharge. The Machine Frame carries the large Block Mold Box, the Bead Fill System charges it with beads, the Steam System fuses them, the Vacuum and Cooling System cools and dries the block, and the Block Tilt and Discharge mechanism tips it out. A Control System system sequences the whole run.
The mold box
The Block Mold Box is the defining part. It is a large rectangular chest with vented steel walls; each Mold Side Wall, the Mold Floor, and the Mold Lid is pierced with hundreds of Vent Plug inserts that pass steam but hold beads in. Behind each wall sits a Steam Plenum that spreads steam evenly across the face, so the block fuses uniformly rather than just at the edges. Because the box is large, the Side Clamping System system uses several Clamp Cylinder units and Clamp Hook latches to hold the walls shut against the steam pressure that builds inside.
Filling
The Bead Fill System fills the box evenly, which is the key to a uniform-density block. Aged beads flow from the Bead Silo through a Rotary Feed Valve airlock into conveying air, and several Fill Injector guns blow them into the box from spread-out points so the box packs without low-density pockets. The Fill Blower supplies the air. Bead age matters here: freshly expanded beads still hold too much pressure and shrink later, so they are aged in the silo for hours to days before molding, which lets them stabilize and take up air for a clean fuse.
Steaming and fusing
Fusing a block this size needs steam driven through the whole bead bed, not just at the surface. The Steam System feeds the plenums from a Steam Header through Steam Valve units in a programmed order: first a cross-steam step that pushes steam in one wall and out the opposite plenum, purging air and condensate, then a through-steam and autoclave step that brings the whole block up to fusing temperature at once. Steam pressure runs around 0.8 to 1.6 bar gauge, watched by Pressure Sensor units on each plenum. Condensate Drain and Steam Trap hardware clear water so cold spots do not leave unfused cores in the centre of the block.
Vacuum, cooling, and discharge
A large block stores a lot of heat and water, so cooling is the longest part of the cycle. The Vacuum and Cooling System pulls vacuum with a Vacuum Pump backed by a Vacuum Receiver Tank receiver so the box can be evacuated quickly. The vacuum flash-boils residual water to carry heat out and lowers the internal pressure that would otherwise swell the block after molding. Cooling Spray Bar bars wet the plenum backs to pull heat through the walls. Once the block is firm and stable the Block Tilt and Discharge mechanism opens a face, the Tilt Cylinder units rotate the box, and the Push Plate ejects the block onto a conveyor that carries it to aging racks before cutting.
Control, downstream, and use
The Control System system runs the long fill-steam-cool cycle, sequencing the steam valves, vacuum, and cooling through a Pneumatic Valve Bank under a PLC, with recipes stored on the Operator Panel. The molded block is not the finished product: after aging to release residual moisture and pressure, it goes to a Hot Wire Foam Cutting Line that slices it into boards and shapes with heated wires. Block plants supply insulation board makers, civil engineering geofoam projects, casting foundries, and packaging converters. The strengths of block molding are low cost per cubic metre, simple plain-shape tooling, and high output; the limits are the steam and vacuum utilities required, the aging time before cutting, and the need for very even fill and steaming to avoid soft cores in a block too big to inspect from outside.
EPS Block Molding Machine parts and their functions
8 top-level parts · 305 parts in total · full bill of materials below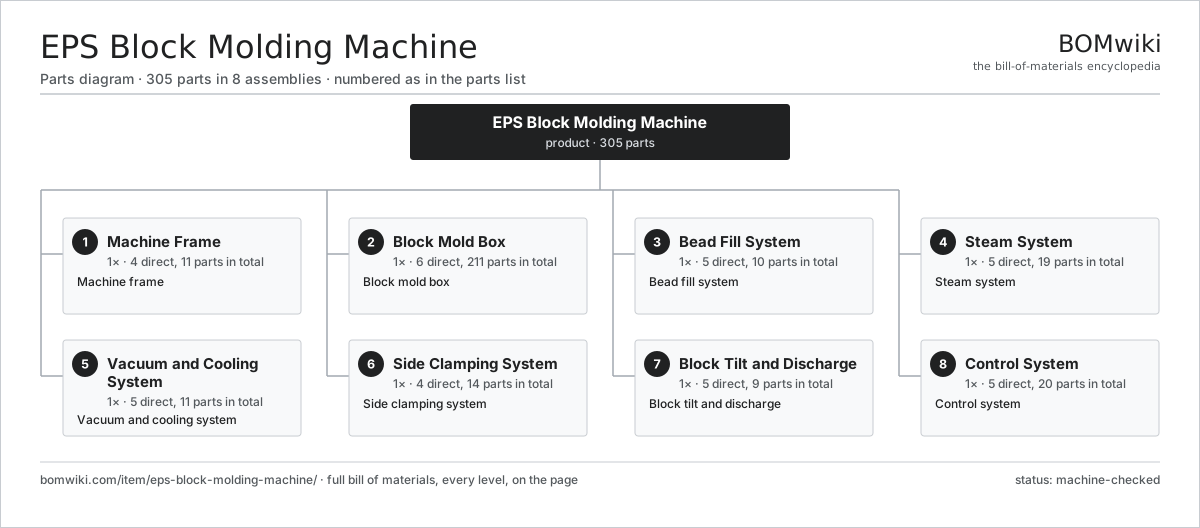
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Machine Frame 4 parts | 1× | Machine frame |
| 2 | Block Mold Box 6 parts | 1× | Block mold box |
| 3 | Bead Fill System 5 parts | 1× | Bead fill system |
| 4 | Steam System 5 parts | 1× | Steam system |
| 5 | Vacuum and Cooling System 5 parts | 1× | Vacuum and cooling system |
| 6 | Side Clamping System 4 parts | 1× | Side clamping system |
| 7 | Block Tilt and Discharge 5 parts | 1× | Block tilt and discharge |
| 8 | Control System 5 parts | 1× | Control system |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for EPS Block Molding Machine
8 top-level lines · 47 rows shown · 305 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Machine Frame 4 parts | eps-block-molding-machine-frame | 1× | 1 | 11 | assembly |
| 1.1 | Base Frame | eps-block-molding-machine-base-frame | 1× | 1 | · | part |
| 1.2 | Side Column | eps-block-molding-machine-side-column | 4× | 4 | · | part |
| 1.3 | Top Beam | eps-block-molding-machine-top-beam | 2× | 2 | · | part |
| 1.4 | Fastener Set | fastener-set | 4× | 4 | · | part |
| 2 | Block Mold Box 6 parts | eps-block-molding-machine-mold-box | 1× | 1 | 211 | assembly |
| 2.1 | Mold Side Wall | eps-block-molding-machine-mold-wall | 4× | 4 | · | part |
| 2.2 | Mold Floor | eps-block-molding-machine-mold-floor | 1× | 1 | · | part |
| 2.3 | Mold Lid | eps-block-molding-machine-mold-lid | 1× | 1 | · | part |
| 2.4 | Vent Plug | eps-block-molding-machine-vent-plug | 200× | 200 | · | part |
| 2.5 | Steam Plenum | eps-block-molding-machine-steam-plenum | 4× | 4 | · | part |
| 2.6 | Box Gasket | eps-block-molding-machine-box-gasket | 1× | 1 | · | part |
| 3 | Bead Fill System 5 parts | eps-block-molding-machine-fill-system | 1× | 1 | 10 | assembly |
| 3.1 | Bead Silo | eps-block-molding-machine-bead-silo | 1× | 1 | · | part |
| 3.2 | Fill Injector | eps-block-molding-machine-fill-injector | 6× | 6 | · | part |
| 3.3 | Fill Blower | eps-block-molding-machine-fill-blower | 1× | 1 | · | part |
| 3.4 | Rotary Feed Valve | eps-block-molding-machine-rotary-valve | 1× | 1 | · | part |
| 3.5 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 4 | Steam System 5 parts | eps-block-molding-machine-steam-system | 1× | 1 | 19 | assembly |
| 4.1 | Steam Header | eps-block-molding-machine-steam-header | 1× | 1 | · | part |
| 4.2 | Steam Valve | eps-block-molding-machine-steam-valve | 6× | 6 | · | part |
| 4.3 | Condensate Drain | eps-block-molding-machine-condensate-drain | 4× | 4 | · | part |
| 4.4 | Steam Trap | eps-block-molding-machine-steam-trap | 4× | 4 | · | part |
| 4.5 | Pressure Sensor | pressure-sensor | 4× | 4 | · | part |
| 5 | Vacuum and Cooling System 5 parts | eps-block-molding-machine-vacuum-system | 1× | 1 | 11 | assembly |
| 5.1 | Vacuum Pump | eps-block-molding-machine-vacuum-pump | 1× | 1 | · | part |
| 5.2 | Vacuum Receiver Tank | eps-block-molding-machine-vacuum-tank | 1× | 1 | · | part |
| 5.3 | Cooling Spray Bar | eps-block-molding-machine-cool-spray | 4× | 4 | · | part |
| 5.4 | Cooling Water Pump | eps-block-molding-machine-cool-pump | 1× | 1 | · | part |
| 5.5 | Vacuum Valve | eps-block-molding-machine-vacuum-valve | 4× | 4 | · | part |
| 6 | Side Clamping System 4 parts | eps-block-molding-machine-clamp | 1× | 1 | 14 | assembly |
| 6.1 | Clamp Cylinder | eps-block-molding-machine-clamp-cylinder | 4× | 4 | · | part |
| 6.2 | Clamp Valve | eps-block-molding-machine-clamp-valve | 2× | 2 | · | part |
| 6.3 | Clamp Hook | eps-block-molding-machine-clamp-hook | 4× | 4 | · | part |
| 6.4 | O-Ring Set | oring-set | 4× | 4 | · | part |
| 7 | Block Tilt and Discharge 5 parts | eps-block-molding-machine-tilt | 1× | 1 | 9 | assembly |
| 7.1 | Tilt Frame | eps-block-molding-machine-tilt-frame | 1× | 1 | · | part |
| 7.2 | Tilt Cylinder | eps-block-molding-machine-tilt-cylinder | 2× | 2 | · | part |
| 7.3 | Push Plate | eps-block-molding-machine-push-plate | 1× | 1 | · | part |
| 7.4 | Push Cylinder | eps-block-molding-machine-push-cylinder | 1× | 1 | · | part |
| 7.5 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 8 | Control System 5 parts | eps-block-molding-machine-control | 1× | 1 | 20 | assembly |
| 8.1 | PLC | eps-block-molding-machine-plc | 1× | 1 | · | part |
| 8.2 | Operator Panel | eps-block-molding-machine-hmi | 1× | 1 | · | part |
| 8.3 | Power Supply | power-supply | 1× | 1 | · | part |
| 8.4 | Relay | relay | 16× | 16 | · | part |
| 8.5 | Pneumatic Valve Bank | eps-block-molding-machine-valve-bank | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Continuous Galvanizing Line
1,296 parts · shares 5 with this page
 Dynamic Balancing Machine
573 parts · shares 5 with this page
Electrocoating Line
2,977 parts · shares 5 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $5k–$2M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| atlascopco.com ↗ | Stockholm, SE | Compressors & industrial | 10 units | 12–20 wks |
|
🇦🇹Andritz
andritz.com ↗
|
Graz, AT | Process plants & machinery | 10 units | 12–20 wks |
| buhlergroup.com ↗ | Uzwil, CH | Food & materials processing | 10 units | 12–20 wks |
| gea.com ↗ | Düsseldorf, DE | Process technology | 10 units | 12–20 wks |
| mhi.com ↗ | Tokyo, JP | Heavy machinery | 10 units | 12–20 wks |
893-word article