Gravity Die Casting Machine
ProductOverview
A gravity die casting machine pours molten metal into a reusable steel mould and lets gravity fill the cavity. Unlike sand casting, where a new mould is broken away from every part, the die is a machined permanent mould that produces thousands of castings. Unlike pressure die casting, no external force drives the metal; the head of liquid in the pour basin does the filling. Modern machines mount the die on a tilting table so the closed mould starts nearly horizontal at the moment of pouring and then rotates slowly upright, letting the metal climb the cavity walls in a smooth wave rather than splashing down a tall sprue. This controlled tilt pour gives clean, low-turbulence filling, which produces dense, fine-grained castings suited to heat treatment.
The machine is built from a Tilting Table that rolls the die through the pour, a Die Carrier that opens and closes the mould, a Core Pull System system for internal features, an Ejection System system, and a Die Thermal System that keeps the die in its working temperature window.
How tilt pouring works
At the start of a cycle the closed die lies tilted so the Pour Basin near the Tilt Carrier Frame pivot can receive the full charge of metal at low height. The operator or an automatic ladle fills the basin, then the Tilt Actuator, usually driven through a Servo Motor for a programmable rate, rotates the table upright. As the die turns, metal flows from the basin through the runner and rises gently into the cavity. A slow, controlled tilt rate keeps the metal front laminar and avoids folding oxide skins into the casting, which is the main cause of weakness in aluminium castings. The rate is part of the stored recipe and is tuned per part.
Die carrier and clamping
The permanent die mounts between a Fixed Platen and a Moving Platen running on Linear Guide Rail rails. A Die Close Cylinder closes and locks the Permanent Die Set before pouring, holding it shut against the metal head and any side pressure. Because gravity casting does not pressurise the metal, clamp force is far lower than in pressure die casting, in the range of 50 to 400 kilonewtons, enough to keep the parting line tight. Two Side Slide units form undercut side features and retract before the die opens.
Cores and ejection
Many gravity castings have internal passages formed by cores. The Core Pull System system uses hydraulic Core Pull Cylinder units to set metal cores into the cavity before pouring and withdraw them once the casting has solidified, with a Core Position Switch confirming each position. Sand cores, used for complex internal shapes, are placed by hand or robot and shaken out after casting. Once cores are clear and the die opens, the Ejection System system drives an Ejector Plate and its Ejector Pin array to lift the casting free, with Ejector Return Spring units resetting the plate.
Thermal management
A permanent die must run hot enough to fill thin sections and cool enough to freeze the casting in a reasonable cycle. At startup a Die Preheat Burner burner brings the cold die up to 200 to 350 degrees Celsius. During production the Die Thermal System runs water through a Cooling Water Manifold to individual zones, each trimmed by a Zone Flow Valve and watched by a Die Thermocouple, with Air Cooling Jet cooling on thick sections. Balanced cooling drives directional solidification toward the feeder so shrinkage porosity ends up in the riser, not the part.
Hydraulics and control
The Hydraulic Power Unit supplies all cylinders through a Hydraulic Valve Block, with an Hydraulic Oil Cooler holding oil temperature steady. The Control Panel runs the cycle from its Machine PLC: die close, core set, tilt pour at the programmed rate, dwell for solidification, tilt back, core pull, die open and eject. Each part has a stored recipe, and a Safety Light Curtain guards the operator side.
Applications
Gravity die casting suits medium-volume aluminium parts that need good mechanical properties and dimensional consistency: cylinder heads, pistons, pump and valve bodies, gearbox housings, cookware and lighting bodies. It also casts copper alloys and zinc. Compared with sand casting it gives a better surface, tighter tolerances and finer grain; compared with pressure die casting it gives sounder, heat-treatable castings with lower tooling cost, at lower output rate. The tilt-pour layout is the standard configuration where casting integrity is the priority over cycle speed.
Maintenance and tooling life
The permanent die is the costly, wearing asset and its life sets the economics of the process. Repeated thermal cycling between the molten metal and the cooling water raises a network of fine heat-checking cracks on the cavity surface, and these eventually print onto the casting and force a die refurbishment or replacement. A protective die coating, sprayed on between casts, both insulates the surface and eases release, and reapplying it correctly is a daily task that strongly affects both die life and casting finish. Ejector pins, side slides and core slides are the moving wear points and are lubricated and inspected on a regular cycle. The hydraulic oil is filtered and its temperature held steady, because contaminated or hot oil degrades the proportional valves that control tilt rate, and an inconsistent tilt rate directly shows up as variable casting soundness from one part to the next.
Gravity Die Casting Machine parts and their functions
8 top-level parts · 120 parts in total · full bill of materials below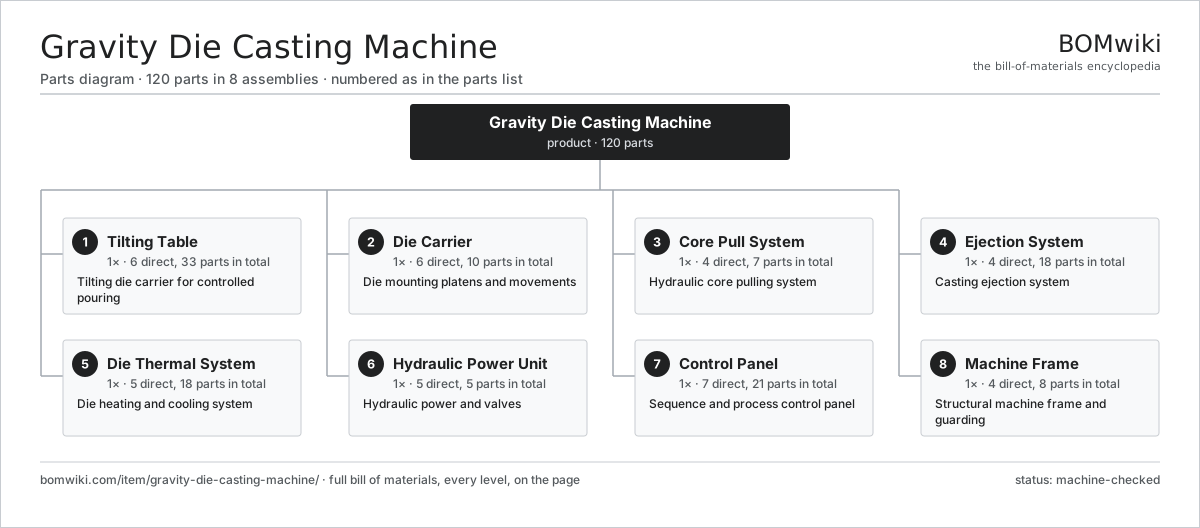
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Tilting Table 6 parts | 1× | Tilting die carrier for controlled pouring |
| 2 | Die Carrier 6 parts | 1× | Die mounting platens and movements |
| 3 | Core Pull System 4 parts | 1× | Hydraulic core pulling system |
| 4 | Ejection System 4 parts | 1× | Casting ejection system |
| 5 | Die Thermal System 5 parts | 1× | Die heating and cooling system |
| 6 | Hydraulic Power Unit 5 parts | 1× | Hydraulic power and valves |
| 7 | Control Panel 7 parts | 1× | Sequence and process control panel |
| 8 | Machine Frame 4 parts | 1× | Structural machine frame and guarding |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Gravity Die Casting Machine
8 top-level lines · 53 rows shown · 120 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Tilting Table 6 parts | gravity-die-casting-machine-tilt-table | 1× | 1 | 33 | assembly |
| 1.1 | Tilt Carrier Frame | gravity-die-casting-machine-tilt-frame | 1× | 1 | · | part |
| 1.2 | Tilt Pivot Bearing | gravity-die-casting-machine-tilt-pivot | 2× | 2 | · | part |
| 1.3 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 1.4 | Tilt Actuator | gravity-die-casting-machine-tilt-cylinder | 1× | 1 | · | part |
| 1.5 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 1.5.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 1.5.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 1.5.3 | Encoder | encoder | 1× | 1 | · | part |
| 1.5.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 1.6 | Pour Basin | gravity-die-casting-machine-pour-basin | 1× | 1 | · | part |
| 2 | Die Carrier 6 parts | gravity-die-casting-machine-die-carrier | 1× | 1 | 10 | assembly |
| 2.1 | Fixed Platen | gravity-die-casting-machine-fixed-platen | 1× | 1 | · | part |
| 2.2 | Moving Platen | gravity-die-casting-machine-moving-platen | 1× | 1 | · | part |
| 2.3 | Die Close Cylinder | gravity-die-casting-machine-close-cylinder | 1× | 1 | · | part |
| 2.4 | Linear Guide Rail | linear-guide | 4× | 4 | · | part |
| 2.5 | Permanent Die Set | gravity-die-casting-machine-die-set | 1× | 1 | · | part |
| 2.6 | Side Slide | gravity-die-casting-machine-side-slide | 2× | 2 | · | part |
| 3 | Core Pull System 4 parts | gravity-die-casting-machine-core-pull | 1× | 1 | 7 | assembly |
| 3.1 | Core Pull Cylinder | gravity-die-casting-machine-core-cylinder | 2× | 2 | · | part |
| 3.2 | Core Slide | gravity-die-casting-machine-core-slide | 2× | 2 | · | part |
| 3.3 | Core Position Switch | gravity-die-casting-machine-core-position-switch | 2× | 2 | · | part |
| 3.4 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 4 | Ejection System 4 parts | gravity-die-casting-machine-ejection | 1× | 1 | 18 | assembly |
| 4.1 | Ejector Plate | gravity-die-casting-machine-ejector-plate | 1× | 1 | · | part |
| 4.2 | Ejector Pin | gravity-die-casting-machine-ejector-pin | 12× | 12 | · | part |
| 4.3 | Ejector Cylinder | gravity-die-casting-machine-ejector-cylinder | 1× | 1 | · | part |
| 4.4 | Ejector Return Spring | gravity-die-casting-machine-return-spring | 4× | 4 | · | part |
| 5 | Die Thermal System 5 parts | gravity-die-casting-machine-thermal-system | 1× | 1 | 18 | assembly |
| 5.1 | Die Preheat Burner | gravity-die-casting-machine-gas-preheater | 1× | 1 | · | part |
| 5.2 | Cooling Water Manifold | gravity-die-casting-machine-water-manifold | 1× | 1 | · | part |
| 5.3 | Zone Flow Valve | gravity-die-casting-machine-flow-valve | 6× | 6 | · | part |
| 5.4 | Die Thermocouple | gravity-die-casting-machine-die-thermocouple | 6× | 6 | · | part |
| 5.5 | Air Cooling Jet | gravity-die-casting-machine-air-jet | 4× | 4 | · | part |
| 6 | Hydraulic Power Unit 5 parts | gravity-die-casting-machine-hydraulic-unit | 1× | 1 | 5 | assembly |
| 6.1 | Hydraulic Pump | gravity-die-casting-machine-hyd-pump | 1× | 1 | · | part |
| 6.2 | Hydraulic Motor | gravity-die-casting-machine-hyd-motor | 1× | 1 | · | part |
| 6.3 | Hydraulic Reservoir | gravity-die-casting-machine-hyd-reservoir | 1× | 1 | · | part |
| 6.4 | Hydraulic Valve Block | gravity-die-casting-machine-valve-block | 1× | 1 | · | part |
| 6.5 | Hydraulic Oil Cooler | gravity-die-casting-machine-oil-cooler | 1× | 1 | · | part |
| 7 | Control Panel 7 parts | gravity-die-casting-machine-control-panel | 1× | 1 | 21 | assembly |
| 7.1 | Machine PLC | gravity-die-casting-machine-plc | 1× | 1 | · | part |
| 7.2 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 7.3 | Relay | relay | 8× | 8 | · | part |
| 7.4 | Connector | connector | 8× | 8 | · | part |
| 7.5 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 7.6 | Microcontroller | mcu | 1× | 1 | · | part |
| 7.7 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8 | Machine Frame 4 parts | gravity-die-casting-machine-frame | 1× | 1 | 8 | assembly |
| 8.1 | Base Frame | gravity-die-casting-machine-base-frame | 1× | 1 | · | part |
| 8.2 | Support Column | gravity-die-casting-machine-column | 2× | 2 | · | part |
| 8.3 | Sheet Metal Panel | sheet-panel | 4× | 4 | · | part |
| 8.4 | Safety Light Curtain | gravity-die-casting-machine-light-curtain | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Industrial Ultrasonic Cleaner
787 parts · shares 19 with this page
Micro Injection Molding Machine
704 parts · shares 19 with this page
Shell Molding Machine
116 parts · shares 19 with this page
 Thermal Spray Coating System
866 parts · shares 19 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $5k–$2M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| atlascopco.com ↗ | Stockholm, SE | Compressors & industrial | 10 units | 12–20 wks |
|
🇦🇹Andritz
andritz.com ↗
|
Graz, AT | Process plants & machinery | 10 units | 12–20 wks |
| buhlergroup.com ↗ | Uzwil, CH | Food & materials processing | 10 units | 12–20 wks |
| gea.com ↗ | Düsseldorf, DE | Process technology | 10 units | 12–20 wks |
| mhi.com ↗ | Tokyo, JP | Heavy machinery | 10 units | 12–20 wks |
1,007-word article