Micro Injection Molding Machine
ProductOverview
A micro injection molding machine makes plastic parts that weigh milligrams and carry features measured in microns: hearing-aid components, watch gears, micro-optics, surgical and endoscopic parts, microfluidic chips, and connector contacts. Standard machines cannot do this well because their screws meter shots far larger than the part, so a tiny dose comes from the leftover end of a much bigger stroke with poor repeatability and long residence time that degrades the melt. A micro machine splits the job: a small Plasticizing & Dosing Unit melts and meters the plastic, then hands a precise dose to a separate Injection Plunger that injects it. This two-stage layout gives clean control over a sub-gram shot.
Dosing unit
The Plasticizing & Dosing Unit is a small extruder. A Micro Screw of 12 to 18 mm turns inside a Dosing Barrel, melting pellets fed from the Feed Hopper and pushing a measured quantity of melt forward. A Melt Shutoff Valve then isolates the dosing barrel from the injection side so the screw can keep plasticizing while the plunger injects. Separating melting from injecting keeps the melt moving and short-resident, which matters because the tiny mass involved would otherwise sit and degrade.
Injection plunger
The Injection Plunger is what gives a micro machine its precision. Rather than using the screw itself as the injection piston, a small dedicated Plunger Rod, often 3 to 8 mm and carbide-tipped, drives the dose into the mold through a short, controlled stroke. The Injection Servo Motor servo turns the Plunger Ball Screw, and a Injection Load Cell plus a Melt Pressure Sensor close the loop on injection pressure. A small plunger over a short stroke resolves the shot far more finely than a large screw could, so a 5 mg part is repeatable shot to shot.
Clamp and ejection
The Micro Clamp Unit is a low-tonnage servo toggle, since the projected area of a micro part is tiny and needs only a few tonnes to hold shut. A Clamp Servo Motor drives the Toggle Linkage through a ball screw against a Clamp Encoder, guided on four Tie Bar columns. Getting the part out is its own problem: the Micro Ejector uses Micro Ejector Pin sets as small as 0.3 mm, driven by a servo so the push force and stroke are gentle enough not to deform the part.
Heating, vacuum, and mold tempering
Filling micron features means the melt must reach the far corners of the cavity before it freezes. The Heating System tightly zones the barrel with a Cartridge Heater set, each built on a Heating Element and read by a Zone Thermocouple. Critically, the Variotherm Mold Heater runs a variotherm cycle: the mold wall is heated hot just before injection so the melt stays fluid into the smallest features, then cooled to freeze the part. The Mold Vacuum System evacuates the cavity through a Vacuum Valve before the shot, because at micron scale even a trace of trapped air would block the melt and leave a short fill. A Mold Vacuum Seal rings the parting line.
Part handling and inspection
Parts this small cannot be sorted by hand and are easy to lose. The Part Handling System system uses a Micro Pick Robot with a Vacuum Gripper to lift each part off the mold, presents it to a Inspection Camera for dimensional and defect inspection, and places good parts into a Tray Placement Station in a known position for the next process. This in-line handling is part of the machine, not an add-on, because manual handling of milligram parts is impractical.
Control, frame, and use
The Control System is built around a high-resolution Motion Controller that resolves injection position to about a micron, with the operator working from the HMI Touchscreen. The Machine Frame sits on a Cast Base Plate with Vibration Isolation Mount isolators, since machine vibration at this scale shows up as part variation. Micro machines mold engineering and high-performance resins, liquid crystal polymer, PEEK, polyoxymethylene, and clear cyclic olefins for optics, in volumes from prototype to millions. They are the route to parts that a standard molder cannot dose accurately, fill completely, or eject and handle without damage.
Runner and gate design is a larger problem at this scale than the part itself. On a 5 mg part the runner that carries melt to the cavity can weigh more than the part, so the shot is mostly waste unless the design minimizes it. Micro molds use small cold sub-runners or, better, hot tips that gate directly into the cavity and leave almost no scrap. Mold tolerances are held to single microns, and the steel is often hardened and polished or electroformed to reproduce features below the resolution of conventional machining. Process windows are narrow: a few degrees of melt temperature or a fraction of a second of hold time changes whether a micron feature fills. For this reason the Inspection Camera inspection is in-line on every part rather than by sampling, because a drift that would be cosmetic on a large part can scrap a micro part outright.
Micro Injection Molding Machine parts and their functions
8 top-level parts · 704 parts in total · full bill of materials below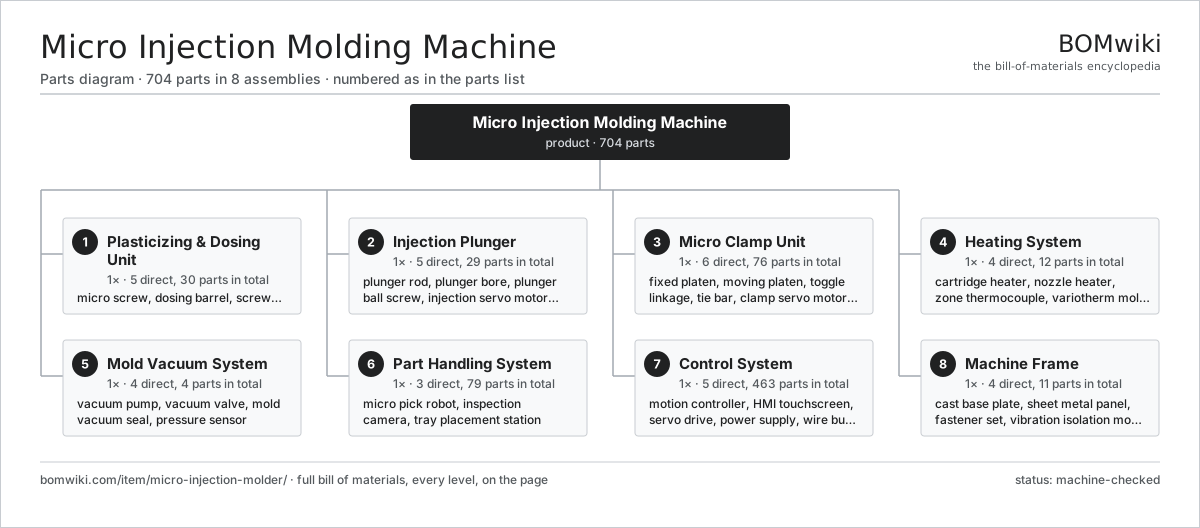
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Plasticizing & Dosing Unit 5 parts | 1× | Small screw or extruder that melts pellets and meters a precise micro-dose. |
| 2 | Injection Plunger 5 parts | 1× | Small piston that injects the metered micro-dose with high control over a tiny shot. |
| 3 | Micro Clamp Unit 6 parts | 1× | Low-tonnage servo toggle clamp sized for very small, precise molds. |
| 4 | Heating System 4 parts | 1× | Tightly zoned barrel and nozzle heaters for stable melt of a tiny mass. |
| 5 | Mold Vacuum System 4 parts | 1× | Evacuates the cavity so trapped air cannot stop melt reaching micro-features. |
| 6 | Part Handling System 3 parts | 1× | Pick robot, vision check, and tray placement for parts too small to handle by hand. |
| 7 | Control System 5 parts | 1× | High-resolution motion controller closing loops on a sub-gram shot. |
| 8 | Machine Frame 4 parts | 1× | Compact benchtop or floor frame on a stable, low-vibration base. |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Micro Injection Molding Machine
8 top-level lines · 79 rows shown · 704 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Plasticizing & Dosing Unit 5 parts | micro-injection-molder-dosing-unit | 1× | 1 | 30 | assembly |
| 1.1 | Micro Screw | micro-injection-molder-micro-screw | 1× | 1 | · | part |
| 1.2 | Dosing Barrel | micro-injection-molder-dosing-barrel | 1× | 1 | · | part |
| 1.3 | Screw Servo Motor 2 parts | micro-injection-molder-screw-motor | 1× | 1 | 26 | assembly |
| 1.3.1 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 1.3.2 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 1.4 | Melt Shutoff Valve | micro-injection-molder-shutoff-valve | 1× | 1 | · | part |
| 1.5 | Feed Hopper | micro-injection-molder-feed-hopper | 1× | 1 | · | part |
| 2 | Injection Plunger 5 parts | micro-injection-molder-injection-plunger | 1× | 1 | 29 | assembly |
| 2.1 | Plunger Rod | micro-injection-molder-plunger-rod | 1× | 1 | · | part |
| 2.2 | Plunger Bore | micro-injection-molder-plunger-bore | 1× | 1 | · | part |
| 2.3 | Plunger Ball Screw 1 parts | micro-injection-molder-plunger-ballscrew | 1× | 1 | · | part |
| 2.3.1 | Ball Screw | ball-screw | 1× | 1 | · | part |
| 2.4 | Injection Servo Motor 2 parts | micro-injection-molder-injection-motor | 1× | 1 | 25 | assembly |
| 2.4.1 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 2.4.2 | Injection Load Cell | micro-injection-molder-injection-loadcell | 1× | 1 | · | part |
| 2.5 | Melt Pressure Sensor 1 parts | micro-injection-molder-melt-sensor | 1× | 1 | · | part |
| 2.5.1 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 3 | Micro Clamp Unit 6 parts | micro-injection-molder-clamp-unit | 1× | 1 | 76 | assembly |
| 3.1 | Fixed Platen | micro-injection-molder-fixed-platen | 1× | 1 | · | part |
| 3.2 | Moving Platen | micro-injection-molder-moving-platen | 1× | 1 | · | part |
| 3.3 | Toggle Linkage 3 parts | micro-injection-molder-toggle | 1× | 1 | 15 | assembly |
| 3.3.1 | Toggle Link | micro-injection-molder-toggle-link | 6× | 6 | · | part |
| 3.3.2 | Toggle Pin | micro-injection-molder-toggle-pin | 8× | 8 | · | part |
| 3.3.3 | Crosshead | micro-injection-molder-crosshead | 1× | 1 | · | part |
| 3.4 | Tie Bar | micro-injection-molder-tie-bar | 4× | 4 | · | part |
| 3.5 | Clamp Servo Motor 3 parts | micro-injection-molder-clamp-motor | 1× | 1 | 26 | assembly |
| 3.5.1 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 3.5.2 | Ball Screw | ball-screw | 1× | 1 | · | part |
| 3.5.3 | Clamp Encoder | micro-injection-molder-clamp-encoder | 1× | 1 | · | part |
| 3.6 | Micro Ejector 3 parts | micro-injection-molder-ejector | 1× | 1 | 29 | assembly |
| 3.6.1 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 3.6.2 | Micro Ejector Pin | micro-injection-molder-ejector-pin | 4× | 4 | · | part |
| 3.6.3 | Ejector Plate | micro-injection-molder-ejector-plate | 1× | 1 | · | part |
| 4 | Heating System 4 parts | micro-injection-molder-heating-system | 1× | 1 | 12 | assembly |
| 4.1 | Cartridge Heater 1 parts | micro-injection-molder-cartridge-heater | 4× | 4 | · | part |
| 4.1.1 | Heating Element | heating-element | 1× | 4 | · | part |
| 4.2 | Nozzle Heater 1 parts | micro-injection-molder-nozzle-heater | 1× | 1 | · | part |
| 4.2.1 | Heating Element | heating-element | 1× | 1 | · | part |
| 4.3 | Zone Thermocouple | micro-injection-molder-thermocouple | 5× | 5 | · | part |
| 4.4 | Variotherm Mold Heater 1 parts | micro-injection-molder-mold-heater | 2× | 2 | · | part |
| 4.4.1 | Heating Element | heating-element | 1× | 2 | · | part |
| 5 | Mold Vacuum System 4 parts | micro-injection-molder-vacuum-system | 1× | 1 | 4 | assembly |
| 5.1 | Vacuum Pump | micro-injection-molder-vacuum-pump | 1× | 1 | · | part |
| 5.2 | Vacuum Valve | micro-injection-molder-vacuum-valve | 1× | 1 | · | part |
| 5.3 | Mold Vacuum Seal 1 parts | micro-injection-molder-vacuum-seal | 1× | 1 | · | part |
| 5.3.1 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 5.4 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 6 | Part Handling System 3 parts | micro-injection-molder-part-handling | 1× | 1 | 79 | assembly |
| 6.1 | Micro Pick Robot 3 parts | micro-injection-molder-pick-robot | 1× | 1 | 75 | assembly |
| 6.1.1 | Servo Motor 4 parts + deeper › | servo-motor | 3× | 3 | 24 | assembly |
| 6.1.2 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 6.1.3 | Vacuum Gripper | micro-injection-molder-vacuum-gripper | 1× | 1 | · | part |
| 6.2 | Inspection Camera 3 parts | micro-injection-molder-vision-camera | 1× | 1 | 3 | assembly |
| 6.2.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 6.2.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 6.2.3 | Image Sensor | micro-injection-molder-camera-sensor | 1× | 1 | · | part |
| 6.3 | Tray Placement Station | micro-injection-molder-tray-station | 1× | 1 | · | part |
| 7 | Control System 5 parts | micro-injection-molder-control-system | 1× | 1 | 463 | assembly |
| 7.1 | Motion Controller 4 parts | micro-injection-molder-controller | 1× | 1 | 130 | assembly |
| 7.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 7.1.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 7.1.3 | SMD Passive (R/C/L) | smd-passives | 120× | 120 | · | part |
| 7.1.4 | Connector | connector | 8× | 8 | · | part |
| 7.2 | HMI Touchscreen 3 parts | micro-injection-molder-hmi | 1× | 1 | 3 | assembly |
| 7.2.1 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 7.2.2 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 7.2.3 | Microcontroller | mcu | 1× | 1 | · | part |
| 7.3 | Servo Drive 3 parts | micro-injection-molder-servo-drive | 4× | 4 | 82 | assembly |
| 7.3.1 | Bare PCB | pcb-bare | 1× | 4 | · | part |
| 7.3.2 | Microcontroller | mcu | 1× | 4 | · | part |
| 7.3.3 | SMD Passive (R/C/L) | smd-passives | 80× | 320 | · | part |
| 7.4 | Power Supply | power-supply | 1× | 1 | · | part |
| 7.5 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 8 | Machine Frame 4 parts | micro-injection-molder-frame | 1× | 1 | 11 | assembly |
| 8.1 | Cast Base Plate | micro-injection-molder-base-plate | 1× | 1 | · | part |
| 8.2 | Sheet Metal Panel | sheet-panel | 5× | 5 | · | part |
| 8.3 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 8.4 | Vibration Isolation Mount | micro-injection-molder-vibration-mount | 4× | 4 | · | part |
Related products
same domain, ranked by shared parts Industrial Ultrasonic Cleaner
787 parts · shares 24 with this page
 Thermal Spray Coating System
866 parts · shares 24 with this page
 Rubber Extrusion Line
524 parts · shares 23 with this page
Powder Coating Line
5,418 parts · shares 23 with this page
 All-Electric Injection Molding Machine
851 parts · shares 22 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $5k–$2M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| atlascopco.com ↗ | Stockholm, SE | Compressors & industrial | 10 units | 12–20 wks |
|
🇦🇹Andritz
andritz.com ↗
|
Graz, AT | Process plants & machinery | 10 units | 12–20 wks |
| buhlergroup.com ↗ | Uzwil, CH | Food & materials processing | 10 units | 12–20 wks |
| gea.com ↗ | Düsseldorf, DE | Process technology | 10 units | 12–20 wks |
| mhi.com ↗ | Tokyo, JP | Heavy machinery | 10 units | 12–20 wks |
949-word article