Squeeze Casting Machine
ProductOverview
A squeeze casting machine pours molten metal into a die and then applies high mechanical pressure, typically 50 to 150 megapascals, while the metal solidifies. Holding pressure on the freezing metal collapses the gas porosity and shrinkage voids that ordinary castings contain, so squeeze castings come out nearly fully dense. That density lets them be heat treated to high strength, welded, and used in safety-critical parts where a porous casting would fail. The process bridges casting and forging: it has the shape freedom and metal economy of casting with the soundness and properties closer to a forging. It runs on aluminium and magnesium alloys and is the usual route for casting metal-matrix composites, where ceramic fibre or particle preforms are infiltrated by pressurised metal.
The machine is a vertical hydraulic press built around a Press Frame that reacts the load, a Clamp and Squeeze Cylinder that applies the squeeze, a heated Die and Punch Tooling that shapes the part, a Metal Feed System that delivers clean metal, and a Hydraulic Power Unit that profiles the pressure.
Direct and indirect squeeze casting
In direct squeeze casting a measured charge of metal is poured straight into an open Lower Die, then an upper Squeeze Punch descends, closes the cavity and presses on the whole metal mass as it freezes. The pressure acts over the full projected area, so it needs high press force but feeds shrinkage everywhere. In indirect squeeze casting the metal is held in a Shot Sleeve and pushed into a closed die through a large gate, then pressure is held through that gate during solidification. Direct gives the densest result and is used for simple compact shapes; indirect handles more complex geometries and is closer to a slow, high-integrity pressure die casting. The same base machine runs both with a tooling change.
Press frame and squeeze cylinder
The Press Frame is a stiff structure of Press Bed, Press Crown and four pre-stressed Tie Rod columns that carry the full squeeze load with minimal deflection, because any frame flexing would let the punch back off and reopen porosity. The Main Squeeze Cylinder drives the Press Slide and punch through a hardened Piston Rod, and a Position Sensor tracks punch position so the controller knows exactly when the metal is contacted and how it compresses.
Pressure profiling
The defining control task is the pressure profile. The Hydraulic Power Unit uses a Servo Valve backed by Hydraulic Accumulator units to raise pressure fast once the punch meets the metal, then hold it precisely on a Pressure Controller loop through the whole solidification time, often 20 to 120 seconds. The pressure must be applied while the metal is still liquid or semi-solid and held until the centre is frozen, otherwise the porosity it is meant to suppress will already have formed. Profile and timing are stored per part in the recipe.
Die and thermal control
The Die and Punch Tooling is H13 hot-work tool steel, heated by Die Cartridge Heater units and a Hot-Oil Temperature Unit and read by Die Thermocouple probes. The die runs at 200 to 350 degrees Celsius, hot enough to keep the metal feeding under pressure yet cool enough to freeze the part in cycle. Vent Insert units let trapped gas escape ahead of the closing punch, and zone cooling through a Cooling Water Manifold with Zone Flow Valve trim and Air Cooling Jet spots drives directional solidification under the held pressure.
Metal feed and ejection
The Metal Feed System delivers a clean, accurately metered charge: an automatic Dosing Ladle driven by a Servo Motor pours through a Pour Trough with low turbulence, after an inline Rotary Degasser has stripped dissolved hydrogen that would otherwise nucleate porosity. After the pressure hold and a short release the Ejection System system lifts the dense casting out with an Ejector Pin array and a Casting Takeout gripper removes it. The Control Panel coordinates the whole sequence through its Machine PLC.
Applications
Squeeze casting makes high-integrity aluminium parts that must be strong and pressure-tight: automotive road wheels, suspension knuckles and control arms, pistons, brake components and chassis nodes. It is the standard process for aluminium metal-matrix composite parts, where pressure forces molten metal into a fibre or particle preform. Compared with gravity or pressure die casting it gives near-zero porosity and full heat-treat response, at the cost of a heavier press, longer cycle and higher pressure-hold demands on the tooling and hydraulics.
Process control and maintenance
Squeeze casting is unforgiving of timing, so process monitoring is heavier than on most casting machines. The controller logs punch position, pressure and time for every shot, and a deviation in any of them flags a suspect part for inspection rather than letting it pass. Metal cleanliness matters more than in low-integrity casting, which is why the degasser runs continuously and the pour temperature is held to a few degrees; dissolved hydrogen and oxide films are the two defects that even high pressure cannot fully cure. On the maintenance side the high squeeze load works the tie rods, the main cylinder seals and the punch face hard, and all three are inspected on a fixed interval. The hydraulic accumulators are checked for pre-charge pressure because a weak accumulator slows the pressure rise and lets porosity form before the squeeze takes hold. The die surface, like any permanent mould, develops heat checking over time and is refurbished on a campaign basis.
Squeeze Casting Machine parts and their functions
8 top-level parts · 117 parts in total · full bill of materials below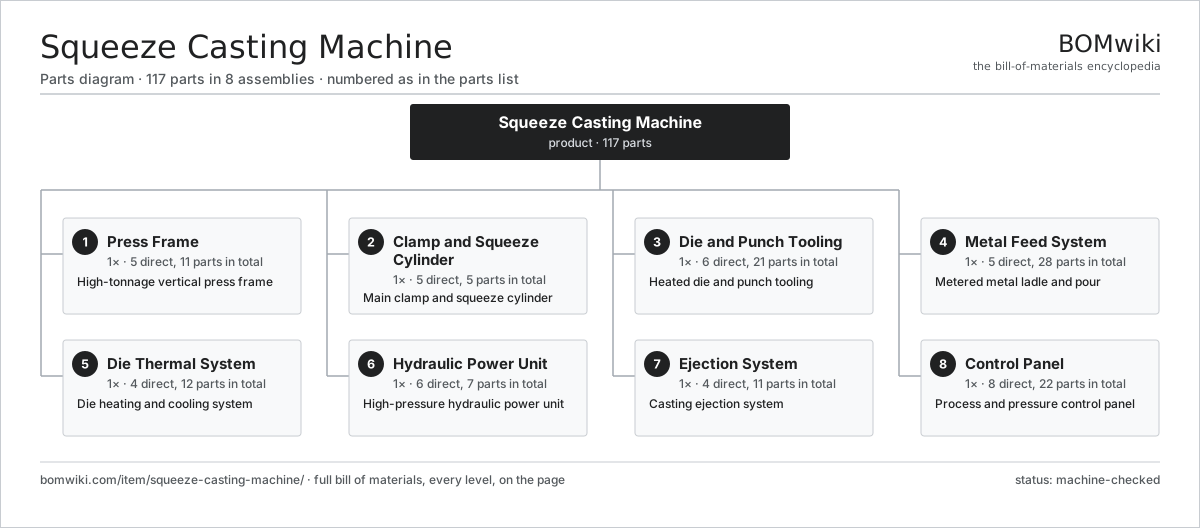
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Press Frame 5 parts | 1× | High-tonnage vertical press frame |
| 2 | Clamp and Squeeze Cylinder 5 parts | 1× | Main clamp and squeeze cylinder |
| 3 | Die and Punch Tooling 6 parts | 1× | Heated die and punch tooling |
| 4 | Metal Feed System 5 parts | 1× | Metered metal ladle and pour |
| 5 | Die Thermal System 4 parts | 1× | Die heating and cooling system |
| 6 | Hydraulic Power Unit 6 parts | 1× | High-pressure hydraulic power unit |
| 7 | Ejection System 4 parts | 1× | Casting ejection system |
| 8 | Control Panel 8 parts | 1× | Process and pressure control panel |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Squeeze Casting Machine
8 top-level lines · 55 rows shown · 117 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Press Frame 5 parts | squeeze-casting-machine-press-frame | 1× | 1 | 11 | assembly |
| 1.1 | Press Bed | squeeze-casting-machine-bed | 1× | 1 | · | part |
| 1.2 | Press Crown | squeeze-casting-machine-crown | 1× | 1 | · | part |
| 1.3 | Tie Rod | squeeze-casting-machine-tie-rod | 4× | 4 | · | part |
| 1.4 | Press Slide | squeeze-casting-machine-slide | 1× | 1 | · | part |
| 1.5 | Linear Guide Rail | linear-guide | 4× | 4 | · | part |
| 2 | Clamp and Squeeze Cylinder 5 parts | squeeze-casting-machine-clamp-cylinder | 1× | 1 | 5 | assembly |
| 2.1 | Main Squeeze Cylinder | squeeze-casting-machine-main-cylinder | 1× | 1 | · | part |
| 2.2 | Piston Rod | squeeze-casting-machine-piston-rod | 1× | 1 | · | part |
| 2.3 | Cylinder Seal Set | squeeze-casting-machine-cylinder-seal | 1× | 1 | · | part |
| 2.4 | Position Sensor | squeeze-casting-machine-position-sensor | 1× | 1 | · | part |
| 2.5 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 3 | Die and Punch Tooling 6 parts | squeeze-casting-machine-die-set | 1× | 1 | 21 | assembly |
| 3.1 | Lower Die | squeeze-casting-machine-lower-die | 1× | 1 | · | part |
| 3.2 | Squeeze Punch | squeeze-casting-machine-punch | 1× | 1 | · | part |
| 3.3 | Die Cartridge Heater | squeeze-casting-machine-die-cartridge-heater | 8× | 8 | · | part |
| 3.4 | Die Thermocouple | squeeze-casting-machine-die-thermocouple | 6× | 6 | · | part |
| 3.5 | Vent Insert | squeeze-casting-machine-vent-insert | 4× | 4 | · | part |
| 3.6 | Shot Sleeve | squeeze-casting-machine-shot-sleeve | 1× | 1 | · | part |
| 4 | Metal Feed System 5 parts | squeeze-casting-machine-metal-feed | 1× | 1 | 28 | assembly |
| 4.1 | Dosing Ladle | squeeze-casting-machine-dosing-ladle | 1× | 1 | · | part |
| 4.2 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 4.2.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 4.2.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 4.2.3 | Encoder | encoder | 1× | 1 | · | part |
| 4.2.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 4.3 | Pour Trough | squeeze-casting-machine-pour-trough | 1× | 1 | · | part |
| 4.4 | Rotary Degasser | squeeze-casting-machine-degasser | 1× | 1 | · | part |
| 4.5 | Metal Thermocouple | squeeze-casting-machine-metal-thermocouple | 1× | 1 | · | part |
| 5 | Die Thermal System 4 parts | squeeze-casting-machine-thermal-system | 1× | 1 | 12 | assembly |
| 5.1 | Cooling Water Manifold | squeeze-casting-machine-water-manifold | 1× | 1 | · | part |
| 5.2 | Zone Flow Valve | squeeze-casting-machine-flow-valve | 6× | 6 | · | part |
| 5.3 | Hot-Oil Temperature Unit | squeeze-casting-machine-oil-temp-unit | 1× | 1 | · | part |
| 5.4 | Air Cooling Jet | squeeze-casting-machine-air-jet | 4× | 4 | · | part |
| 6 | Hydraulic Power Unit 6 parts | squeeze-casting-machine-hydraulic-unit | 1× | 1 | 7 | assembly |
| 6.1 | Hydraulic Pump | squeeze-casting-machine-hyd-pump | 1× | 1 | · | part |
| 6.2 | Hydraulic Motor | squeeze-casting-machine-hyd-motor | 1× | 1 | · | part |
| 6.3 | Hydraulic Accumulator | squeeze-casting-machine-accumulator | 2× | 2 | · | part |
| 6.4 | Servo Valve | squeeze-casting-machine-servo-valve | 1× | 1 | · | part |
| 6.5 | Hydraulic Reservoir | squeeze-casting-machine-hyd-reservoir | 1× | 1 | · | part |
| 6.6 | Hydraulic Oil Cooler | squeeze-casting-machine-oil-cooler | 1× | 1 | · | part |
| 7 | Ejection System 4 parts | squeeze-casting-machine-ejection | 1× | 1 | 11 | assembly |
| 7.1 | Ejector Plate | squeeze-casting-machine-ejector-plate | 1× | 1 | · | part |
| 7.2 | Ejector Pin | squeeze-casting-machine-ejector-pin | 8× | 8 | · | part |
| 7.3 | Ejector Cylinder | squeeze-casting-machine-ejector-cylinder | 1× | 1 | · | part |
| 7.4 | Casting Takeout | squeeze-casting-machine-takeout | 1× | 1 | · | part |
| 8 | Control Panel 8 parts | squeeze-casting-machine-control-panel | 1× | 1 | 22 | assembly |
| 8.1 | Machine PLC | squeeze-casting-machine-plc | 1× | 1 | · | part |
| 8.2 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 8.3 | Pressure Controller | squeeze-casting-machine-pressure-controller | 1× | 1 | · | part |
| 8.4 | Relay | relay | 8× | 8 | · | part |
| 8.5 | Connector | connector | 8× | 8 | · | part |
| 8.6 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 8.7 | Microcontroller | mcu | 1× | 1 | · | part |
| 8.8 | Bare PCB | pcb-bare | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Gravity Die Casting Machine
120 parts · shares 18 with this page
 Industrial Ultrasonic Cleaner
787 parts · shares 18 with this page
Micro Injection Molding Machine
704 parts · shares 18 with this page
 Rubber Extrusion Line
524 parts · shares 18 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $5k–$2M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| atlascopco.com ↗ | Stockholm, SE | Compressors & industrial | 10 units | 12–20 wks |
|
🇦🇹Andritz
andritz.com ↗
|
Graz, AT | Process plants & machinery | 10 units | 12–20 wks |
| buhlergroup.com ↗ | Uzwil, CH | Food & materials processing | 10 units | 12–20 wks |
| gea.com ↗ | Düsseldorf, DE | Process technology | 10 units | 12–20 wks |
| mhi.com ↗ | Tokyo, JP | Heavy machinery | 10 units | 12–20 wks |
1,006-word article