Desiccant Resin Dryer
ProductOverview
A desiccant resin dryer prepares hygroscopic plastics, the ones that absorb water deep into the pellet, for molding and extrusion. Resins such as PET, PA, PC, and PBT take up moisture that a simple hot-air hopper cannot remove, because the limit is not heat but the dryness of the air. This machine supplies very dry air, with a dewpoint far below freezing, by passing the process air over a Desiccant Beds of molecular sieve. The Process Blower drives the air, the Process Heater warms it, the Drying Hopper holds the resin, and the Aftercooler and Regeneration System keep the desiccant working. A Changeover Valves set swaps the beds, the Dryer Control runs the cycle, and the Cabinet and Frame houses it all.
The defining trick is the twin bed: while one bed dries the process air, the other is being baked clean of the moisture it captured earlier, so the dryer can deliver dry air without interruption. This is what separates a desiccant dryer from the hot-air hopper used for commodity resins.
The desiccant beds
The Desiccant Beds is where the air is dried. Two Desiccant Tower canisters each hold a charge of Molecular Sieve beads, a zeolite that adsorbs water vapor onto its enormous internal surface, pulling the process air down to a dewpoint of around minus forty degrees. Retaining Screen retainers hold the beads in place against the airflow. At any moment one tower is online drying the process air while the other is offline being regenerated. A Dewpoint Sensor measures how dry the delivered air actually is, which is the truest check that the resin is being properly dried, since temperature alone does not prove dryness.
Process air loop
On the resin side, the dryer runs a closed loop much like a hot-air hopper but fed with desiccant-dried air. The Process Blower uses a Blower Impeller driven by a Blower Motor in a Blower Scroll to push the dried air through the Process Heater, where several Heating Element units in a Heater Can raise it to drying temperature under Process Thermocouple control, with a Thermal Fuse as a high-limit backup. The hot dry air then enters the Drying Hopper, passes up through the resin, picks up moisture, and returns to the bed to be dried again. Recirculating the air this way is efficient because the returning air is already warm and the desiccant only has to remove the small amount of water the resin gives off.
The drying hopper
The Drying Hopper holds the resin in the dry air stream long enough to dry it through. A stainless Hopper Cone shaped for mass flow keeps every pellet moving down at the same rate, surrounded by Hopper Insulation to hold the heat. Dry air enters through an Air Diffuser that spreads it evenly across the base, and leaves the top through a Return Filter that catches resin dust before it fouls the beds. Dried resin discharges through the Discharge Gate to the machine. Residence time is set by the hopper size against the throughput, since hygroscopic resins need a few hours in dry air to release their absorbed water.
Regeneration and changeover
A desiccant bed fills up with water and must be cleaned out, which is the job of the Regeneration System. A Regeneration Blower pushes air heated by its own Heating Element units through the offline bed, driving the trapped moisture out and carrying it away through the Exhaust Duct under Regen Thermocouple control. When the online bed nears saturation, the Changeover Valves swaps the two: a Rotary Valve turned by a Valve Actuator and sealed by Valve Seal gaskets routes the freshly regenerated bed into the process loop and sends the spent bed to regeneration. Changeover can be timed or, better, triggered by the Dewpoint Sensor so a bed is swapped only when it actually needs it, which saves regeneration energy.
Aftercooling and control
A bed adsorbs water best from cool air, but the air returning from the resin is warm, so the Aftercooler cools it first. A Cooler Coil served by a Cooler Fan pulls heat out of the return air before it re-enters the desiccant tower, improving the dewpoint the bed can reach. Over the whole machine the Dryer Control holds drying temperature, times or triggers the bed changeover, and watches dewpoint and temperature on the Operator Touchscreen, switching heaters and valves through a Relay bank. Many controllers also pair temperature to airflow and drop the heat when no resin is being drawn, to avoid over-drying resin that sits idle.
Resins and use
Desiccant dryers are reserved for resins that genuinely need them. PET demands very low dewpoint and careful temperature because residual water makes it break down during melting, PA and PC absorb water deeply and mold with splay and weak welds if dried poorly, and TPU and PBT have similar needs. Commodity polyolefins like PP and PE do not absorb water and are served by a plain hot-air hopper instead, since a desiccant dryer would only waste energy on them. In a plant the dryer stands beside or above the molding machine on its Cabinet and Frame frame, fed from a central resin line, and its dewpoint readout is the operator's proof that the resin is dry before it is ever melted. The main upkeep is replacing the Molecular Sieve charge as it ages, keeping the Return Filter clean, and verifying the dewpoint sensor.
Desiccant Resin Dryer parts and their functions
9 top-level parts · 88 parts in total · full bill of materials below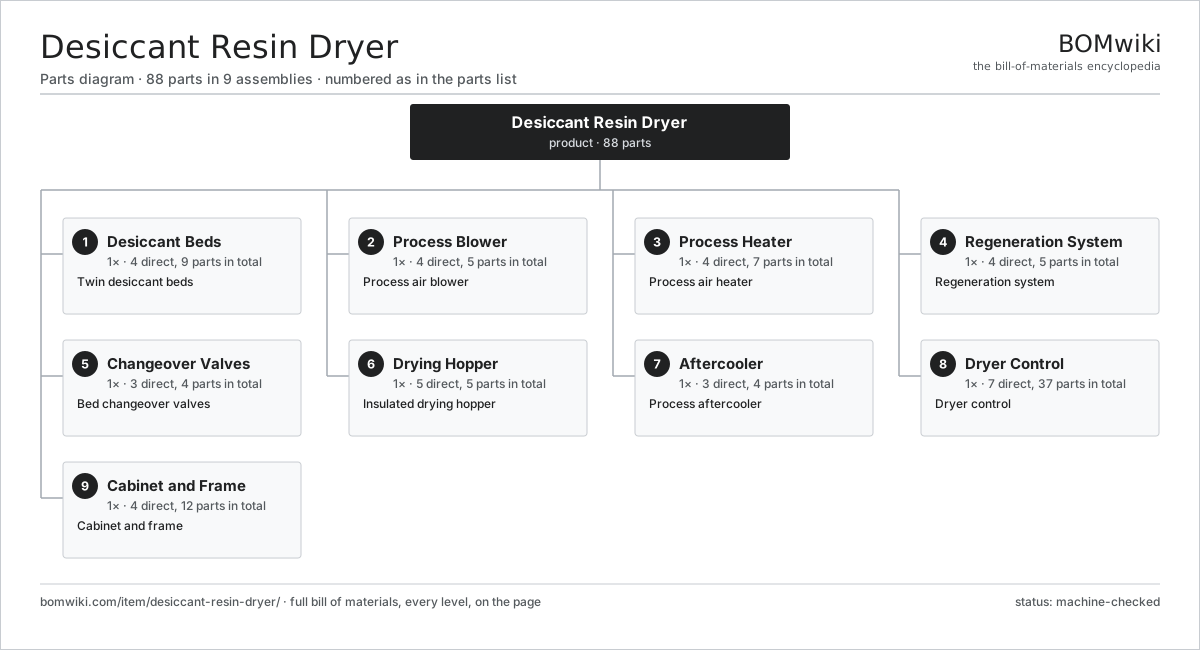
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Desiccant Beds 4 parts | 1× | Twin desiccant beds |
| 2 | Process Blower 4 parts | 1× | Process air blower |
| 3 | Process Heater 4 parts | 1× | Process air heater |
| 4 | Regeneration System 4 parts | 1× | Regeneration system |
| 5 | Changeover Valves 3 parts | 1× | Bed changeover valves |
| 6 | Drying Hopper 5 parts | 1× | Insulated drying hopper |
| 7 | Aftercooler 3 parts | 1× | Process aftercooler |
| 8 | Dryer Control 7 parts | 1× | Dryer control |
| 9 | Cabinet and Frame 4 parts | 1× | Cabinet and frame |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Desiccant Resin Dryer
9 top-level lines · 47 rows shown · 88 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Desiccant Beds 4 parts | desiccant-resin-dryer-desiccant-bed | 1× | 1 | 9 | assembly |
| 1.1 | Desiccant Tower | desiccant-resin-dryer-bed-tower | 2× | 2 | · | part |
| 1.2 | Molecular Sieve | desiccant-resin-dryer-molecular-sieve | 2× | 2 | · | part |
| 1.3 | Retaining Screen | desiccant-resin-dryer-bed-screen | 4× | 4 | · | part |
| 1.4 | Dewpoint Sensor | desiccant-resin-dryer-dewpoint-sensor | 1× | 1 | · | part |
| 2 | Process Blower 4 parts | desiccant-resin-dryer-process-blower | 1× | 1 | 5 | assembly |
| 2.1 | Blower Impeller | desiccant-resin-dryer-blower-impeller | 1× | 1 | · | part |
| 2.2 | Blower Motor | desiccant-resin-dryer-blower-motor | 1× | 1 | · | part |
| 2.3 | Blower Scroll | desiccant-resin-dryer-blower-scroll | 1× | 1 | · | part |
| 2.4 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 3 | Process Heater 4 parts | desiccant-resin-dryer-process-heater | 1× | 1 | 7 | assembly |
| 3.1 | Heating Element | heating-element | 3× | 3 | · | part |
| 3.2 | Heater Can | desiccant-resin-dryer-heater-can | 1× | 1 | · | part |
| 3.3 | Process Thermocouple | desiccant-resin-dryer-process-thermocouple | 2× | 2 | · | part |
| 3.4 | Thermal Fuse | thermal-fuse | 1× | 1 | · | part |
| 4 | Regeneration System 4 parts | desiccant-resin-dryer-regen-system | 1× | 1 | 5 | assembly |
| 4.1 | Regeneration Blower | desiccant-resin-dryer-regen-blower | 1× | 1 | · | part |
| 4.2 | Heating Element | heating-element | 2× | 2 | · | part |
| 4.3 | Regen Thermocouple | desiccant-resin-dryer-regen-thermocouple | 1× | 1 | · | part |
| 4.4 | Exhaust Duct | desiccant-resin-dryer-exhaust-duct | 1× | 1 | · | part |
| 5 | Changeover Valves 3 parts | desiccant-resin-dryer-changeover-valve | 1× | 1 | 4 | assembly |
| 5.1 | Rotary Valve | desiccant-resin-dryer-rotary-valve | 1× | 1 | · | part |
| 5.2 | Valve Actuator | desiccant-resin-dryer-valve-actuator | 1× | 1 | · | part |
| 5.3 | Valve Seal | desiccant-resin-dryer-valve-seal | 2× | 2 | · | part |
| 6 | Drying Hopper 5 parts | desiccant-resin-dryer-drying-hopper | 1× | 1 | 5 | assembly |
| 6.1 | Hopper Cone | desiccant-resin-dryer-hopper-cone | 1× | 1 | · | part |
| 6.2 | Hopper Insulation | desiccant-resin-dryer-hopper-insulation | 1× | 1 | · | part |
| 6.3 | Air Diffuser | desiccant-resin-dryer-air-diffuser | 1× | 1 | · | part |
| 6.4 | Return Filter | desiccant-resin-dryer-return-filter | 1× | 1 | · | part |
| 6.5 | Discharge Gate | desiccant-resin-dryer-discharge-gate | 1× | 1 | · | part |
| 7 | Aftercooler 3 parts | desiccant-resin-dryer-aftercooler | 1× | 1 | 4 | assembly |
| 7.1 | Cooler Coil | desiccant-resin-dryer-cooler-coil | 1× | 1 | · | part |
| 7.2 | Cooler Fan | desiccant-resin-dryer-cooler-fan | 1× | 1 | · | part |
| 7.3 | Water Hose | water-hose | 2× | 2 | · | part |
| 8 | Dryer Control 7 parts | desiccant-resin-dryer-control | 1× | 1 | 37 | assembly |
| 8.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 8.3 | Operator Touchscreen | desiccant-resin-dryer-touchscreen | 1× | 1 | · | part |
| 8.4 | Relay | relay | 8× | 8 | · | part |
| 8.5 | Power Supply | power-supply | 1× | 1 | · | part |
| 8.6 | Connector | connector | 24× | 24 | · | part |
| 8.7 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 9 | Cabinet and Frame 4 parts | desiccant-resin-dryer-cabinet | 1× | 1 | 12 | assembly |
| 9.1 | Base Frame | desiccant-resin-dryer-base-frame | 1× | 1 | · | part |
| 9.2 | Sheet Metal Panel | sheet-panel | 6× | 6 | · | part |
| 9.3 | Caster | desiccant-resin-dryer-caster | 4× | 4 | · | part |
| 9.4 | Fastener Set | fastener-set | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Industrial FDM Printer
98 parts · shares 8 with this page
Soap Plodder
61 parts · shares 8 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $5k–$2M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| atlascopco.com ↗ | Stockholm, SE | Compressors & industrial | 10 units | 12–20 wks |
|
🇦🇹Andritz
andritz.com ↗
|
Graz, AT | Process plants & machinery | 10 units | 12–20 wks |
| buhlergroup.com ↗ | Uzwil, CH | Food & materials processing | 10 units | 12–20 wks |
| gea.com ↗ | Düsseldorf, DE | Process technology | 10 units | 12–20 wks |
| mhi.com ↗ | Tokyo, JP | Heavy machinery | 10 units | 12–20 wks |
1,040-word article