Two-Shot Injection Molding Machine
ProductOverview
A two-shot, or 2K, injection molding machine makes a single part from two different plastics in one automated cycle. It has two complete injection units and a mold whose cavity changes between the first and second shot, usually by rotating the part 180 degrees on a Rotary Platen. The Primary Injection Unit unit fills the first cavity to form the substrate; the platen indexes, carrying that part to a second cavity; then the Secondary Injection Unit unit injects the second material around or onto it. The part is never removed between shots, so the two materials bond while the first is still warm and the second is fresh. This makes soft-grip handles, sealed buttons, multi-color housings, and toothbrushes in one operation.
Primary injection unit
The Primary Injection Unit unit is a conventional horizontal screw. Pellets enter the Water-Cooled Feed Throat of the Primary Barrel, the Primary Screw melts and meters them past a Non-Return Check Ring, and the Primary Injection Cylinder rams the shot through the Primary Nozzle into the first cavity. This shot is the rigid substrate, often a glass-filled or unfilled engineering resin. The Primary Screw Drive turns the screw during recharge.
Secondary injection unit
The Secondary Injection Unit unit injects the second material into the second cavity. It is built the same way, with its own Secondary Screw and Secondary Nozzle, but it is mounted off the main axis: piggyback above the primary unit, vertically over the clamp, or at a right angle, set by the Piggyback Mount Bracket bracket and the part geometry. Running a separate unit lets the second material, frequently a thermoplastic elastomer for soft grip, be processed at its own temperature and pressure independent of the first.
Rotary platen and clamp
The trick of two-shot molding is moving the first-shot part to the second cavity without losing position. The Rotary Platen center disc carries the cores; its Index Drive servo rotates it exactly 180 degrees against a Index Position Encoder, and a Media Rotary Coupling passes cooling water and hydraulics across the turning interface. The whole stack is held shut by the Clamp Unit, a toggle clamp on four Tie Bar columns whose Toggle Linkage linkage multiplies the Clamp Cylinder force into clamp tonnage. When both shots are complete on each side, the Ejector System releases the finished two-material part.
Hydraulic and heating systems
Because two injections plus the index all draw power, the Hydraulic System is sized generously around a Variable Displacement Pump and a Valve Manifold with extra Proportional Valve and Directional Valve channels, plus an Accumulator for the fast strokes. The Barrel Heating System is doubled: each barrel has its own Barrel Band Heater zones, every one built on a Heating Element and read by a Zone Thermocouple, so the two resins hold separate melt profiles.
Control and safety
The Control System runs a more complex sequence than a single-shot machine: it must time both injections, confirm the platen reached position, and interlock the clamp around the rotation. The Machine Controller handles the logic and the operator sets both shots on the HMI Touchscreen. The Safety System guards both injection units and the rotating platen with a Sliding Safety Gate chain of Interlock Switch interlocks, a Light Curtain, and the Emergency Stop.
Materials, bonding, and use
The two materials bond either chemically, when the resins are compatible, or mechanically, when the second shot flows into undercuts and through-holes in the first. Material selection is the heart of 2K design: a polypropylene substrate pairs with a PP-based TPE, polyamide with a polyamide-grade elastomer, polycarbonate with a bonding-grade TPU. Common products include power-tool and razor handles with soft overmold, sealed membrane keypads, automotive switches with light-piped icons, and two-color caps. The alternative process, core-back molding, opens a shutoff inside one mold instead of rotating, but the rotary-platen machine described here is the general-purpose choice because it keeps both cavities filling every cycle. The Base Frame is longer than a standard machine to carry the second unit alongside the first.
Timing is the constraint that sets cycle time. The two shots cannot fire at once: the first must fill and partially set before the platen indexes, and the second injects only after rotation completes and the clamp is fully locked. The Rotary Platen index of roughly one to two seconds adds to every cycle, so 2K parts cost more than single-shot parts both in tooling and in time. The mold is also more complex, since it carries two cavities that must register precisely across the rotation; the first-shot core must seal against the second-shot cavity without flash. For these reasons 2K molding is chosen when the alternative, molding two parts and assembling them, would cost more in labor, tolerance stack-up, or sealing than the dual machine adds. High-volume consumer parts with a soft grip or a sealed button are the classic case.
Two-Shot Injection Molding Machine parts and their functions
9 top-level parts · 376 parts in total · full bill of materials below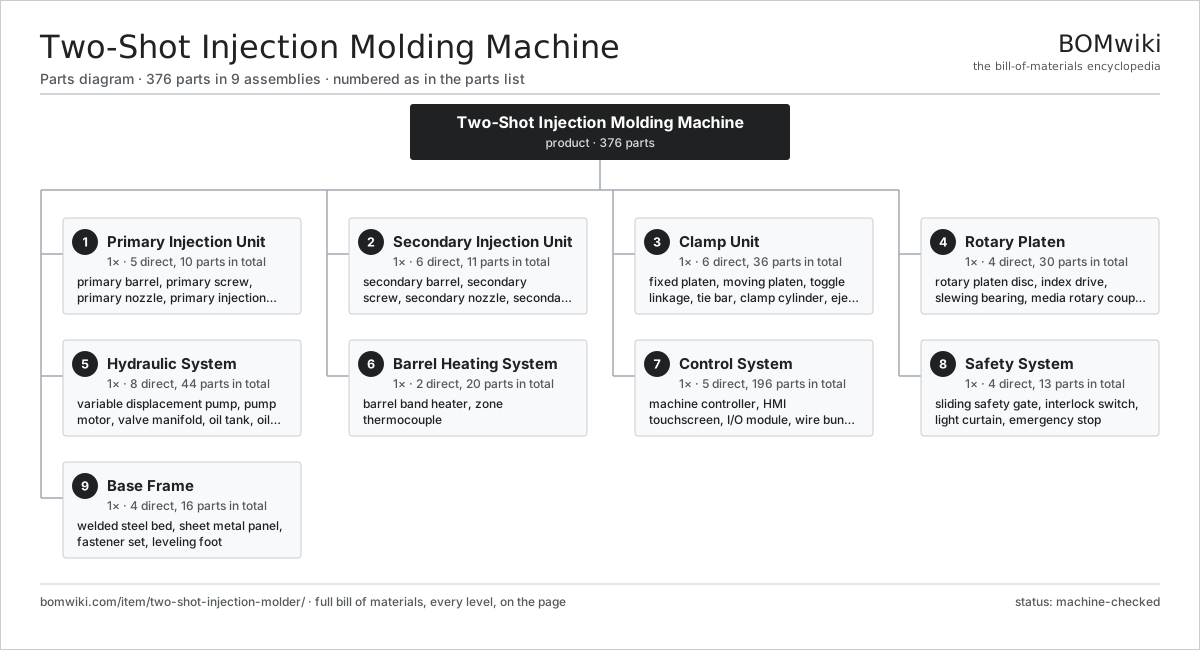
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Primary Injection Unit 5 parts | 1× | Horizontal screw injecting the first material (substrate) into the mold. |
| 2 | Secondary Injection Unit 6 parts | 1× | Second screw, often top- or piggyback-mounted, injecting the overmold material. |
| 3 | Clamp Unit 6 parts | 1× | Toggle clamp holding the two-station mold shut against both injections. |
| 4 | Rotary Platen 4 parts | 1× | Servo-indexed center platen that carries the first-shot part to the second cavity. |
| 5 | Hydraulic System 8 parts | 1× | Pump and dual injection manifold powering both shots and the clamp. |
| 6 | Barrel Heating System 2 parts | 1× | Independent zone heaters for each barrel so two resins run at their own profiles. |
| 7 | Control System 5 parts | 1× | Controller sequencing two injections, the index, and the clamp. |
| 8 | Safety System 4 parts | 1× | Interlocked guards covering both injection units and the rotating platen. |
| 9 | Base Frame 4 parts | 1× | Welded bed carrying clamp, rotary platen, and two injection units. |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Two-Shot Injection Molding Machine
9 top-level lines · 96 rows shown · 376 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Primary Injection Unit 5 parts | two-shot-injection-molder-primary-injection | 1× | 1 | 10 | assembly |
| 1.1 | Primary Barrel 2 parts | two-shot-injection-molder-primary-barrel | 1× | 1 | 2 | assembly |
| 1.1.1 | Barrel Tube | two-shot-injection-molder-barrel-tube | 1× | 1 | · | part |
| 1.1.2 | Water-Cooled Feed Throat | two-shot-injection-molder-feed-throat | 1× | 1 | · | part |
| 1.2 | Primary Screw 2 parts | two-shot-injection-molder-primary-screw | 1× | 1 | 2 | assembly |
| 1.2.1 | Screw Body | two-shot-injection-molder-screw-body | 1× | 1 | · | part |
| 1.2.2 | Non-Return Check Ring | two-shot-injection-molder-check-ring | 1× | 1 | · | part |
| 1.3 | Primary Nozzle 1 parts | two-shot-injection-molder-primary-nozzle | 1× | 1 | · | part |
| 1.3.1 | Heating Element | heating-element | 1× | 1 | · | part |
| 1.4 | Primary Injection Cylinder | two-shot-injection-molder-primary-cylinder | 1× | 1 | · | part |
| 1.5 | Primary Screw Drive 3 parts | two-shot-injection-molder-primary-drive | 1× | 1 | 4 | assembly |
| 1.5.1 | Hydraulic Motor | two-shot-injection-molder-hydraulic-motor | 1× | 1 | · | part |
| 1.5.2 | Helical Gear Pair | gear-pair | 1× | 1 | · | part |
| 1.5.3 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 2 | Secondary Injection Unit 6 parts | two-shot-injection-molder-secondary-injection | 1× | 1 | 11 | assembly |
| 2.1 | Secondary Barrel 2 parts | two-shot-injection-molder-secondary-barrel | 1× | 1 | 2 | assembly |
| 2.1.1 | Barrel Tube | two-shot-injection-molder-barrel-tube | 1× | 1 | · | part |
| 2.1.2 | Water-Cooled Feed Throat | two-shot-injection-molder-feed-throat | 1× | 1 | · | part |
| 2.2 | Secondary Screw 2 parts | two-shot-injection-molder-secondary-screw | 1× | 1 | 2 | assembly |
| 2.2.1 | Screw Body | two-shot-injection-molder-screw-body | 1× | 1 | · | part |
| 2.2.2 | Non-Return Check Ring | two-shot-injection-molder-check-ring | 1× | 1 | · | part |
| 2.3 | Secondary Nozzle 1 parts | two-shot-injection-molder-secondary-nozzle | 1× | 1 | · | part |
| 2.3.1 | Heating Element | heating-element | 1× | 1 | · | part |
| 2.4 | Secondary Injection Cylinder | two-shot-injection-molder-secondary-cylinder | 1× | 1 | · | part |
| 2.5 | Secondary Screw Drive 3 parts | two-shot-injection-molder-secondary-drive | 1× | 1 | 4 | assembly |
| 2.5.1 | Hydraulic Motor | two-shot-injection-molder-hydraulic-motor | 1× | 1 | · | part |
| 2.5.2 | Helical Gear Pair | gear-pair | 1× | 1 | · | part |
| 2.5.3 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 2.6 | Piggyback Mount Bracket | two-shot-injection-molder-secondary-mount | 1× | 1 | · | part |
| 3 | Clamp Unit 6 parts | two-shot-injection-molder-clamp-unit | 1× | 1 | 36 | assembly |
| 3.1 | Fixed Platen | two-shot-injection-molder-fixed-platen | 1× | 1 | · | part |
| 3.2 | Moving Platen | two-shot-injection-molder-moving-platen | 1× | 1 | · | part |
| 3.3 | Toggle Linkage 3 parts | two-shot-injection-molder-toggle | 1× | 1 | 19 | assembly |
| 3.3.1 | Toggle Link | two-shot-injection-molder-toggle-link | 8× | 8 | · | part |
| 3.3.2 | Toggle Pin | two-shot-injection-molder-toggle-pin | 10× | 10 | · | part |
| 3.3.3 | Crosshead | two-shot-injection-molder-crosshead | 1× | 1 | · | part |
| 3.4 | Tie Bar | two-shot-injection-molder-tie-bar | 4× | 4 | · | part |
| 3.5 | Clamp Cylinder | two-shot-injection-molder-clamp-cylinder | 1× | 1 | · | part |
| 3.6 | Ejector System 3 parts | two-shot-injection-molder-ejector | 1× | 1 | 10 | assembly |
| 3.6.1 | Ejector Cylinder | two-shot-injection-molder-ejector-cylinder | 1× | 1 | · | part |
| 3.6.2 | Ejector Plate | two-shot-injection-molder-ejector-plate | 1× | 1 | · | part |
| 3.6.3 | Ejector Pin | two-shot-injection-molder-ejector-pin | 8× | 8 | · | part |
| 4 | Rotary Platen 4 parts | two-shot-injection-molder-rotary-platen | 1× | 1 | 30 | assembly |
| 4.1 | Rotary Platen Disc | two-shot-injection-molder-rotary-disc | 1× | 1 | · | part |
| 4.2 | Index Drive 3 parts | two-shot-injection-molder-index-drive | 1× | 1 | 27 | assembly |
| 4.2.1 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 4.2.2 | Helical Gear Pair | gear-pair | 2× | 2 | · | part |
| 4.2.3 | Index Position Encoder | two-shot-injection-molder-index-encoder | 1× | 1 | · | part |
| 4.3 | Slewing Bearing 1 parts | two-shot-injection-molder-rotary-bearing | 1× | 1 | · | part |
| 4.3.1 | Ball Bearing | ball-bearing | 1× | 1 | · | part |
| 4.4 | Media Rotary Coupling | two-shot-injection-molder-rotary-coupling | 1× | 1 | · | part |
| 5 | Hydraulic System 8 parts | two-shot-injection-molder-hydraulic-system | 1× | 1 | 44 | assembly |
| 5.1 | Variable Displacement Pump | two-shot-injection-molder-pump | 1× | 1 | · | part |
| 5.2 | Pump Motor 2 parts | two-shot-injection-molder-pump-motor | 1× | 1 | · | part |
| 5.2.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 5.2.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 5.3 | Valve Manifold 3 parts | two-shot-injection-molder-valve-manifold | 1× | 1 | 13 | assembly |
| 5.3.1 | Proportional Valve | two-shot-injection-molder-proportional-valve | 4× | 4 | · | part |
| 5.3.2 | Directional Valve | two-shot-injection-molder-directional-valve | 8× | 8 | · | part |
| 5.3.3 | Manifold Block | two-shot-injection-molder-manifold-block | 1× | 1 | · | part |
| 5.4 | Oil Tank | two-shot-injection-molder-oil-tank | 1× | 1 | · | part |
| 5.5 | Oil Cooler | two-shot-injection-molder-oil-cooler | 1× | 1 | · | part |
| 5.6 | Accumulator | two-shot-injection-molder-accumulator | 1× | 1 | · | part |
| 5.7 | Pressure Sensor | pressure-sensor | 4× | 4 | · | part |
| 5.8 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 6 | Barrel Heating System 2 parts | two-shot-injection-molder-heating-system | 1× | 1 | 20 | assembly |
| 6.1 | Barrel Band Heater 1 parts | two-shot-injection-molder-band-heater | 9× | 9 | · | part |
| 6.1.1 | Heating Element | heating-element | 1× | 9 | · | part |
| 6.2 | Zone Thermocouple | two-shot-injection-molder-thermocouple | 11× | 11 | · | part |
| 7 | Control System 5 parts | two-shot-injection-molder-control-system | 1× | 1 | 196 | assembly |
| 7.1 | Machine Controller 4 parts | two-shot-injection-molder-controller | 1× | 1 | 152 | assembly |
| 7.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 7.1.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 7.1.3 | SMD Passive (R/C/L) | smd-passives | 140× | 140 | · | part |
| 7.1.4 | Connector | connector | 10× | 10 | · | part |
| 7.2 | HMI Touchscreen 3 parts | two-shot-injection-molder-hmi | 1× | 1 | 3 | assembly |
| 7.2.1 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 7.2.2 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 7.2.3 | Microcontroller | mcu | 1× | 1 | · | part |
| 7.3 | I/O Module 3 parts | two-shot-injection-molder-io-module | 3× | 3 | 13 | assembly |
| 7.3.1 | Bare PCB | pcb-bare | 1× | 3 | · | part |
| 7.3.2 | Relay | relay | 8× | 24 | · | part |
| 7.3.3 | Connector | connector | 4× | 12 | · | part |
| 7.4 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 7.5 | Power Supply | power-supply | 1× | 1 | · | part |
| 8 | Safety System 4 parts | two-shot-injection-molder-safety-system | 1× | 1 | 13 | assembly |
| 8.1 | Sliding Safety Gate 1 parts | two-shot-injection-molder-safety-gate | 2× | 2 | · | part |
| 8.1.1 | Sheet Metal Panel | sheet-panel | 2× | 4 | · | part |
| 8.2 | Interlock Switch | two-shot-injection-molder-safety-switch | 6× | 6 | · | part |
| 8.3 | Light Curtain | two-shot-injection-molder-light-curtain | 1× | 1 | · | part |
| 8.4 | Emergency Stop | two-shot-injection-molder-estop | 2× | 2 | · | part |
| 9 | Base Frame 4 parts | two-shot-injection-molder-base-frame | 1× | 1 | 16 | assembly |
| 9.1 | Welded Steel Bed | two-shot-injection-molder-bed | 1× | 1 | · | part |
| 9.2 | Sheet Metal Panel | sheet-panel | 8× | 8 | · | part |
| 9.3 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 9.4 | Leveling Foot | two-shot-injection-molder-leveling-foot | 6× | 6 | · | part |
Related products
same domain, ranked by shared parts Industrial Parts Washer
423 parts · shares 23 with this page
Vertical Injection Molding Machine
264 parts · shares 23 with this page
Shell Molding Machine
116 parts · shares 22 with this page
Coil Coating Line
1,767 parts · shares 22 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $5k–$2M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| atlascopco.com ↗ | Stockholm, SE | Compressors & industrial | 10 units | 12–20 wks |
|
🇦🇹Andritz
andritz.com ↗
|
Graz, AT | Process plants & machinery | 10 units | 12–20 wks |
| buhlergroup.com ↗ | Uzwil, CH | Food & materials processing | 10 units | 12–20 wks |
| gea.com ↗ | Düsseldorf, DE | Process technology | 10 units | 12–20 wks |
| mhi.com ↗ | Tokyo, JP | Heavy machinery | 10 units | 12–20 wks |
983-word article