Plastic Thermoforming Line
ProductOverview
A plastic thermoforming line turns a roll of flat plastic sheet into finished parts like food trays, drink cups, lids, and blister packs. It works by a simple idea repeated fast: heat the sheet until it is soft and rubbery, stretch it over or into a mold, hold it there with vacuum until it cools and keeps the shape, then cut the parts out of the sheet. A roll-fed line does this continuously, gripping the sheet by its edges and indexing it one frame at a time through a heating oven, a forming station, and a trim press, so a wide sheet with many cavities yields dozens of parts every few seconds. It is the dominant way to make thin-wall packaging because the tooling is cheaper than injection molds and the output is very high.
The line feeds and indexes sheet through the Sheet Feed, heats it in the Heating Oven, shapes it at the Forming Station over the Forming Mold, cuts parts in the Trim Press, collects them at the Stacker Outfeed, supplies forming vacuum and air through the Vacuum and Air System, and runs from the Line Controller.
Feeding and indexing the sheet
The Sheet Feed grips and moves the sheet. A Sheet Unwind pays roll sheet into the line, and two Pin Chain Rail rails pierce the sheet edges with spikes and carry it through every station. The Index Drive advances the chain one exact step per cycle using a Helical Gear Pair reduction and an Encoder for position, while Edge Guide guides keep the sheet aligned. Indexing accuracy matters because the same frame of sheet has to register under the heaters, then the mold, then the trim die: any drift and the trim die cuts into the wrong place. The whole line is paced by this index, so its cycle rate sets the output of the machine.
Heating
The Heating Oven is where the sheet is brought to forming temperature, and even heating is the hardest part of running a line. Banks of ceramic Heating Element radiant heaters above and below the sheet are grouped into Heater Zone zones so the operator can put more heat where the sheet runs cool, such as the edges held by the chain. A set of Sheet Pyrometer sensors reads the sheet surface temperature and a Sag Sensor watches the natural droop of the hot sheet, because the right forming temperature shows up as a specific amount of sag. Too cold and the sheet will not draw into deep corners; too hot and it sags, thins, or sticks. The Oven Shell insulates and reflects heat to keep the oven even and efficient.
Forming over the mold
At the Forming Station, the soft sheet is shaped. A Toggle Drive closes the Upper Platen and Lower Platen on Linear Guide Rail rails so the clamp frame seals the sheet over the Forming Mold. For deep parts a heated Plug Assist pushes down first to pre-stretch the sheet mechanically so the walls come out even, then the Vacuum and Air System pulls a vacuum through fine holes in the Vent Insert pieces and draws the sheet tight onto the Cavity Block. Water in the Cooling Channel chills the mold so the part sets in a second or two, then a Ejector Ring and a puff of air release it. Plug assist plus vacuum, sometimes with added air pressure, is what lets a line make deep cups with reasonably uniform walls instead of a thin, over-stretched base.
Trimming and stacking
The formed parts are still joined to the surrounding web, so the Trim Press cuts them free. A Trim Die driven by the Trim Platen punches every part out of its frame in one stroke, and the leftover skeleton web goes to a Scrap Grinder that reduces it to regrind for reuse, which matters because thermoforming generates a lot of edge scrap. The cut parts pass to the Stacker Outfeed, where Stacking Fingers catch and nest them, a Count and Eject Unit counts off a set number, and a Outfeed Conveyor carries counted stacks to packing. Many lines form and trim in separate stations like this; some do both in one tool, trading flexibility for speed.
Vacuum, air, and control
The Vacuum and Air System supplies the forces that shape the part. A Vacuum Pump keeps a Vacuum Tank surge tank charged so the sheet forms in a fast, deep pull rather than a slow draw, an Air Compressor supplies pressure air for pressure forming and part release, and a fast Valve Bank switches vacuum, pressure, and ejection in time with the cycle. The Line Controller cabinet runs the whole sequence: an Microcontroller paces the index, oven zones, forming, trim, and stacking, and the operator works from the Operator Screen to call up a stored recipe for a given part, sheet, and material. These lines run in packaging plants making the trays, cups, and lids used across food, retail, and medical packaging, where high cycle rates and low tooling cost make thermoforming the economical choice for thin-wall plastic parts in large volumes.
Plastic Thermoforming Line parts and their functions
8 top-level parts · 224 parts in total · full bill of materials below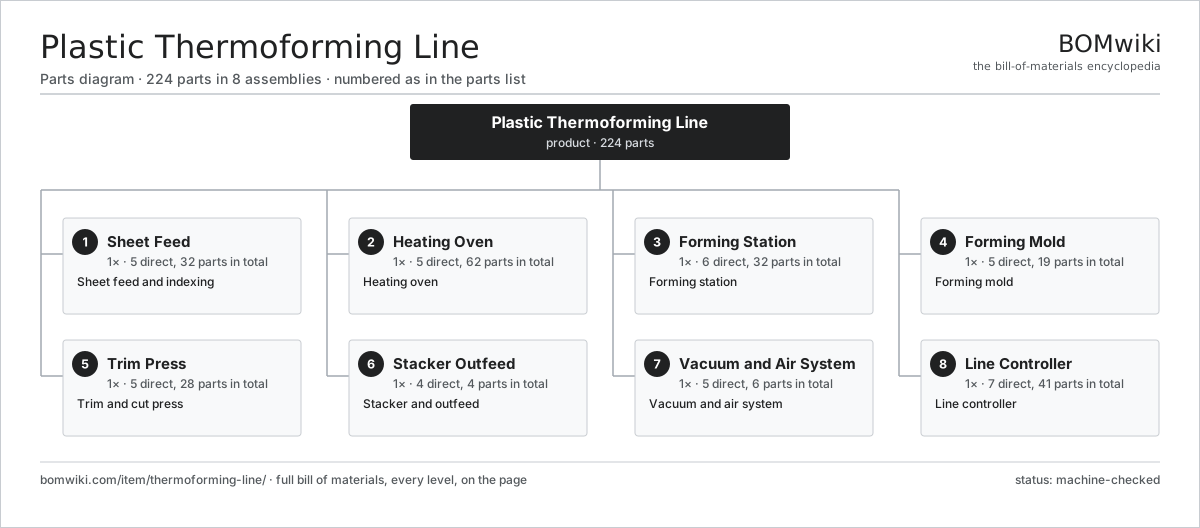
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Sheet Feed 5 parts | 1× | Sheet feed and indexing |
| 2 | Heating Oven 5 parts | 1× | Heating oven |
| 3 | Forming Station 6 parts | 1× | Forming station |
| 4 | Forming Mold 5 parts | 1× | Forming mold |
| 5 | Trim Press 5 parts | 1× | Trim and cut press |
| 6 | Stacker Outfeed 4 parts | 1× | Stacker and outfeed |
| 7 | Vacuum and Air System 5 parts | 1× | Vacuum and air system |
| 8 | Line Controller 7 parts | 1× | Line controller |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Plastic Thermoforming Line
8 top-level lines · 65 rows shown · 224 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Sheet Feed 5 parts | thermoforming-line-sheet-feed | 1× | 1 | 32 | assembly |
| 1.1 | Sheet Unwind | thermoforming-line-unwind-roll | 1× | 1 | · | part |
| 1.2 | Pin Chain Rail | thermoforming-line-pin-chain | 2× | 2 | · | part |
| 1.3 | Index Drive 3 parts | thermoforming-line-index-drive | 1× | 1 | 3 | assembly |
| 1.3.1 | Helical Gear Pair | gear-pair | 1× | 1 | · | part |
| 1.3.2 | Gearbox Housing | gearbox-housing | 1× | 1 | · | part |
| 1.3.3 | Encoder | encoder | 1× | 1 | · | part |
| 1.4 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 1.4.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 1.4.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 1.4.3 | Encoder | encoder | 1× | 1 | · | part |
| 1.4.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 1.5 | Edge Guide | thermoforming-line-edge-guide | 2× | 2 | · | part |
| 2 | Heating Oven 5 parts | thermoforming-line-oven | 1× | 1 | 62 | assembly |
| 2.1 | Heating Element | heating-element | 48× | 48 | · | part |
| 2.2 | Heater Zone | thermoforming-line-heater-zone | 8× | 8 | · | part |
| 2.3 | Sheet Pyrometer | thermoforming-line-pyrometer | 4× | 4 | · | part |
| 2.4 | Oven Shell | thermoforming-line-oven-shell | 1× | 1 | · | part |
| 2.5 | Sag Sensor | thermoforming-line-sag-sensor | 1× | 1 | · | part |
| 3 | Forming Station 6 parts | thermoforming-line-forming-station | 1× | 1 | 32 | assembly |
| 3.1 | Upper Platen | thermoforming-line-upper-platen | 1× | 1 | · | part |
| 3.2 | Lower Platen | thermoforming-line-lower-platen | 1× | 1 | · | part |
| 3.3 | Plug Assist | thermoforming-line-plug-assist | 1× | 1 | · | part |
| 3.4 | Toggle Drive | thermoforming-line-toggle-drive | 1× | 1 | · | part |
| 3.5 | Linear Guide Rail | linear-guide | 4× | 4 | · | part |
| 3.6 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 3.6.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 3.6.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 3.6.3 | Encoder | encoder | 1× | 1 | · | part |
| 3.6.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 4 | Forming Mold 5 parts | thermoforming-line-mold | 1× | 1 | 19 | assembly |
| 4.1 | Cavity Block | thermoforming-line-cavity-block | 1× | 1 | · | part |
| 4.2 | Vent Insert | thermoforming-line-vent-insert | 12× | 12 | · | part |
| 4.3 | Cooling Channel | thermoforming-line-cooling-channel | 1× | 1 | · | part |
| 4.4 | Ejector Ring | thermoforming-line-ejector-ring | 1× | 1 | · | part |
| 4.5 | O-Ring Set | oring-set | 4× | 4 | · | part |
| 5 | Trim Press 5 parts | thermoforming-line-trim-press | 1× | 1 | 28 | assembly |
| 5.1 | Trim Die | thermoforming-line-trim-die | 1× | 1 | · | part |
| 5.2 | Trim Platen | thermoforming-line-trim-platen | 1× | 1 | · | part |
| 5.3 | Press Frame | thermoforming-line-press-frame | 1× | 1 | · | part |
| 5.4 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 5.4.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 5.4.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 5.4.3 | Encoder | encoder | 1× | 1 | · | part |
| 5.4.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 5.5 | Scrap Grinder | thermoforming-line-scrap-grinder | 1× | 1 | · | part |
| 6 | Stacker Outfeed 4 parts | thermoforming-line-stacker | 1× | 1 | 4 | assembly |
| 6.1 | Stacking Fingers | thermoforming-line-stack-fingers | 1× | 1 | · | part |
| 6.2 | Count and Eject Unit | thermoforming-line-counter | 1× | 1 | · | part |
| 6.3 | Outfeed Conveyor | thermoforming-line-outfeed-conveyor | 1× | 1 | · | part |
| 6.4 | Drive Belt | drive-belt | 1× | 1 | · | part |
| 7 | Vacuum and Air System 5 parts | thermoforming-line-vacuum-system | 1× | 1 | 6 | assembly |
| 7.1 | Vacuum Pump | thermoforming-line-vacuum-pump | 1× | 1 | · | part |
| 7.2 | Vacuum Tank | thermoforming-line-vacuum-tank | 1× | 1 | · | part |
| 7.3 | Air Compressor | thermoforming-line-air-compressor | 1× | 1 | · | part |
| 7.4 | Valve Bank | thermoforming-line-valve-bank | 1× | 1 | · | part |
| 7.5 | Pressure Sensor | pressure-sensor | 2× | 2 | · | part |
| 8 | Line Controller 7 parts | thermoforming-line-control | 1× | 1 | 41 | assembly |
| 8.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 8.3 | Operator Screen | thermoforming-line-hmi | 1× | 1 | · | part |
| 8.4 | Power Supply | power-supply | 1× | 1 | · | part |
| 8.5 | Relay | relay | 12× | 12 | · | part |
| 8.6 | Connector | connector | 24× | 24 | · | part |
| 8.7 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Rubber Extrusion Line
524 parts · shares 23 with this page
 Continuous Galvanizing Line
1,296 parts · shares 22 with this page
Powder Coating Line
5,418 parts · shares 22 with this page
Shell Molding Machine
116 parts · shares 21 with this page
Electrocoating Line
2,977 parts · shares 22 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $5k–$2M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| atlascopco.com ↗ | Stockholm, SE | Compressors & industrial | 10 units | 12–20 wks |
|
🇦🇹Andritz
andritz.com ↗
|
Graz, AT | Process plants & machinery | 10 units | 12–20 wks |
| buhlergroup.com ↗ | Uzwil, CH | Food & materials processing | 10 units | 12–20 wks |
| gea.com ↗ | Düsseldorf, DE | Process technology | 10 units | 12–20 wks |
| mhi.com ↗ | Tokyo, JP | Heavy machinery | 10 units | 12–20 wks |
920-word article