Continuous Galvanizing Line
ProductOverview
A continuous galvanizing line turns bare cold-rolled steel coil into zinc-coated strip in one unbroken pass. The strip is welded end to end into an effectively endless ribbon, cleaned, annealed in a reducing atmosphere, dipped through a bath of molten zinc near 460 C, wiped to a precise coating weight by gas jets, cooled, given a surface finish, passivated, oiled and rewound. The line runs continuously at the pot even though coils are finite, which is the reason for the welder and the two accumulators: they let the entry and exit ends stop for coil changes while the central process holds constant speed and temperature.
The coating forms because hot clean steel wets molten zinc and a thin iron-zinc alloy layer grows at the interface, bonding the coat metallurgically rather than mechanically. Everything upstream of the Zinc Pot Section exists to deliver the strip clean, oxide-free and at the right temperature, and everything downstream exists to set the coating weight, freeze it without marking, and protect it for storage.
Entry and continuous feeding
Two coils are loaded in turn by the Coil Loading Car onto the Expanding Mandrel of each Pay-off Reel. While one reel pays off, the next coil is staged on the second reel. When the running coil nears its end, the Strip Joiner takes over: the Crop Shear squares both strip ends, the Strip Welder fuses them with its Seam Weld Wheel electrodes, and the Seam Trimmer dresses the bead flush so it passes through the rolls and pot without trouble. During this weld the entry end is stationary, so the Entry Accumulator pays out its stored loop. Its Accumulator Carriage rides up and down a tall Accumulator Tower, lengthening or shortening the festoon over the Loop Roll rolls to absorb the speed difference. The Entry Bridle sets the tension that carries the strip into the cleaning section.
Cleaning
Cold-rolled strip arrives covered in rolling oil and iron fines, and zinc will not wet a dirty surface. The Cleaning Section removes both. The strip first runs through the Degrease Tank, where heated alkaline cleaner is sprayed and the strip is dipped. The Brush Scrubber then scrubs both faces with rotating Brush Roll rolls to lift loosened soils. A cascade Rinse Tank flushes the alkali away, Wringer Roll wringer rolls strip the carry-over water, and the Strip Dryer leaves the surface dry before it enters the furnace.
Annealing furnace
The Annealing Furnace does two jobs at once: it recrystallizes the cold-worked steel to restore ductility, and it reduces the thin surface oxide so the steel will bond with zinc. Heating is by Radiant Tube tubes fired by Recuperative Burner burners, so the combustion gases stay inside the tubes and never touch the strip. The strip climbs in temperature through the Preheat Zone and Radiant Heating Zone, holds in the Soak Zone, then drops in the Jet Cooling Zone to a few degrees above bath temperature. Throughout, the Atmosphere System holds a reducing mix of hydrogen in nitrogen with a low dew point, watched by the Dew Point Sensor and Oxygen Analyzer. The strip is steered by Hearth Roll rolls and leaves through the Furnace Snout, a sealed throat whose Snout Tip sits just below the zinc surface so the hot strip enters the melt without ever meeting air.
Zinc pot and coating
The Zinc Pot Vessel holds the molten zinc, lined with refractory by the Pot Refractory Liner and kept at temperature by the Channel Induction Heater, which heats the metal by inducing current in a circulating loop of melt. The strip descends through the snout, wraps the Sink Roll at the bottom of the bath and rises again, steadied by the Stabilizer Roll rolls so it leaves the bath without flutter. These submerged rolls run on the Pot Roll Bearing bearings carried by the Pot Roll Support Arm. The bath surface is kept clean by the Dross Skimmer, and zinc level is held by the Zinc Ingot Feeder.
As the strip rises out of the bath it carries far more zinc than the finished spec allows. The Air Knife Section section fixes that: the Air Knife Header nozzles, fed by the Air Knife Blower, blow a thin sheet of gas at the strip and strip the excess zinc back into the pot. Coating weight is set by the gas pressure, the nozzle gap and the line speed, with the Knife Positioner holding the gap and the Coating Weight Gauge reading the result on both faces so the control loop can trim the knives in real time.
Cooling, finishing and exit
The wiped coating is still molten, so the Cooling Tower freezes it with forced air from the Air Cooling Box boxes before any roll touches it. Once solid, the strip runs through the Skin Pass and Leveler section, where the Skin-Pass Mill Stand applies a small elongation to set surface texture and the Tension Leveler takes out residual shape. The Chemical Treatment then applies a passivation film at the Passivation Coater to resist white rust in storage and an oil film at the Electrostatic Oiler for forming and corrosion protection.
At the exit the Exit Accumulator mirrors the entry: it stores strip so the Recoiler can stop while the Exit Shear cuts a finished coil free and the Belt Wrapper starts the next one. The Exit Bridle holds exit tension while the reel winds the coated coil.
Drive and control
The whole line is tied together by the Drive and Control System system. Each reel and bridle runs on a regenerative AC Drive in the cooled Drive Cabinet, so a decelerating reel feeds energy to the accelerating bridles. The Line PLC coordinates speed, tension, bath temperature and furnace atmosphere as one process, taking strip tension from the Tensiometer Roll rolls and presenting recipes and live readings to the operator on the Operator HMI. The coating spec, the steel grade and the line speed all sit in those recipes, and the controller balances them so the strip leaves with the ordered coating weight, finish and flatness.
Continuous Galvanizing Line parts and their functions
10 top-level parts · 1,296 parts in total · full bill of materials below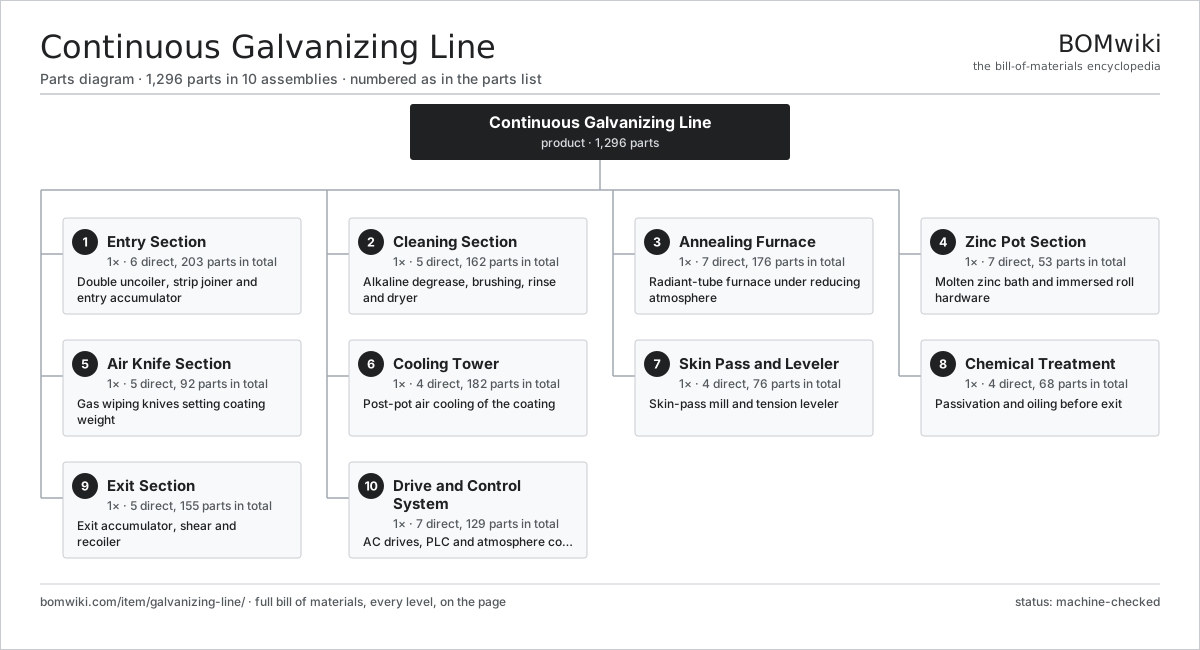
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Entry Section 6 parts | 1× | Double uncoiler, strip joiner and entry accumulator |
| 2 | Cleaning Section 5 parts | 1× | Alkaline degrease, brushing, rinse and dryer |
| 3 | Annealing Furnace 7 parts | 1× | Radiant-tube furnace under reducing atmosphere |
| 4 | Zinc Pot Section 7 parts | 1× | Molten zinc bath and immersed roll hardware |
| 5 | Air Knife Section 5 parts | 1× | Gas wiping knives setting coating weight |
| 6 | Cooling Tower 4 parts | 1× | Post-pot air cooling of the coating |
| 7 | Skin Pass and Leveler 4 parts | 1× | Skin-pass mill and tension leveler |
| 8 | Chemical Treatment 4 parts | 1× | Passivation and oiling before exit |
| 9 | Exit Section 5 parts | 1× | Exit accumulator, shear and recoiler |
| 10 | Drive and Control System 7 parts | 1× | AC drives, PLC and atmosphere control |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Continuous Galvanizing Line
10 top-level lines · 208 rows shown · 1,296 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Entry Section 6 parts | galvanizing-line-entry-section | 1× | 1 | 203 | assembly |
| 1.1 | Pay-off Reel 5 parts | galvanizing-line-uncoiler | 2× | 2 | 29 | assembly |
| 1.1.1 | Expanding Mandrel | galvanizing-line-mandrel | 1× | 2 | · | part |
| 1.1.2 | Mandrel Expansion Cylinder | galvanizing-line-mandrel-cylinder | 1× | 2 | · | part |
| 1.1.3 | Pay-off Gearbox | galvanizing-line-uncoiler-gearbox | 1× | 2 | · | part |
| 1.1.4 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 2 | 24 | assembly |
| 1.1.5 | Ball Bearing | ball-bearing | 2× | 4 | · | part |
| 1.2 | Coil Loading Car | galvanizing-line-coil-car | 1× | 1 | · | part |
| 1.3 | Strip Joiner 4 parts | galvanizing-line-strip-joiner | 1× | 1 | 16 | assembly |
| 1.3.1 | Crop Shear 3 parts + deeper › | galvanizing-line-crop-shear | 1× | 1 | 5 | assembly |
| 1.3.2 | Strip Welder 4 parts + deeper › | galvanizing-line-welder | 1× | 1 | 8 | assembly |
| 1.3.3 | Strip Clamp | galvanizing-line-weld-clamp | 2× | 2 | · | part |
| 1.3.4 | Seam Trimmer | galvanizing-line-seam-trimmer | 1× | 1 | · | part |
| 1.4 | Entry Pinch Roll 4 parts | galvanizing-line-entry-pinch | 1× | 1 | 8 | assembly |
| 1.4.1 | Lower Pinch Roll | galvanizing-line-pinch-roll-lower | 1× | 1 | · | part |
| 1.4.2 | Upper Pinch Roll | galvanizing-line-pinch-roll-upper | 1× | 1 | · | part |
| 1.4.3 | Pneumatic Cylinder | pneumatic-cylinder | 2× | 2 | · | part |
| 1.4.4 | Ball Bearing | ball-bearing | 4× | 4 | · | part |
| 1.5 | Entry Accumulator 5 parts | galvanizing-line-entry-accumulator | 1× | 1 | 60 | assembly |
| 1.5.1 | Accumulator Carriage | galvanizing-line-accumulator-carriage | 1× | 1 | · | part |
| 1.5.2 | Loop Roll | galvanizing-line-loop-roll | 8× | 8 | · | part |
| 1.5.3 | Carriage Hoist Drive 3 parts + deeper › | galvanizing-line-carriage-drive | 1× | 1 | 34 | assembly |
| 1.5.4 | Accumulator Tower | galvanizing-line-accumulator-tower | 1× | 1 | · | part |
| 1.5.5 | Ball Bearing | ball-bearing | 16× | 16 | · | part |
| 1.6 | Entry Bridle 4 parts | galvanizing-line-entry-bridle | 1× | 1 | 60 | assembly |
| 1.6.1 | Bridle Roll | galvanizing-line-bridle-roll | 3× | 3 | · | part |
| 1.6.2 | Bridle Bearing Block 3 parts + deeper › | galvanizing-line-bridle-bearing-block | 6× | 6 | 4 | assembly |
| 1.6.3 | Helical Gearbox 4 parts + deeper › | gearbox | 1× | 1 | 9 | assembly |
| 1.6.4 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 2 | Cleaning Section 5 parts | galvanizing-line-cleaning-section | 1× | 1 | 162 | assembly |
| 2.1 | Degrease Tank 4 parts | galvanizing-line-degrease-tank | 1× | 1 | 34 | assembly |
| 2.1.1 | Process Tank Shell | galvanizing-line-tank-shell | 1× | 1 | · | part |
| 2.1.2 | Spray Header | galvanizing-line-spray-header | 4× | 4 | · | part |
| 2.1.3 | Recirculation Pump 3 parts + deeper › | galvanizing-line-recirc-pump | 1× | 1 | 27 | assembly |
| 2.1.4 | Heating Element | heating-element | 2× | 2 | · | part |
| 2.2 | Brush Scrubber 4 parts | galvanizing-line-brush-scrubber | 2× | 2 | 32 | assembly |
| 2.2.1 | Brush Roll | galvanizing-line-brush-roll | 2× | 4 | · | part |
| 2.2.2 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 2 | 24 | assembly |
| 2.2.3 | Ball Bearing | ball-bearing | 4× | 8 | · | part |
| 2.2.4 | Brush Arbor | galvanizing-line-brush-arbor | 2× | 4 | · | part |
| 2.3 | Rinse Tank 3 parts | galvanizing-line-rinse-tank | 1× | 1 | 30 | assembly |
| 2.3.1 | Process Tank Shell | galvanizing-line-tank-shell | 1× | 1 | · | part |
| 2.3.2 | Spray Header | galvanizing-line-spray-header | 2× | 2 | · | part |
| 2.3.3 | Recirculation Pump 3 parts + deeper › | galvanizing-line-recirc-pump | 1× | 1 | 27 | assembly |
| 2.4 | Wringer Roll | galvanizing-line-squeegee-roll | 2× | 2 | · | part |
| 2.5 | Strip Dryer 3 parts | galvanizing-line-strip-dryer | 1× | 1 | 32 | assembly |
| 2.5.1 | Dryer Blower 2 parts + deeper › | galvanizing-line-dryer-blower | 1× | 1 | 26 | assembly |
| 2.5.2 | Heating Element | heating-element | 2× | 2 | · | part |
| 2.5.3 | Drying Air Nozzle | galvanizing-line-air-nozzle | 4× | 4 | · | part |
| 3 | Annealing Furnace 7 parts | galvanizing-line-annealing-furnace | 1× | 1 | 176 | assembly |
| 3.1 | Preheat Zone 3 parts | galvanizing-line-preheat-zone | 1× | 1 | 28 | assembly |
| 3.1.1 | Furnace Wall Panel | galvanizing-line-furnace-wall | 4× | 4 | · | part |
| 3.1.2 | Radiant Tube | galvanizing-line-radiant-tube | 6× | 6 | · | part |
| 3.1.3 | Recuperative Burner 3 parts + deeper › | galvanizing-line-furnace-burner | 6× | 6 | 3 | assembly |
| 3.2 | Radiant Heating Zone 4 parts | galvanizing-line-radiant-zone | 1× | 1 | 58 | assembly |
| 3.2.1 | Radiant Tube | galvanizing-line-radiant-tube | 12× | 12 | · | part |
| 3.2.2 | Recuperative Burner 3 parts + deeper › | galvanizing-line-furnace-burner | 12× | 12 | 3 | assembly |
| 3.2.3 | Furnace Wall Panel | galvanizing-line-furnace-wall | 6× | 6 | · | part |
| 3.2.4 | Zone Thermocouple | galvanizing-line-zone-thermocouple | 4× | 4 | · | part |
| 3.3 | Soak Zone 3 parts | galvanizing-line-soak-zone | 1× | 1 | 18 | assembly |
| 3.3.1 | Furnace Wall Panel | galvanizing-line-furnace-wall | 6× | 6 | · | part |
| 3.3.2 | Radiant Tube | galvanizing-line-radiant-tube | 8× | 8 | · | part |
| 3.3.3 | Zone Thermocouple | galvanizing-line-zone-thermocouple | 4× | 4 | · | part |
| 3.4 | Jet Cooling Zone 3 parts | galvanizing-line-jet-cool-zone | 1× | 1 | 57 | assembly |
| 3.4.1 | Cooling Gas Fan 2 parts + deeper › | galvanizing-line-cooling-fan | 2× | 2 | 26 | assembly |
| 3.4.2 | Cooling Jet Box | galvanizing-line-jet-box | 4× | 4 | · | part |
| 3.4.3 | Protective Gas Cooler | galvanizing-line-gas-cooler | 1× | 1 | · | part |
| 3.5 | Furnace Snout 3 parts | galvanizing-line-snout | 1× | 1 | 3 | assembly |
| 3.5.1 | Snout Body | galvanizing-line-snout-body | 1× | 1 | · | part |
| 3.5.2 | Snout Atmosphere Seal | galvanizing-line-snout-seal | 1× | 1 | · | part |
| 3.5.3 | Snout Tip | galvanizing-line-snout-tip | 1× | 1 | · | part |
| 3.6 | Atmosphere System 5 parts | galvanizing-line-atmosphere-system | 1× | 1 | 6 | assembly |
| 3.6.1 | Hydrogen Supply Skid | galvanizing-line-h2-supply | 1× | 1 | · | part |
| 3.6.2 | Nitrogen Supply Skid | galvanizing-line-n2-supply | 1× | 1 | · | part |
| 3.6.3 | Dew Point Sensor | galvanizing-line-dewpoint-sensor | 2× | 2 | · | part |
| 3.6.4 | Oxygen Analyzer | galvanizing-line-o2-analyzer | 1× | 1 | · | part |
| 3.6.5 | Gas Mixing Panel | galvanizing-line-gas-mixer | 1× | 1 | · | part |
| 3.7 | Hearth Roll | galvanizing-line-hearth-roll | 6× | 6 | · | part |
| 4 | Zinc Pot Section 7 parts | galvanizing-line-zinc-pot | 1× | 1 | 53 | assembly |
| 4.1 | Zinc Pot Vessel 3 parts | galvanizing-line-pot-vessel | 1× | 1 | 3 | assembly |
| 4.1.1 | Pot Refractory Liner | galvanizing-line-pot-liner | 1× | 1 | · | part |
| 4.1.2 | Pot Steel Shell | galvanizing-line-pot-shell | 1× | 1 | · | part |
| 4.1.3 | Pot Insulation | galvanizing-line-pot-insulation | 1× | 1 | · | part |
| 4.2 | Channel Induction Heater 4 parts | galvanizing-line-induction-heater | 1× | 1 | 4 | assembly |
| 4.2.1 | Induction Coil | galvanizing-line-induction-coil | 1× | 1 | · | part |
| 4.2.2 | Inductor Channel Block | galvanizing-line-inductor-channel | 1× | 1 | · | part |
| 4.2.3 | Power Supply | power-supply | 1× | 1 | · | part |
| 4.2.4 | Inductor Cooling Unit | galvanizing-line-induction-cooling | 1× | 1 | · | part |
| 4.3 | Sink Roll 3 parts | galvanizing-line-sink-roll | 1× | 1 | 5 | assembly |
| 4.3.1 | Sink Roll Body | galvanizing-line-sink-roll-body | 1× | 1 | · | part |
| 4.3.2 | Pot Roll Bearing | galvanizing-line-pot-bearing | 2× | 2 | · | part |
| 4.3.3 | Pot Roll Journal | galvanizing-line-roll-journal | 2× | 2 | · | part |
| 4.4 | Stabilizer Roll | galvanizing-line-stabilizer-roll | 2× | 2 | · | part |
| 4.5 | Pot Roll Support Arm 3 parts | galvanizing-line-pot-roll-arm | 1× | 1 | 4 | assembly |
| 4.5.1 | Pot Support Frame | galvanizing-line-support-frame | 1× | 1 | · | part |
| 4.5.2 | Roll Arm Cylinder | galvanizing-line-arm-cylinder | 2× | 2 | · | part |
| 4.5.3 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 4.6 | Dross Skimmer 3 parts | galvanizing-line-dross-skimmer | 1× | 1 | 34 | assembly |
| 4.6.1 | Skimmer Paddle | galvanizing-line-skimmer-paddle | 1× | 1 | · | part |
| 4.6.2 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 4.6.3 | Helical Gearbox 4 parts + deeper › | gearbox | 1× | 1 | 9 | assembly |
| 4.7 | Zinc Ingot Feeder | galvanizing-line-ingot-feeder | 1× | 1 | · | part |
| 5 | Air Knife Section 5 parts | galvanizing-line-air-knife | 1× | 1 | 92 | assembly |
| 5.1 | Air Knife Header 3 parts | galvanizing-line-knife-header | 2× | 2 | 4 | assembly |
| 5.1.1 | Knife Lip | galvanizing-line-knife-lip | 2× | 4 | · | part |
| 5.1.2 | Knife Plenum | galvanizing-line-knife-plenum | 1× | 2 | · | part |
| 5.1.3 | Fastener Set | fastener-set | 1× | 2 | · | part |
| 5.2 | Air Knife Blower 3 parts | galvanizing-line-knife-blower | 1× | 1 | 27 | assembly |
| 5.2.1 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 5.2.2 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 5.2.3 | Blower Impeller | galvanizing-line-blower-impeller | 1× | 1 | · | part |
| 5.3 | Knife Positioner 3 parts | galvanizing-line-knife-positioner | 1× | 1 | 52 | assembly |
| 5.3.1 | Ball Screw | ball-screw | 2× | 2 | · | part |
| 5.3.2 | Servo Motor 4 parts + deeper › | servo-motor | 2× | 2 | 24 | assembly |
| 5.3.3 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 5.4 | Coating Weight Gauge 3 parts | galvanizing-line-coating-gauge | 1× | 1 | 3 | assembly |
| 5.4.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 5.4.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 5.4.3 | Gauge Source Head | galvanizing-line-gauge-source | 1× | 1 | · | part |
| 5.5 | Edge Baffle | galvanizing-line-edge-baffle | 2× | 2 | · | part |
| 6 | Cooling Tower 4 parts | galvanizing-line-cooling-tower | 1× | 1 | 182 | assembly |
| 6.1 | Air Cooling Box 2 parts | galvanizing-line-cooling-box | 4× | 4 | 32 | assembly |
| 6.1.1 | Drying Air Nozzle | galvanizing-line-air-nozzle | 6× | 24 | · | part |
| 6.1.2 | Cooling Gas Fan 2 parts + deeper › | galvanizing-line-cooling-fan | 1× | 4 | 26 | assembly |
| 6.2 | Tower Cooling Fan 2 parts | galvanizing-line-tower-fan | 2× | 2 | 26 | assembly |
| 6.2.1 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 2 | 24 | assembly |
| 6.2.2 | Ball Bearing | ball-bearing | 2× | 4 | · | part |
| 6.3 | Top Deflector Roll | galvanizing-line-tower-deflector | 1× | 1 | · | part |
| 6.4 | Cooling Tower Frame | galvanizing-line-tower-frame | 1× | 1 | · | part |
| 7 | Skin Pass and Leveler 4 parts | galvanizing-line-skin-pass | 1× | 1 | 76 | assembly |
| 7.1 | Skin-Pass Mill Stand 4 parts | galvanizing-line-temper-mill | 1× | 1 | 13 | assembly |
| 7.1.1 | Temper Work Roll | galvanizing-line-work-roll | 2× | 2 | · | part |
| 7.1.2 | Backup Roll | galvanizing-line-backup-roll | 2× | 2 | · | part |
| 7.1.3 | Mill Housing | galvanizing-line-mill-housing | 1× | 1 | · | part |
| 7.1.4 | Ball Bearing | ball-bearing | 8× | 8 | · | part |
| 7.2 | Tension Leveler 3 parts | galvanizing-line-tension-leveler | 1× | 1 | 25 | assembly |
| 7.2.1 | Leveler Roll | galvanizing-line-leveler-roll | 8× | 8 | · | part |
| 7.2.2 | Leveler Cassette | galvanizing-line-leveler-cassette | 1× | 1 | · | part |
| 7.2.3 | Ball Bearing | ball-bearing | 16× | 16 | · | part |
| 7.3 | Mill Drive Train 3 parts | galvanizing-line-mill-drive | 1× | 1 | 34 | assembly |
| 7.3.1 | Helical Gearbox 4 parts + deeper › | gearbox | 1× | 1 | 9 | assembly |
| 7.3.2 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 7.3.3 | Helical Gear Pair | gear-pair | 1× | 1 | · | part |
| 7.4 | Mill Screwdown 2 parts | galvanizing-line-roll-positioner | 1× | 1 | 4 | assembly |
| 7.4.1 | Pneumatic Cylinder | pneumatic-cylinder | 2× | 2 | · | part |
| 7.4.2 | Pressure Sensor | pressure-sensor | 2× | 2 | · | part |
| 8 | Chemical Treatment 4 parts | galvanizing-line-chemical-treatment | 1× | 1 | 68 | assembly |
| 8.1 | Passivation Coater 3 parts | galvanizing-line-passivation-unit | 1× | 1 | 30 | assembly |
| 8.1.1 | Coater Roll | galvanizing-line-coater-roll | 2× | 2 | · | part |
| 8.1.2 | Recirculation Pump 3 parts + deeper › | galvanizing-line-recirc-pump | 1× | 1 | 27 | assembly |
| 8.1.3 | Process Tank Shell | galvanizing-line-tank-shell | 1× | 1 | · | part |
| 8.2 | Treatment Dryer 3 parts | galvanizing-line-treatment-dryer | 1× | 1 | 32 | assembly |
| 8.2.1 | Heating Element | heating-element | 2× | 2 | · | part |
| 8.2.2 | Dryer Blower 2 parts + deeper › | galvanizing-line-dryer-blower | 1× | 1 | 26 | assembly |
| 8.2.3 | Drying Air Nozzle | galvanizing-line-air-nozzle | 4× | 4 | · | part |
| 8.3 | Electrostatic Oiler 3 parts | galvanizing-line-oiler | 1× | 1 | 4 | assembly |
| 8.3.1 | Oil Metering Pump | galvanizing-line-oil-pump | 1× | 1 | · | part |
| 8.3.2 | Charged Spray Electrode | galvanizing-line-spray-electrode | 2× | 2 | · | part |
| 8.3.3 | Power Supply | power-supply | 1× | 1 | · | part |
| 8.4 | Wringer Roll | galvanizing-line-squeegee-roll | 2× | 2 | · | part |
| 9 | Exit Section 5 parts | galvanizing-line-exit-section | 1× | 1 | 155 | assembly |
| 9.1 | Exit Accumulator 5 parts | galvanizing-line-exit-accumulator | 1× | 1 | 60 | assembly |
| 9.1.1 | Accumulator Carriage | galvanizing-line-accumulator-carriage | 1× | 1 | · | part |
| 9.1.2 | Loop Roll | galvanizing-line-loop-roll | 8× | 8 | · | part |
| 9.1.3 | Carriage Hoist Drive 3 parts + deeper › | galvanizing-line-carriage-drive | 1× | 1 | 34 | assembly |
| 9.1.4 | Accumulator Tower | galvanizing-line-accumulator-tower | 1× | 1 | · | part |
| 9.1.5 | Ball Bearing | ball-bearing | 16× | 16 | · | part |
| 9.2 | Exit Bridle 4 parts | galvanizing-line-exit-bridle | 1× | 1 | 60 | assembly |
| 9.2.1 | Bridle Roll | galvanizing-line-bridle-roll | 3× | 3 | · | part |
| 9.2.2 | Bridle Bearing Block 3 parts + deeper › | galvanizing-line-bridle-bearing-block | 6× | 6 | 4 | assembly |
| 9.2.3 | Helical Gearbox 4 parts + deeper › | gearbox | 1× | 1 | 9 | assembly |
| 9.2.4 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 9.3 | Exit Shear 3 parts | galvanizing-line-exit-shear | 1× | 1 | 5 | assembly |
| 9.3.1 | Shear Blade | galvanizing-line-shear-blade | 2× | 2 | · | part |
| 9.3.2 | Pneumatic Cylinder | pneumatic-cylinder | 2× | 2 | · | part |
| 9.3.3 | Shear Frame | galvanizing-line-shear-frame | 1× | 1 | · | part |
| 9.4 | Recoiler 5 parts | galvanizing-line-recoiler | 1× | 1 | 29 | assembly |
| 9.4.1 | Expanding Mandrel | galvanizing-line-mandrel | 1× | 1 | · | part |
| 9.4.2 | Mandrel Expansion Cylinder | galvanizing-line-mandrel-cylinder | 1× | 1 | · | part |
| 9.4.3 | Recoiler Gearbox | galvanizing-line-recoiler-gearbox | 1× | 1 | · | part |
| 9.4.4 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 9.4.5 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 9.5 | Belt Wrapper | galvanizing-line-belt-wrapper | 1× | 1 | · | part |
| 10 | Drive and Control System 7 parts | galvanizing-line-drive-control | 1× | 1 | 129 | assembly |
| 10.1 | AC Drive 4 parts | galvanizing-line-ac-drive | 8× | 8 | 12 | assembly |
| 10.1.1 | Bare PCB | pcb-bare | 1× | 8 | · | part |
| 10.1.2 | IGBT Power Module | igbt-module | 6× | 48 | · | part |
| 10.1.3 | DC-Link Capacitor | dc-link-cap | 4× | 32 | · | part |
| 10.1.4 | Microcontroller | mcu | 1× | 8 | · | part |
| 10.2 | Drive Cabinet 4 parts | galvanizing-line-drive-cabinet | 1× | 1 | 10 | assembly |
| 10.2.1 | Sheet Metal Panel | sheet-panel | 6× | 6 | · | part |
| 10.2.2 | Power Supply | power-supply | 1× | 1 | · | part |
| 10.2.3 | Cabinet Cooling Fan | galvanizing-line-cabinet-fan | 2× | 2 | · | part |
| 10.2.4 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 10.3 | Line PLC 4 parts | galvanizing-line-line-plc | 1× | 1 | 8 | assembly |
| 10.3.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 10.3.2 | Microcontroller | mcu | 2× | 2 | · | part |
| 10.3.3 | PLC I/O Module | galvanizing-line-io-module | 4× | 4 | · | part |
| 10.3.4 | Power Supply | power-supply | 1× | 1 | · | part |
| 10.4 | Operator HMI 3 parts | galvanizing-line-hmi | 1× | 1 | 3 | assembly |
| 10.4.1 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 10.4.2 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 10.4.3 | Microcontroller | mcu | 1× | 1 | · | part |
| 10.5 | Remote I/O Rack | galvanizing-line-io-rack | 3× | 3 | · | part |
| 10.6 | Tensiometer Roll 2 parts | galvanizing-line-tension-meter | 2× | 2 | 4 | assembly |
| 10.6.1 | Tension Load Cell | galvanizing-line-load-cell | 2× | 4 | · | part |
| 10.6.2 | Ball Bearing | ball-bearing | 2× | 4 | · | part |
| 10.7 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Investment Casting Shell Line
869 parts · shares 24 with this page
Casting Fettling Machine
802 parts · shares 22 with this page
Cast Film Extrusion Line
406 parts · shares 22 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $5k–$2M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| atlascopco.com ↗ | Stockholm, SE | Compressors & industrial | 10 units | 12–20 wks |
|
🇦🇹Andritz
andritz.com ↗
|
Graz, AT | Process plants & machinery | 10 units | 12–20 wks |
| buhlergroup.com ↗ | Uzwil, CH | Food & materials processing | 10 units | 12–20 wks |
| gea.com ↗ | Düsseldorf, DE | Process technology | 10 units | 12–20 wks |
| mhi.com ↗ | Tokyo, JP | Heavy machinery | 10 units | 12–20 wks |
1,123-word article