All-Electric Injection Molding Machine
ProductOverview
An all-electric injection molding machine replaces every hydraulic cylinder and the central pump with servo motors and ball screws. Each function, clamp, injection, screw rotation, ejection, and carriage, has its own dedicated servo axis driven from a shared Servo Drive Cabinet cabinet. There is no oil tank, no pump running continuously, and no hydraulic valves. The result is lower energy use, faster and more repeatable motion, no oil contamination, and quieter operation, which is why these machines dominate medical, optical, electronics, and clean-room molding. The trade-off is higher purchase cost and tonnage that historically topped out lower than the largest hydraulic machines.
Electric injection unit
The Electric Injection Unit uses two motors. The Plasticizing Motor turns the Reciprocating Screw through an Toothed Belt Drive to melt and meter the shot, just as the screw does on any machine. The injection stroke is different: the Injection Ball-Screw Drive uses a servo turning two ball screws to push the screw forward linearly. An Injection Force Load Cell measures injection force directly so the controller can hold a precise pressure profile, and the Thrust Bearing carries the axial load. The Injection Carriage runs on its own servo screw to seat the Injection Nozzle against the mold. Because the injection axis has no oil compressibility in the way, the response is faster and the shot-to-shot weight variation is smaller than on a hydraulic machine.
Electric clamp unit
The Electric Clamp Unit keeps the familiar toggle geometry but drives the Crosshead with the Clamp Ball-Screw Drive instead of a hydraulic cylinder. A servo turns a high-lead ball screw that pushes the crosshead, the Toggle Linkage links straighten to multiply force into clamp tonnage and lock near top-dead-center, and an Clamp Position Encoder reports position so mold-open and mold-close profiles can be shaped for fast, gentle motion. The mold halves bolt to the Fixed Platen and Moving Platen guided on four Tie Bar columns. Part release is handled by the separate Electric Ejector, a servo ball-screw ejector whose stroke and force are programmable, which protects thin or delicate parts.
Servo drives and energy
The Servo Drive Cabinet cabinet holds one Servo Amplifier per axis, each switching an IGBT Power Module, all sharing one Shared DC Bus. The energy story is the main selling point: a servo only draws power while its axis is moving, so during cooling and idle the machine draws almost nothing, unlike a hydraulic pump that runs all cycle. A Regenerative Unit captures the energy of clamp deceleration and returns it to the bus rather than burning it in a resistor, and a Line Reactor smooths the supply. Total energy use is commonly 30 to 60 percent below a comparable hydraulic machine.
Heating and control
The Barrel Heating System is the same as any machine: a Barrel Band Heater per barrel zone, each built on a Heating Element, with a Zone Thermocouple per zone. The Control System is where an electric machine is more demanding than hydraulic: the Motion Controller must coordinate five servo axes with tight position and force loops, achieving ±0.01 mm repeatability on screw position. The operator sets velocity and pressure profiles on the HMI Touchscreen.
Safety
The Safety System keeps the interlocked Sliding Safety Gate and Interlock Switch chain of any molding machine, but adds a Safe-Torque-Off Module that removes torque from the servo amplifiers when a guard opens, a faster and more certain stop than dumping hydraulic pressure. The Emergency Stop cuts the drive enable directly.
Materials, variants, and use
All-electric machines are the standard for precision parts: optical lenses, connectors, syringes, micro gears, and thin-wall packaging where weight repeatability and clean operation matter. The absence of hydraulic oil makes them suitable for clean rooms and food-contact molding. Hybrid machines exist that keep an electric injection axis but use a hydraulic clamp for high tonnage, splitting the difference on cost. The largest all-electric machines have grown past 450 t as ball-screw and servo sizes increased, narrowing the old tonnage gap. The Base Frame is shorter and lighter than a hydraulic machine of the same tonnage because there is no oil tank or cooler to carry.
The maintenance profile differs from a hydraulic machine. There is no oil to filter, sample, or change, and no seals to weep, which removes a class of housekeeping and contamination problems. The wear items become the Injection Ball-Screw Drive and the Clamp Ball-Screw Drive, which need periodic lubrication and eventually replacement after many million cycles; a worn ball screw shows up as lost position accuracy long before it fails. The Toggle Linkage pivot pins and bushings still wear as on any toggle machine. Because each axis is independent, the machine can run motions in parallel that a single hydraulic pump must run in sequence, for example recharging the screw while the clamp opens, which trims cycle time further. This parallelism plus the energy savings is why the higher purchase price is usually recovered over the machine's life in high-volume production.
All-Electric Injection Molding Machine parts and their functions
8 top-level parts · 851 parts in total · full bill of materials below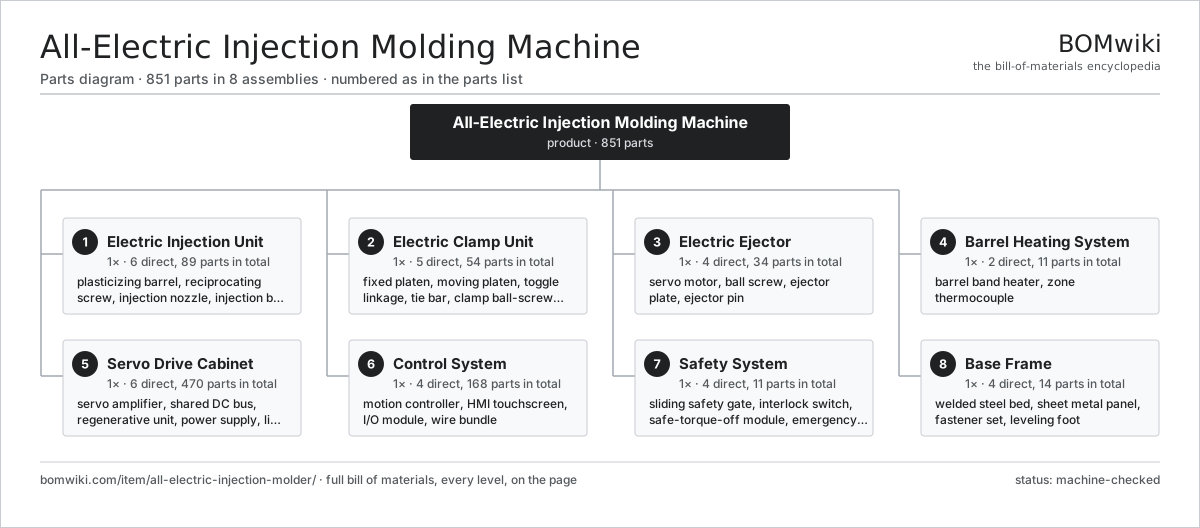
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Electric Injection Unit 6 parts | 1× | Two servo motors drive screw rotation and a ball-screw injection stroke. |
| 2 | Electric Clamp Unit 5 parts | 1× | Servo ball-screw drives a toggle that closes the mold and builds tonnage. |
| 3 | Electric Ejector 4 parts | 1× | Servo ball-screw ejector with programmable stroke and force. |
| 4 | Barrel Heating System 2 parts | 1× | Zoned band heaters and thermocouples for the melt profile. |
| 5 | Servo Drive Cabinet 6 parts | 1× | Amplifiers, regen unit, and DC bus feeding all axis motors. |
| 6 | Control System 4 parts | 1× | Motion controller closing position and force loops on every axis. |
| 7 | Safety System 4 parts | 1× | Interlocked guards plus safe-torque-off on the servo drives. |
| 8 | Base Frame 4 parts | 1× | Welded bed with no oil tank, carrying clamp and injection units. |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for All-Electric Injection Molding Machine
8 top-level lines · 86 rows shown · 851 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Electric Injection Unit 6 parts | all-electric-injection-molder-injection-unit | 1× | 1 | 89 | assembly |
| 1.1 | Plasticizing Barrel 2 parts | all-electric-injection-molder-barrel | 1× | 1 | 2 | assembly |
| 1.1.1 | Barrel Tube | all-electric-injection-molder-barrel-tube | 1× | 1 | · | part |
| 1.1.2 | Water-Cooled Feed Throat | all-electric-injection-molder-feed-throat | 1× | 1 | · | part |
| 1.2 | Reciprocating Screw 2 parts | all-electric-injection-molder-screw | 1× | 1 | 2 | assembly |
| 1.2.1 | Screw Body | all-electric-injection-molder-screw-body | 1× | 1 | · | part |
| 1.2.2 | Non-Return Check Ring | all-electric-injection-molder-check-ring | 1× | 1 | · | part |
| 1.3 | Injection Nozzle 1 parts | all-electric-injection-molder-nozzle | 1× | 1 | · | part |
| 1.3.1 | Heating Element | heating-element | 1× | 1 | · | part |
| 1.4 | Injection Ball-Screw Drive 5 parts | all-electric-injection-molder-injection-ballscrew | 1× | 1 | 30 | assembly |
| 1.4.1 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 1.4.2 | Ball Screw | ball-screw | 2× | 2 | · | part |
| 1.4.3 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 1.4.4 | Thrust Bearing 1 parts + deeper › | all-electric-injection-molder-thrust-bearing | 1× | 1 | · | part |
| 1.4.5 | Injection Force Load Cell | all-electric-injection-molder-load-cell | 1× | 1 | · | part |
| 1.5 | Plasticizing Motor 3 parts | all-electric-injection-molder-plasticizing-motor | 1× | 1 | 27 | assembly |
| 1.5.1 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 1.5.2 | Toothed Belt Drive 1 parts + deeper › | all-electric-injection-molder-belt-drive | 1× | 1 | · | part |
| 1.5.3 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 1.6 | Injection Carriage 3 parts | all-electric-injection-molder-carriage | 1× | 1 | 27 | assembly |
| 1.6.1 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 1.6.2 | Carriage Ball Screw 1 parts + deeper › | all-electric-injection-molder-carriage-screw | 1× | 1 | · | part |
| 1.6.3 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 2 | Electric Clamp Unit 5 parts | all-electric-injection-molder-clamp-unit | 1× | 1 | 54 | assembly |
| 2.1 | Fixed Platen | all-electric-injection-molder-fixed-platen | 1× | 1 | · | part |
| 2.2 | Moving Platen | all-electric-injection-molder-moving-platen | 1× | 1 | · | part |
| 2.3 | Toggle Linkage 3 parts | all-electric-injection-molder-toggle | 1× | 1 | 19 | assembly |
| 2.3.1 | Toggle Link | all-electric-injection-molder-toggle-link | 8× | 8 | · | part |
| 2.3.2 | Toggle Pin | all-electric-injection-molder-toggle-pin | 10× | 10 | · | part |
| 2.3.3 | Crosshead | all-electric-injection-molder-crosshead | 1× | 1 | · | part |
| 2.4 | Tie Bar | all-electric-injection-molder-tie-bar | 4× | 4 | · | part |
| 2.5 | Clamp Ball-Screw Drive 4 parts | all-electric-injection-molder-clamp-ballscrew | 1× | 1 | 29 | assembly |
| 2.5.1 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 2.5.2 | Ball Screw | ball-screw | 2× | 2 | · | part |
| 2.5.3 | Clamp Position Encoder | all-electric-injection-molder-clamp-encoder | 1× | 1 | · | part |
| 2.5.4 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 3 | Electric Ejector 4 parts | all-electric-injection-molder-ejector-drive | 1× | 1 | 34 | assembly |
| 3.1 | Servo Motor 4 parts | servo-motor | 1× | 1 | 24 | assembly |
| 3.1.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 1 | 3 | assembly |
| 3.1.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 1 | 19 | assembly |
| 3.1.3 | Encoder | encoder | 1× | 1 | · | part |
| 3.1.4 | Motor Housing | motor-housing | 1× | 1 | · | part |
| 3.2 | Ball Screw | ball-screw | 1× | 1 | · | part |
| 3.3 | Ejector Plate | all-electric-injection-molder-ejector-plate | 1× | 1 | · | part |
| 3.4 | Ejector Pin | all-electric-injection-molder-ejector-pin | 8× | 8 | · | part |
| 4 | Barrel Heating System 2 parts | all-electric-injection-molder-heating-system | 1× | 1 | 11 | assembly |
| 4.1 | Barrel Band Heater 1 parts | all-electric-injection-molder-band-heater | 5× | 5 | · | part |
| 4.1.1 | Heating Element | heating-element | 1× | 5 | · | part |
| 4.2 | Zone Thermocouple | all-electric-injection-molder-thermocouple | 6× | 6 | · | part |
| 5 | Servo Drive Cabinet 6 parts | all-electric-injection-molder-servo-drives | 1× | 1 | 470 | assembly |
| 5.1 | Servo Amplifier 4 parts | all-electric-injection-molder-servo-amplifier | 5× | 5 | 93 | assembly |
| 5.1.1 | Bare PCB | pcb-bare | 1× | 5 | · | part |
| 5.1.2 | Microcontroller | mcu | 1× | 5 | · | part |
| 5.1.3 | SMD Passive (R/C/L) | smd-passives | 90× | 450 | · | part |
| 5.1.4 | IGBT Power Module | all-electric-injection-molder-igbt-module | 1× | 5 | · | part |
| 5.2 | Shared DC Bus | all-electric-injection-molder-dc-bus | 1× | 1 | · | part |
| 5.3 | Regenerative Unit | all-electric-injection-molder-regen-unit | 1× | 1 | · | part |
| 5.4 | Power Supply | power-supply | 1× | 1 | · | part |
| 5.5 | Line Reactor | all-electric-injection-molder-line-reactor | 1× | 1 | · | part |
| 5.6 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 6 | Control System 4 parts | all-electric-injection-molder-control-system | 1× | 1 | 168 | assembly |
| 6.1 | Motion Controller 4 parts | all-electric-injection-molder-motion-controller | 1× | 1 | 142 | assembly |
| 6.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 6.1.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 6.1.3 | SMD Passive (R/C/L) | smd-passives | 130× | 130 | · | part |
| 6.1.4 | Connector | connector | 10× | 10 | · | part |
| 6.2 | HMI Touchscreen 3 parts | all-electric-injection-molder-hmi | 1× | 1 | 3 | assembly |
| 6.2.1 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 6.2.2 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 6.2.3 | Microcontroller | mcu | 1× | 1 | · | part |
| 6.3 | I/O Module 3 parts | all-electric-injection-molder-io-module | 2× | 2 | 11 | assembly |
| 6.3.1 | Bare PCB | pcb-bare | 1× | 2 | · | part |
| 6.3.2 | Relay | relay | 6× | 12 | · | part |
| 6.3.3 | Connector | connector | 4× | 8 | · | part |
| 6.4 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 7 | Safety System 4 parts | all-electric-injection-molder-safety-system | 1× | 1 | 11 | assembly |
| 7.1 | Sliding Safety Gate 1 parts | all-electric-injection-molder-safety-gate | 2× | 2 | · | part |
| 7.1.1 | Sheet Metal Panel | sheet-panel | 2× | 4 | · | part |
| 7.2 | Interlock Switch | all-electric-injection-molder-safety-switch | 4× | 4 | · | part |
| 7.3 | Safe-Torque-Off Module | all-electric-injection-molder-sto-module | 1× | 1 | · | part |
| 7.4 | Emergency Stop | all-electric-injection-molder-estop | 2× | 2 | · | part |
| 8 | Base Frame 4 parts | all-electric-injection-molder-base-frame | 1× | 1 | 14 | assembly |
| 8.1 | Welded Steel Bed | all-electric-injection-molder-bed | 1× | 1 | · | part |
| 8.2 | Sheet Metal Panel | sheet-panel | 6× | 6 | · | part |
| 8.3 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 8.4 | Leveling Foot | all-electric-injection-molder-leveling-foot | 6× | 6 | · | part |
Related products
same domain, ranked by shared parts Industrial Ultrasonic Cleaner
787 parts · shares 23 with this page
Powder Coating Line
5,418 parts · shares 23 with this page
 Rubber Extrusion Line
524 parts · shares 22 with this page
 Tensile Testing Machine
608 parts · shares 22 with this page
Micro Injection Molding Machine
704 parts · shares 22 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $5k–$2M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| atlascopco.com ↗ | Stockholm, SE | Compressors & industrial | 10 units | 12–20 wks |
|
🇦🇹Andritz
andritz.com ↗
|
Graz, AT | Process plants & machinery | 10 units | 12–20 wks |
| buhlergroup.com ↗ | Uzwil, CH | Food & materials processing | 10 units | 12–20 wks |
| gea.com ↗ | Düsseldorf, DE | Process technology | 10 units | 12–20 wks |
| mhi.com ↗ | Tokyo, JP | Heavy machinery | 10 units | 12–20 wks |
982-word article