Wax Pattern Injection Press
ProductOverview
A wax pattern injection press makes the wax copies that start the investment casting process. Soft pattern wax is pushed under pressure into a metal die whose cavity is the shape of the part. The wax sets in seconds, and the pattern is ejected, then later assembled with others onto a wax sprue and coated with ceramic to build the casting shell. Because every dimension of the final metal casting traces back to this wax pattern, the press has to fill the die completely, pack it firmly enough to avoid sink marks, and release the pattern without bending it. Pattern wax is not a true liquid at injection: it is held as a semi-solid slurry so it fills smoothly with low shrinkage, which makes wax handling the defining feature of these presses compared to plastic injection machines.
The press reacts its forces through a Press Frame carrying a Clamp Unit that holds the die shut while the Injection Unit fills it. Wax is held ready in the Wax Conditioner, every zone is held by the Temperature Control system, and the Hydraulic Power Unit and Control System drive and sequence the shot behind the Safety and Guarding guards.
How a shot works
A cycle begins with the Clamp Cylinder closing the two die halves and holding them under clamp force on the Moving Platen. The Heated Nozzle mates the die sprue, the Shutoff Valve opens, and the Injection Cylinder drives the Wax Piston forward to push wax into the cavity. The Proportional Valve proportional valves shape the shot, fast fill to avoid cold shut, then a slower pack-and-hold that feeds shrinkage as the wax solidifies. The cavity-pressure reading from the Wax Flow Meter and the Pressure Sensor confirms the cavity is full and packed. The die, cooled by the Die Chiller, sets the wax in seconds, the clamp opens, and the Ejector Mechanism pins lift the soft pattern clear. Hold and cool times dominate the cycle because rushing them warps the pattern.
Wax conditioning
Pattern wax behaves well only inside a narrow temperature and consistency window, so the Wax Conditioner is as important as the injection unit. The Conditioning Tank holds the wax as a controlled slurry of solid and liquid, kept uniform by a Tank Stirrer and held to temperature by a Heating Jacket. Injecting wax as a paste rather than a free liquid cuts shrinkage and avoids the surface defects a fully molten shot would leave. A Transfer Pump feeds conditioned wax to the injection cylinder, and a Reclaim Filter cleans returned sprues and runner wax so they can be remelted into the batch, since pattern wax is expensive and reused many times.
Temperature control
Three zones must be held steady at once. The Temperature Control system runs separate loops on the wax tank, the Heated Nozzle and the die, each with its own Thermocouple feeding the Temperature Controller. The tank holds the wax at injection consistency, the nozzle is held just above the wax melt point so it never freezes off between shots, and the die is actively chilled by the Die Chiller so the pattern sets fast. A few degrees of drift on any zone changes shot weight, surface finish or shrinkage, so the loops are tuned tight and logged.
Clamp, frame and ejection
The wax shot pressure is modest next to plastic injection, but the clamp must still hold the die dead flat so no wax flashes the parting line. The Press Frame reacts that force through Tie Bar bars between the fixed and moving platens, and Linear Guide Rail rails keep the moving platen square as it closes. Because wax patterns are fragile and warp easily, the Ejector Mechanism uses many pins driven together at low, even force off the Ejector Bar, with Coil Spring returns, so the pattern lifts straight off the cavity rather than being pushed off a few points.
Variants and use
Presses range from small bench units of a couple of tonnes clamp for jewelry and dental patterns up to floor machines of fifty tonnes for large industrial castings. Some run a single fixed die; production cells use quick-change Die Mounting Plate plates so dies swap in minutes between patterns. The whole shot is profiled and stored by the PLC and set up on the Operator HMI, where an operator keeps a recipe of injection speed, pressure, hold, cool and temperatures for each die. Because the moving clamp can crush a hand, the Safety Gate and Light Curtain block any motion while the loading face is open, and the E-Stop Button buttons drop pressure and heat together. The wax patterns it produces feed straight onto the trees built by an investment casting shell line.
Wax Pattern Injection Press parts and their functions
8 top-level parts · 107 parts in total · full bill of materials below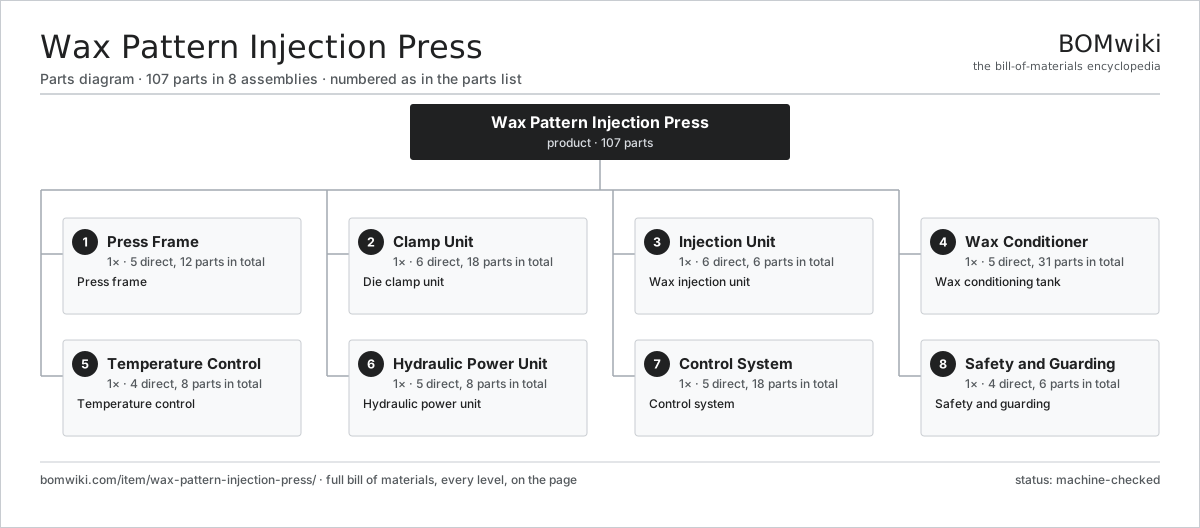
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Press Frame 5 parts | 1× | Press frame |
| 2 | Clamp Unit 6 parts | 1× | Die clamp unit |
| 3 | Injection Unit 6 parts | 1× | Wax injection unit |
| 4 | Wax Conditioner 5 parts | 1× | Wax conditioning tank |
| 5 | Temperature Control 4 parts | 1× | Temperature control |
| 6 | Hydraulic Power Unit 5 parts | 1× | Hydraulic power unit |
| 7 | Control System 5 parts | 1× | Control system |
| 8 | Safety and Guarding 4 parts | 1× | Safety and guarding |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Wax Pattern Injection Press
8 top-level lines · 61 rows shown · 107 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Press Frame 5 parts | wax-pattern-injection-press-frame | 1× | 1 | 12 | assembly |
| 1.1 | Frame Weldment | wax-pattern-injection-press-frame-weldment | 1× | 1 | · | part |
| 1.2 | Tie Bar | wax-pattern-injection-press-tie-bar | 4× | 4 | · | part |
| 1.3 | Fixed Platen | wax-pattern-injection-press-fixed-platen | 1× | 1 | · | part |
| 1.4 | Leveling Foot | wax-pattern-injection-press-leveling-foot | 4× | 4 | · | part |
| 1.5 | Fastener Set | fastener-set | 2× | 2 | · | part |
| 2 | Clamp Unit 6 parts | wax-pattern-injection-press-clamp | 1× | 1 | 18 | assembly |
| 2.1 | Moving Platen | wax-pattern-injection-press-moving-platen | 1× | 1 | · | part |
| 2.2 | Clamp Cylinder | wax-pattern-injection-press-clamp-cylinder | 1× | 1 | · | part |
| 2.3 | Die Mounting Plate | wax-pattern-injection-press-die-mount | 2× | 2 | · | part |
| 2.4 | Ejector Mechanism 3 parts | wax-pattern-injection-press-ejector | 1× | 1 | 11 | assembly |
| 2.4.1 | Ejector Bar | wax-pattern-injection-press-ejector-bar | 1× | 1 | · | part |
| 2.4.2 | Ejector Pin | wax-pattern-injection-press-ejector-pin | 6× | 6 | · | part |
| 2.4.3 | Coil Spring | coil-spring | 4× | 4 | · | part |
| 2.5 | Linear Guide Rail | linear-guide | 2× | 2 | · | part |
| 2.6 | O-Ring Set | oring-set | 1× | 1 | · | part |
| 3 | Injection Unit 6 parts | wax-pattern-injection-press-injection-unit | 1× | 1 | 6 | assembly |
| 3.1 | Injection Cylinder | wax-pattern-injection-press-inj-cylinder | 1× | 1 | · | part |
| 3.2 | Heated Nozzle | wax-pattern-injection-press-nozzle | 1× | 1 | · | part |
| 3.3 | Shutoff Valve | wax-pattern-injection-press-shutoff-valve | 1× | 1 | · | part |
| 3.4 | Wax Piston | wax-pattern-injection-press-wax-piston | 1× | 1 | · | part |
| 3.5 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 3.6 | Wax Flow Meter | wax-pattern-injection-press-flow-meter | 1× | 1 | · | part |
| 4 | Wax Conditioner 5 parts | wax-pattern-injection-press-wax-conditioner | 1× | 1 | 31 | assembly |
| 4.1 | Conditioning Tank | wax-pattern-injection-press-wax-tank | 1× | 1 | · | part |
| 4.2 | Tank Stirrer 3 parts | wax-pattern-injection-press-wax-stirrer | 1× | 1 | 27 | assembly |
| 4.2.1 | Stirrer Blade | wax-pattern-injection-press-stirrer-blade | 1× | 1 | · | part |
| 4.2.2 | Servo Motor 4 parts + deeper › | servo-motor | 1× | 1 | 24 | assembly |
| 4.2.3 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 4.3 | Heating Jacket | wax-pattern-injection-press-wax-jacket | 1× | 1 | · | part |
| 4.4 | Transfer Pump | wax-pattern-injection-press-wax-pump | 1× | 1 | · | part |
| 4.5 | Reclaim Filter | wax-pattern-injection-press-reclaim-filter | 1× | 1 | · | part |
| 5 | Temperature Control 4 parts | wax-pattern-injection-press-temp-control | 1× | 1 | 8 | assembly |
| 5.1 | Heating Element | heating-element | 2× | 2 | · | part |
| 5.2 | Thermocouple | wax-pattern-injection-press-thermocouple | 4× | 4 | · | part |
| 5.3 | Temperature Controller | wax-pattern-injection-press-temp-controller | 1× | 1 | · | part |
| 5.4 | Die Chiller | wax-pattern-injection-press-chiller | 1× | 1 | · | part |
| 6 | Hydraulic Power Unit 5 parts | wax-pattern-injection-press-hydraulics | 1× | 1 | 8 | assembly |
| 6.1 | Hydraulic Pump | wax-pattern-injection-press-hpu-pump | 1× | 1 | · | part |
| 6.2 | Pump Motor | wax-pattern-injection-press-hpu-motor | 1× | 1 | · | part |
| 6.3 | Accumulator | wax-pattern-injection-press-accumulator | 1× | 1 | · | part |
| 6.4 | Proportional Valve | wax-pattern-injection-press-hpu-valve | 4× | 4 | · | part |
| 6.5 | Oil Tank | wax-pattern-injection-press-hpu-tank | 1× | 1 | · | part |
| 7 | Control System 5 parts | wax-pattern-injection-press-control | 1× | 1 | 18 | assembly |
| 7.1 | PLC 4 parts | wax-pattern-injection-press-plc | 1× | 1 | 7 | assembly |
| 7.1.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 7.1.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 7.1.3 | Relay | relay | 4× | 4 | · | part |
| 7.1.4 | SMD Passive (R/C/L) | smd-passives | 1× | 1 | · | part |
| 7.2 | Operator HMI 3 parts | wax-pattern-injection-press-hmi | 1× | 1 | 3 | assembly |
| 7.2.1 | LCD Panel | lcd-panel | 1× | 1 | · | part |
| 7.2.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 7.2.3 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 7.3 | Power Supply | power-supply | 1× | 1 | · | part |
| 7.4 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 7.5 | Connector | connector | 6× | 6 | · | part |
| 8 | Safety and Guarding 4 parts | wax-pattern-injection-press-safety | 1× | 1 | 6 | assembly |
| 8.1 | Safety Gate | wax-pattern-injection-press-safety-gate | 1× | 1 | · | part |
| 8.2 | Light Curtain | wax-pattern-injection-press-light-curtain | 1× | 1 | · | part |
| 8.3 | E-Stop Button | wax-pattern-injection-press-estop | 2× | 2 | · | part |
| 8.4 | Sheet Metal Panel | sheet-panel | 2× | 2 | · | part |
Related products
same domain, ranked by shared parts Rubber Extrusion Line
524 parts · shares 23 with this page
Powder Coating Line
5,418 parts · shares 23 with this page
Casting Fettling Machine
802 parts · shares 22 with this page
Spin Welding Machine
91 parts · shares 21 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $5k–$2M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| atlascopco.com ↗ | Stockholm, SE | Compressors & industrial | 10 units | 12–20 wks |
|
🇦🇹Andritz
andritz.com ↗
|
Graz, AT | Process plants & machinery | 10 units | 12–20 wks |
| buhlergroup.com ↗ | Uzwil, CH | Food & materials processing | 10 units | 12–20 wks |
| gea.com ↗ | Düsseldorf, DE | Process technology | 10 units | 12–20 wks |
| mhi.com ↗ | Tokyo, JP | Heavy machinery | 10 units | 12–20 wks |
926-word article