Resin Drying Hopper
ProductOverview
A resin drying hopper removes the surface and absorbed moisture from plastic pellets before they go into an injection molding machine or extruder. Most engineering resins pick up water from the air, and if that water is still present when the plastic melts it causes splay marks, bubbles, weak parts, and in some resins permanent chemical degradation. The hopper solves this by holding the pellets in a heated, ventilated bed: the Drying Vessel holds the resin, the Process Heater warms a stream of air, the Process Blower drives that air up through the bed and back through the Return Air Filter, the Vacuum Loader keeps the vessel full, and the Temperature Controller holds the temperature, with the whole unit carried on a Mounting Frame.
The simplest version is a hot-air hopper that heats ambient air. For resins that absorb water deeply, such as PA, PC, and PET, a desiccant dryer is used instead because it supplies very dry air, but the hopper vessel and airflow design are much the same. This hopper covers the hot-air case while sharing the construction of the desiccant type.
The drying vessel
The Drying Vessel is built to hold resin at temperature with even airflow. A stainless Inner Cone holds the pellets and is shaped for mass flow, so the resin moves down in an even column and every pellet gets the same drying time rather than channeling. An Outer Shell surrounds it with a Insulation Blanket blanket between them to keep heat in and the outside cool to touch. A Sight Glass lets the operator check the resin level, and a Discharge Slide at the cone tip feeds dried resin to the machine throat. Mass-flow geometry matters here because a hopper that lets resin funnel down the center would deliver some pellets dried and others barely warmed.
Heating and air delivery
Drying works by passing hot air through the resin so it carries moisture away, and the Process Heater sets the air temperature. Several Heating Element units in a Heater Housing warm the recirculating air to the temperature the resin needs, with Air Thermocouple sensors reading both delivery and return air and a Thermal Fuse cutting power if the heater runs away. The hot air enters through the Air Inlet Diffuser, where a Diffuser Cone turns the stream upward and a Spreader Plate evens it across the base so the entire bed sees the same airflow. Even distribution is what makes the difference between uniformly dried resin and a hopper with dry edges and a wet core.
The air loop
The Process Blower keeps the air moving in a closed loop. A Blower Impeller turned by a Blower Motor in a Blower Housing pulls return air through the heater and pushes it up through the resin, where the air picks up moisture, then draws it back out the top of the vessel. Running the air in a closed loop saves energy because the air is already warm on its return, and it keeps shop dust out of the resin. Before the return air reaches the blower it passes through the Return Air Filter, whose Filter Cartridge in a Filter Housing sealed by a Filter Seal traps the fine dust that resin sheds, protecting the heater and impeller from buildup.
Keeping the hopper full
A drying hopper only works if it stays full, because the resin must spend enough time in the heated bed to dry. The Vacuum Loader handles refilling: a Vacuum Pump pulls fresh resin from the supply into a Vacuum Receiver at the top of the vessel, and when a Level Probe senses the level has dropped, the Dump Valve opens to drop the conveyed resin in. By topping up from the top while the machine draws from the bottom, the loader keeps the bed depth and therefore the residence time roughly constant.
Control and protection
The Temperature Controller holds the drying conditions steady. Its controller runs a PID loop on the Air Thermocouple reading, switching the Heating Element units through a Relay bank to hold the air at the setpoint shown on the Operator Display. The same controller triggers the Vacuum Loader on the level probe signal and raises an alarm if the temperature strays or the airflow drops. Because too much heat can melt or yellow the resin, the controller also enforces limits and works alongside the Thermal Fuse as a backup against overheating.
Resins, settings, and use
Drying conditions depend entirely on the resin. Hygroscopic engineering plastics like PA, PC, and PET need higher temperatures, longer times, and the very dry air of a desiccant dryer, while commodity resins like PP and PE barely absorb water and may need only a short hot-air pass to drive off surface moisture. The operator sets the temperature and bed depth from the resin maker's data, since too little drying leaves defects and too much degrades the polymer. In a molding cell the hopper usually mounts on the Mounting Frame directly over the machine throat so dried resin feeds straight down with no chance to reabsorb water, and the Vacuum Loader keeps it supplied from a central resin line. The main upkeep is changing the Filter Cartridge and verifying the Air Thermocouple reading so the resin sees the temperature the recipe calls for.
Resin Drying Hopper parts and their functions
8 top-level parts · 54 parts in total · full bill of materials below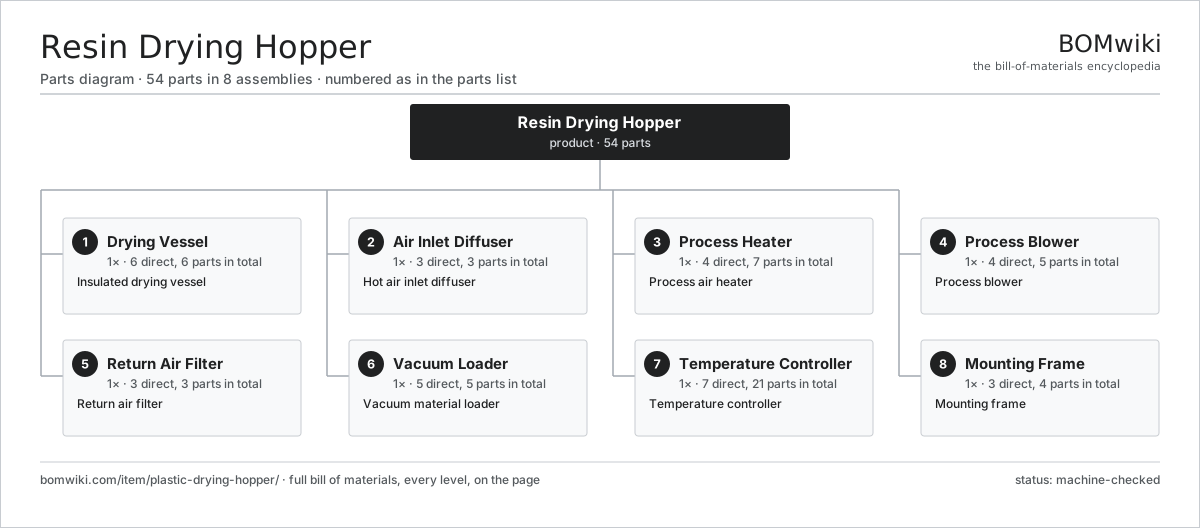
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Drying Vessel 6 parts | 1× | Insulated drying vessel |
| 2 | Air Inlet Diffuser 3 parts | 1× | Hot air inlet diffuser |
| 3 | Process Heater 4 parts | 1× | Process air heater |
| 4 | Process Blower 4 parts | 1× | Process blower |
| 5 | Return Air Filter 3 parts | 1× | Return air filter |
| 6 | Vacuum Loader 5 parts | 1× | Vacuum material loader |
| 7 | Temperature Controller 7 parts | 1× | Temperature controller |
| 8 | Mounting Frame 3 parts | 1× | Mounting frame |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Resin Drying Hopper
8 top-level lines · 43 rows shown · 54 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Drying Vessel 6 parts | plastic-drying-hopper-vessel | 1× | 1 | 6 | assembly |
| 1.1 | Inner Cone | plastic-drying-hopper-inner-cone | 1× | 1 | · | part |
| 1.2 | Outer Shell | plastic-drying-hopper-outer-shell | 1× | 1 | · | part |
| 1.3 | Insulation Blanket | plastic-drying-hopper-insulation | 1× | 1 | · | part |
| 1.4 | Sight Glass | plastic-drying-hopper-sight-glass | 1× | 1 | · | part |
| 1.5 | Discharge Slide | plastic-drying-hopper-discharge-slide | 1× | 1 | · | part |
| 1.6 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 2 | Air Inlet Diffuser 3 parts | plastic-drying-hopper-air-inlet | 1× | 1 | 3 | assembly |
| 2.1 | Diffuser Cone | plastic-drying-hopper-diffuser-cone | 1× | 1 | · | part |
| 2.2 | Spreader Plate | plastic-drying-hopper-spreader-plate | 1× | 1 | · | part |
| 2.3 | Inlet Flange | plastic-drying-hopper-inlet-flange | 1× | 1 | · | part |
| 3 | Process Heater 4 parts | plastic-drying-hopper-heater | 1× | 1 | 7 | assembly |
| 3.1 | Heating Element | heating-element | 3× | 3 | · | part |
| 3.2 | Heater Housing | plastic-drying-hopper-heater-housing | 1× | 1 | · | part |
| 3.3 | Air Thermocouple | plastic-drying-hopper-air-thermocouple | 2× | 2 | · | part |
| 3.4 | Thermal Fuse | thermal-fuse | 1× | 1 | · | part |
| 4 | Process Blower 4 parts | plastic-drying-hopper-blower | 1× | 1 | 5 | assembly |
| 4.1 | Blower Impeller | plastic-drying-hopper-blower-impeller | 1× | 1 | · | part |
| 4.2 | Blower Motor | plastic-drying-hopper-blower-motor | 1× | 1 | · | part |
| 4.3 | Blower Housing | plastic-drying-hopper-blower-housing | 1× | 1 | · | part |
| 4.4 | Ball Bearing | ball-bearing | 2× | 2 | · | part |
| 5 | Return Air Filter 3 parts | plastic-drying-hopper-filter | 1× | 1 | 3 | assembly |
| 5.1 | Filter Cartridge | plastic-drying-hopper-filter-cartridge | 1× | 1 | · | part |
| 5.2 | Filter Housing | plastic-drying-hopper-filter-housing | 1× | 1 | · | part |
| 5.3 | Filter Seal | plastic-drying-hopper-filter-seal | 1× | 1 | · | part |
| 6 | Vacuum Loader 5 parts | plastic-drying-hopper-loader | 1× | 1 | 5 | assembly |
| 6.1 | Vacuum Receiver | plastic-drying-hopper-receiver | 1× | 1 | · | part |
| 6.2 | Vacuum Pump | plastic-drying-hopper-vacuum-pump | 1× | 1 | · | part |
| 6.3 | Level Probe | plastic-drying-hopper-level-probe | 1× | 1 | · | part |
| 6.4 | Dump Valve | plastic-drying-hopper-dump-valve | 1× | 1 | · | part |
| 6.5 | Water Hose | water-hose | 1× | 1 | · | part |
| 7 | Temperature Controller 7 parts | plastic-drying-hopper-control | 1× | 1 | 21 | assembly |
| 7.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 7.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 7.3 | Operator Display | plastic-drying-hopper-display | 1× | 1 | · | part |
| 7.4 | Relay | relay | 4× | 4 | · | part |
| 7.5 | Power Supply | power-supply | 1× | 1 | · | part |
| 7.6 | Connector | connector | 12× | 12 | · | part |
| 7.7 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
| 8 | Mounting Frame 3 parts | plastic-drying-hopper-frame | 1× | 1 | 4 | assembly |
| 8.1 | Support Stand | plastic-drying-hopper-stand | 1× | 1 | · | part |
| 8.2 | Mounting Bracket | plastic-drying-hopper-mount-bracket | 2× | 2 | · | part |
| 8.3 | Fastener Set | fastener-set | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Industrial FDM Printer
98 parts · shares 7 with this page
Soap Plodder
61 parts · shares 7 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $5k–$2M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| atlascopco.com ↗ | Stockholm, SE | Compressors & industrial | 10 units | 12–20 wks |
|
🇦🇹Andritz
andritz.com ↗
|
Graz, AT | Process plants & machinery | 10 units | 12–20 wks |
| buhlergroup.com ↗ | Uzwil, CH | Food & materials processing | 10 units | 12–20 wks |
| gea.com ↗ | Düsseldorf, DE | Process technology | 10 units | 12–20 wks |
| mhi.com ↗ | Tokyo, JP | Heavy machinery | 10 units | 12–20 wks |
984-word article