Pressure Forming Machine
ProductOverview
A pressure forming machine is a thermoformer that pushes the hot sheet onto the mold with compressed air as well as pulling it with vacuum. Plain vacuum forming can only apply about one atmosphere of force, which limits how sharply the sheet will copy fine detail. By sealing a pressure box against the back of the sheet and filling it with air at several atmospheres, pressure forming applies several times that force, so the plastic is driven hard into crisp radii, fine texture, and sharp features. The result is a part that rivals injection molding for surface detail and definition while keeping the low tooling cost and large-part capability of thermoforming, which makes it the method of choice for medical enclosures, machine covers, kiosk panels, and other large cosmetic parts made in moderate volumes.
The machine builds and holds force in the Machine Frame, heats the sheet with the Dual Heater, presses on it with the Pressure Box, forms it over the Mold Station, supplies air and vacuum through the Air System, holds tool temperature with the Mold Cooling System, finishes the part on the CNC Trim Station, and runs from the Machine Controller.
Frame and clamp
Because pressure forming puts air pressure behind the sheet, the Machine Frame must hold the pressure box closed against that internal force, so it is heavier than a vacuum former. A welded Base Frame reacts the load, and a powered Clamp Frame driven by Clamp Cylinder cylinders on Linear Guide Rail rails pins the sheet flat and seals it between the box and the mold. The clamp force has to exceed the box pressure acting over the sheet area, or the box leaks and the part loses detail.
Heating
The Dual Heater is a dual bank above and below the sheet, because the thicker sheets pressure forming uses need heat driven in from both sides to reach the core without scorching the surface. Banks of quartz Heating Element elements are grouped into many Heater Zone zones so heat can be tuned across the sheet, and a set of Sheet Pyrometer sensors closes the loop on sheet temperature. A Heater Slide moves the banks clear before forming. Even heating is critical here: pressure can force a slightly uneven sheet into the mold, but uneven temperature still shows up as uneven wall thickness and stress in the finished part.
Pressure box and forming
The defining part is the Pressure Box. Its Pressure Box Shell is a steel chamber rated for several bar that seals against the back of the clamped sheet through the Box Face Seal, with a Relief Valve for safety and Pressure Sensor feedback on box pressure. When the Mold Station lifts the mold against the sheet and the box fills with air, the sheet is pressed into the mold while Vent Slot slots on the mold side pull a vacuum, so pressure and vacuum work together to force the plastic into every detail. A heated Plug Assist pre-stretches the sheet into deep features first so the walls stay even, and where a part has undercuts, retracting Moving Core cores form them and then withdraw so the part can come out.
The mold
The Detailed Mold is what justifies the whole machine. It is a CNC-machined aluminium Mold Cavity held at a controlled temperature, carrying sharp radii and, through etched Texture Insert inserts, a grained or patterned surface that the high forming pressure reproduces faithfully. Drilled Cooling Line channels run coolant through the tool so each part sets fast and at the same temperature, which keeps the parts dimensionally consistent across a run. Aluminium is used because it machines to fine detail and conducts heat well for cooling, and because the moderate volumes of pressure forming do not justify the cost of hardened injection tooling.
Air, cooling, trim, and use
The Air System supplies the forces. An Air Compressor charges a Pressure Reservoir so the box pressure rises quickly, a Vacuum Pump evacuates the mold side, a Pressure Regulator sets the forming pressure for the part, and a Valve Bank switches it all in sequence. The Mold Cooling System system runs a Mold Chiller and Coolant Pump through a Cooling Manifold to hold the tool steady. Because pressure-formed parts carry too much detail and too many openings for a simple punch, they go to the CNC Trim Station station, a 3-axis router on Ball Screw and Linear Guide Rail axes driven by Servo Motor servos, that trims the outline and cuts openings against a vacuum Trim Table. The Machine Controller cabinet sequences heat, clamp, lift, pressure, vacuum, and cooling, with an Microcontroller running the cycle and the operator setting recipes on the Operator Screen. Pressure forming sits between vacuum forming and injection molding: it gives near-injection surface quality on large parts at tooling costs and volumes where an injection mold would never pay back, which is why it dominates cosmetic enclosures for medical, instrument, and equipment housings.
Pressure Forming Machine parts and their functions
8 top-level parts · 217 parts in total · full bill of materials below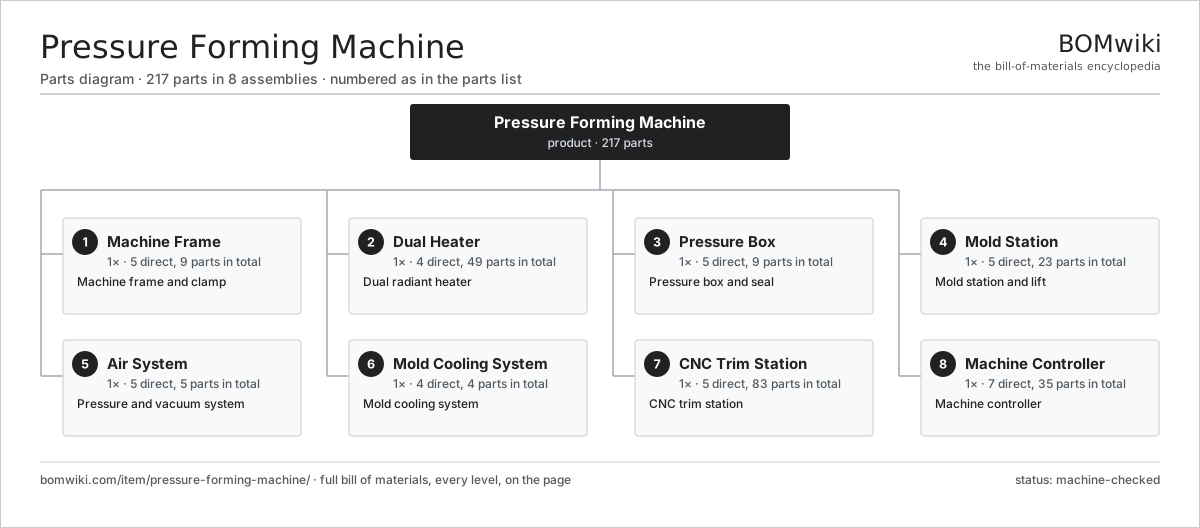
| # | Part | Qty | What it does |
|---|---|---|---|
| 1 | Machine Frame 5 parts | 1× | Machine frame and clamp |
| 2 | Dual Heater 4 parts | 1× | Dual radiant heater |
| 3 | Pressure Box 5 parts | 1× | Pressure box and seal |
| 4 | Mold Station 5 parts | 1× | Mold station and lift |
| 5 | Air System 5 parts | 1× | Pressure and vacuum system |
| 6 | Mold Cooling System 4 parts | 1× | Mold cooling system |
| 7 | CNC Trim Station 5 parts | 1× | CNC trim station |
| 8 | Machine Controller 7 parts | 1× | Machine controller |
3D model
No 3D model yet. Have a CAD file of this? Add a 3D model — STL renders right on this page; STEP, FreeCAD, and OpenSCAD sources are welcome too (openly licensed, like all 3D models on BOMwiki).
Build & assembly graph
expand / collapse · shared sub-assemblies converge · links to related products · est. labourTap an assembly to expand/collapse · tap a part to open it · use “Open page” for any node · drag to pan, scroll to zoom.
Bill of materials for Pressure Forming Machine
8 top-level lines · 56 rows shown · 217 parts total · indented to 3 levels| # | Item / sub-assembly | Part no. | Qty/assy | Ext. qty | Parts | Type |
|---|---|---|---|---|---|---|
| 1 | Machine Frame 5 parts | pressure-forming-machine-frame | 1× | 1 | 9 | assembly |
| 1.1 | Base Frame | pressure-forming-machine-base-frame | 1× | 1 | · | part |
| 1.2 | Clamp Frame | pressure-forming-machine-clamp-frame | 1× | 1 | · | part |
| 1.3 | Clamp Cylinder | pressure-forming-machine-clamp-cylinder | 2× | 2 | · | part |
| 1.4 | Linear Guide Rail | linear-guide | 4× | 4 | · | part |
| 1.5 | Fastener Set | fastener-set | 1× | 1 | · | part |
| 2 | Dual Heater 4 parts | pressure-forming-machine-heater | 1× | 1 | 49 | assembly |
| 2.1 | Heating Element | heating-element | 32× | 32 | · | part |
| 2.2 | Heater Zone | pressure-forming-machine-heater-zone | 12× | 12 | · | part |
| 2.3 | Sheet Pyrometer | pressure-forming-machine-pyrometer | 4× | 4 | · | part |
| 2.4 | Heater Slide | pressure-forming-machine-heater-slide | 1× | 1 | · | part |
| 3 | Pressure Box 5 parts | pressure-forming-machine-pressure-box | 1× | 1 | 9 | assembly |
| 3.1 | Pressure Box Shell | pressure-forming-machine-box-shell | 1× | 1 | · | part |
| 3.2 | Box Face Seal | pressure-forming-machine-box-seal | 1× | 1 | · | part |
| 3.3 | Relief Valve | pressure-forming-machine-relief-valve | 1× | 1 | · | part |
| 3.4 | Pressure Sensor | pressure-sensor | 2× | 2 | · | part |
| 3.5 | O-Ring Set | oring-set | 4× | 4 | · | part |
| 4 | Mold Station 5 parts | pressure-forming-machine-mold-station | 1× | 1 | 23 | assembly |
| 4.1 | Mold Platen | pressure-forming-machine-mold-platen | 1× | 1 | · | part |
| 4.2 | Lift Cylinder | pressure-forming-machine-lift-cylinder | 1× | 1 | · | part |
| 4.3 | Detailed Mold 4 parts | pressure-forming-machine-detail-mold | 1× | 1 | 18 | assembly |
| 4.3.1 | Mold Cavity | pressure-forming-machine-mold-cavity | 1× | 1 | · | part |
| 4.3.2 | Vent Slot | pressure-forming-machine-vent-slot | 12× | 12 | · | part |
| 4.3.3 | Texture Insert | pressure-forming-machine-texture-insert | 4× | 4 | · | part |
| 4.3.4 | Cooling Line | pressure-forming-machine-cooling-line | 1× | 1 | · | part |
| 4.4 | Plug Assist | pressure-forming-machine-plug-assist | 1× | 1 | · | part |
| 4.5 | Moving Core | pressure-forming-machine-moving-core | 2× | 2 | · | part |
| 5 | Air System 5 parts | pressure-forming-machine-air-system | 1× | 1 | 5 | assembly |
| 5.1 | Air Compressor | pressure-forming-machine-air-compressor | 1× | 1 | · | part |
| 5.2 | Pressure Reservoir | pressure-forming-machine-air-reservoir | 1× | 1 | · | part |
| 5.3 | Vacuum Pump | pressure-forming-machine-vacuum-pump | 1× | 1 | · | part |
| 5.4 | Valve Bank | pressure-forming-machine-valve-bank | 1× | 1 | · | part |
| 5.5 | Pressure Regulator | pressure-forming-machine-regulator | 1× | 1 | · | part |
| 6 | Mold Cooling System 4 parts | pressure-forming-machine-cooling | 1× | 1 | 4 | assembly |
| 6.1 | Mold Chiller | pressure-forming-machine-chiller | 1× | 1 | · | part |
| 6.2 | Coolant Pump | coolant-pump | 1× | 1 | · | part |
| 6.3 | Cooling Manifold | pressure-forming-machine-mold-manifold | 1× | 1 | · | part |
| 6.4 | Pressure Sensor | pressure-sensor | 1× | 1 | · | part |
| 7 | CNC Trim Station 5 parts | pressure-forming-machine-trim-cnc | 1× | 1 | 83 | assembly |
| 7.1 | Router Spindle | pressure-forming-machine-router-spindle | 1× | 1 | · | part |
| 7.2 | Trim Table | pressure-forming-machine-trim-table | 1× | 1 | · | part |
| 7.3 | Ball Screw | ball-screw | 3× | 3 | · | part |
| 7.4 | Servo Motor 4 parts | servo-motor | 3× | 3 | 24 | assembly |
| 7.4.1 | Stator Assembly 3 parts + deeper › | stator-assembly | 1× | 3 | 3 | assembly |
| 7.4.2 | Rotor Assembly 4 parts + deeper › | rotor-assembly | 1× | 3 | 19 | assembly |
| 7.4.3 | Encoder | encoder | 1× | 3 | · | part |
| 7.4.4 | Motor Housing | motor-housing | 1× | 3 | · | part |
| 7.5 | Linear Guide Rail | linear-guide | 6× | 6 | · | part |
| 8 | Machine Controller 7 parts | pressure-forming-machine-control | 1× | 1 | 35 | assembly |
| 8.1 | Bare PCB | pcb-bare | 1× | 1 | · | part |
| 8.2 | Microcontroller | mcu | 1× | 1 | · | part |
| 8.3 | Operator Screen | pressure-forming-machine-hmi | 1× | 1 | · | part |
| 8.4 | Power Supply | power-supply | 1× | 1 | · | part |
| 8.5 | Relay | relay | 10× | 10 | · | part |
| 8.6 | Connector | connector | 20× | 20 | · | part |
| 8.7 | Wire Bundle | wire-bundle | 1× | 1 | · | part |
Related products
same domain, ranked by shared parts Industrial Ultrasonic Cleaner
787 parts · shares 21 with this page
Micro Injection Molding Machine
704 parts · shares 21 with this page
 Rubber Extrusion Line
524 parts · shares 21 with this page
 Thermal Spray Coating System
866 parts · shares 21 with this page
 Continuous Galvanizing Line
1,296 parts · shares 20 with this page
Sourcing: possible vendors
Prices, MOQ, and lead times are algorithmic estimates, not quotes, and not claims about these companies. Company mappings are curated by keyword; est. price band $5k–$2M. How estimates work| Vendor | HQ | Specialty | MOQ | Lead time |
|---|---|---|---|---|
| atlascopco.com ↗ | Stockholm, SE | Compressors & industrial | 10 units | 12–20 wks |
|
🇦🇹Andritz
andritz.com ↗
|
Graz, AT | Process plants & machinery | 10 units | 12–20 wks |
| buhlergroup.com ↗ | Uzwil, CH | Food & materials processing | 10 units | 12–20 wks |
| gea.com ↗ | Düsseldorf, DE | Process technology | 10 units | 12–20 wks |
| mhi.com ↗ | Tokyo, JP | Heavy machinery | 10 units | 12–20 wks |
934-word article